Capital Carbon Expands rCB Capacity To Tackle Supply Chain Issues
- By Gaurav Nandi
- January 14, 2025
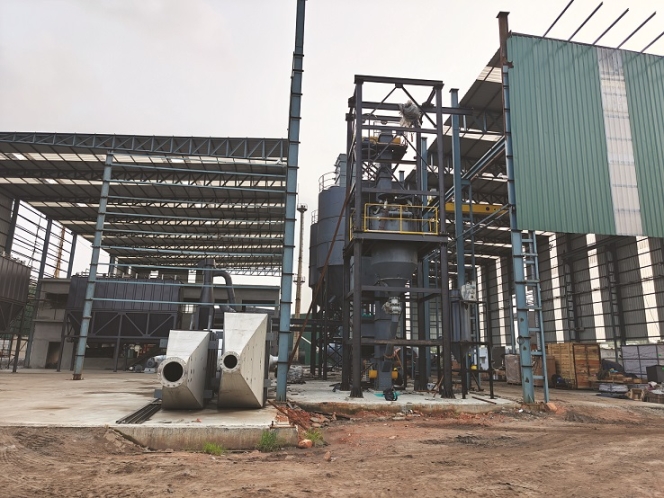
The Tamil Nadu-based company’s greenfield expansion will propel its rCB capacity from 5,000-20,000 metric tonnes. Director Ravi Rathi explained that there has been a change in attitude towards rCB within tyre companies, leading to heightened demand.
Tamil Nadu-based Capital Carbon is expanding its recovered carbon black (rCB) capacity by 15,000 metric tonnes with a new greenfield project at Gummidipoondi. The plant is slated to become operational by January 2025 and boost the capacity from 5,000 metric tonnes to 20,000 metric tonnes, annually.
Speaking to Tyre Trends, Director Ravi Rathi explained, “The decision to pursue a greenfield expansion in the rCB sector stemmed from the rapid development of this innovative product over the past four to five years. Given our background in the pyrolysis business, expanding into rCB felt like a natural progression. rCB is still a relatively new product and both manufacturers and users are in the process of learning about its applications. When we first began exploring this market, around four years ago, it was challenging. Many tyre manufacturers would dismiss our proposals even before we could present our case as they were hesitant to incorporate recycled materials into their mainstream formulations.”
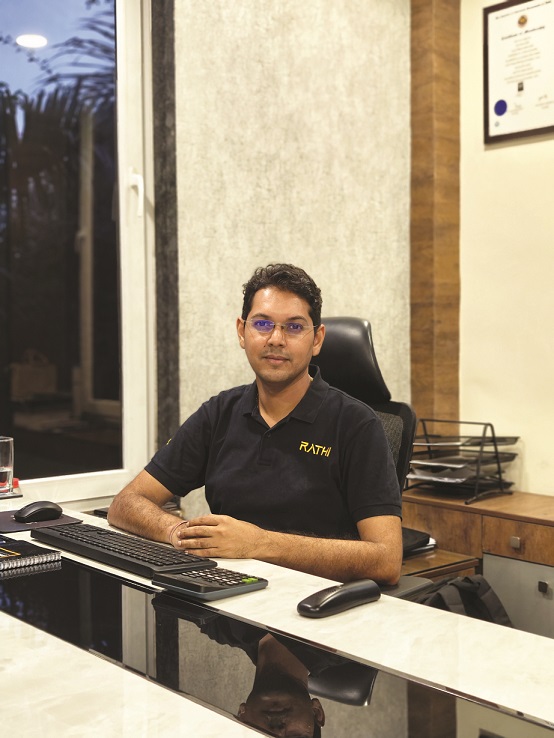 “However, in recent years, attitudes have shifted significantly due to increasing emphasis on sustainability and circular economy principles. The industry is now more open to integrating green products. We started with a modest capacity of 5,000 metric tonnes per annum, which allowed us to gain insights into customer needs. Gradually, we scaled our operations from small quantities to commercial sales. The key driver for our recent expansion is customer demand. We have obtained product approval, and customers are eager to purchase rCB,” he added.
He also noted that companies wanted assurance that the demands could be met consistently, which was also a factor behind the expansion. Furthermore, having multiple units also allows the company to manage any potential supply chain issues, effectively. “If a minor problem arises in one unit, we can still supply material from another, minimising disruptions for our customers,” said Rathi.
The entire CAPEX for the greenfield plant is set at INR 20 crore.
Pyrolysis to rCB
Capital Carbon commenced operations in 2012 with a modest pyrolysis capacity of 10 tonnes per day. Over the years, it has consistently expanded its capacity, increasing to 150 metric tonnes per day. The company has also bolstered its backend operations, enhancing sourcing capabilities and adding substantial shredding and crumbing capacity.
Additionally, Capital Carbon has focused on value-added products including pyrolysis oil distillation and rCB. As of now, it operates a shredding capacity of 120,000 metric tonnes per annum for captive consumption. This capacity is supplemented by sourcing contaminated tyre bales, which typically have 20-30 percent rubber contamination. This material is cleaned to yield 98 percent pure steel, with the remaining rubber used for pyrolysis, creating a separate business vertical.
Currently, the company processes approximately 50,000 to 52,000 metric tonnes of tyres per annum through its pyrolysis operations. In terms of value addition, Capital Carbon produces between 20,000 to 24,000 tonnes of pyrolysis oil, annually.
When asked about the motivation behind establishing a pyrolysis plant, Rathi noted, “My father worked at Birla Carbon and retired in 2019. Although we lacked prior business experience, we were inspired by the industrial upbringing and the promising potential of the pyrolysis sector. Following the completion of my chartered accountancy studies, I decided to pursue this opportunity.”
He acknowledged that pyrolysis often has a negative reputation in India, where it is sometimes viewed as a ‘dirty business’. To combat this perception, Capital Carbon prioritises quality management and environmental responsibility in its operations. IT employs fuel-based heating methods in its pyrolysis process as electric heating is generally not feasible due to the high volumes involved in tyre pyrolysis. The initial heating requires some fuel, which can include biomass or pyrolysis oil, but the system becomes self-sufficient once it reaches a certain temperature.
The primary outputs from the pyrolysis process include fuel oil, carbon char (used as raw material for rCB or as an alternative energy source for cement plants), steel wires and pyrolysis gases, which are utilised for heating purposes.
He highlighted that the pyrolysis oil produced is of high quality with low sulfur and carbon content, making it cleaner than many conventional heating fuels used in India.
Quality control
The company’s sourcing strategy primarily focuses on domestic suppliers. It procures rejected tyres and dealer returns from various companies, which constitute a substantial portion of the feedstock. This local sourcing approach ensures that it maintains a steady supply of raw materials
Following sourcing, the production of recovered carbon black involves several critical steps. Initially, tyres are shredded to extract carbon black, steel and other components. The distinction in product application necessitates tailored processing methods.
For instance, producing carbon char for energy requires less stringent technical specifications compared to producing carbon black intended for high-performance applications, such as tyre manufacturing or footwear.
“The quality of the final product begins with meticulous sorting of tyres to determine suitability for pyrolysis. This initial step is vital for ensuring consistent output quality. Following sorting, the tyres are shredded into steel-free rubber chips of 15-20 millimetres. During pyrolysis, we focus on maintaining specific quality parameters for the pyrochar produced. This includes stringent controls to limit ash content, which must remain below 20-22 percent to ensure product consistency. The handling of impurities such as wires and stones in the pyrochar is essential. Post-processing, the pyrochar is milled to fine particle sizes (10-15 microns), enhancing its surface area for better compatibility with rubber compounds,” explained Rathi.
Once the recovered carbon black is processed, palletisation becomes the next step. This method streamlines handling and ensures that the product meets industry standards. While the equipment resembles that used for traditional carbon black, adaptations are necessary to accommodate the unique characteristics of recovered carbon black.
“To facilitate customer adoption, we offer tailored packaging solutions including 25kg paper bags, EVA / LDPE bags and FIBC bags, allowing clients to integrate our products seamlessly into their existing production processes,” he added.
As the industry evolves, the need for standardised quality benchmarks for recovered carbon black has become increasingly clear. Major corporations have driven this change, leading ASTM to establish a dedicated committee (D36) focused on developing specific standards for recovered carbon black. Unlike conventional carbon black, which adheres to existing standards, recovered carbon black requires new metrics to account for its varied origins and compositions.
The committee is currently validating a series of standards including moisture content, pallet hardness and particle size analysis, specifically for rCB. This ongoing development is slated to enhance product credibility and facilitate broader market acceptance.
Commenting on the same lines, Rathi mentioned, “We maintain a dedicated quality lab to refine our production processes continually. Our focus on evolving our offerings has resulted in the introduction of two new grades of recovered carbon black, aimed at meeting diverse market needs. Our commitment to leveraging advanced machinery and improved grinding techniques reflects our proactive approach to quality enhancement and capacity expansion.”
Optimistic market outlook
The demand for recovered carbon black in India is poised for significant growth, driven by a strong shift toward sustainability. Customers are increasingly seeking high-quality suppliers, indicating a burgeoning market for rCB.
“Globally, rCB production currently accounts for less than one percent of total carbon black production, underscoring a substantial opportunity for expansion. As customer awareness and demand for sustainable products increase, we anticipate a corresponding rise in rCB consumption,” informed Rathi.
He added, “Many major corporations have committed to achieving carbon neutrality by 2050, necessitating immediate action to integrate green and circular products into their supply chains. As these companies strive to meet their net-zero targets, they are turning to recovered materials such as rCB to fulfil sustainability mandates. Our role is crucial in assisting these customers to achieve their goals through the production of eco-friendly and circular products derived from end-of-life tyres.”
Speaking on market opportunities, he said, “India remains our largest market, but we are also making significant inroads into Sri Lanka. The European market is particularly promising, though it presents challenges related to certifications and distribution. We are currently working on obtaining the necessary certifications, including ISCC Plus, to unlock this market potential.”
“Our immediate focus is on completing our current expansion project, after which we will enhance our pyrolysis capacity to align with the growing demand from our customers. As the volumes of recovered carbon black usage increase, we aim to be ready with sufficient supply,” he added.
He expects to penetrate the European market by the first half of FY26, following the completion of the current plant expansion.
Challenges in scaling production
“One of the primary challenges in scaling rCB production is the scarcity of raw materials. The supply of suitable feedstock is diverse and scattered, making it difficult to source consistently. In the past, customers struggled to understand the differences between recovered carbon black and virgin carbon black grades, often asking if we could produce specific grades like L550 or L660. However, as knowledge in the market has matured, customers are increasingly recognising that rCB is a distinct material requiring tailored processing approaches,” informed Rathi.
- Association of Natural Rubber Producing Countries
- ANRPC
- Monthly NR Statistical Report
- Natural Rubber
ANRPC Publishes Monthly NR Statistical Report For August 2026
- By TT News
- October 02, 2026
The Association of Natural Rubber Producing Countries (ANRPC) published its Monthly Natural Rubber Statistical Report for August 2026, noting firmer prices in several markets. Supply constraints, stable downstream demand and persistent geopolitical and macroeconomic uncertainty shaped the month. Renewed conflict and disruptions to major shipping routes added further pressure.
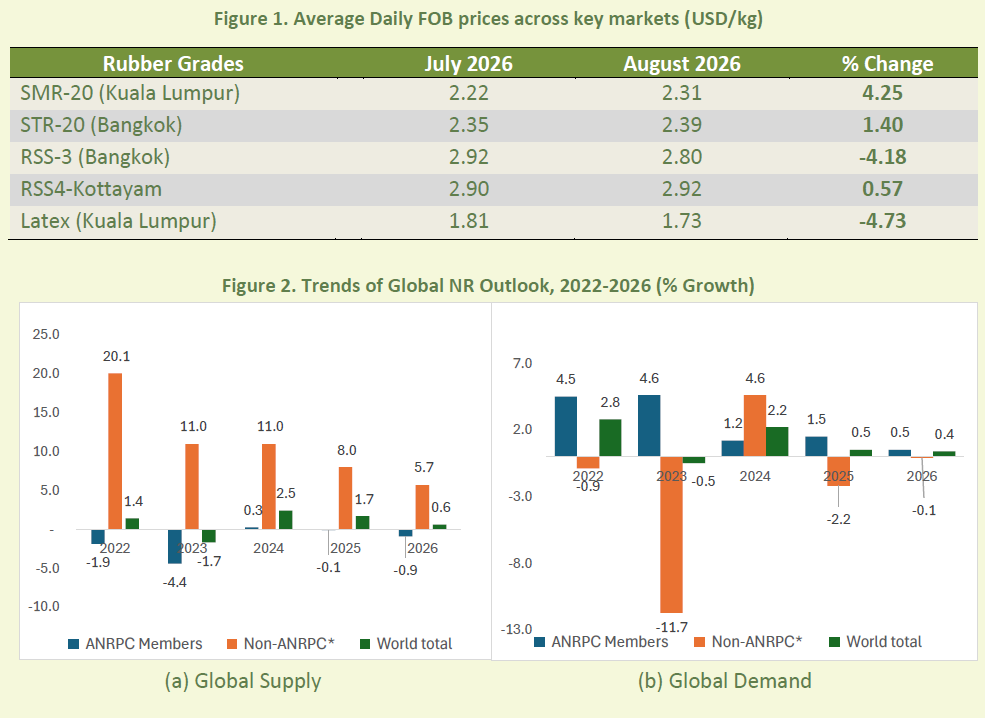
Physical prices for major grades moved in different directions. SMR-20 in Kuala Lumpur averaged USD 2.31 per kg, up 4.25 percent from July, while STR-20 in Bangkok rose 1.40 percent to USD 2.39 per kg. RSS-3 dropped 4.18 percent to USD 2.80 per kg, but RSS-4 in Kottayam gained 0.57 percent to USD 2.92 per kg. Latex-in-bulk fell 4.73 percent to USD 1.73 per kg. Brent crude averaged USD 91.08 per barrel, driven by concerns over possible restrictions on oil shipments through the Strait of Hormuz and wider Middle East instability, which raised energy supply risks and strengthened the oil market risk premium.
On trade, China's imports climbed 3.39 percent month-on-month, while India fell 10.18 percent and Malaysia dropped 8.24 percent; Viet Nam rose 5.08 percent. Exports advanced 5.63 percent in Viet Nam but declined in Thailand (-5.24 percent), Indonesia (-5.36 percent), Malaysia (-1.48 percent) and Cambodia (-1.88 percent).
Global production is projected to rise 0.6 percent to 15.039 million tons in 2026 from 14.952 million tonnes in 2025, after revisions to Thailand's 2025 output and updated 2026 estimates for Thailand, Malaysia and Indonesia. Weather, including erratic rainfall and drier Southeast Asian conditions, affected output. August 2026 production was estimated at 1.396 million tonnes, down 4.51 percent from 1.462 million tonnes a year earlier. Demand is forecast to grow 0.4 percent to 15.356 million tonnes in 2026 from 15.301 million tonnes, with the largest consumption gains expected in China, Malaysia and Cambodia. Prospects depend on vehicle sales, tyre production, shipping conditions and weather-related supply disruptions, while steady EV-linked demand supported modest growth led by China and India. The ringgit traded between RM4.02 per USD and RM4.09 per USD, and the baht between 32.68 and 33.34. The SHFE January 2027 contract averaged 18,109 CNY per tonne, up 7.78 percent month-on-month, while the SGX November 2026 contract averaged USD 2.24 per kg, up 4.32 percent.
HS HYOSUNG To Expand Mexico Investments From 2027 Under New State Agreement
- By TT News
- September 30, 2026
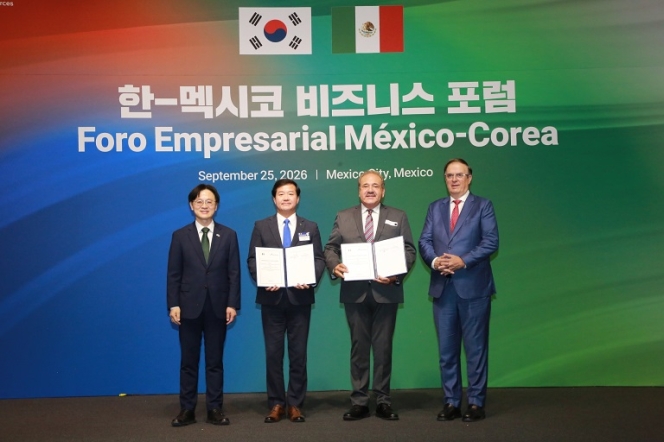
HS HYOSUNG has formalised a memorandum of understanding (MoU) with the State Government of San Luis Potosí, with the signing taking place at the World Trade Center Mexico City. The event formed part of the Korea-Mexico Business Forum, held alongside the Korean economic delegation's visit to Mexico.
Attending officials included Marcelo Ebrard, Mexico's Secretary of Economy, and Mario García Valdez, Secretary of Economic Development of San Luis Potosí. The two sides confirmed their shared resolve to back the company's local investment and regional growth. Separately, HS HYOSUNG's leadership met bilaterally with Secretary Ebrard to elaborate on its strategic vision and investment plans.
The agreement sets out a phased expansion of HS HYOSUNG's investments in San Luis Potosí beginning in 2027, with the goal of creating a major advanced materials production hub that bolsters supply for North American and wider global markets. The company's advanced materials span tyre cord, a flagship world-leading product, along with mobility, energy, aerospace and defence applications. Its North American operations, spanning Mexico and the United States, turn out tyre cord, airbag materials and mobility interior components for global leaders such as General Motors and Goodyear, underpinned by a highly dependable global supply chain.
Nak-yang Sung, CEO, HS HYOSUNG ADVANCED MATERIALS, said, “This investment goes beyond establishing a simple manufacturing base – it reflects our strategy to turn Mexico into a pivotal hub connecting North America with global supply networks. We are also committed to strengthening local supply chains and creating high-quality jobs to contribute directly to the region's industrial ecosystem.”
Kumho Petrochemical Group Shifts Focus To R&D and Speciality Materials
- By TT News
- September 25, 2026
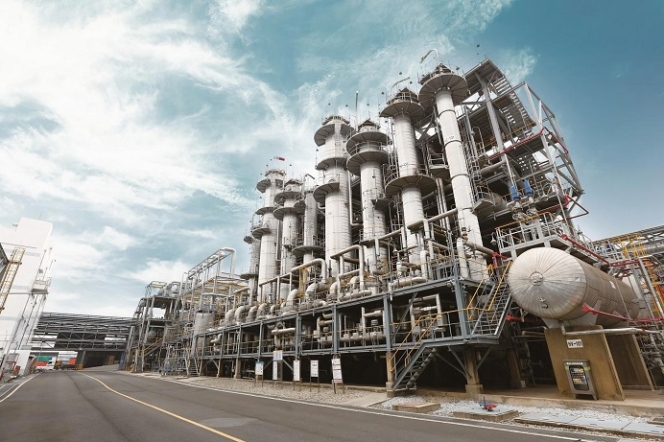
Kumho Petrochemical Group is steering its business towards research-driven, higher-value outputs as oversupply and soft demand continue to weigh on the worldwide petrochemical sector. The Seoul-based group outlined plans to boost spending on speciality chemicals, sustainable materials and novel production methods, a push intended to lift profits while building a foundation for future expansion.
Underlying the move is a deliberate evolution in the group's identity, from a bulk materials vendor to a provider of technology-backed solutions that address shifting customer requirements and stricter environmental rules. A central element of that effort involves widening the speciality lineup, exemplified by added capacity for solution styrene butadiene rubber, a synthetic rubber that enhances durability, rolling resistance and tread wear in high-performance electric vehicle tyres.
Environmental initiatives form another pillar. Facilities built by the company can trap approximately 76,000 metric tonnes of carbon dioxide each year, while separately developed technology turns recycled acrylonitrile butadiene styrene sourced from scrapped household appliances into automotive-grade interior components that satisfy performance standards and generate fewer emissions than conventional methods. The group has also joined forces with POSCO Future M and BEI on anode-free lithium-metal battery development.
Parallel technology-focused programmes are underway at affiliated units. Kumho P&B Chemicals is formulating water-based epoxy resins that curb volatile organic compound releases while incorporating more bio-based inputs to reduce carbon intensity. Kumho Mitsui Chemicals is advancing bio-based polyurethane systems and electric vehicle materials, alongside debottlenecking work to add 100,000 tonnes of annual methylene diphenyl diisocyanate capacity. Kumho Polychem, meanwhile, is targeting ethylene propylene diene monomer through low-temperature polymerisation paired with energy-efficiency improvements.
Birla Carbon Announces Asia-Wide Speciality Materials Price Hike Of Up To 15%
- By TT News
- September 22, 2026
Birla Carbon has confirmed a price increase of up to 15 percent for its Speciality Materials products across Asia, scheduled to take effect on 1 October 2026. The company pointed to significant and sustained rises in feedstock costs, driven partly by ongoing geopolitical instability and disruptions in global feedstock markets, as the reason behind the adjustment.
Although Birla Carbon pursued operational efficiencies, supply chain optimisation and disciplined cost management to soften the impact, the scale and persistence of the cost escalation left a price adjustment unavoidable. The company's sales teams will engage customers directly to explain the details and help them navigate the transition.
Comments (0)
ADD COMMENT