Refurbished tyre-recycling machines are emerging as a practical answer to rising compliance pressure and capital constraints across the sector. As demand grows for faster, lower-cost capacity expansion, Revyre Global’s decision to release a complete, operational processing line highlights how secondary equipment markets are becoming strategically relevant to recyclers.
Refurbished machines are finding renewed demand in the tyre-recycling industry as processors look to expand capacity quickly without the capital burden and long delivery cycles of new equipment.
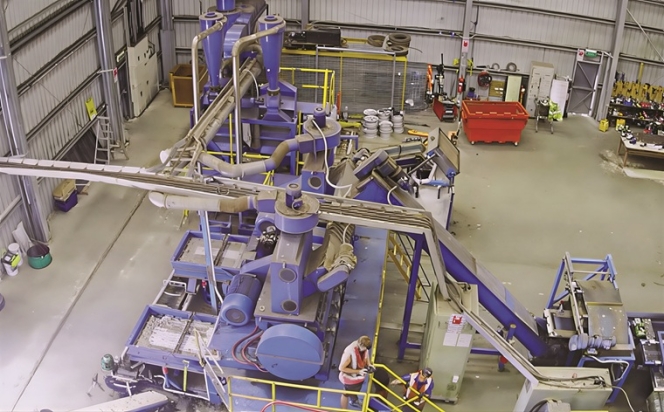
Against this backdrop, New Zealand-based recycling firm Revyre Global is releasing a suite of previously used, fully operational machinery from its tyre-recycling line, offering other recyclers access to proven processing systems spanning shredding, separation and granulation, along with critical spares to support uninterrupted operations.
Speaking to Tyre Trends exclusively, Chief Executive Officer Shaun Zukor noted, “Demand for refurbished tyre‑recycling equipment is expected to increase as global EPR regulations intensify and scrutiny grows around whole‑bale tyre handling. Many operators are seeking leaner, downsized plant and equipment configurations to meet compliance requirements while reducing capital expenditure. As regulatory pressure mounts, refurbished systems present a practical and cost‑effective solution for meeting mandated recycling obligations.”
The equipment sale aligns with Revyre’s broader strategy to expand capacity and scale into new markets, particularly in roading and water-proofing applications where demand for high‑quality recycled polymer products is growing rapidly. These sectors require higher production volumes and upgrading to next‑generation technology positions the company to fulfil those larger‑scale opportunities.
The line for sale can produce approximately two tonnes per hour of product, which is standard with current smaller operational outputs. The new processing line’s output is highly adaptable and could be rapidly configured to produce a range of materials based on market demand.
“This flexible production capability allowed the system to switch between product types without significant downtime or reconfiguration, enabling throughput levels that aligned competitively with industry standards. The ability to modify production on demand ensured efficient utilisation of capacity under varying operational requirements,” explained Zukor.
The primary target buyers of the company are new market entrants with vertically integrated operations, particularly those managing tyre‑collection networks. Such buyers can benefit from processing tyres earlier in the value chain, improving transport efficiency by reducing bulk volume and lowering the need for extensive pre‑processing at the final facility. This machinery offers an accessible entry point for organisations seeking scalable, cost‑efficient recycling capability.
TURNING THE BLADES
According to Zukor, Revyre’s existing mechanical tyre‑shredding system faced significant operational constraints due to its reliance on multiple moving components, which resulted in frequent breakdowns, high maintenance costs and extensive downtime.
The traditional multi‑stage process viz-a-viz shredding, rasping and grinding required substantial manual supervision and labour input, creating both inefficiencies and higher operating expenditure. These limitations collectively hindered scalability and consistent production performance, prompting the shift to more advanced and efficient technology.
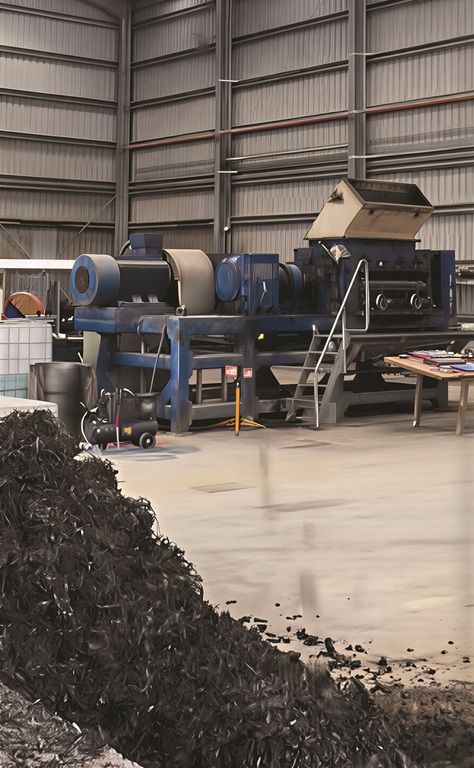 “The next‑generation system offers a markedly more automated process that consolidates material reduction into a single grinding stage. This significantly reduces maintenance requirements, labour dependency and risk of mechanical failure. The improved system delivers higher throughput rates, more consistent and higher‑purity output materials and substantially lower contamination levels. In addition, improved energy efficiency across the system contributes to lower operational costs and a more sustainable processing footprint,” explained Zukor.
While all used equipment carries inherent operational risks, the system on sale recently underwent a repair and replacement of key wear components. “With proper upkeep, the line is expected to deliver at least another 10 years of reliable performance. The sale package includes spare parts and maintenance support to help buyers manage operational continuity and compliance requirements,” added Zukor.
He also noted that providing reliable, industrial‑grade equipment lowers capital barriers and reduces development time for new entrants. Furthermore, by extending the lifecycle of existing machinery, Revyre reinforces the principles of circularity, effectively recycling the recycling equipment, which is aligned with the organisation’s mission and sustainability values.
Currently, the company is actively advancing towards fully automated, digitally controlled recycling systems to reduce human exposure to mechanical processes and improve operational safety.
Increased automation will also reduce labour overheads and enables more consistent, globally competitive production output, supporting its long‑term vision of efficient, technology‑driven resource recovery.
“This upgrade is a major step towards establishing Revyre as a leader in high‑value polymer recovery, enabling production of superior‑grade materials for roading, water-proofing and masterbatch applications. Enhanced quality, scalability and process efficiency will strengthen our circular‑economy partnerships including potential collaborations with tyre manufacturers seeking reliable, high‑performance recycled inputs,” noted Zukor.
Revyre’s equipment sale underlines a broader shift in tyre recycling where affordability, compliance and speed to market matter as much as technology. By extending machinery lifecycles while upgrading its own capability, the company reflects an industry increasingly viewing refurbished systems as both an economic and circular solution.
- Swarnakaruna Princeton Rubber Industries
- N Swarnalatha
- Princenton Rubber Industries
- retreading
- tyre
- Ashish Kumar Isukapati
- IFCI Venture Capital
State-Backed Capital Powers Swarnakaruna Princeton’s Expansion Push
- By Gaurav Nandi
- November 02, 2026
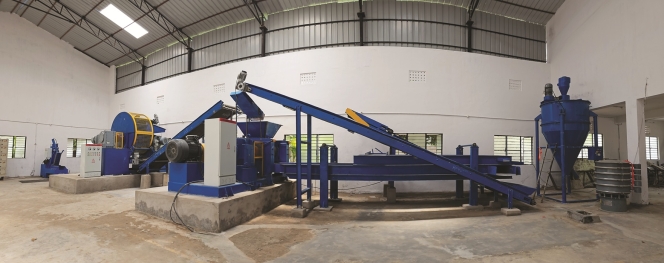
Swarnakaruna Princeton Rubber Industries has built capacity to recycle about 96,000 end-of-life tyres annually after government-backed financing helped the Visakhapatnam company transition from processing buffing waste to recycling whole tyres. The recycler is now targeting larger industrial buyers while exploring tyre imports to lower raw-material costs.
India’s push to formalise its end-of-life tyre recycling ecosystem is creating room for smaller recyclers to scale, but access to capital, machinery reliability, raw-material costs and the economics of producing higher-grade crumb rubber remain significant constraints.
Visakhapatnam-based Swarnakaruna Princeton Rubber Industries Private Limited offers a case in point. The company has expanded from a small operation processing buffing powder to a whole-tyre recycling business capable of producing around 300–400 tonnes of crumb rubber a month following financial support channelled through IFCI Venture Capital under a government-backed programme for Scheduled Caste entrepreneurs.
The business traces its roots to 2014, when Managing Director N Swarnalatha established K.S. Princeton Rubber Industries after approaching the District Industries Centre in Visakhapatnam with plans to become an entrepreneur.
The original operation had a single grinder and relied on buffing powder as its principal feedstock because it lacked the equipment required to process complete end-of-life tyres.
“The company started in 2014, but the setup was very minimal. We had just one grinder and were not capable of recycling a whole tyre, so buffing powder was our raw material,” said Swarnakaruna Princeton Rubber Industries Chief Executive Officer Ashish Kumar Isukapati.
That model began changing in 2018 when the company sought funding from IFCI Venture Capital Limited. The proprietorship was subsequently converted into a private limited company as part of the process of securing the investment. Funding was eventually released in stages, with commercial production from the expanded facility beginning in August 2024.
According to Isukapati, the project received about INR 50 million from IFCI Venture Capital, alongside a promoter contribution of INR 17.1 million. The overall project cost was approximately INR 67.21 million.
The money was deployed largely towards machinery and rebuilding and expanding the existing manufacturing premises.
Isukapati said the financing was particularly significant because conventional access to growth capital can prove difficult for first-generation entrepreneurs.
TYRES TO CRUMB
The expanded operation can process roughly 8,000 end-of-life tyres each month, equivalent to around 96,000 tyres annually, according to Isukapati. At the upper end of production, the facility can manufacture around 400 tonnes of crumb rubber a month, while recovered steel accounts for roughly 25 percent of output by weight or around 100 tonnes at that production level.
The company currently sells entirely into the domestic market, with Kerala representing its largest destination. It also supplies TVS Sundaram Industries in Chennai.
However, the economics vary considerably according to crumb size and end application.
More than 70 percent of the company’s current crumb-rubber production goes to non-tyre applications, particularly rubber-mat manufacturers in Kerala. These customers typically consume 20 and 24 mesh material. TVS Sundaram Industries takes roughly 60–80 tonnes a month, with the company supplying 30-mesh crumb rubber.
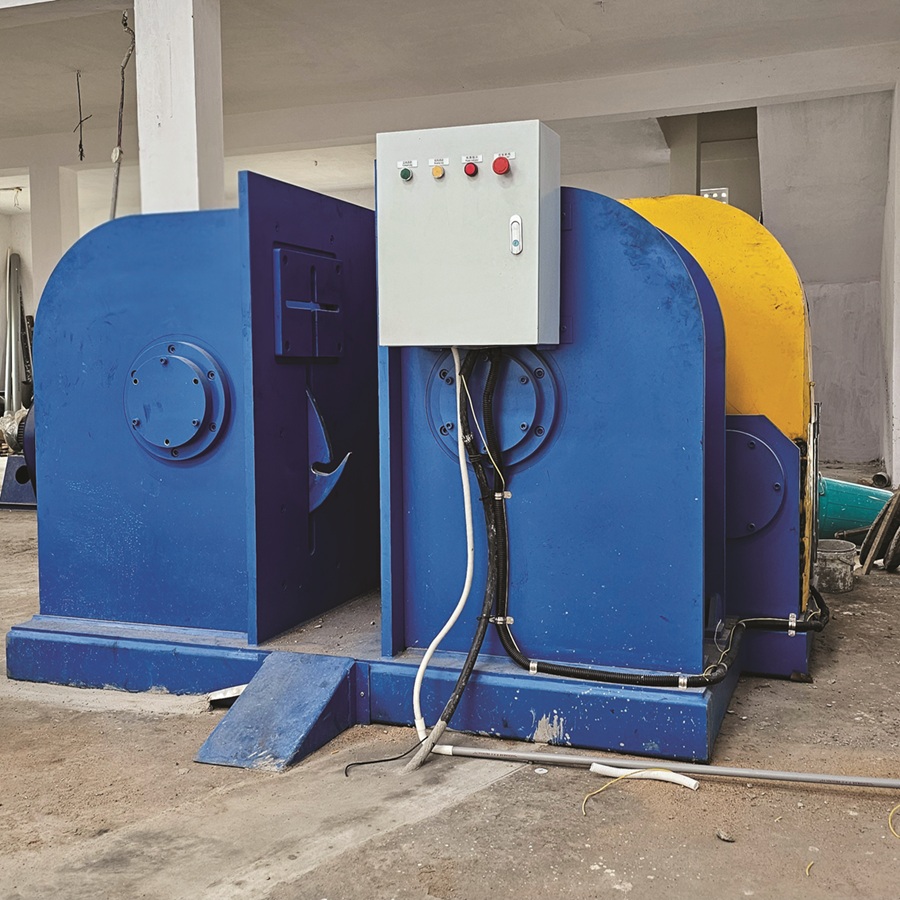
Tyre-related customers typically require finer grades such as 40, 60 and 80 mesh crumb rubber. The company has pulverising equipment capable of producing material in those ranges, but finer grinding lowers throughput and changes the economics of the operation.
“We are capable of manufacturing the higher meshes, but the overall output comes down. We have to balance which mesh we manufacture against the quantity we can produce because crumb rubber itself is a relatively low-priced product. The way to generate sustainable revenue is through volume,” Isukapati said.
That volume-quality equation has become particularly important as the recycler seeks to tap larger customers closer to its Visakhapatnam plant.
One of its main targets is HINCOL, which Isukapati said operates a facility locally and requires around 500 tonnes of crumb rubber a month. The company has so far been unable to fully address that opportunity because of the combination of volume, quality specifications and tender pricing.
Isukapati sees similar opportunities with buyers across the eastern and southern tyre and rubber manufacturing belt. He estimates that potential demand within roughly 300 kilometres of its operation could exceed 1,000 tonnes a month.
The challenge is converting that proximity into profitable sales.
PORT OPPORTUNITY
The company currently sources a significant portion of its tyres through Andhra Pradesh State Road Transport Corporation auctions. And the company is also seeking a licence to import end-of-life tyres, a move it believes could allow it to leverage its proximity to Visakhapatnam port and reduce feedstock costs.
“We are trying to capitalise on Visakhapatnam port and have applied for an import licence. If that works out, we could spend less on raw material, which would give us an advantage in offering a more competitive price,” Isukapati said.
The company’s expansion has not been without setbacks. Location presents a significant constraint. The facility operates on a plot of about 980 square yards, where incoming tyres, finished crumb rubber and recovered steel all have to be stored and managed. Expanding towards the 500-tonne monthly volumes sought by larger customers could therefore require the company to address its space limitations.
Technical support and spare-part availability are also more difficult in Visakhapatnam than in established manufacturing clusters, Isukapati said.
BIGGER CHALLENGE
Swarnakaruna does not currently operate a dedicated research and development department. Product development and process adjustments are handled by its production manager and technical staff, while third-party laboratories are occasionally used when customers require test reports.
Beyond the company’s own expansion, Isukapati sees feedstock pricing as one of the biggest problems confronting India’s mechanical tyre recyclers.
Waste-tyre prices can rise when pyrolysis operators increase production, but crumb-rubber producers cannot necessarily pass those higher costs to customers because buyers have multiple competing suppliers.
He also called for greater policy attention to the procurement and channelisation of waste tyres, arguing that mechanical recyclers do not necessarily receive a commercial advantage for converting end-of-life tyres into reusable rubber products.
His comments come as India’s tyre-recycling ecosystem adjusts to extended producer responsibility requirements and increasing competition for waste-tyre feedstock.
For the tyre recycler, the next phase will therefore be less about simply adding equipment and more about achieving scale economically. The company is seeking cheaper feedstock, higher production, access to larger nearby customers and potentially a more formal research and development structure.
Recovered steel also remains important to the economics of the operation. Despite the constraints, he sees a sizeable addressable market around the company’s Visakhapatnam base.
“The opportunity is absolutely there. If we can get the right balance between the mesh we manufacture, the quantity we produce and the price, there is a huge opportunity out there,” Isukapati said.
- DUNLOP
- Sumitomo Rubber Industries
- SENSING CORE Technology
- Wheel Detachment Prediction Detection System
- Isuzu Motors
- Medium-Duty Trucks
Dunlop's SENSING CORE Adopted For Isuzu FORWARD Trucks
- By TT News
- October 30, 2026
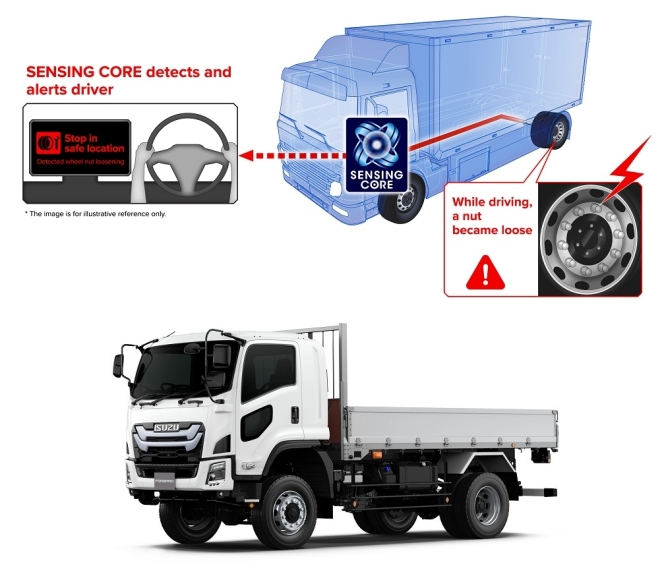
DUNLOP (company name: Sumitomo Rubber Industries) has confirmed that its proprietary SENSING CORE technology has been adopted for medium-duty truck models. The system, designed to detect the conditions of tyres, vehicles and road surfaces, is fitted to Isuzu Motors' FORWARD medium-duty trucks with a gross vehicle weight exceeding 14.5 metric tonnes, which come standard with the Wheel Detachment Prediction Detection System, one of the functions offered by SENSING CORE.
SENSING CORE is a software technology built on expertise gained from the Deflation Warning System, a tyre pressure warning system. It analyses wheel speed data generated by tyre rotation together with controller area network data transmitted through the vehicle's control system, allowing it to detect various tyre and road conditions, including tyre pressure, wear, load and signs of potential wheel detachment. The Wheel Detachment Prediction Detection System in Isuzu's FORWARD models detects loosening of wheel nuts while the vehicle is in motion, alerting the driver through a warning message and buzzer if an abnormality is found.
This capability complements conventional inspections and driver experience and is expected to play a significant role in preventing wheel separation accidents. Isuzu's FORWARD is a medium-duty truck with a broad lineup designed to meet diverse logistics industry needs, and such trucks are widely used in local delivery, long-haul transport and building and construction operations, serving as a vital means of transportation.
Operated across urban areas and major highways, wheel detachment accidents involving these trucks could cause serious harm to third parties such as pedestrians and cyclists, driving growing societal demand for improved safety. Preventing such accidents requires fundamental inspection and maintenance measures, yet drivers find it difficult to detect loosening wheel nuts while driving, making early-detection technologies essential. The provision of the Wheel Detachment Prediction Detection System to medium-duty trucks enables early detection of signs of vehicle malfunctions and contributes to further improving safety and preventing wheel detachment accidents.
- SYMX.AI
- Ascent Capital Partners
- Yokohama Off-Highway Tires
- Ash Agarwal
- Peter Xavier
- Loïc Ravasio
- Jonathan Loeffler
SYMX.AI Raises USD 6 Mln in Series A And Agrees Global Partnership With Yokohama
- By TT News
- October 27, 2026
SYMX.AI, a developer of artificial intelligence technology for mobile industrial equipment, has raised USD 6 million in Series A financing led by Ascent Capital Partners and agreed a global technology and commercial partnership with Yokohama Off-Highway Tires.
The Canadian company develops software and hardware for mining, construction and forestry operations. Its platform provides connectivity in areas without network coverage, integrates data from equipment made by different manufacturers and supports fleet optimisation.
Its products cover dispatch, fleet management, enterprise asset management and tyre life management, as well as equipment health, fuel consumption, haul road intelligence, inventory and operator performance. The company also holds patents covering its internet of things and AI technologies, including a patent for its “Greenhouse Gas Emissions Data Collection and Cross-Validation System”, granted in 2026.
SYMX.AI has also launched an AI-powered inspection platform and a chatbot for industrial operations.
“Physical AI has been struggling in mining for simple reasons. The machines are mobile, mixed-fleet data is vendor-locked, and most of the industry has limited to no network coverage. Intelligence needs a body and a nervous system before we deploy a model. Even today, assembling that foundation takes seven or eight vendors and up to twelve months. We deliver it in a week. We built the hardware and the connectivity first, which is why our AI layer delivers real results. I am glad that capital is finally flowing to atoms again, and mining will finally get what it has long deserved,” said Ash Agarwal, CEO of SYMX.AI.
Technology tested in mining operations
SYMX.AI said it had validated its technology through projects across the mining value chain. At Glencore's Onaping Depth project in Ontario, Canada, the company demonstrated battery monitoring, short-interval control and fleet optimisation for battery-electric vehicles.
“The problem SYMX.AI solves is foundational,” said Peter Xavier, Chief Operating Officer of Canada Metals, a Glencore company. “Connectivity and cross-OEM data integration at the point of work are infrastructure gaps the mining industry has struggled with for decades, but SYMX.AI changes the paradigm. Our proof-of-concept validation of the SYMX.AI platform on our OEM BEV equipment successfully supports underground short-interval control, battery monitoring and fleet optimization. This level of integration and insight is exactly what the industry needs to move forward.”
Global partnership with Yokohama
Under the partnership, Yokohama Off-Highway Tires will offer the integrated hardware and software platform to customers through its international commercial network. SYMX.AI will supply the internet of things hardware, connectivity, cloud platform and intelligence capabilities.
Customers will be able to adopt the technology as a standalone tyre intelligence solution or as part of a broader fleet optimisation platform.
“The tyre technology market is crowded with TPMS providers, but most systems monitor pressure and temperature while offering little insight beyond those measurements. Operators are asking a more important question: can the same system help us increase production, protect valuable assets such as tires and reduce fuel consumption? SYMX.AI has built a complete platform that addresses this market need by connecting tire condition with equipment performance, haul road conditions and operator behavior. This helps sites reduce costs, extend tire life and improve overall fleet performance,” said Loïc Ravasio, President of Yokohama Off-Highway Tires. “By working with SYMX.AI and offering flexible business models, Yokohama OTR is becoming a true digital partner to the industry, helping customers optimize their operations.”
Expansion and investment
SYMX.AI is expanding its product range with an AI-driven dispatch and fleet management system and an enterprise asset management platform based on live machine sensor data and fault codes.
The asset management system combines equipment health monitoring, diagnostic alarm management, oil analysis and work order management. The company says the system is designed to reduce reliance on fixed maintenance schedules and manual data entry.
Its products integrate with AVEVA Connect, SAP, Oracle and existing data historians, allowing operators to add the technology without replacing their existing systems.
The company said it supported open-pit and underground operations in Kazakhstan, the US, Mexico, Europe and Asia.
“We have watched this team for three years demonstrating grit, perseverance, and commitment. They build things that work in places most software never reaches, and the customers keep renewing worldwide. That is rare in this industry. The comprehensive IoT, connectivity, and AI app layer is deployed at difficult sites, and I’m glad that the market is finally catching up,” said Jonathan Loeffler, Co-Founder and Managing Partner of Ascent Capital Partners.
The financing will support international deployment, development of the AI platform and a broader range of wireless communication products, SYMX.AI said.
Anyline Rolls Out TireBuddy 1.9 With Redesigned Inspection Report
- By TT News
- October 25, 2026
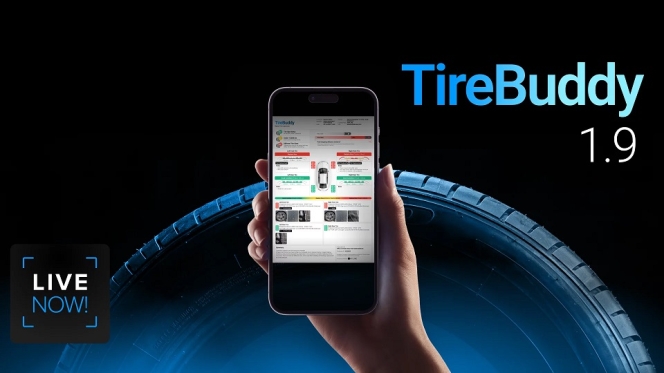
Anyline, a global leader in mobile AI and intelligent data capture technology, has rolled out version 1.9 of TireBuddy, featuring a redesigned inspection report that aims to help customers more easily understand the condition of their tyres and place greater trust in technician recommendations. The updated report is intended to make the information gathered during an inspection simpler for customers to digest.
The report presents tread depth, tyre age and estimated braking distance to convey overall tyre health, while make, model, size and seasonal markings identify exactly which tyres are mounted on the vehicle. The new version also allows technicians to attach images of sidewall and rim damage to the report, transparently documenting issues that require attention so customers can have confidence in the recommended work.
Technicians can now record rim and tyre damage, such as scratches on rims and bulges on sidewalls, during the inspection workflow and display it in the report. Photo evidence of rim and sidewall damage can be attached to technician notes and added to the report. A not-roadworthy flag can also be set for a tyre with healthy tread depth but other serious defects, showing in the report as recommended for immediate replacement. All existing and new elements continue to fit on a single page, which can be saved as an image or PDF for sharing with the customer.
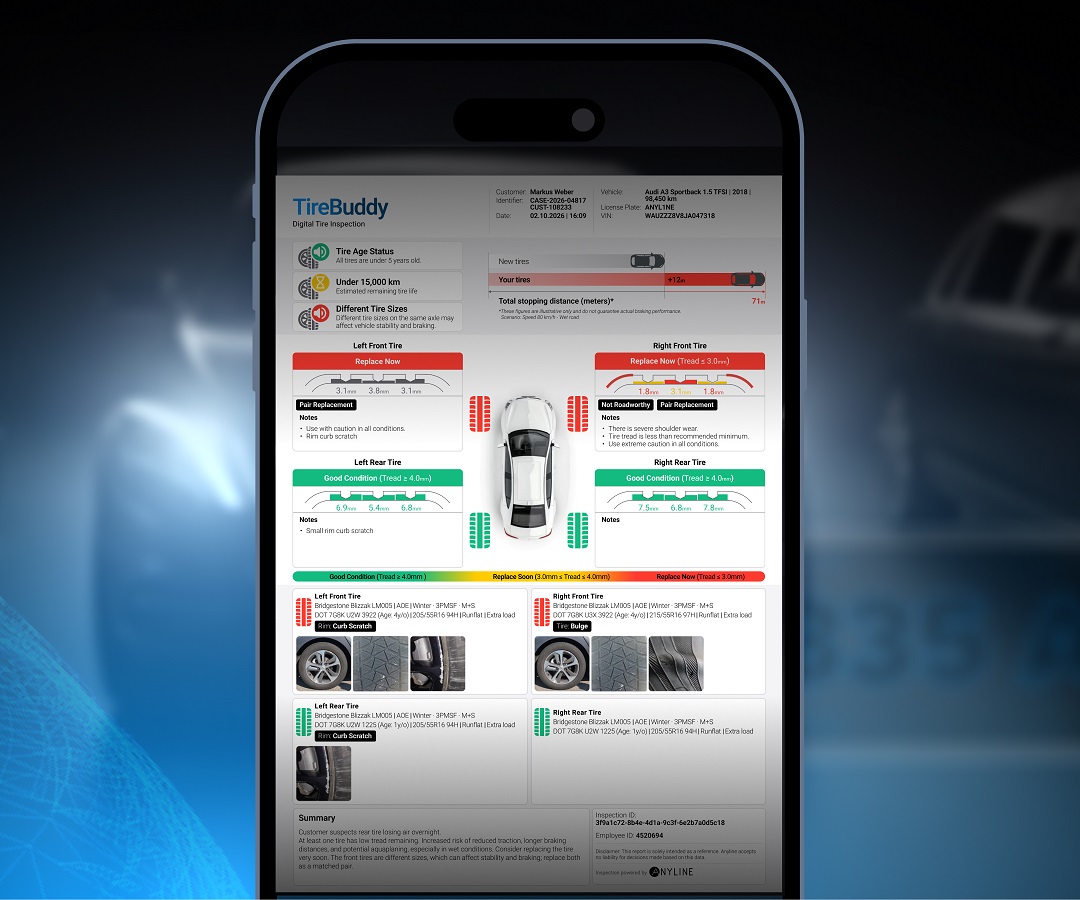
The TireBuddy report addresses a critical issue for workshops by ensuring customers fully understand inspection findings. Verbally conveying such information is not always easy, and traditional inspection forms tend to be dense and text-heavy. Everything a technician finds in the bay needs to be detailed in the report the customer sees, which should serve as visual support for service recommendations. With version 1.9, evidence appears alongside the recommendation, and photos of tyre or rim damage are inserted with other tyre information so customers can recognise findings without entering the bay.
Damages are categorised alongside visual evidence, so a bulge is recorded consistently regardless of technician, location or shift, turning individual reports into a comparable record that still captures the state of every tyre on the inspection day. From version 1.9, every report can carry damage, roadworthiness and photo evidence alongside the tread reading. Smaller changes include an optional pair replacement setting that automatically marks the paired tyre on the same axle for replacement when one tyre is not OK, up to 10 custom fields per account in the vehicle identification step for work order or storage numbers and a redesigned vehicle identification screen consistent with the tyre identification screen.
Lukas Kinigadner, CRO, Anyline, “Every replacement recommendation is a request for trust. With 1.9, the technician doesn't have to ask for it. The damage is on the report, photographed, next to the tyre it belongs to.”
Comments (0)
ADD COMMENT