Most of us know the alleged Chinese curse: ‘May you live in interesting times…’. This term, in fact, is not of Chinese origin: it was first used by a British diplomat in the late 19th century and is a kind of upper-class British joke.
And yet, as we look at the world today, in political, economic, technological and environmental terms, most of us would agree that the times we live in are far too ‘interesting’ for comfort. Predicting even the near-term future is becoming more difficult, while making rational longer-term investment decisions often feels like a high-risk gamble.
Managing uncertainty requires a very special set of skills – and uncertainty is exactly what the tyre industry is being asked to deal with right now. We can all make a list of the individual challenges we face, but perhaps the best and simplest way to define this issue is by saying that the business model of the tyre industry is in question.
CHALLENGES TO THE BUSINESS MODEL
The modern tyre plant is a product of globalisation. It depends on relatively open supply chains, predictable logistics, ready access to materials, affordable energy and steady demand for products. Unfortunately, these factors can no longer be relied on.
Mike Norman
The vehicle market is changing, notably by the rapid rise in demand for electric vehicles, while the number of tyre variants is also growing fast. We are moving to a market reality in which volume may stay more or less the same, but the number of different tyre designs is rising and the volumes per SKU are going down.
Globalisation has gone into reverse, with a rise in protectionism and tariffs, leading to ‘reshoring’ and a trend to more local production, based closer to the markets being served, enabling more agile response to demand.
A technology revolution is taking place, with automation altering the cost base and leading to a levelling up in quality – a process that has been going on for a long time. Price premiums across a wide range of market segments are starting to disappear because quality standards are now so good across the market that it is becoming harder to justify higher prices for ‘premium brands’.
We can all agree therefore that the industry is changing – but it is not so easy to define where it is heading.
THE SHAPE OF THE FUTURE?
There is overwhelming evidence that the tyre industry of the future will look very different from the industry of today. It is tempting to present a single model of the future and invite all the different industry players to plan their own roadmap to that single future. That would be a mistake – the industry is diverse and we think it will remain so. There is a clear direction of travel (towards more comprehensive automation, greater agility, lower energy use, ability to manage a greater number of variants, use of new materials, reduced environmental impact…), but the options remain broad and the future is still unpredictable.
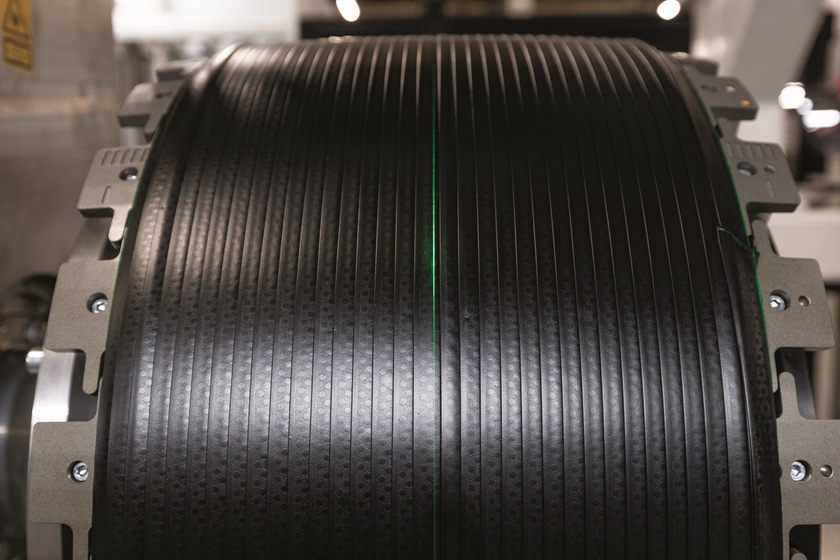
VMI not only has a vision of the future but works continuously to develop innovative solutions that support the industry and its development. In fact, we have even successfully built a true single cell production platform. This is UNIXX, which is designed to make tyres within a single process, from initial compound mixing to the finished product. You can manage as many variants as you wish, because each individual product can be made profitably – a true ‘market of one’ approach. The footprint is very small, compared with current plants, and environmentally it is far more responsible, using less energy and with much lower levels of pollution.
Surely, this is where we should be heading? Well, perhaps it is, but life is not that simple. Every business has to start from where it is right now, which is why we celebrate:
THE IMPORTANCE OF EVOLUTION
In evolutionary theory, there is an ecosystem, which is a common space inhabited by many different species. They sometimes compete for resources, sometimes complement and help each other, while they all have to deal with bigger forces from the outside. In the distant past, these might have been volcanoes and meteorites, but in our case, the external forces are probably wars and tariffs.
The key is not to focus on a single image of the ‘perfect’ future design but to have the ability to evolve as the environment changes – and keep evolving. You must start from where you are today and then follow the logic of the market, emerging technology and your own strategic priorities. The result will be – as with natural evolution – a lot of diversity but with every player moving in a common direction: towards a future that is more automated, more efficient, more flexible.
So what does the market look like right now?
There is still that familiar divide between Tier 1, Tier 2 and Tier 3, but the old definitions and distinctions are no longer as solid as they once were.
Most Tier 1s are losing their price advantage, at least in certain markets, because the Tier 2s have now reached a comparable quality level. Tier 3 businesses are exploiting their generally lower cost base, combined with advanced, highly automated factories to build advantage in the market through a highly competitive price point. Each type of business has its own operational realities and long-term goals. They are all moving through their own evolutionary journey. The big question we at VMI ask ourselves is this: How can we help them all to develop as successfully as possible?
KEY LESSONS OF EVOLUTION
When you start a journey of change, there are some basic priorities that apply to us all.
Simplify and take out costs. To make sure that business change projects deliver real benefits, the first task is to take out cost and reduce risk by simplifying and accelerating your existing processes. Simplification will lead to reduced energy and materials use (saving money at once), fewer human touch points (also saving money) and potentially could enable you to reduce the footprint of your plant (freeing capital for productive investment).
Every year, VMI brings out new refinements to existing systems, solutions and investments, designed to improve performance and take out cost. Here are some of the most recent of these:
- Smart Splice Ply fits to existing VMI TBMs already on site to reduce variations in play and splices. It raises quality, saves material and speeds the process.
- Then there is OEE (Overall Equipment Effectiveness) Reporter, a purely software solution that identifies areas for process improvement for reasons that range from downtime to operator issues, with the aim of moving towards 100 percent effective operation.
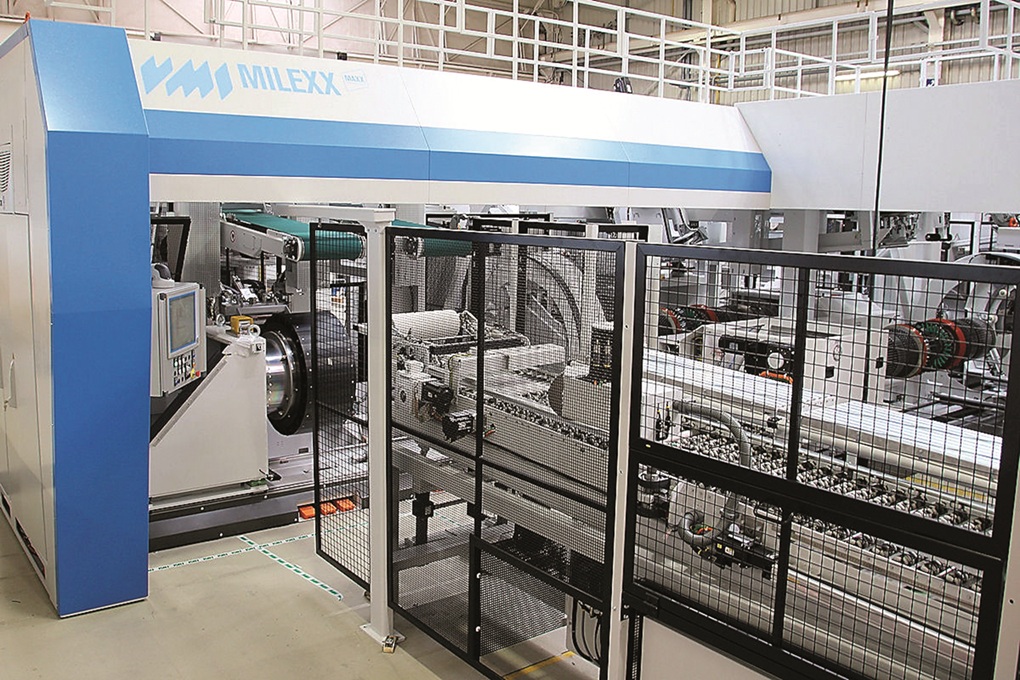
- Perhaps the most exciting of these new developments is the Autonomous Materials Delivery (AMD) solution, which combines automated handling of compound rolls, Smart Run Empty (designed to cut out compound wastage) and interface with Automated Guided Vehicles.
AMD summarises the ways in which the operation of existing machines, investments and solutions can be continuously improved to reduce the need for human intervention, reduce machine downtime, cut down wastage and drive higher operational efficiency – all without disruption to business as usual while maximising the potential of existing investments.
This is the very definition of stage one in the evolutionary change journey: improve what you have and bank the savings for reinvestment in the future.
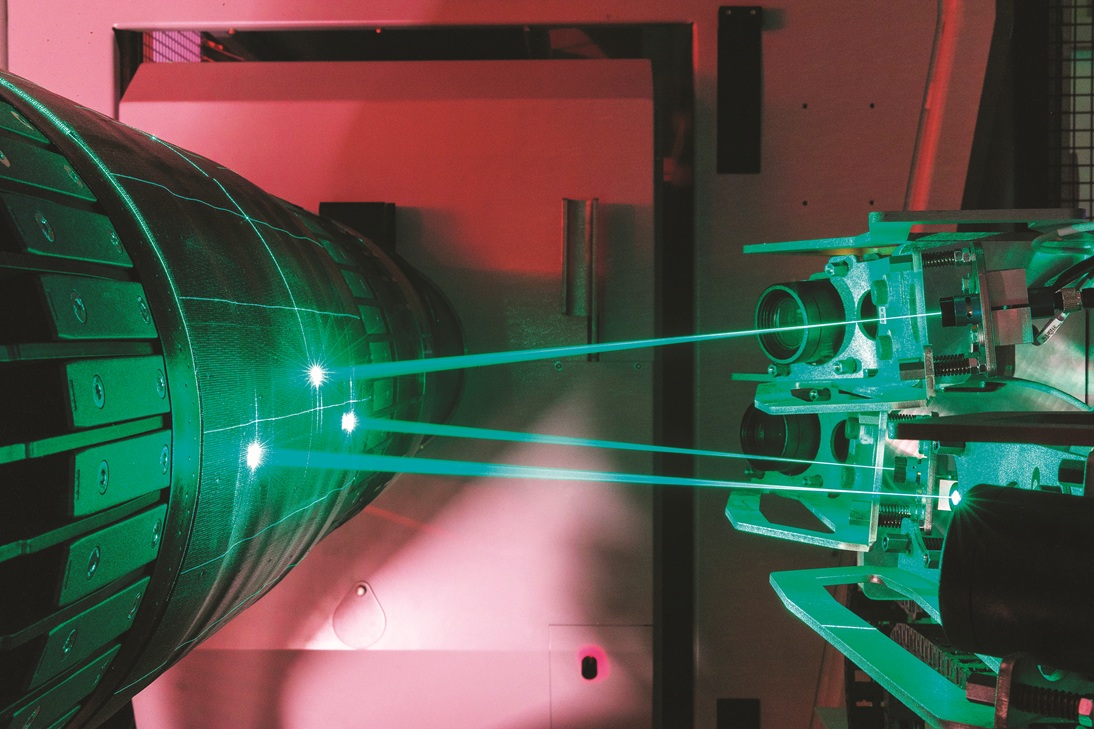 Implement new technologies, one by one. We understand there can be no ‘big bang’ changes in the tyre industry, but we can start to profit from the most advanced new technologies today without the disruption that wholesale change would cause, adding new concepts alongside existing investments in the second stage of evolutionary change.
In some cases, this makes it possible to close down existing processes completely, making machines redundant and delivering significant savings. In others, we can eliminate specific stages in a process, again leading to simplification, higher quality and cost reductions. Here are two examples:
- UNIXX Beltmaker (now with hot gum strip feature) carries out most of the activities of a traditional calendering line but faster and more efficiently. Given the size and high energy use of calendering in tyre plants, the potential for reducing plant footprint and energy costs is enormous.
- VMI’s new Strip Winder, again developed for UNIXX, is now available for evaluation and review, with the potential for simplifying some aspects of production while offering a number of quality and design advantages.
This is a technique that many companies have struggled to master but which is fully operational right now. You can see it for yourselves, as well, because VMI’s mobile Strip Winding roadshow will make it possible to watch, test, examine, ask difficult questions and prove for yourselves that it works.
Extend the scope of automation. Industrial automation is what VMI stands for, so moving to the next stage is not a break from the past but an evolutionary move. As part of the TKH Group, VMI is now not just benefitting from its own in-house (but globally located) R&D activity but is also building on the AI capability inside the Group.
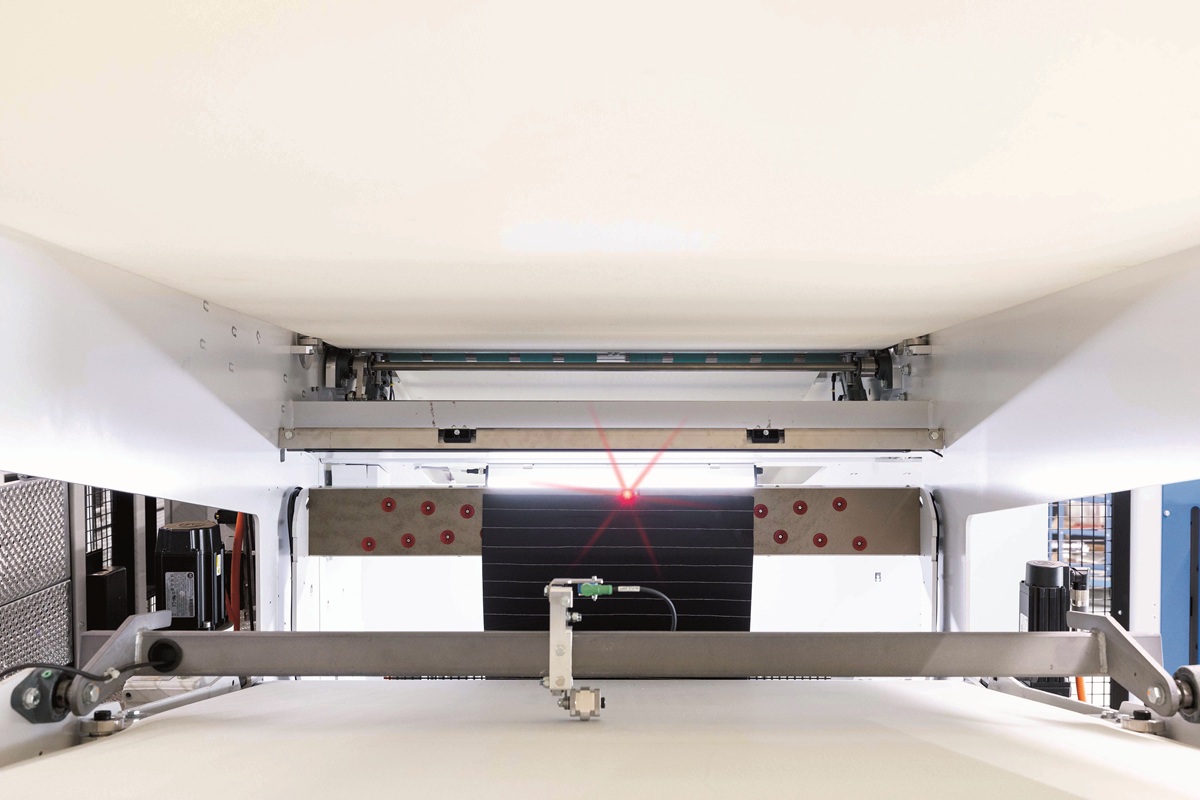
There are some aspects of AI that attract some scepticism (rightly), but industrial automation is the most natural development of AI – and VMI is driving it forward at speed. During the rest of this year, we will complete development work on a decision support GenAI-enabled system that will make it easy for operators to optimise machine performance while giving assurance to employers that the operators themselves will be able to work more efficiently.
This will be just the first step in a process of continual evolution, in which machine intelligence will be exploited in more intuitive ways to enable faster skills development, deeper insights and eventually lower requirements for human intervention at all. Current VMI solutions already include advanced sensor arrays, pattern recognition (for anomaly detection) and machine learning. Many of the key elements of true AI are in place, therefore, and development has started to accelerate!
Move towards the Dark Factory. The end point of industrial AI, as defined by industry leaders in other sectors, is the idea of Autonomous Production, sometimes known as the Dark Factory – not just hands off, eyes off, to use VMI’s familiar mantra, but lights off, too!
We think use of AI in this context is the most important of all evolutionary steps, as it enables tyre manufacturers to start gaining cost and agility benefits fast while closing down redundant processes and hardware in their own time. To be clear, there will remain major differences in scope, size and potential between different industry players in the age of AI, but implementing a governing intelligence, end to end, will be common to all.
STARTING THE JOURNEY
All of us have our own individual, evolutionary journey. The key objective for every business leader in this complex, global industry is how to build their own roadmap to the future. There is no longer any question about whether we need to change or not – we certainly do – but we have no choice about where we start from. Our starting position also defines our short-term objectives.
Our conclusions are simple but – we think – unavoidable.
- Change is coming for us all. We have the option of choosing our own path and our own priorities. But not of standing still.
- Change is not just about technology: it also covers the organisation, people, partners and customers. Technology might be powerful, but if you can’t find the skills and budget to implement it, then it remains theoretical.
- AI is not a magic bullet: this simple term covers a complex suite of capabilities and techniques that need to be understood in depth and implemented with care.
- All change processes follow the same basic rules and stages. Simplify and save money now; mitigate risk and be able to stop and go back if needed; test new concepts one by one and don’t go onto the next until you have mastered the first.
The journey is what matters, and you will need a map, guidance, partners and friends to make the journey both safe and productive. It’s not revolution but evolution: that is the word that defines both the challenge and the way to make change work for you.
The author is the Chief Commercial Officer at VMI.

Comments (0)
ADD COMMENT