- Vehicle Dynamics Conference
- VDC 2026
- Tom Thomas
- S K P Amarnath
- Apollo Tyres
- Renault India
- Dr Vikraman
- Shiv Sikand
- Drako Tech
- Manoj Agarwal
- Maruti Suzuki India
- Piyush Kende
- Tata Motors
- Arjun Balasubramanian
- Apollo Tyres
- Ankur Sharma
- JSW MG Motor India
- Prajakta Khare
- Dassault Systemes
- Dr Nagesh Poojary
- IPG Automotive
- Sharad Matade
- Tyre Trends
- Vishwadev Muraleedharan
- Simple Energy
- Prithvi Raj S
- Raptee HV
- Nilesh Wadhwa
- Gopal Musale
- BWM TechWorks India
- Alexander Aydt
- Vector Informatik
- Darren Jeseritz
- MTS
- Rajaram Kumble
- Daimler Truck Innovation Centre India
- M K Jain
- JK Tyre & Industries
- Dhanasekar Venkatesan
- Cadence
Vehicle Dynamics At The Crossroads And The New Rules Of Mobility
- By Bhushan Mhapralkar and Nilesh Wadhwa
- September 01, 2026
Vehicle Dynamics Conference 2026
From software-defined architectures and virtual proving grounds to the evolving role of tyres and ADAS, the third Vehicle Dynamics Conference in Chennai captured an industry in rapid transition. Industry leaders examined the trade-offs, technological leaps and competitive pressures that will define the next decade of vehicle engineering in India.
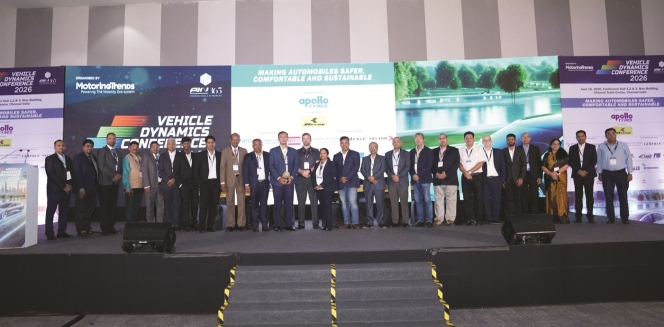
It was on 16 June 2026 that the 3rd edition of the Vehicle Dynamics Conference took place at Chennai Trade Centre, bringing together close to 200 stakeholders from the auto industry across India and internationally and marking another milestone for automotive development.
The event focused on the rapid evolution taking place across vehicle engineering, focusing on safety, performance, ride and handling, efficiency and emerging technology developments.
Opening the conference, Tom Thomas, Conference Chairman, underlined the significant transformation gripping the automotive sector. In his welcome address, Thomas noted, “Advances in software-defined vehicles, simulation technologies, electrification, safety systems, connectivity and vehicle performance are redefining the future of mobility.”
Building upon this perspective, S K P Amarnath, Vice-President of R&D, Apollo Tyres, declared that the event had matured into a vital platform where the entire ecosystem is discussed, status quos are challenged and new ideas are exchanged.
“Multiple transformational forces are converging at the first time in auto industry’s history, creating a defining moment for mobility,” Amarnath stated in his opening address.
He emphasised that the industry stands united in creating safer, smarter, comfortable, and sustainable vehicles, observing, “The disruptions – connected, autonomous, electric and software-defined vehicles (SDVs) – are happening at a speed and scale never experienced before.”
Amarnath further described India’s remarkable rise as a global automotive hub that faces fresh competitive pressures from China and Eastern Europe. “The speed of change is fast and influencing key attributes like vehicle dynamics and energy management. OTAs are becoming common and vehicles are turning into a continuously evolving platform,” Amarnath explained.
Turning attention to hardware, he identified the tyre as the most neglected part of the vehicle despite being the only component in direct contact with the road surface.
Revealing that Renault engineers devoted extensive track time to tyre testing at the Madras Racing Circuit, Dr Vikraman explained, “The slip angle, slip ratio, steering response, ride comfort, cornering stiffness optimisation etc. were achieved on dot through thousands of tuning cycles.”
He outlined that three guiding principles – be clear, be sure and be clever – guided target setting, vehicle character creation, kinematics, simulation and real-world proving ground evaluations. He observed that while precise tuning makes a vehicle exceptional, ADAS has compounded the paradox regarding vehicle dynamics.
Dr Vikraman mentioned that to overcome regional road variations, Renault clever-engineered the Duster’s ADAS technology specifically for local conditions where regulations regarding speed humps and barricades are rarely enforced.
Asserting India’s growing importance, Dr Vikraman concluded, “Engineers are expected to solve complex problems with creative solutions. Indian engineers should be creative and disruptive. They should be also proud.”
In the session focused on software, simulation and NVH, Shiv Sikand, Co-Founder of Drako Tech, spoke on the future of self-driving connected vehicles. “The architecture necessary to deliver AI connectivity, ADAS and OTA has simply been too expensive to put into a mainstream vehicle programme,” Sikand noted.
“Drako architecture – founded specifically to eliminate that barrier – enables the addition of new features through a mere software push,” said Sikand, explaining that traditional vehicle designs are frozen when shipped, leaving engineering cycles four to six years old by the time cars reach consumers.
He mentioned, “Tesla proved what seemed impossible 10 years ago. It proved that a software-first vehicle architecture could deliver a better product at lower long-term cost. Chinese manufacturers took that lesson – specifically BYD – and industrialised it at scale.”
The executive explained that Drako’s DriveOS single-ECU platform replaces kilometres of wiring and dozens of isolated ECUs with a single USB backbone and commodity hardware, cutting cost, weight and carbon footprint.
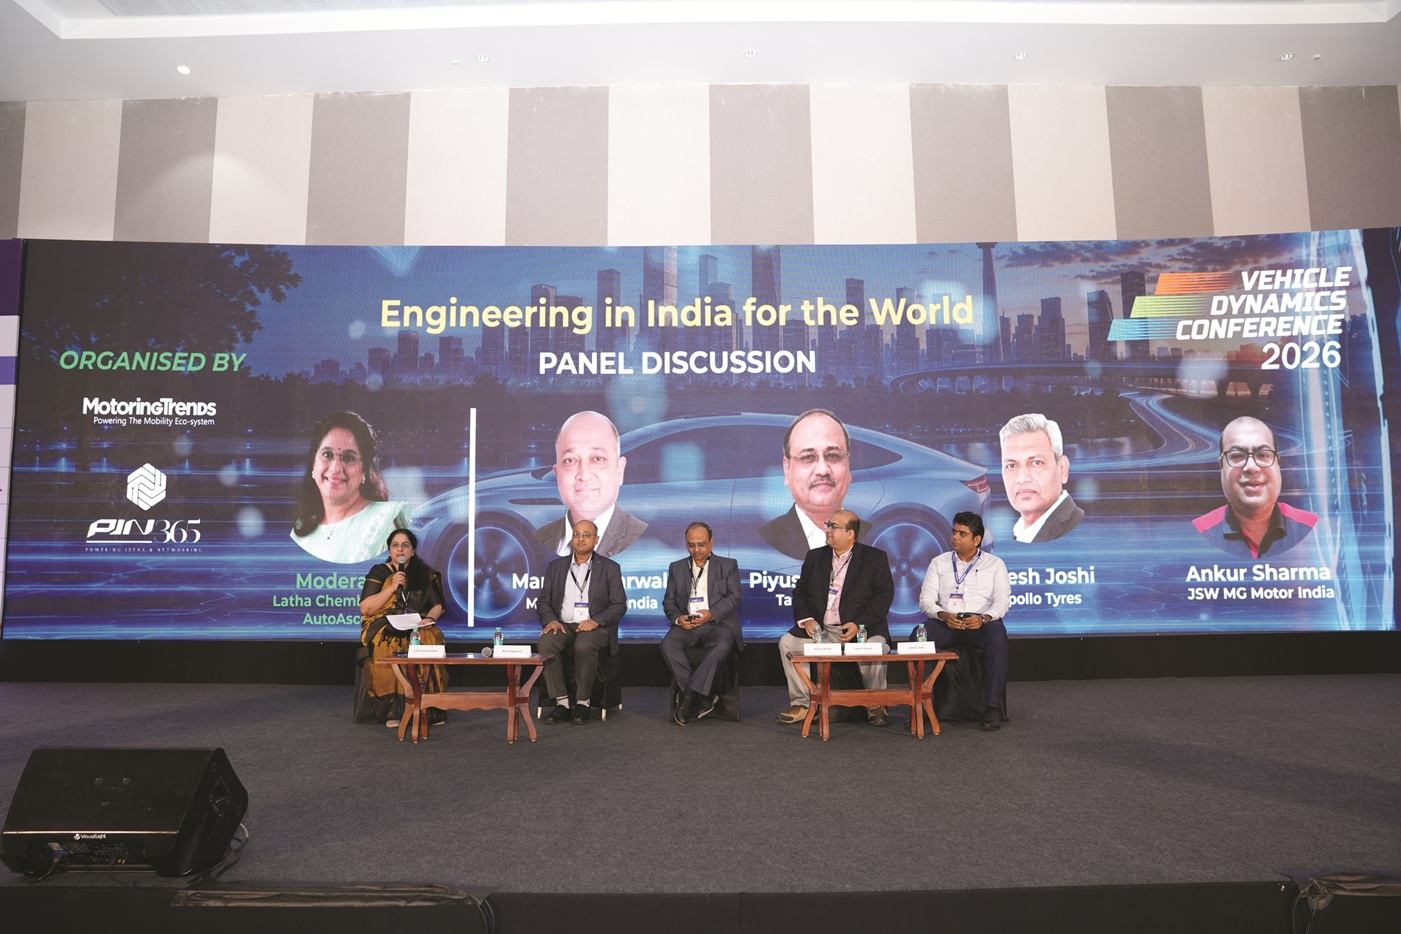
During the panel discussion titled ‘Engineering in India for the World’, moderated by AutoAscend’s CEO Latha Chembrakalam, industry executives evaluated local development trends.
 Manoj Aggarwal, Vice-President of Engineering at Maruti Suzuki India, observed that while central computing was once considered too costly, current focus centre’s entirely on software systems and exporting Indian products to Europe and Japan.
Aggarwal noted, “The ISO 26262 standard has been adopted and work is progressing on digital twins with Japan and Germany to deliver a global product. In vehicle dynamics, much work is taking place on virtualisation.” He added that Maruti Suzuki maintains a dedicated division to collaborate directly with startups.
Piyush Kende, Senior General Manager of Vehicle Integration at Tata Motors, emphasised that changing regulations and multi-fuel options are driving rapid engineering shifts. “SDVs are a new trend and are creating a need to work on them faster from India perspective,” Kende said, noting that Tata develops platforms in-house.
“Young engineers need to be pushed into innovation and IP creation. There is a gap regarding knowledge vis-à-vis real-world understanding,” he added and explained that regulatory frameworks encourage local engineering while global supply chain strategies protect against international disruptions.
Arjun Balasubramanian, Division Head of Product Development (PCR-OE) at Apollo Tyres, shared, “We are tackling geopolitical issues that add a different perspective to the supply chain, resources and engineering opportunities. We are also collaborating with academia regarding engineering, governance etc. We are also making patents and building technology.” He added that evolving tyre emission regulations require active academic and industrial research.
Ankur Sharma, Head of Platform Engineering at JSW MG Motor India, highlighted that vehicle development is no longer purely mechanical, remarking, “There’s AI at work.” Sharma explained that Indian testing includes unique local edge cases, stating, “We have had scenarios with a vehicle hitting a cow or vice versa as a test parameter that is unique to India. This could be applied to markets that face such a challenge.” He added that workforce availability and time-to-market demands make academic collaboration essential.
Addressing computer-aided engineering, Prajakta Khare, Technical Manager of Multibody Dynamics at Dassault Systemes, presented on Simulia Simpack.
L-R: Latha Chembrakalam, CEO, AutoAscend; Manoj Aggarwal, VP – Engineering, Maruti Suzuki India; Piyush Kende, Sr Gen Manager,
Vehicle Integration, Tata Motors; Ankur Sharma, Head – Platform Engineering, JSW MG Motor India and Hitesh Joshi, Head of Technology, Apollo Tyres.Your contribution played a pivotal role in making GTRC 2026 a resounding success. We deeply appreciate your trust and collaboration, and we look forward to welcoming you again as we continue to shape the future of the tyre industry together.
Khare noted, “Simulia Simpack is unique and delivers in terms of accuracy, efficiency, team automation and robustness, among others. In the face of challenges that include market pressure, complexity and diversity, this helps to do CAE led development, including in the area of vehicle dynamics.”
She added that Simulia resolves complex physical factors in software-defined vehicles, including high vehicle mass, regenerative braking, battery placement and tyre properties.
Dr Nagesh Poojary, Managing Director of IPG Automotive India, spoke on virtual validation ecosystems, warning that software recalls could cost the industry USD 30 billion to USD 35 billion in warranty expenses. “Doing real-world tests is not feasible while the need to test more is increasing,” Dr Poojary noted, explaining that continuous virtual validation under ISO 26262 enables manufacturers to handle software complexity efficiently.
In the safety and performance session moderated by Sharad Matade, Executive Editor of Motoring Trends, panellists examined two-wheeler engineering.
Vishwadev Muraleedharan, Head of Vehicle Dynamics at Simple Energy, pointed out that the rider constitutes 50 percent of total vehicle dynamics. “A technology like ABS is mandatory and there should be a clear line between the system intervening and not intruding in a two-wheeler,” Muraleedharan mentioned. He revealed that electric two-wheeler battery compartments form a critical structural part of the chassis and urged ground-up component design. He noted that Simple Energy utilises a mid-drive motor near the swingarm pivot to centralise mass near the centre of gravity.
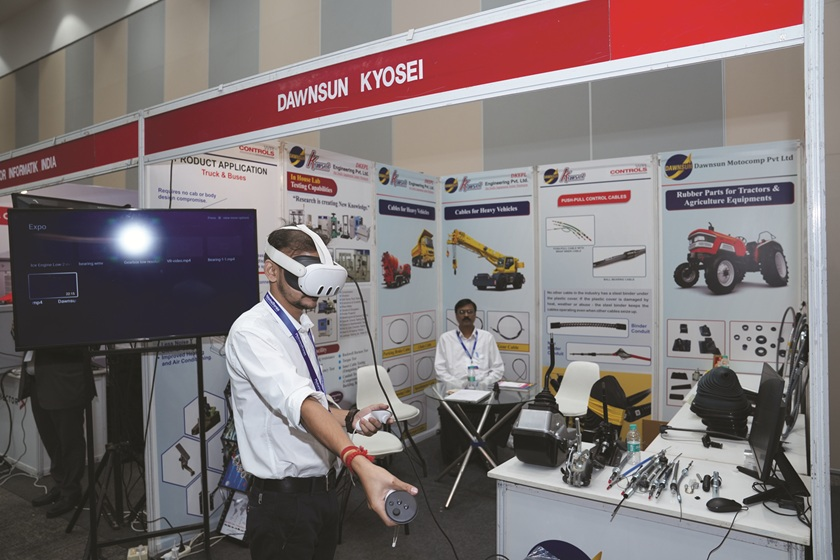 Prithivi Raj S, Technical Manager of Vehicle Engineering at Raptee HV, agreed that two-wheeler packaging is complicated by high centre-of-gravity requirements. He suggested that Inertial Measurement Units could generate rider safety scores alongside managing ABS lean angles.
“We have engineered a huge battery box to get the Cente of Gravity (CG) right in terms of dynamics. The most underrated factor in ride and handling is tyre pressure. A tyre is not only for grip but also a significant part of the spring damper system,” Prithivi Raj averred, stressing that system interventions must not override driver control unpredictably.
In a panel on smart hardware and software moderated by Nilesh Wadhwa, Assistant Editor of Motoring Trends, Gopal Musale, Cluster Head of Digital Product Engineering at BMW TechWorks India, announced, “The use of software and hardware is at a point where more software will come in hereafter. Vehicle improvement is going to be closely linked to AI in the coming times and software updates will be over the air (OTA).”
Musale explained that BMW utilises digital twins and a six-degree-of-freedom simulator in Munich to evaluate vehicle behaviour virtually before building physical prototypes, saving significant time and testing costs.
Alexander Aydt, Senior Fellow for ADAS/AD Tooling at Vector Informatik, noted that AI accelerates code generation and object detection, such as identifying a child running behind a ball. However, Aydt emphasised, “Humans are still strong at predicting the unimaginable.” He added that software-defined architecture allows engineers to alter intrusive vehicle features with ease compared to rigid mechanical designs.
Darren Jeseritz, Senior Applications Engineer at MTS, presented on hybrid simulation and Model-in-the-Loop (mHiL) testing. Jeseritz explained that MTS hybrid simulation integrates physical hardware with virtual multibody models, enabling steering and suspension certification on virtual tracks before physical prototypes exist. He noted that four-corner systems allow for complete vehicle dynamics simulation in laboratory environments.
The commercial vehicle session, moderated by Bhushan Mhapralkar, Editor of Motoring Trends, addressed decarbonisation and efficiency. Rajaram Kumble, Section Manager at Volvo India, noted that Volvo evaluates safety for both occupants and pedestrians. He shared that systems like predictive cruise control deliver 5 to 7 percent efficiency gains, while Volvo Dynamic Steering reduces steering effort in heavy manoeuvres by up to 70 percent.
Ramakrishna Donakonda, Vice-President and Head of Powertrain and eDrives at Daimler Truck Innovation Centre India, contrasted European staggered regulations with India’s simultaneous regulatory deadlines, such as 2027 ADAS mandates.
Donakonda explained that OEMs prioritise scalable platforms, noting, “Ultimately, what is offered to the customer is what they want and at prices that are acceptable to them.” He added that commercial electric vehicle adoption remains governed by charging infrastructure availability.
M K Jain, Tyre Technologist at JK Tyre, observed that commercial vehicle technology is rapidly adopting passenger car innovations, including Tyre Pressure Monitoring Systems and ‘Tyre-as-a-Service’ models. Jain noted that as per-kilometre payment models expand, tyre manufacturers are transitioning into ongoing tyre managers rather than pure hardware suppliers.
Concluding the technical presentations, Dhanasekar Venkatesan, Senior Principal Application Engineer at Cadence, highlighted that compressed launch timelines push teams towards zero-prototype development. Venkatesan explained that Cadence provides the MSC Adams multibody dynamics tool – a 50-year-old software used in space programmes – to accurately predict motion, forces, durability and vibration under complex Indian road conditions.
The third Vehicle Dynamics Conference demonstrated that vehicle engineering has transitioned into an integrated ecosystem where software, virtual simulation and mechanical design converge to shape the future of global mobility.
The Goodyear Tire & Rubber Company has elected Joe Hinrichs as chairman of its Board of Directors, effective 7 October 2026. He will also chair the board's Governance and Executive Committees. Hinrichs joined the board in 2023 and succeeds Laurette Koellner, who will retire at the 2027 annual meeting under Goodyear's Corporate Governance Guidelines.
Hinrichs most recently served as President and Chief Executive Officer of CSX Corporation. Before that, he held numerous leadership roles at Ford Motor Company, including President of the Global Automotive Business, Executive Vice President and President of Global Operations, Executive Vice President and President of the Americas, President of Asia Pacific and Africa, and Chairman and Chief Executive Officer of Ford China. He also led Ford Canada. Hinrichs holds a bachelor's degree in electrical engineering from the University of Dayton and an MBA from Harvard Business School.
Koellner previously held several leadership roles at The Boeing Company. She joined Goodyear's board in 2015, became independent Lead Director in 2019, and Non-Executive Chairman in 2024.
Hinrichs said, "I would like to recognise and thank Laurette for her leadership, dedication and unwavering commitment to Goodyear. On behalf of the Board, we are grateful for her many contributions throughout her more than a decade of service. I look forward to working alongside my fellow board members and the leadership team as we continue to innovate, strengthen our competitive position, create long-term value for our shareholders and build a stronger Goodyear."
CEAT Specialty’s Off-Highway Tyre Playbook
- By Sharad Matade
- October 09, 2026
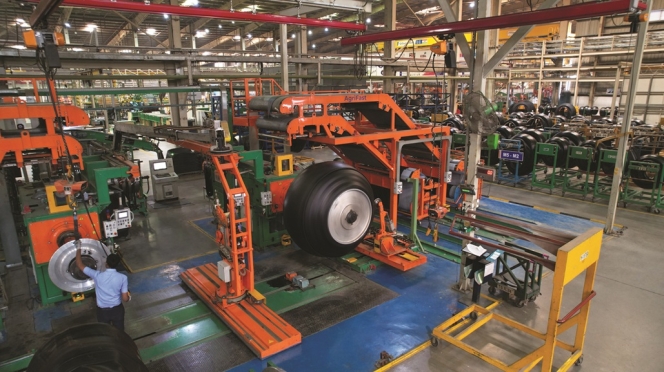
CEAT’s Chennai and Halol plants are the only tyre facilities globally with two WEF Global Lighthouse Network inductions, and the company has also won the Deming Grand Prize for manufacturing excellence.
Yet 30 km from Mumbai, CEAT Specialty’s 49-acre Ambernath plant tells a different story: tyres too heavy for automation, built instead around nitrogen curing, induction presses and orders as small as one unit – a bet that sustainability will win markets in Europe and America.
The stakes: an INR 5 billion investment in all-steel radial technology, capacity expansion to 160 tonnes/day and a Camso manufacturing deal Tolani pegs at up to USD 1 billion – turning a manufacturing constraint into a competitive edge.
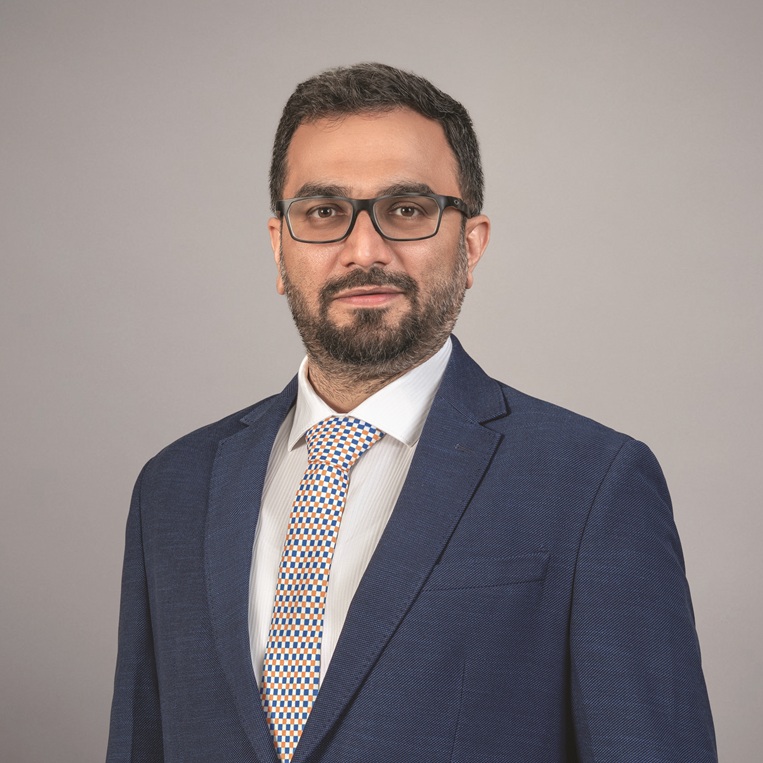
Amit Tolani, Chief Executive of CEAT Specialty, does not talk about tyres the way most executives talk about their products. He talks about them the way an engineer talks about a puzzle that keeps changing shape. “The way to look at it is that the manufacturing processes that we follow – how modern they are, how capable they are, how technically efficient – that’s what matters,” he says, sitting inside the plant that has become the nerve centre of CEAT’s off-highway tyre (OHT) business.
That plant – the Ambernath facility, a division of Mumbai-headquartered RPG Group’s CEAT Limited – is not a conventional tyre factory. It builds tyres that can weigh up to over 600 kilogrammes, tyres too large and too heavy for the automation that has transformed the passenger-car tyre business. And it is this constraint, as much as any strategic masterplan, that has shaped how CEAT Specialty has chosen to compete.
A PLANT THAT CANNOT SIMPLY COPY THE ROBOTS
Ask Tolani why Ambernath has not adopted the wall-to-wall robotic automation seen at CEAT’s Chennai or Halol facility, and the answer is refreshingly unglamorous: physics. “PCR tyres can be lifted by an ordinary human being, or a forklift, or robots,” he explains. “For these tyres, which are 600–700 kg, it’s very difficult to have a conveyor that can just lift them.” In the processes that do lend themselves to automation – mixing, calendering, curing – Ambernath’s equipment, he insists, is ‘as modern as the Chennai plant. More modern’. The plant intends to formalise that claim in the coming months by pursuing Industry 4.0 certification.
Where the physical limits of scale end, digital ones have taken over. A SCADA system tracks steam lines running beneath the plant floor. Where a leak once required a worker to walk the line, take manual temperature readings and diagnose the fault, artificial intelligence now flags the location almost instantly. “The point time taken to identify the problem is close to zero,” Tolani says. Every tyre carries a digital identity from raw material to finished good; a single scan reveals the batch, the machine, the operator and the timestamp behind it. AI is also being trained on the plant’s visual tyre inspection – traditionally a human, eyeball-driven task – using high-resolution cameras to catch defects, and on optimising mixing recipes and cycle times, the invisible chemistry that determines how a tyre performs in a paddy field or a quarry.
CURING WITHOUT STEAM
The most technically striking claim to emerge from Ambernath concerns curing – the energy-intensive process of vulcanising rubber under heat and pressure that has, for a century, meant steam. “This plant has already started using nitrogen curing on one of the lines,” Tolani says. Alongside it sit two proof-of-concept induction curing presses – a steam-free process, while the nitrogen conversion has come via LMT. “There are two presses that are already commissioned here,” he says. “We’ve already started working in that direction, where we want to take a lead in this space.”
The bulk of the plant’s newest investment, however, is going into something more conventional in principle but strategically significant in intent: all-steel radial off-the-road tyres. CEAT Specialty has committed INR 5 billion to this latest phase of expansion, representing a decisive shift in product architecture. Where a car’s tyres are universally radial, only 60–70 percent of truck tyres have made that transition, and agricultural and OTR applications lag further still – agriculture because usage is seasonal, OTR because a fabric-belted bias tyre still does much of the heavy lifting. All-steel radial construction changes that calculus by delivering higher load-carrying capacity and greater comfort, attributes increasingly demanded not only by Indian buyers but, crucially, by European and American customers. “It’s for demand from the European market, the US market – and the Indian market is also growing in such a handsome fashion that we want to cater to it,” Tolani says.
LEAN BY DESIGN, NOT BY SLOGAN
CEAT’s manufacturing philosophy is inseparable from its most prized accolade: in 2017, CEAT became the first tyre company outside Japan to win the Deming Prize, the world’s most prestigious award for total quality management; in 2023, it became the first tyre company anywhere to win the Deming Grand Prize, a distinction held by only 33 organisations globally as of 2025. Inside CEAT, this discipline is branded QBM – Quality Based Management – a homegrown fusion of Total Quality Management, the Toyota Production System and Total Productive Maintenance.
“We are a Deming Grand organisation. That means we follow the philosophy of lean manufacturing – not to use resources or have any wastage in the process,” Tolani says. That philosophy is embedded, quite literally, in the plant’s straight-flow layout, which runs from raw material storage through mixing, stock preparation, tyre building, curing and final finish in a single unbroken line. Even small batch sizes, he says, are produced without the wastage, excess labour or lost efficiency – what the plant’s internal vocabulary calls ‘Muri’ – that might otherwise creep in.
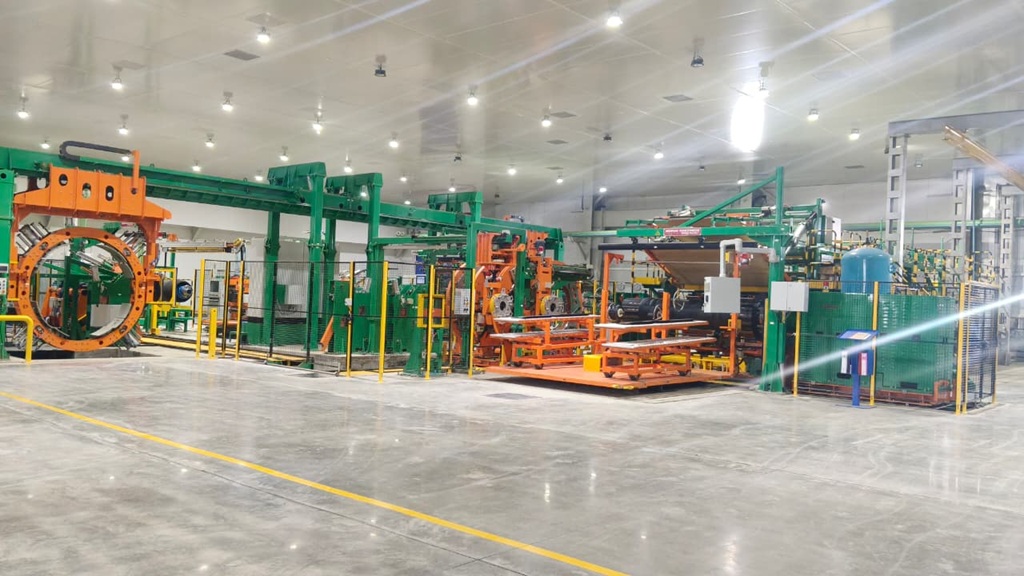
That same lean instinct underpins one of Ambernath’s more unusual competitive claims: a minimum order quantity of one. In an industry historically built around economies of scale, the plant will build a single speciality tyre to a customer’s specification without demanding batch aggregation – a capability the company says few OHT plants worldwide can match. Self-managed teams on the shop floor plan and execute changeovers themselves, allowing a highly automated, digitally traceable line to pivot rapidly to low-volume, customised orders. A related innovation, branded Unistage, builds and shapes an agricultural or OTR radial carcass into its final toroidal form on a single drum rather than the conventional two-stage process, reducing the handovers.
AN R&D CENTRE BUILT FOR SPEED, NOT SCALE
CEAT Specialty operates a dedicated in-house research and development facility at Ambernath, distinct from the group’s broader R&D infrastructure, and Tolani is candid about why. Tolani says, “This business is very, very different. There is no Pareto here – no 80/20 rule where a handful of product sizes serve the bulk of demand. Because farm and off-highway equipment come in such a long tail of sizes and configurations, and because the plant supplies numerous international OEMs directly, the time taken to develop, validate and commercialise a new tyre has to be compressed.”
“We needed a dedicated facility, closer to the manufacturing, so that we can quickly pilot, quickly turn around,” he adds. A new Compound Laboratory, opened in September 2025, now anchors materials science work spanning OTR, agricultural and industrial segments, while AI-assisted testing has trimmed, by Tolani’s estimate, roughly a third off the time from concept to market. The centre’s pipeline currently spans all-steel OTR tyres, a newly launched forestry range, very high flexion (VF) agricultural tyres and expanding work in earthmoving and material handling.
CAMSO ACQUIRED FOR BRAND, CHANNEL AND CATEGORY
CEAT Specialty’s move into Camso – a name Tolani values at up to USD 1 billion in brand potential across agricultural tracks, power sport tracks and material handling – may be its most consequential strategic bet. “It was a natural fit for us in terms of completing our portfolio,” he says. Ambernath, built in 2018 solely for agricultural radial tyres, gains through Camso’s new OEM ties (Massey Ferguson, John Deere) and construction-channel access across South America and Europe.
Under a three-year Michelin agreement, CEAT can currently manufacture and sell only compact construction tyres and tracks under Camso, taking over end-consumer sales in that segment – with other categories opening up once the term ends. The impact is already visible: standalone, CEAT Specialty’s off-highway mix is 85:15 agriculture to non-agriculture; with Camso’s, it shifts toward 50:50.
THE NUMBERS BEHIND THE AMBITION
Ambernath is running at 105 tonnes a day, at 92–95 percent utilisation – ahead of schedule. A further phase, due within 45 to 60 days, will lift capacity to 160 tonnes. Camso, still integrating, runs at roughly 50 percent.
Off-highway tyres make up close to 20 percent of CEAT’s speciality revenue, with the agriculture-to-non-agriculture split narrowing from 85:15 to near 50:50 once Camso is included. Domestically, Tolani credits GST reforms for a strong OEM market, led by Mahindra and TAFE, while mining stays flat – a segment Camso’s construction heritage should help lift as the new all-steel OTR line comes online.
Inside CEAT’S Factories Of The Future: A Conversation With Jayasankar Kuruppal
- By Sharad Matade
- October 09, 2026
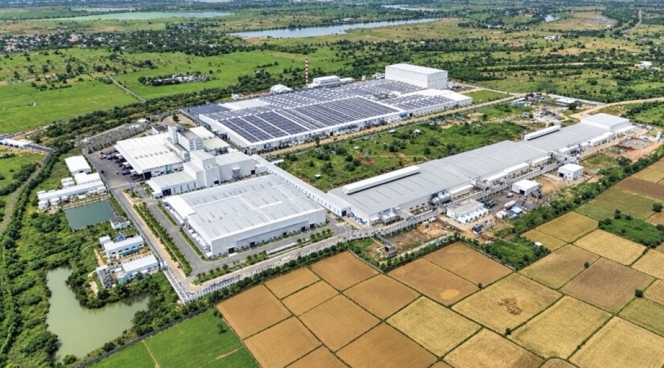
When the World Economic Forum inducted CEAT’s Chennai facility into its Global Lighthouse Network in January 2025, it made the Indian tyre-maker the first tyre brand in the world to hold two such honours – Chennai following in the footsteps of the company’s Halol plant. Add to that CEAT’s Deming Grand Prize, awarded by the Union of Japanese Scientists and Engineers for sustained excellence in Total Quality Management, and the company finds itself in rarefied company: one of only a handful of manufacturers worldwide, and the only tyre brand to hold both distinctions.
Behind these accolades sits a quieter, harder story – one of culture change, shop-floor scepticism and years of disciplined, incremental investment in artificial intelligence, the Industrial Internet of Things and automation. In an interview with Tyre Trends, Jayasankar Kuruppal, Senior Vice President, Manufacturing at CEAT, spoke on what these recognitions actually mean on the factory floor, and where the company believes manufacturing is headed next.
AWARDS AS A BY-PRODUCT, NOT THE GOAL
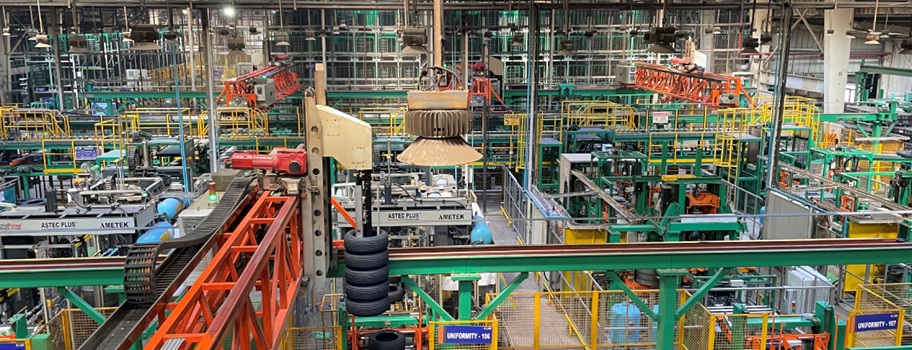
CEAT’s Chennai plant has posted striking numbers since its digital transformation began: a 54 percent improvement in dispatch turnaround, a 25 percent uplift in labour productivity, an 18 percent reduction in cycle times, a 31 percent improvement in operating cost and a 47 percent cut in Scope 1 and 2 emissions. Yet Kuruppal is quick to reframe the narrative around these achievements.
“The awards are lagging indicators, not the goal. What actually matters is what they force us to build: a common language for problem-solving across every plant, real-time visibility into quality and efficiencies and a workforce that trusts data over gut-feel,” Kuruppal said.
“That discipline shows up directly in the numbers – tighter process capability, better efficiencies and faster changeovers leading to shorter lead times. There is a commercial dividend too: global OEMs increasingly audit manufacturing maturity, and being part of the WEF Global Lighthouse Network gives us instant credibility in those conversations,” he added.
WHAT’S REALLY DRIVING THE INVESTMENT
CEAT has been pouring capital into AI, IIoT and automation across its plants. Is this cost pressure, premiumisation or a simple need to stay globally competitive? Kuruppal’s answer suggests it is all three, each playing a distinct role.
Kuruppal explained, “Quality, cost and efficiency is what gets the funding approved. Premiumisation is what’s shaping which lines we automate or upgrade first – you cannot hold the tolerances a premium radial demands with manual, operator-dependent processes.” According to him, global competitiveness, meanwhile, sets the ambition. “We’re not benchmarking ourselves against the best tyre plant in India anymore – we’re benchmarking against the best factories in any industry,” he added.
Asked to rank the three forces, he summarised neatly: competitiveness sets the ambition, premiumisation sets the sequencing and cost discipline keeps the whole effort honest.
REPLICATING HALOL AT CHENNAI: CULTURE OVER CODE
Chennai’s transformation built directly on lessons learned at Halol, the world’s first tyre facility inducted into the Lighthouse Network. And when asked what proved hardest to replicate, the technology, the culture or getting the underlying processes right, Kuruppal said, “Technology was actually the easiest part to copy. A use case that works at Halol can be re-deployed at Chennai in weeks.”
But the real difficulty, as per Kuruppal, was culture, people and change management. At Halol, habits such as daily data reviews, operator ownership of quality metrics and a managerial focus on coaching rather than firefighting were built steadily over several years. Chennai, by contrast, has had to replicate that trajectory on a compressed timeline, with a workforce encountering these practices for the first time.
“We had to resist the temptation to just parachute in dashboards and call it digital. We spent real time getting the underlying process standardisation right first, because AI on top of an unstable process just gives you a faster route to the wrong answer,” Kuruppal said.
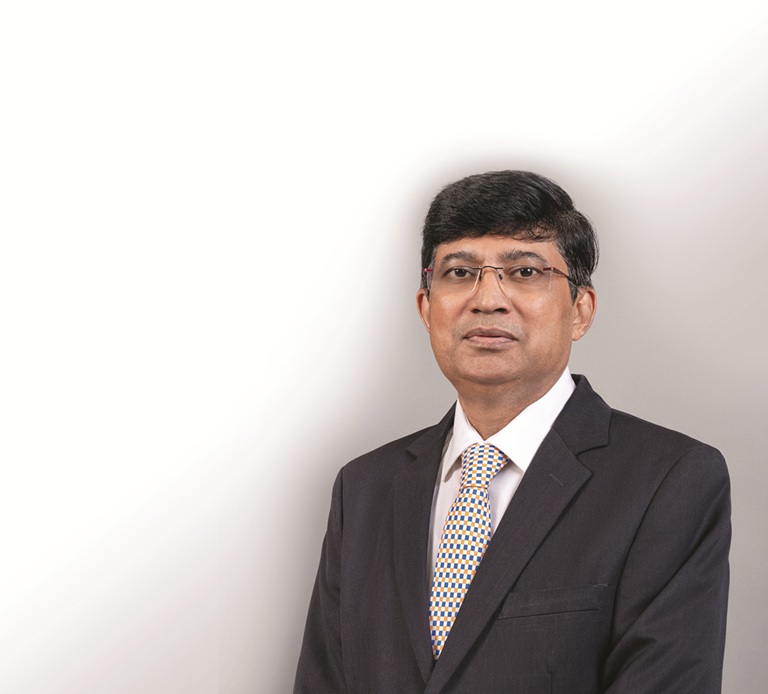
Jayasankar Kuruppal, Senior Vice President, Manufacturing, CEAT
WHERE THE RETURNS SHOW UP – AND WHERE THEY HAVEN’T YET
The productivity and dispatch gains at Chennai, he explained, hit the balance sheet in different ways. The productivity improvement lowers conversion cost per tyre and improves absorption of fixed costs as volumes grow. The dispatch improvement is more of a customer-experience story: less finished-goods inventory sitting idle, and OEMs and dealers receiving faster, more predictable delivery windows – ‘which matters a lot when you’re chasing premium and export business’.
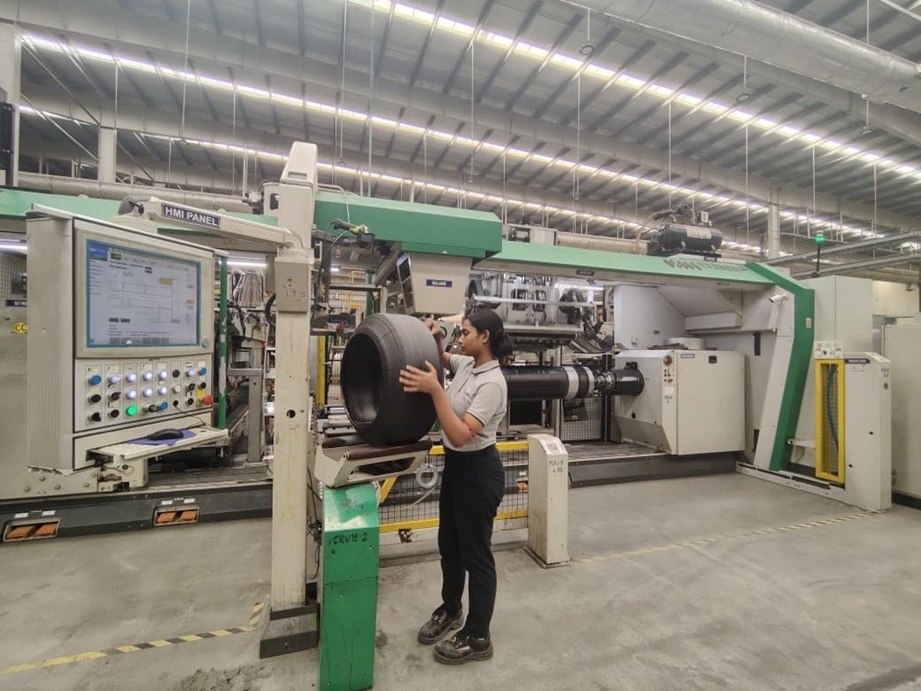 Not every initiative has paid off yet, however. Kuruppal was candid about the areas still short of return, singling out ‘some of the more exploratory AI use cases – like computer-vision pilots – which need more data cycles before the accuracy justifies scaling them further’.
QUALITY, MAINTENANCE, OUTPUT: AI TOUCHES ALL THREE
Rather than picking a single area where artificial intelligence delivers most value, Kuruppal argued that its power lies in the way it now touches quality, maintenance and output simultaneously – and that these reinforce one another. “Better quality data feeds better predictive-maintenance models, which reduces unplanned downtime, which directly lifts output,” he said. The most immediate impact shows up in more consistent product quality, higher yields and earlier detection of equipment issues. He pushed back, though, on the idea that AI at CEAT is a single flagship project: “On our floor, it’s dozens of narrow, specific use cases, each solving one operator’s or one supervisor’s actual problem.”
JUSTIFYING THE SPEND IN A MARGIN-TIGHT BUSINESS
Tyre manufacturing is not a business with room for indulgent technology spending, and Kuruppal was clear that CEAT does not fund innovation for its own sake. “Every use case has to show a clear line to quality, efficiency, cost or capacity enhancement before it gets budget,” he said. The company deliberately starts small – piloting on a single line, proving value with real production data, and scaling only what works – a discipline that means ‘the savings from scaled use cases fund the next round of pilots’. He offered a broader rationale too: in a commodity-adjacent business where raw material costs sit largely outside a manufacturer’s control, manufacturing capability itself becomes the differentiator. “If we can’t always control input costs, we can control how efficiently and consistently we convert them into tyres,” he added.
CHENNAI PLANT WIDENS ITS PREMIUM PUSH
CEAT on Oct. 1 announced an expansion of manufacturing capabilities at its Chennai plant across passenger car and SUV, commercial vehicle and two-wheeler tyres. The company said the move targets premium customers in India, Europe and North America.
What’s new
Cars and SUVs: The plant now makes the SportDrive SUV ZR22. CEAT said this makes it the first Indian tyre company to manufacture 22-inch tyres in India. It also makes the 4SeasonDrive+ all-season tyre and the CrossDrive RT rugged-terrain tyre, built for the U.S. market.
Trucks and buses: The plant can now produce seven advanced truck and bus radial sizes, including wide-base tyres that can replace dual-tyre setups, and low-profile sizes. CEAT is also scaling light truck steel radials in 15-, 16- and 17.5-inch sizes.
Two-wheelers: The SportRad Racing Slick range targets track use, and SportRad ST is a sport-touring range for motorcycles above 650cc.
“This investment strengthens our ability to compete in premium segments with products developed and manufactured in India,” CEAT managing director and CEO Arnab Banerjee said.
The 163-acre plant in Sriperumbudur, Kanchipuram, runs on connected machinery and real-time analytics. It also has a 9 MW rooftop solar installation and operates as a zero-liquid-discharge facility.
FROM PILOT TO SCALE: AN OPERATING-MODEL PROBLEM
With a large share of CEAT’s lines now running as ‘smart lines’, when asked what changes when a company moves from isolated pilots to scaling technology across multiple plants, the CEAT executive explained, “The problem changes completely. A pilot is a technology and data-science problem – get the model working, prove the use case. Scaling is an operating-model problem – standard work, training, change management, IT infrastructure that can handle load across sites and governance so every plant isn’t reinventing its own version of the same solution.”
CEAT has built what he calls a central playbook – reusable architecture, common data standards and the ability to roll a proven use case out to a new plant in weeks rather than months. “Just as importantly, ownership shifts: at pilot stage, a project team owns the initiative; at scale, it must become the plant’s own way of working, run by operations rather than a digital team sitting alongside it,” he added.
BRINGING 80 PERCENT OF THE WORKFORCE ALONG
CEAT reports that more than 80 percent of its workforce is now digitally enabled – a transformation Kuruppal admits did not come without resistance. “Yes, and I’d be understating it if I said otherwise,” he said. Crucially, he insists the resistance was never really about technology itself but about ease of operation. What worked, he explained, was making tools visibly useful to the person using them first – an operator seeing a dashboard that helps them hit their own target before it ever becomes a management reporting tool. CEAT invested heavily in shop-floor-specific training rather than generic digital-literacy courses and made a point of promoting from within, demonstrating that digital skills opened up better roles rather than closing off old ones. The company has also created new shop-floor roles beyond data scientists and engineers – ‘Business Translators’ and ‘Champions’ who act as torchbearers driving scaled implementation and wider blue-collar involvement.
CONSISTENCY, NOT JUST DEFECT COUNTS
Asked whether tighter process control has genuinely reduced defects, Kuruppal reframed the question around consistency. “Tighter process control means less batch-to-batch variation, which matters enormously in tyre manufacturing because so much of performance and durability comes down to material consistency through mixing, extrusion and curing,” he said. Real-time monitoring now catches drift early, rather than at final inspection – both a quality win and a material-efficiency win, in the form of less scrap and rework. The habit that has changed most, he said, is that quality data now drives daily decisions on the shop floor, rather than featuring only in a monthly review.
MANUFACTURING FOR A PREMIUM, ELECTRIC FUTURE
CEAT’s push into premium tyres calls for a step-change in manufacturing discipline. “Premium tyres are far less forgiving of variation, so the shift starts with tightening process capability across every stage – not just final inspection. That means more precise equipment, better process capability and closed-loop control,” said Kuruppal. In this context, flexibility takes on a different meaning: a wider SKU mix, smaller batch sizes and faster changeovers are pushing the company towards more modular manufacturing, alongside a workforce increasingly weighted towards process engineering expertise.
Electric vehicles introduce an additional layer of complexity. EV tyres must carry greater weight, handle instant torque and operate more quietly, tightening specifications around structural strength, noise and rolling resistance beyond those of conventional tyres. On the shop floor, that translates into new compound formulations requiring precise mixing, reinforced construction demanding tighter control of building machines and significantly lower tolerance for micro-variation.
CEAT’s existing leadership in the e-two-wheeler tyre segment, Kuruppal noted, is already feeding lessons – particularly on noise and efficiency – into how the company prepares lines for growing e-four-wheeler volumes in India.
 SUSTAINABILITY AND RESILIENCE, BUILT IN
Sustainability, once a separate reporting exercise, is now ‘a line item in almost every manufacturing decision’, with energy and emissions sitting alongside cost and quality when evaluating new processes or equipment – Chennai’s 47 percent emissions reduction being the clearest proof point. Resilience, too, has become as much a data problem as a sourcing one. “Real-time visibility into inventory, machine health and production schedules means we can see a disruption coming and reschedule around it rather than reacting after a line has already stopped,” Kuruppal said, pointing also to greater flexibility in shifting product mix between lines and earlier warning signals from digitised supplier and logistics data.
SPEED AS A COMPETITIVE WEAPON
Manufacturing speed and flexibility, Kuruppal argues, have become one of CEAT’s most important competitive dimensions, as OEMs compress their own development cycles and expect tyre partners to match their pace – faster prototyping, faster line trials, faster ramp-up to volume. Chennai’s faster dispatch turnaround is part of the same story. “It’s not just about making tyres faster; it’s about the whole chain from order to delivery being more predictable and quicker,” he said.
GROUND STILL TO COVER
For all its Lighthouse credentials, Kuruppal was refreshingly honest about the distance still to travel. “Being part of that network is genuinely humbling. You see factories in electronics and consumer goods running end-to-end AI-driven planning and quality systems at a level of maturity we’re still building towards – particularly in advanced analytics for demand-and-production planning and in scaling generative-AI use cases beyond pilots,” he said. CEAT’s strength, he believes, lies in shop-floor execution and quality; the next frontier is connecting that data seamlessly across the full value chain, from raw-material sourcing to the end customer.
MANUFACTURING AS A GROWTH DRIVER
Perhaps the most striking shift Kuruppal describes is a change in how manufacturing itself is perceived within the business. “Traditionally, manufacturing was viewed in this industry as a cost centre that executes what sales and product teams decide,” he said.
“Today, our manufacturing capability is directly opening up premium and export opportunities, because global customers evaluate factory maturity as part of their sourcing decision. It works in the other direction too, shaping which premium and EV products the company can confidently commit to launching. Manufacturing has moved from being an execution function to being a genuine input into growth strategy,” he added.
WHAT COMES NEXT
Looking ahead, Kuruppal frames the next horizon as connecting what CEAT has built plant-by-plant into a single, integrated digital thread – spanning raw-material and demand planning, production and distribution – so decisions are optimised end-to-end rather than site-by-site. Generative AI, he said, is increasingly being explored for process and equipment troubleshooting and knowledge capture, making the expertise of CEAT’s best engineers accessible across every plant. Sustainability, meanwhile, will be designed into new lines from the outset rather than retrofitted. “The common thread is moving from isolated smart use cases to a genuinely integrated smart manufacturing system,” he explained.
THE ONE NUMBER THAT MATTERS
Answering the question on if he could track just one metric across every CEAT plant, what would it be, he admitted, “If I’m honest, no single number tells the whole story, but if forced to pick one, it would be Overall Equipment Effectiveness – OEE.”
“As a composite of availability, performance and quality, a healthy and rising OEE generally signals that machines are running, running at the right speed and producing good tyres – which is really the definition of a plant working as it should,” he said. It has its limits – OEE alone won’t reveal a lapse in safety culture or the pace of digital adoption – which is why, in the end, Kuruppal names two figures he watches above all: OEE and safety indicators.
Panu Ärölä Returns To Tana Oy In Territory Business Manager Role
- By TT News
- October 07, 2026
Tana Oy has appointed Panu Ärölä as its new Territory Business Manager, a role he will assume on 2 November. In this capacity, he will focus on strengthening customer and distributor relationships across designated markets while contributing to the company’s ongoing expansion within the waste management and recycling sector.
Ärölä returns to Tana after previously serving as Sales Manager, where he developed expertise in distributor network growth. His background includes extensive international experience in sales, marketing, business development and strategic leadership. Most recently, he held the position of Head of Sales and Marketing at Jet-Tekno Oy, overseeing customer relationship development and business growth initiatives.
Gerd Schreier, VP – Sales, Marketing & Channel Development, said, “We are delighted to welcome Panu back to Tana. His industry knowledge, customer focus and experience in international sales make him a valuable addition to our team. We look forward to working with him as we continue to develop our business and create value for our customers and partners.”
Comments (0)
ADD COMMENT