Making The Tyre Industry Truly Sustainable
- By TT News
- December 15, 2025
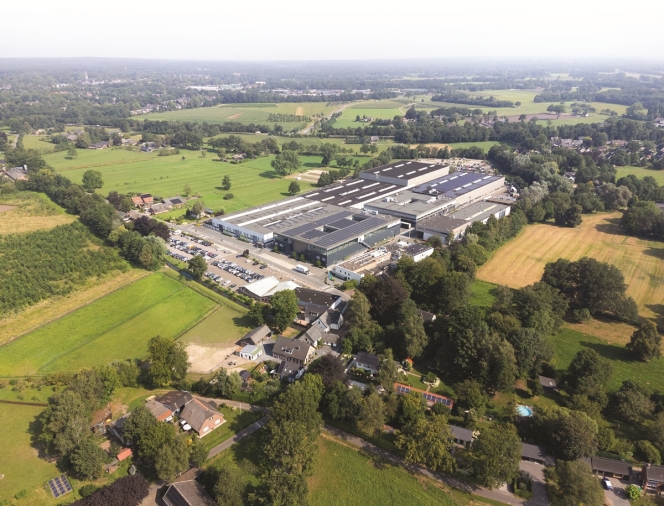
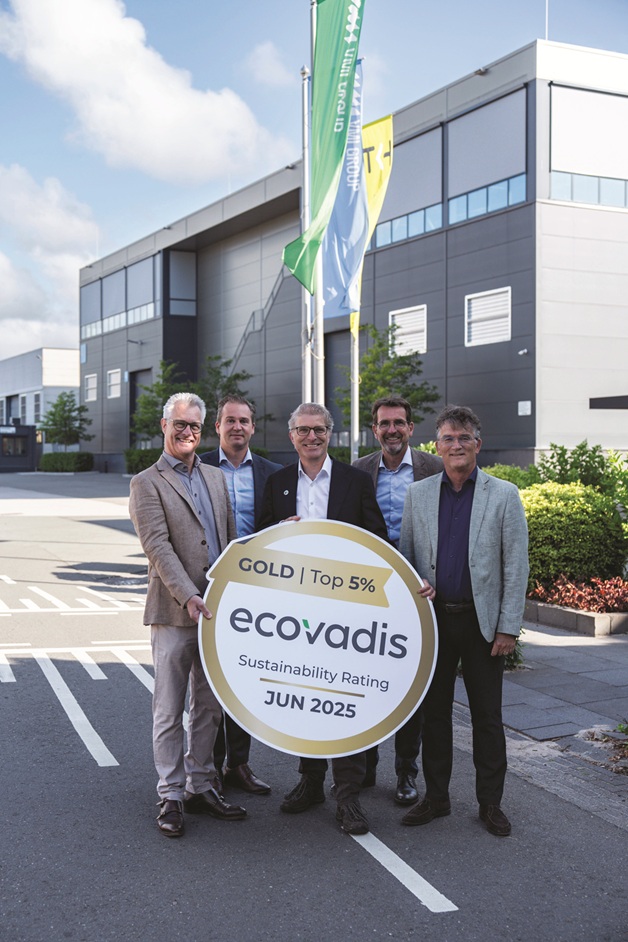
Harm Voortman, Chief Executive of VMI Group, explains how his company is mobilising its resources to cut energy use and reduce emissions, together with other forms of pollution in its strategic drive to make the business more sustainable and environmentally responsible. Having just been awarded the prestigious EcoVadis Gold Award in recognition of the progress made already, VMI is determined to keep enhancing its own performance while helping customers worldwide achieve better sustainability.
A STRATEGIC INDUSTRY
Tyres are essential for the modern economy. That’s a simple fact of life because much of the global economy depends on motor vehicles, and all those vehicles run on tyres. Two billion tyres are made every year across the world, and a high proportion of these are built on tyre building machines designed, built and supplied by VMI.
There is, however, another side to this story of economic and manufacturing efficiency. Those two billion new tyres every year also translate into something like six million tonnes of microplastics. These highly polluting particles end up in the environment – much of it in the oceans of the world. This means that one of the essential drivers for the global economy is also a major contributor to pollution and environmental damage.
The big question for all of us is how can we maintain the benefits of the tyre industry while also finding ways to reduce the harms it causes. In other words, how can we make it transformationally more sustainable?
OUR GREATEST CHALLENGE?
Sustainability is “not just a nice to have” it is an essential and non-negotiable requirement for every manufacturer and operator of automotive products.
Motor vehicles still largely use fossil fuels and require roads that must be built across the countryside, then constantly maintained and upgraded. Inevitably, this causes environmental damage.
 Tyres are made from increasingly complex blends of materials, which are used to make the novel compounds required to meet the changing demands of the automotive industry. This requires a huge amount of energy and a continuous stream of raw materials.
The move to electric vehicles (EVs), a key factor in making the industry more sustainable by reducing reliance on fossil fuels, also has one major disadvantage. EVs are often heavier than the conventional vehicles they replace. That leads to greater wear and tear on the road surface, generating a higher level of particulates that are harmful to the environment and to human health.
The need to make the entire industry less environmentally damaging, more efficient and sustainable is a challenge that every participant – car and truck manufacturers, energy companies and, above all, tyre builders – have no choice but to face. Here, as in so many other ways, VMI is leading the way.
COMMITMENT TO INNOVATION
 VMI has become a strong and respected global player because it is an innovator. Many of the concepts that have transformed the tyre industry were developed by VMI, including ‘hands off, eyes off’ automation, advanced visions systems and now the use of AI to help eliminate errors and optimise production.
Yet perhaps the most important application for innovation today is in sustainability. Fresh ideas in this field lead to better environmental performance, assured regulatory compliance and to better commercial results as well. VMI believes that doing the right thing for the planet can also lead to the best outcome for shareholders.
The drive for enhanced sustainability has become a major focus for all VMI’s employees: one of its most striking features is how it involves everyone, at all levels and in all disciplines. This has become a personal goal, with every member of the wider VMI team committed to looking for new and better ways to reduce the environmental impact of their work.
At all times, the aim is to look for new methods that can deliver a real win-win to manufacturers and customers.
There is a continuing search for ways to use less energy in production, reduce waste and scrap, while eliminating errors – thereby cutting down on the amount of materials used. Reducing emissions and pollution also leads to business benefit, because less energy used means lower costs. Less scrap and waste leads to improved efficiency and, once again, cuts costs significantly.
Tyre manufacturers understand better than ever that commitment to sustainability is not just responsible, not just essential for regulatory compliance and being a good corporate citizen: it also ends up being good for shareholders through higher profits and better brand reputation.
KEY FOCUS AREAS FOR SUSTAINABILITY IMPROVEMENT
VMI’s policy focuses on four main areas of activity:
- Energy and emissions
- Efficient use of materials
- Eliminating errors and waste
- Whole lifecycle management
This strategic approach has delivered measurable benefits to VMI and also helps customers to improve their own performance. The positive impact on environmental performance is also now a matter of public record.
So how can other manufacturers learn from the approach taken by VMI? Let’s look at this in more detail.
ENERGY AND EMISSIONS
Improved energy efficiency does not usually make progress through a few big breakthroughs: instead, it’s the sum total of small improvements made to every stage of every process, and that involves the work of every employee in every department. From the design stage on, energy efficiency is a key factor in new concepts, but, at the same time, each team of engineers is accountable (and rewarded) for identifying ways in which their objectives can be reached more efficiently by using less energy.
This process starts very early. VMI sponsors educational programmes designed to build energy consciousness into future engineers from very early on and each team is empowered to scrutinise their processes critically to develop better methods. Above all, VMI and other responsible manufacturers use the regulatory system not as a painful duty to be obeyed but as a useful incentive for better performance.
Just as every employee has to be engaged in the drive for sustainability, VMI has taken the view that every supplier and partner also needs to be actively mobilised to enhance every aspect of sustainability performance. VMI’s vision is closely aligned with the EU’s adoption of the GHG Protocol’s Scope 1, 2 and 3 frameworks, which require manufacturers to account for their entire value chain emissions, not just those under their direct control.
Scope 1 covers direct emissions, Scope 2 includes indirect emissions from purchased energy and Scope 3 encompasses all other upstream and downstream indirect emissions, obliging manufacturers to take responsibility for the environmental impact of their entire value chain while driving sustainability across their supply chains.
By working actively with suppliers on every aspect of joint working, it is possible to enhance everything from component design, fabrication methods, transportation efficiency and even packaging to ensure progressive and measurable improvements. By making this not simply a ‘box ticking’ exercise but a mission that engages every participant, extraordinary improvements have been – and will continue to be – delivered.
EFFICIENT USE OF MATERIALS
One of the most important aspects of tyre design is the growing use of advanced new materials designed to reduce weight without any loss of tensile strength or safety performance, cut down on rolling resistance, reduce particulate emission and enable higher efficiency in operation. The rise of EV use is a key factor in driving this kind of research as EVs are often heavier, have different driving characteristics and are moving towards a self-driving future.
Every tyre manufacturer is now committing considerable resources into developing materials with precisely calibrated operating characteristics. They also need to deliver specialised tyres in smaller batches then before without waste, on time and efficiently enough to make a profit even from very short production runs.
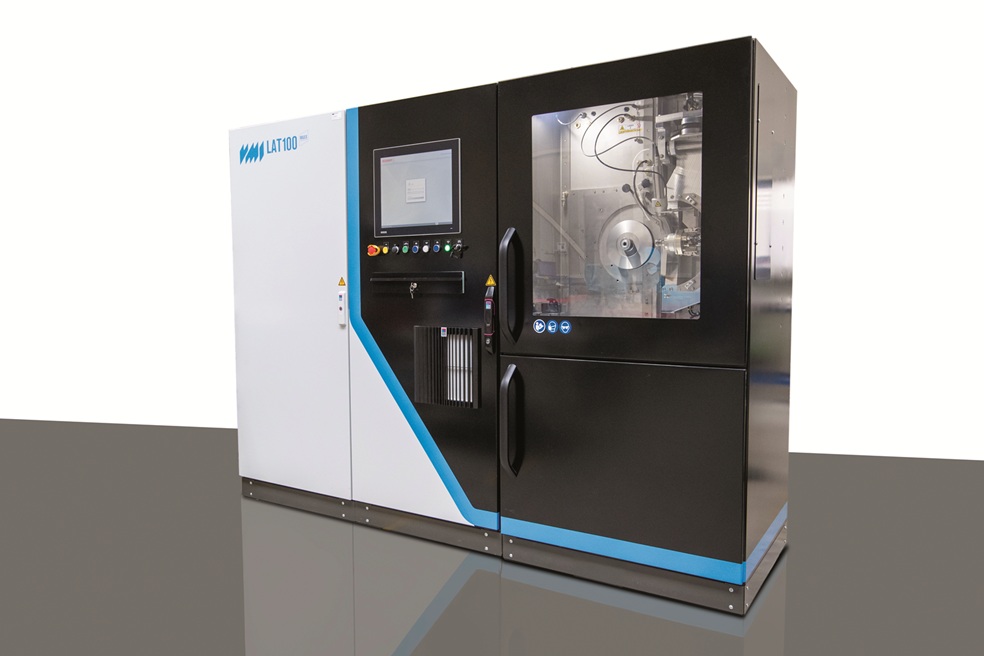
VMI focuses on developing and testing new compounds in the lab without the need to rely only on trial and error. Lab testing is not a new technique – the VMI LAT100 tyre tread compound tester was first developed some decades ago – but use of advanced simulation software now means lab testing can be embedded within the tyre design and development process as never before. New compounds can be made, tested, evaluated, fine-tuned and tested all over again within (using a term borrowed from the software industry) a ‘DevOps’ approach to manufacture.
In this concept, there is no firm line between disciplines (design, build, test, core engineering…) because the entire end-to-end process is treated as an integrated whole. The tyre industry knows that new and higher performing, more sustainable compounds are a core requirement for staying competitive into the future. VMI’s integrated, lab-focused approach can fast-track new concepts and, used with new developments in continuous mixing and extrusion, this is a practical way to accelerate development without significant environmental impact.
ELIMINATING ERRORS AND WASTE
Tyre building, even with automated production systems, requires a complex blend of processes. In practice, it is as if a series of ‘just in time’ activities co-exist within a single factory with different machines, often supplied by different manufacturers, fabricating components, many of which are then moved to where the next process takes place.
There is huge scope for wastage in the average tyre factory as materials are loaded, unloaded, moved by truck or automated vehicle, put into storage until needed, then reloaded onto another machine, processed, stored again…
Innovators across the industry understand that the sheer complexity of this approach limits both the energy savings and emissions reduction that can be achieved – for the moment. Yet new technologies are being used today to make significant progress possible. Again, VMI has been a major innovator in this field as well.
OPEN SIDE BAR
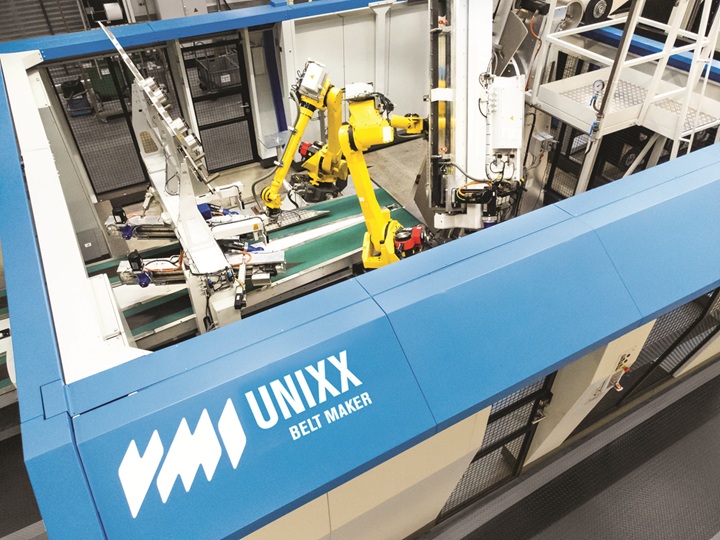
There are many ways in which taking an integrated view of tyre building processes can bring greater efficiency with better sustainability performance to the whole process. VMI has taken aspects of its UNIXX single cell technology to deliver standalone solutions that can be used with a conventional TBM to streamline conventional methods, leading to greater efficiency, reduced footprint, drastically lower energy use and better sustainability performance.
The UNIXX Beltmaker, for example, cuts out the need for a separate calendering line with the massive energy use and huge space required. By using UNIXX Beltmaker, and considering use of continuous extrusion Strip Winding, it is possible not just to eliminate process stages but accelerate production and build smaller batches without damaging profitability. All this can be achieved with lower energy use, reduced emissions and much lower wastage.
CLOSE SIDE BAR
VMI introduced vision systems to measure the placement of materials as they enter a MAXX automated Tyre Building Machine (TBM). Now these increasingly advanced vision systems are being matched with emerging AI to improve other aspects of performance. This enables automated placing, use of pattern recognition and machine learning (ML) to deliver accurate cuts and AI algorithms to ensure higher efficiency in materials usage, leading to a major reduction in all aspects of wastage due to errors.
VMI, like other businesses in the wider industry, is investing heavily in specialised software development and management, with AI now forming a major part of its solutions.
Beyond the hype caused by GenAI, we can see that the combination of sensors, pattern recognition, ML and data analytics is a proven AI combination that delivers higher sustainability through reduced waste, scrap, rework and energy investment. The intelligence of each system is now greater than ever and the sustainability benefits are increasing in step.
WHOLE LIFECYCLE MANAGEMENT
VMI moved from building standalone machines some years ago and now specialises in Production Platforms, which are designed to be updated regularly over an extended lifecycle. VMI tyre building machines are designed to operate at maximum efficiency over a very long lifecycle (between 10 and 20 years is normal), and the Platform approach adds value by making it easier to keep machines operating at best practice level. They are designed to make it easy for higher performance components, assemblies and upgrades to be retrofitted over the lifetime of the product.
The goal now is to make sure that the TBM at the heart of any production facility lasts for longer, continues to meet sustainability goals, remains highly efficient and is always at best practice level. Yet, that is not the whole story. VMI is also aware that end-of-life is part of the process as well and that all systems must be designed for safe recycling (including extended life for specific components) and environmentally responsible disposal.
End-of-life management has to be designed into a product from the very start. This is now a basic requirement for all VMI machines.
WHAT ABOUT THE FUTURE?
The tyre industry is essential for almost all aspects of economic life. The world economy runs on the road, and every vehicle runs on tyres. This simple truth means that every method we can find to improve performance in terms of efficiency and sustainability is a benefit to the world.
This is why the VMI approach matters. It was VMI that enabled the whole industry, not just the ‘Tier Ones’, to use the most advanced, automated systems in their daily activities. Others have followed – yet VMI’s pioneering work in creating and making available automated production systems, even to relatively small companies, has been transformational.
Today, MAXX for passenger tyres and MILEXX for trucks are in use worldwide and have made it possible for companies originating in China and India, for example, to challenge the biggest companies in the world, while many other countries have become major production hubs for the industry. VMI has had a permanent presence in China for almost 30 years and has important centres in India, Brazil, Thailand, US, Poland, Germany, Malaysia and, from the end of this year, in Mexico as well.
There is a clear roadmap to the future for the industry wherein we will see an increasing use of specialised software, including AI, to reduce human touch points still further, cut out errors and optimise quality. Further use of automation will reduce the need to move materials by hand and further cut wastage through optimised handling. We are already using hybrid systems, with UNIXX Beltmaker and Strip Winder, combined with MAXX TBMs to enable profitable, quality-assured building of small tyre batches.
The next step will be the use of single cell machines, in which ‘batches of one’ are the norm, with every stage of production taking place as part of the same process, cutting waste as close to zero as possible while driving down energy use and emissions still further.
The tyre industry remains at the heart of the world economy, but its very importance makes it essential for all of us who are shaping the future of this business to keep sustainability front and centre of our minds. VMI is proud of the way we combine innovation and care to deliver outstanding results for our customers, but there is still a lot of work to do, and we are already focused on the next steps.
Now and into the future: Sustainability is at the heart of our strategy.
Pirelli Softs And Mediums Frame Mexico Thriller As Kimi Antonelli Seals Historic Title
- By TT News
- November 02, 2026
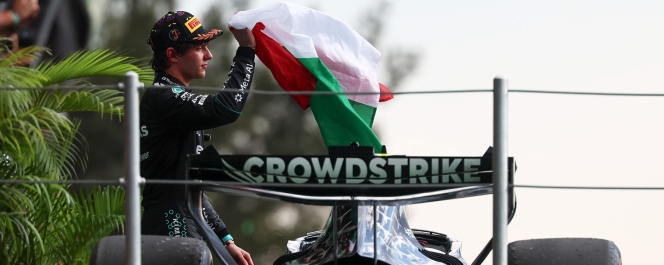
Pirelli's medium and soft compounds shaped the Mexico City Grand Prix, where Max Verstappen took victory for Red Bull and Kimi Antonelli secured the Formula 1 World Championship with a third-place finish. Lewis Hamilton completed the podium in second for Ferrari at the circuit named after the Rodríguez brothers.
Verstappen triumphed through a two-stop strategy, beginning on mediums before switching to softs on lap 27. After 18 laps on the C5 compound, a red flag stopped the race, and the Dutchman used the pause to fit another set of softs, then resisted Hamilton's challenge to the finish. Hamilton had started on softs, moved to mediums and took another set of softs during the Safety Car that preceded the red flag, later choosing a previously run soft set at the restart while setting fastest laps on both compounds.
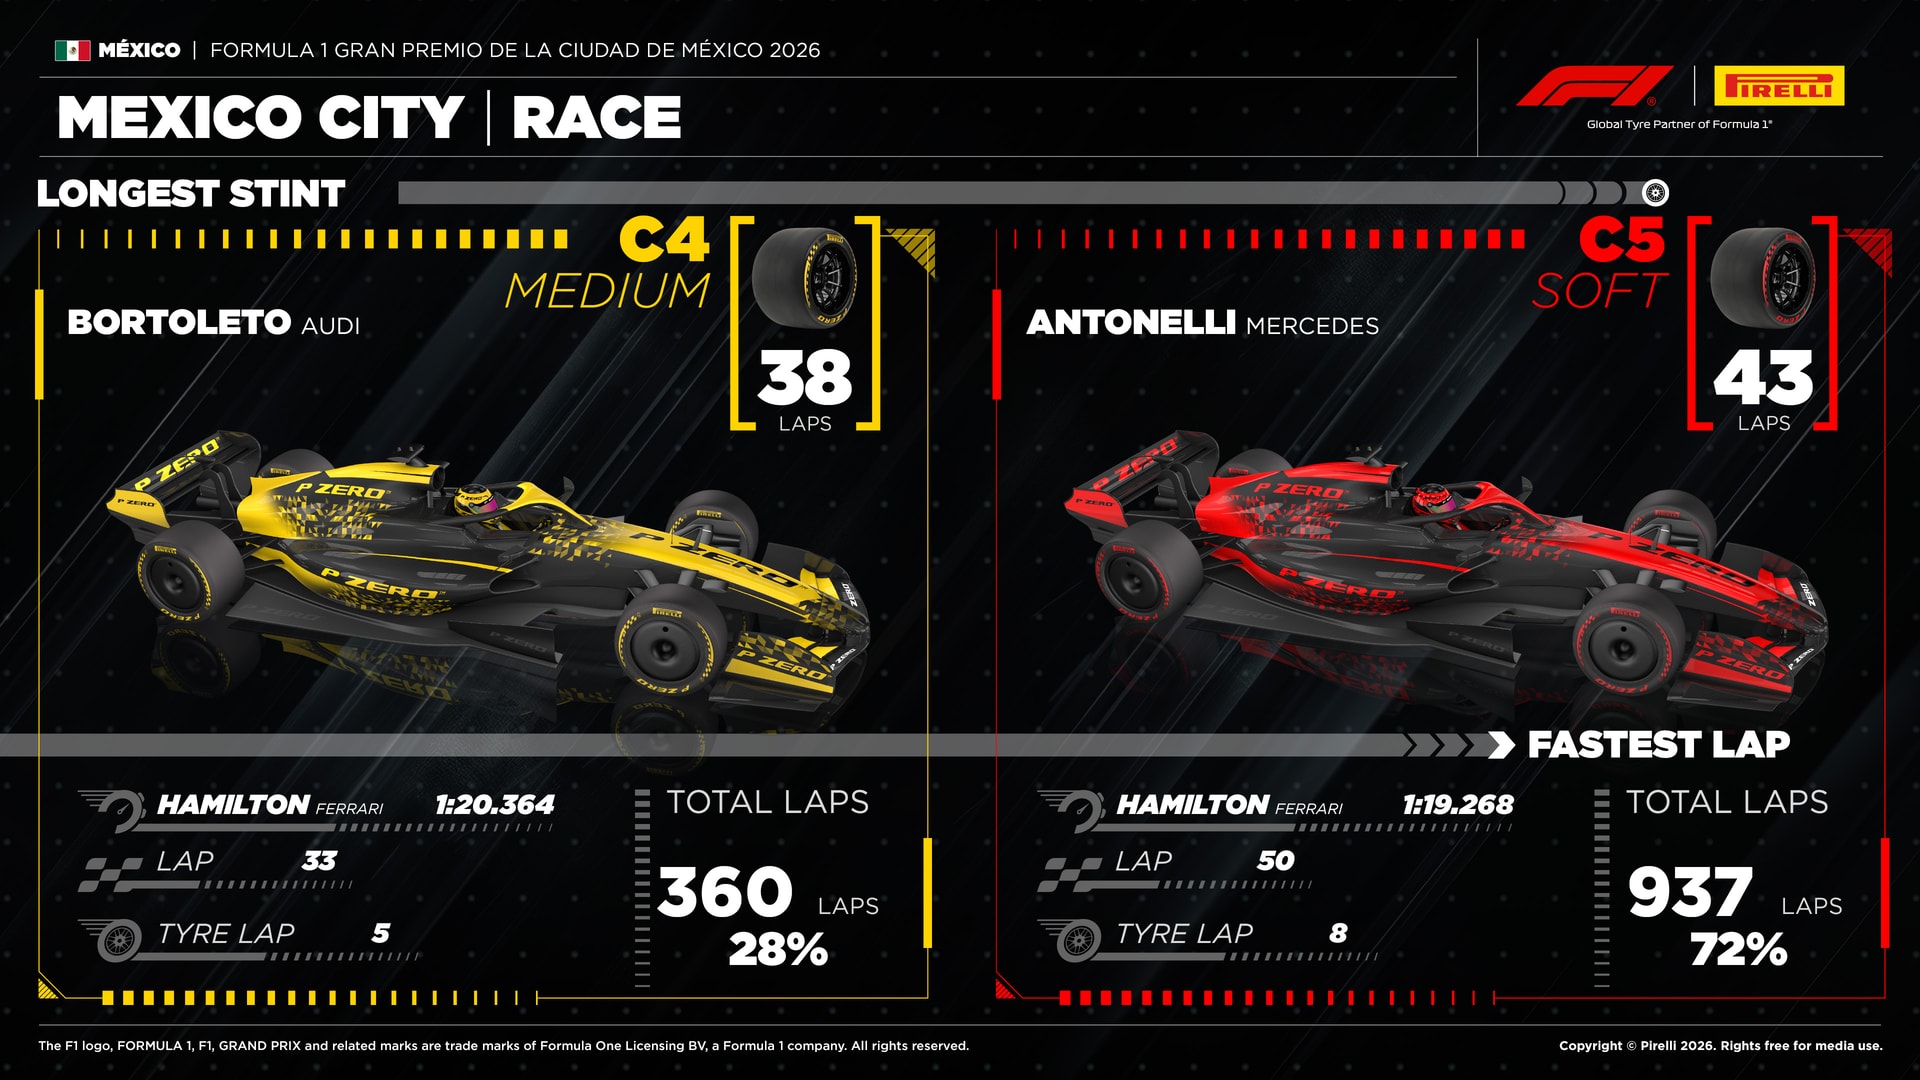
Antonelli, at 20, becomes Formula 1's youngest World Champion, breaking Sebastian Vettel's record of 23. The Italian started on softs, switched to mediums on lap 43 and used the red flag to fit another used set of softs, a strategy that delivered third place and the title. The podium contained only World Champions, with Verstappen on four titles, Hamilton on seven and Antonelli on his first.
Antonelli is the third Italian driver to claim the championship. His predecessors also won exclusively on Pirelli tyres, with Giuseppe Farina taking the inaugural 1950 title across six races and Alberto Ascari securing his second consecutive crown in 1953 by winning all eight Grands Prix he entered.
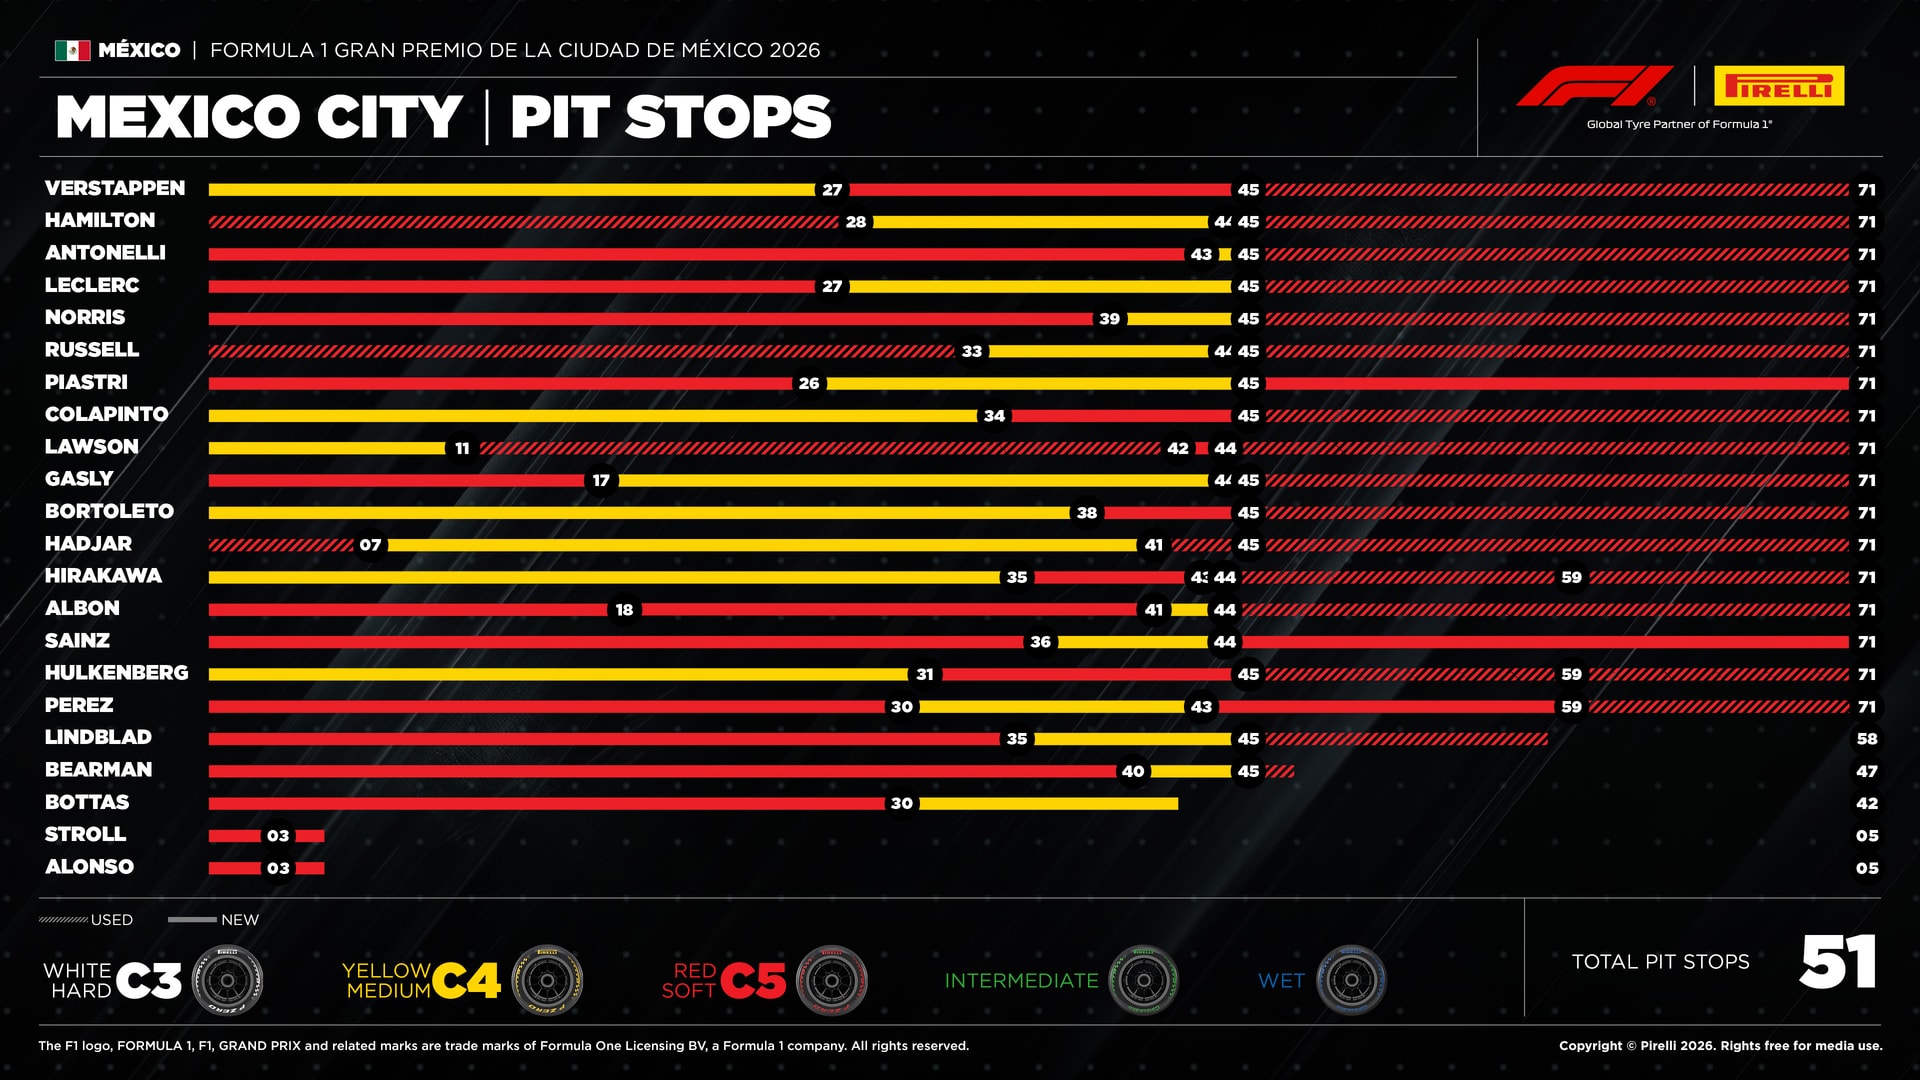
Dario Marrafuschi, Pirelli Motorsport Director, said, “Congratulations to Kimi Antonelli on winning the World Championship. It is a thoroughly deserved success, built on the consistency he has demonstrated throughout the season and sealed today with another outstanding performance, culminating in a podium finish in a race packed with drama alongside two World Champions. Without the neutralisations, a one-stop strategy would have been the most competitive option for this Grand Prix. Both the Soft and Medium compounds proved capable of covering around half the race distance, making it possible to complete the event with a single tyre change. The C5 once again confirmed itself as the benchmark compound in terms of grip and driver confidence, although the performance gap to the C4 was very small, with both compounds showing similar levels of degradation. It was therefore no surprise that every driver chose the Soft for the final stint after the Safety Car, despite also having the Hard compound available.
“From a technical perspective, tyre behaviour was very positive. We recorded no significant graining, and degradation remained within expected levels, proving lower than what had been observed on Friday. A lock-up by Leclerc at the restart following the red flag also provided further evidence of the robustness of Formula 1 tyres. The tyre sliding across the asphalt caused particularly severe localised wear on the front-left tyre, bringing it very close to the internal structural layers. This is certainly not a routine occurrence, but it is one that is consistently taken into account throughout Pirelli’s development and validation processes, including through rigorous indoor testing programmes. The ultimate objective is to ensure that the tyre maintains an appropriate level of integrity even under extreme conditions, allowing drivers to continue racing in complete safety.
“The performance of the Soft compound was particularly interesting, as demonstrated by Antonelli’s lengthy stint. He completed 43 laps while maintaining very limited degradation and a competitive pace right through to the closing stages of the race. The C3, meanwhile, was not considered by the teams because, under race conditions, it did not offer any performance advantage over the two softer compounds. Overall, the data collected confirmed a very clear picture, fully consistent with the simulations carried out before the event, both in terms of degradation and the competitiveness of the various strategic options.”
Goodyear Rolls Into Norwood's Automile With New Auto Service Store
- By TT News
- November 02, 2026
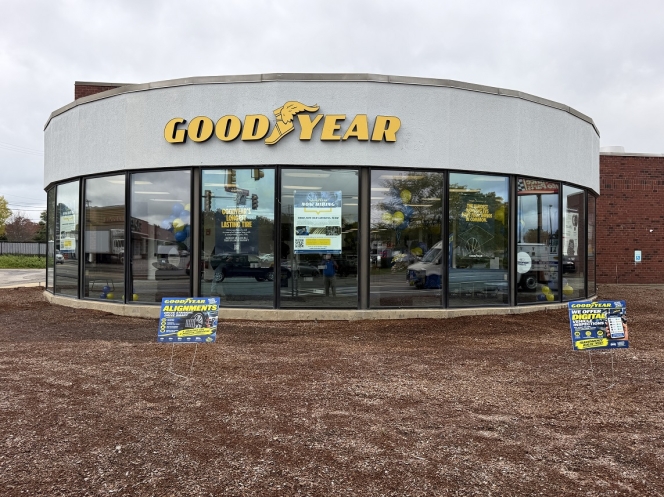
Goodyear has expanded its presence in Norwood with a new Goodyear Auto Service store at 981 Boston Providence Hwy., situated in the Automile area just off Route 1. The store marked its arrival with a grand opening ribbon-cutting ceremony on 30 September, giving local drivers fresh access to professional tyre and automotive care.
Motorists visiting the location can choose from Goodyear and Cooper tyre lines, which cater to a range of vehicles, budgets and driving preferences. Among the Goodyear offerings are the Eagle F1 All Season for year-round capability, the Wrangler Steadfast HT for dependable comfort, the Assurance WeatherReady 2 for all-weather conditions and the ElectricDrive 2 for electric vehicle performance.
Beyond tyre sales and installation, the Norwood team provides oil changes, alignments, brake service, battery replacement, air conditioning service and preventive maintenance. With heavy commuter traffic along Route 1 wearing down tyres and colder weather elevating the need for proper care, the store invites drivers to receive a complimentary tyre air pressure check or consultation. Tyre rotation, wheel balancing and TPMS inspections are also available.
Several promotional offers are currently available. Through 30 November, customers who purchase and install select Goodyear or Cooper tyres with the Goodyear Credit Card can receive up to USD 200 back, while a full-synthetic oil change is priced at USD 69.99 through 1 December at participating locations. Qualifying oil changes and services also earn up to USD 20 in Valvoline rebates through 31 December. The store operates Monday through Saturday from 7:30 a.m. to 6 p.m.
Marsha Nelson, Store Manager, said, “Backed by more than 125 years of expertise, our Goodyear team is ready to help customers choose the right tyres and provide the service their vehicles need to get them where they’re going with confidence. We’re committed to exceptional customer service and top-quality products, and we look forward to building lasting relationships with Norwood-area drivers and their vehicles.”
Maxxis Victra RC-1 Tyres Headed To SEMA On Nissan Project NAT2
- By TT News
- November 02, 2026
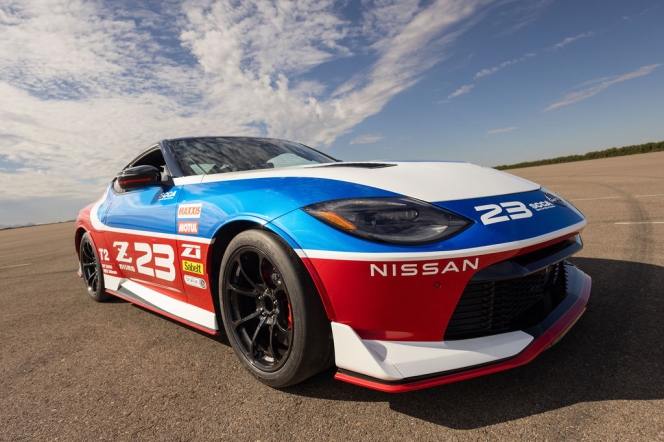
Maxxis International will display its Victra RC-1 tyres on Nissan's Project NAT2 SCCA Touring 23 car at the SEMA Show 2026, scheduled for 3–6 November at the Las Vegas Convention Center, continuing a partnership with the Nissan Acceleration Team (NAT) that dates to 2020. NAT is an all-volunteer motorsports group staffed by Nissan employees, and the Victra RC-1 has become a popular choice among club racers and enthusiasts for its grip, handling and heat cycle performance.
Project NAT2 is a Nissan Z fitted with upgraded engine, suspension and braking systems for the SCCA T2 road-racing class, which balances performance across production-based sports cars and sedans through rules on eligibility, modifications, weight and tyres. The car will run on 100TW Victra RC-1s in 275/35ZR18, retaining much of its production character while being prepared for serious wheel-to-wheel competition with safety, handling, braking and reliability upgrades.
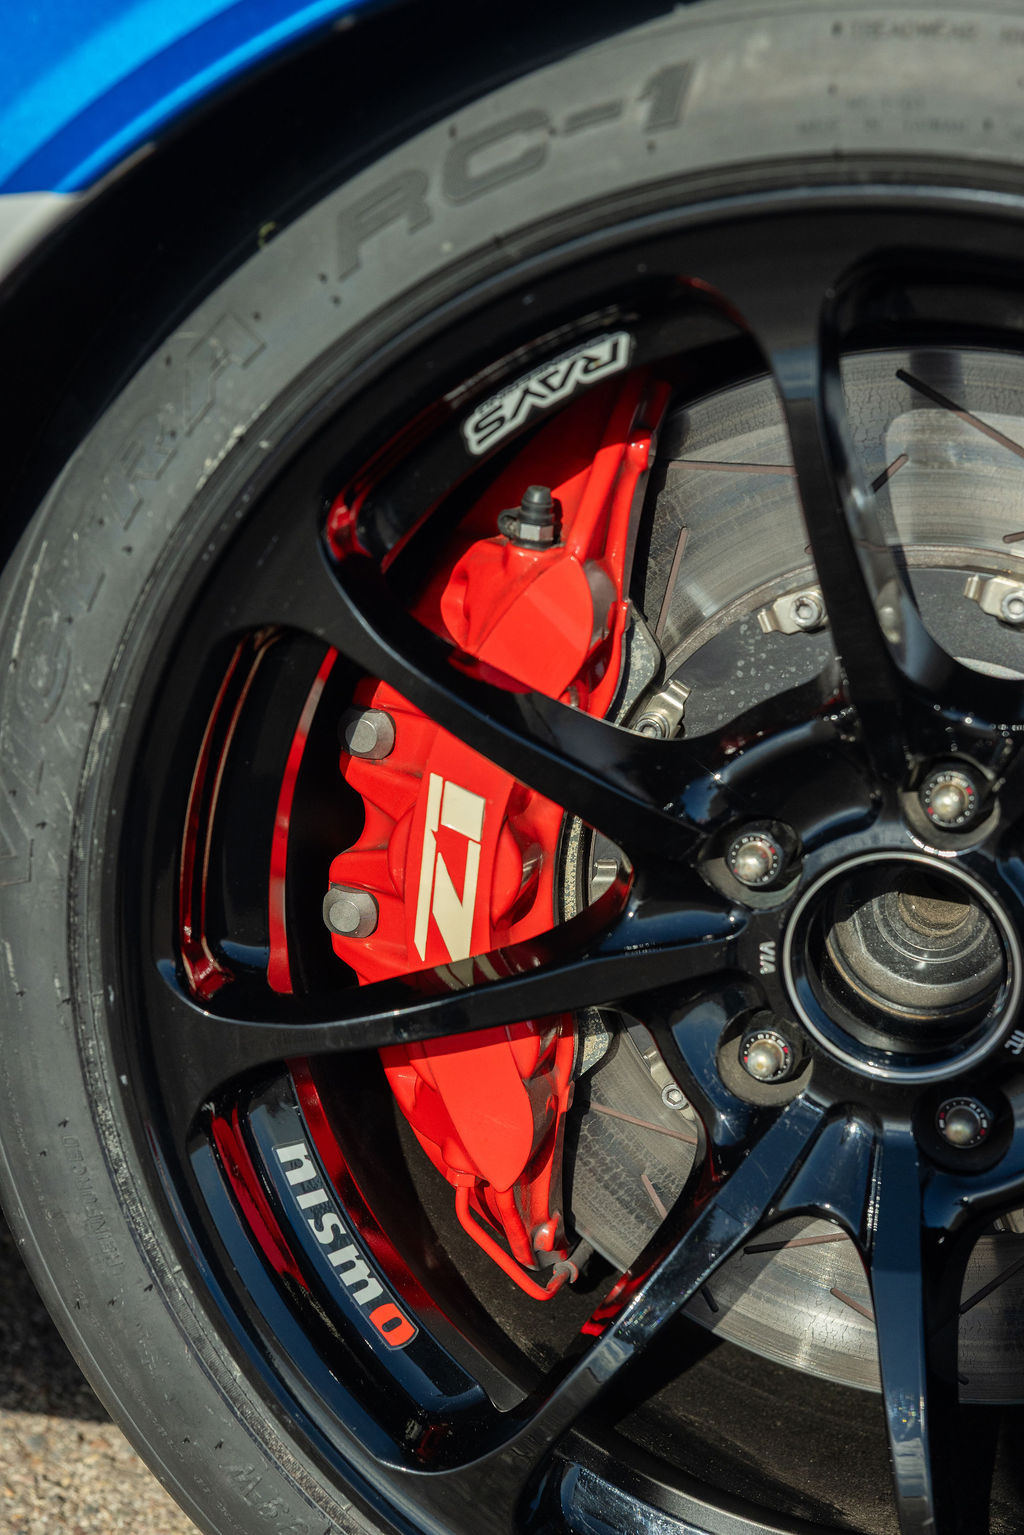
Visitors can see the Project NAT2 Z and its Victra RC-1 tyres at Nissan's Booth #21521 in Central Hall at the Las Vegas Convention Center. Additional Maxxis tyres are on display at the outdoor booth #82002 in the Silver Lot and the indoor booth #41086 in South Hall Lower near the Bronze Lot.
Hankook Tire Hosts '2026 Design Innovation Day' Outlining Design Strategy Across Key Brands
- By TT News
- November 02, 2026
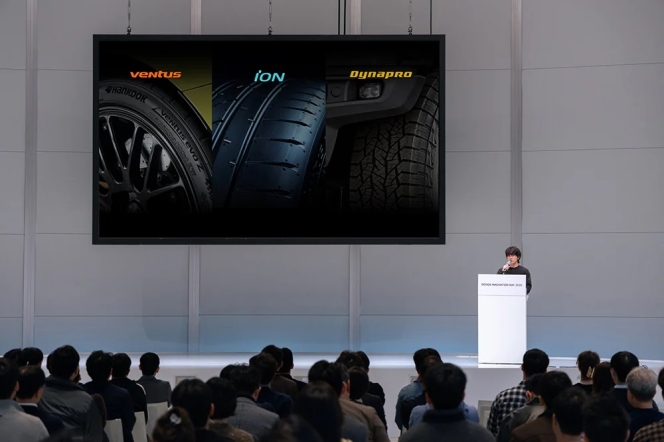
Hankook Tire held its 2026 Design Innovation Day on 30 October at Hankook Technodome, the company’s advanced research and development centre in Yuseong-gu, Daejeon, South Korea. The event, themed ‘Shaping Identity, Sculpting Performance’, gave employees a chance to learn about the tyre maker’s design strategies and major accomplishments.
A central highlight was the company’s first public presentation of a unified product design identity framework covering its principal brands: iON, the world’s first full-lineup tyre brand dedicated to electric vehicles; Ventus, its flagship line and Dynapro, its SUV-focused brand. Hankook Tire also introduced a next-generation product design language for the first time and explained how it will be applied to future products, clarifying each brand’s design direction and creating a consistent approach across the portfolio.
The programme featured three sessions. One addressed design strategies for conveying product performance while preserving brand identity and introduced guidelines for turning ‘invisible performance’ developed during R&D into design elements consumers can recognise, with approaches tailored to different product characteristics. Another session presented the next-generation design language for iON, Ventus and Dynapro, translating each brand’s core values into distinctive design elements. Hankook Tire further shared a framework for collaboration among R&D, product planning, marketing and design teams so they can develop products under unified design standards.
Through the event, Hankook Tire seeks to align design strategies and direction across the organisation, improve product development efficiency and speed decision-making while strengthening global brand recognition and its premium image. The company also aims to bolster design competitiveness in original equipment collaborations with global automakers and in product development for global markets. Hankook Tire continues to earn international design recognition, including three Product Design awards at the 2026 Red Dot Design Awards for Ventus evo, iON AT and Laufenn S FIT2, plus six Design Concept awards comprising two Best of the Best honours and four Red Dot awards.
Comments (0)
ADD COMMENT