- Shanghai Cheeshine Novel Materials Technology
- Hai Li
- School of Polymer Materials
- Qingdao University of Science and Technology
Are Bio-Based Materials A Growing Trend Within The Tyre Industry?
- By Sharad Matade & Gaurav Nandi
- July 02, 2025
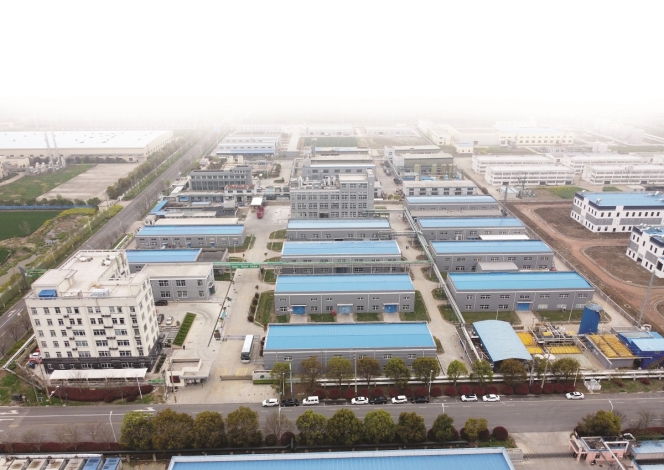
As sustainability becomes central to the tyre industry’s evolution, the spotlight is now shifting from just recyclability and circularity to a newer, promising domain – bio-based materials. While global tyre manufacturers invest heavily in de-carbonisation strategies, companies like Shanghai Cheeshine Novel Materials Technology Co., Ltd. are at the forefront of pushing this transition further. With a growing portfolio of innovative, high-performance bio-based solutions, Cheeshine is betting on the increasing demand for greener alternatives. However, as industry adoption remains cautious, especially in replacing petroleum-derived materials, the road to mainstream acceptance of bio-based materials may still require both technological refinement and a stronger market-driven pull.
Sustainability, recyclability, circularity and renewable materials are the main keywords of the current tyre industry. Companies have invested millions in its efforts towards reaching sustainability goals and attaining a circular economy.
But there is also a new buzz word in town – bio-based raw materials. Cheeshine is confident that the tyre industry has developed an interest towards such materials in its quest towards a sustainable future.
Speaking exclusively to Tyre Trends, the company’s Director of Research and Development Centre, Hai Li, said, “Our goal is to support the rubber industry’s sustainable development. That’s why we’ve selected certain bio-based materials, and through modification, enhanced their properties to make them suitable for rubber applications. There’s growing demand for bio-based materials in tyres due to increased environmental awareness and the need for greener alternatives.”
Founded in 2005 in Shanghai, the company delivers different products and services to the rubber industry. Over more than a decade of growth, the company has expanded its footprint with factories and offices in Jiangsu Huai’an, Jiangsu Suzhou, Shandong Linyi, Hong Kong, Chongqing, Tianjin, India and France, serving a global customer base.
It maintains long-term collaboration with leading Chinese universities and in 2016 established the ‘Cheeshine Scholarship’ at the School of Polymer Materials, Qingdao University of Science and Technology to support innovation in research and development.
With strong research and development capabilities and large-scale production capacity, Cheeshine offers six core product categories including low rolling resistance silane, high-temperature resistant cross-linking agents, wet-skid resistant resins, adhesion promoters, special reinforcing fillers and environmentally friendly processing oils.
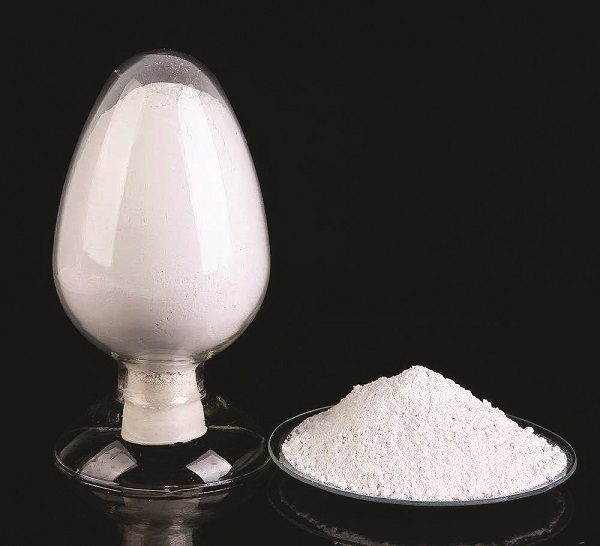
It currently holds 108 patents and several technologies for which it has filed PCTs. A standout example is its high dispersion precipitated silica by carbonisation, the precipitated silica via CO₂ substitution for sulfuric acid, a process that currently sets it apart as the only manufacturer with this capability.
MANUFACTURING PROWESS
The company focuses on the ‘magic triangle’, which, in the tyre industry, is referred to the balance between three critical performance factors viz-a-viz rolling resistance, wet grip and wear resistance.
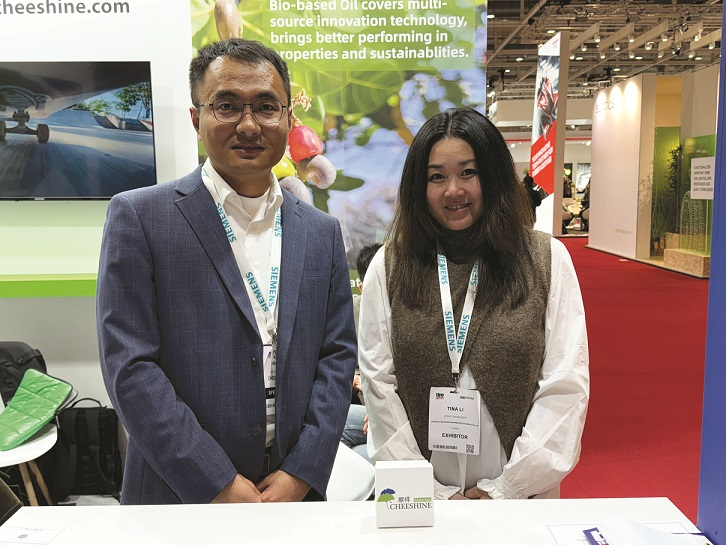
Cheeshine Materials manufactures through its three factories in China and ships worldwide. Its research and development hubs are also located within the country. “We’re a research and development-driven company. Our largest development centre is in Suzhou with over 80 team members, most of whom hold master’s or doctoral degrees. We have a total of three R&D centres. Our teams work closely with clients to co-develop customised and high-performance solutions. We have two main production bases – one in Hua’an, Jiangsu Province, and another in Shandong Province,” said Li.
The company registered a turnover of USD 120 million in 2024 and serves a global base of over 500 customers. Within the tyre industry, it majorly works with the global top 10.
Li expressed pride in the company’s innovations and emphasised on the broad portfolio of rubber additives and sustainable materials. Claiming that the company has a strong market presence both in China and internationally, he provided an overview of the core offerings.
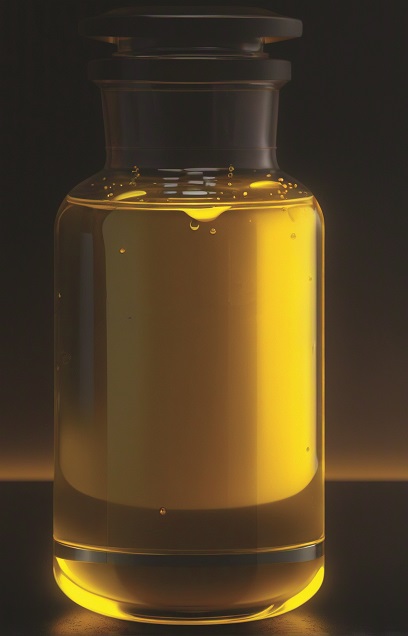 Under the category of bio-based products, Li highlighted a rubber processing oil derived from modified cashew nut shell oil, a product he claimed is manufactured in China only by his company. This oil not only improves compatibility with rubber compounds but also contributes to sustainability. Another innovation was the modified natural rubber (epoxidised NR), developed to serve as a bio-based alternative to synthetic SSBR, offering enhanced performance.
In terms of eco-friendly fillers, he pointed to the high-dispersion precipitated silica by carbonisation, which is more environmentally friendly than traditional sulfuric acid-derived silica and also improves dispersion in rubber compounds. He also mentioned a high-performance liquid rubber additive known for its excellent compatibility and market success.
For advanced functional additives, he cited the modified silane coupling agent, designed to replace TESPT and improve rolling resistance and silica dispersion and currently protected under a PCT patent. The company’s multi-functional cross-linking agent enhances durability and strength, while a line of environmentally friendly accelerators was developed to minimise environmental impact during vulcanisation.
The portfolio also includes speciality resins such as a tear-resistant resin for improved tyre durability and several wet skid-resistant resins, including AMS and modified AMS resin, hydrogenated resin, bio-based resin and modified C5/C9 resin, targeted at enhancing grip on wet surfaces. Additionally, the company produces various phenolic and formaldehyde resins for specific performance attributes like heat resistance and bonding, along with anti-reversion agents and silica dispersion agents that support high-performance compound development.
Among the company’s most cutting-edge innovations is a sulfur-free curing agent, an alternative that replaces traditional sulfur in rubber vulcanisation and enhance tyre ageing resistance and wear resistance while significantly boosting overall durability performance. This agent helps reduce tyre cracking over time and extend product life. Li noted that Cheeshine Materials is currently the only company globally manufacturing this agent and has secured a PCT patent for it.
When asked about the source of their materials, Li acknowledged that while many of the older products were petrochemical-based, the company is now strongly shifting towards bio-based alternatives including bio-oils, resins and natural rubber modifications, in alignment with the industry’s evolving sustainability goals.
MARKET TALK
While the company has a kitty of impressive offerings that might cater to the emerging and evolving demands of the tyre industry, replacing traditional materials completely is a matter that is to be taken up in the near future. Of all the raw materials that go into a tyre, replacing synthetic rubber seems to be a very vague concept for many.
 Alluding to why the industry will choose modified natural rubber over SSBR, Li explained, “Modified natural rubber offers higher bio-based content, which supports sustainability goals. Through our proprietary modifications, we enhance its ageing, physical and dynamic properties, making it a strong alternative to synthetic rubber.”
Commenting on challenges, Li said, “Our main challenge is the constant push to develop better products and solutions. Innovation is an ongoing effort. We’re continually working to modify bio-based materials like lignin. Many projects are ongoing, focused on improving sustainability and performance. On the cost front, we aim to keep the cost of our new products on par with conventional ones while providing the added value of sustainability.”
Li described that the business is fairly balanced between domestic and international markets. In terms of global expansion, he mentioned that growth is being driven through a network of affiliates and distributors. The company already has team members based in Paris, Copenhagen and Mumbai and are actively engaging with international partners to access new markets.
In response to questions about the shifting dynamics in Europe, particularly with some local plants shutting down, Li noted that the company is continuing to expand its manufacturing capacity in China. He cited the country’s cost advantages and strong pool of research and development talent as key factors. Looking ahead, the company plans to strengthen its presence in Europe by hiring more local technical support staff to better serve the region.
As for establishing a manufacturing plant in Europe, Li shared that there are no immediate plans to do so. However, the company may consider this move in about two or three years, particularly after the full commissioning of the new domestic plant as part of a longer-term strategy to navigate tariffs and support local demand.
When asked about the future vision, Li stated that Cheeshine Materials’ ambition is to become a true pioneer of the unexplored territories in the rubber industry. The focus remains on leading innovation and continually expanding the company’s global influence.
The Tyre Giant That Doesn’t Want A Dark Factory
- By Sharad Matade
- October 13, 2026
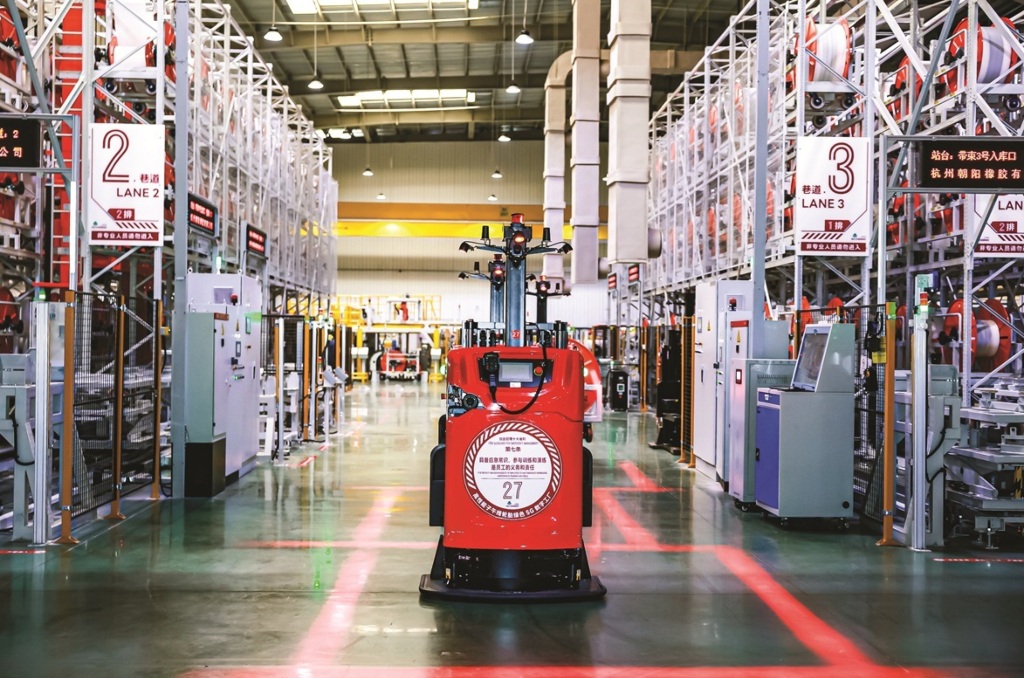
ZC Rubber, China’s largest tyre maker, is running 18 AI agents across its Hangzhou 5G plant. It insists the goal is smarter manufacturing, not emptier factory floors.
Walk into the industrial conversation about automation these days and ‘lights-out’ production tends to come up within minutes: factories with no people, no lighting and machines working in the dark. However, ZC Rubber, the Hangzhou-based group that ranks among the world’s top nine tyre companies, would like to correct that impression before it takes hold.
“We see this as a 5G Smart Factory, or Future Factory V2.0, rather than a ‘dark factory’. The goal is intelligent manufacturing, not simply removing people from the production process,” the company said in an interview.
That is a notable position from a company that has just put 18 AI agents to work across its production chain and reports defect rates well under half those of its earlier operations. It is also a considered one, and the details explain a good deal about how the world’s largest tyre market is approaching the factory of the future.
PEOPLE AT THE EXCEPTIONS
ZC Rubber’s division of labour is simple. Automation, AI and real-time data are steadily taking over what the company calls ‘repetitive and highly standardised operations.’ Its people are being moved towards engineering, process management, quality assurance and the handling of exceptions, meaning the unusual problems that no model has seen before.
“We will continue to increase automation, but fully unmanned production is not the goal,” ZC Rubber said. “It is about combining intelligent systems with human expertise.”
The same logic applies to the future. Asked whether lights-out production is on the roadmap, ZC Rubber was clear. “We do not see fully lights-out production as a goal in itself. Technology will be introduced where it brings clear improvements in quality, efficiency, safety and sustainability,” it said.
EIGHTEEN AGENTS, ONE PRODUCTION CHAIN
The scale of the AI deployment is considerable. Since June 2025, ZC Rubber has introduced 18 AI agents across the full production chain. Their use ranges from AI-assisted formulation and virtual simulation to equipment maintenance, production scheduling and quality control. According to the company, they have helped shorten tyre development cycles by 50 percent and lifted production efficiency by 50 percent.
Where does the value come from? Not from any single stage, the company suggests. “The biggest value comes from using AI to analyse production data, optimise process parameters and support faster decision-making across the manufacturing process,” it said. ZC Rubber does not currently publish a stage-by-stage breakdown of the gains.
INSPECTION AND THE DEFECT RATE
Quality control is where the company’s numbers are most striking. Its latest AI-based visual inspection systems, it says, can achieve a defect detection rate of close to 100 percent, improving both the speed and the consistency of inspection. That matters most in high-volume passenger car radial (PCR) output, where human inspectors face the twin problems of fatigue and sheer throughput.
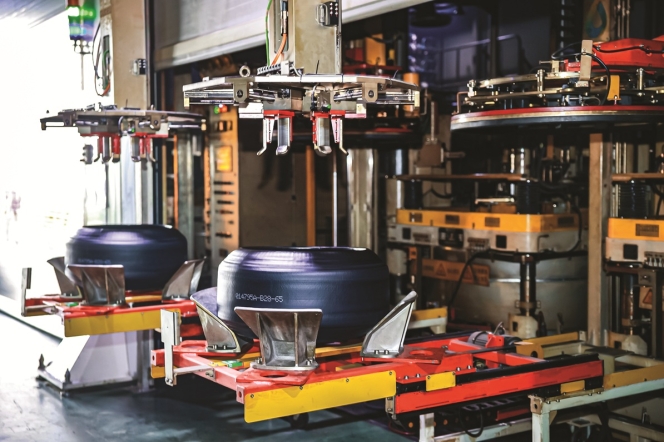
 Zooming out, the company says AI and digital quality control across its smart manufacturing system have cut its product defect rate from 1.2 percent to 0.5 percent.
HOW THE SYSTEMS TALK TO EACH OTHER
“Thousands of sensors collect production data in real time, while 5G connects equipment, quality inspection and logistics systems,” the company said. The APS+MES system pulls production, quality and logistics information into one place ‘so operations can be monitored and adjusted quickly’. AI and big data analytics then help staff spot problems and make faster production decisions.
AN EARLIER SET OF NUMBERS, UPDATED
ZC Rubber’s earlier claims of a 15 percent efficiency gain, up to 40 percent lower defect rates and a 5 percent cut in energy use make one notice that the latest figures are considerably better. The company is candid about why. “Those figures reflect an earlier stage of our smart factory development,” it said.
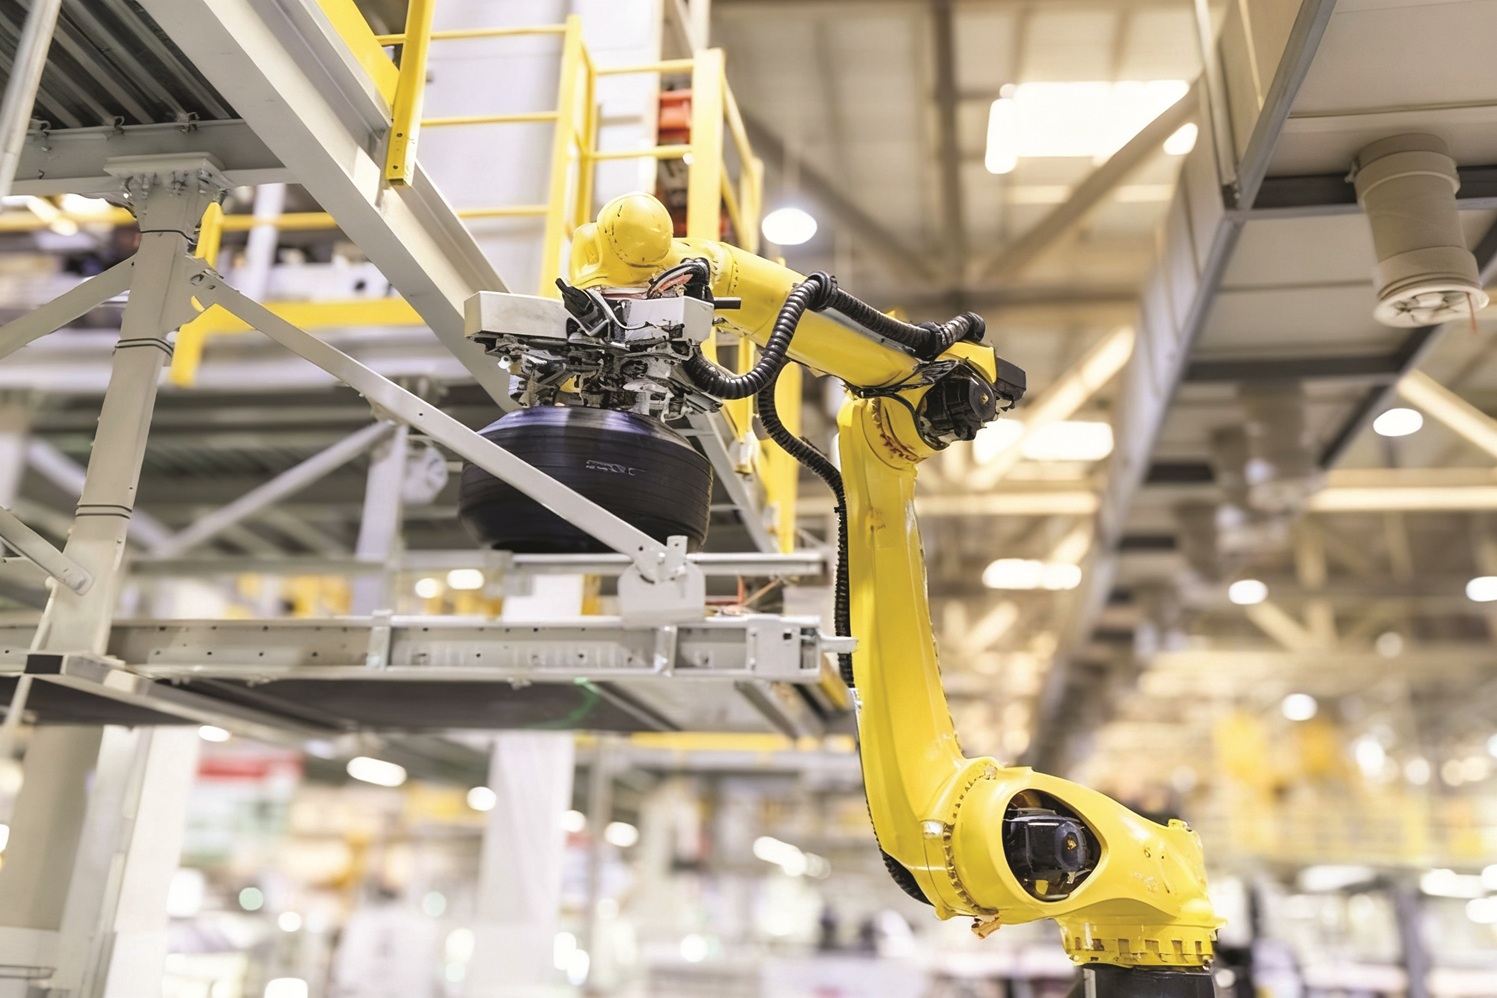
The current numbers, for the 5G Smart Factory, are a 50 percent improvement in production efficiency, defect rates down from 1.2 percent to 0.5 percent and a 10 percent reduction in overall energy consumption.
As for which technology deserves the credit, ZC Rubber declines to rank them. “We do not break down the improvement by individual technology,” it said, naming instead the key components: AI-based process control, automated inspection, intelligent logistics, APS+MES production management and data-driven quality control.
ENERGY, MEASURED VALVE BY VALVE
The energy figure is worth a closer look, because it comes from a fairly granular system. ZC Rubber’s energy management combines 5G, IoT, big data, AI and digital-twin technologies. Smart sensors, smart meters and smart valves feed real-time data into a central energy platform, while AI supports analysis and operational optimisation.
The division of labour among the technologies is neat. “5G provides the connectivity, while AI, big data and digital twins help turn the data into better energy-management decisions,” the company said.
TWO PLATFORMS AND A DIFFERENT STARTING POINT
The manufacturing story is inseparable from the development story. ZC Rubber runs two proprietary technology platforms: the X-Tech System, primarily for truck and bus radial (TBR) tyres, and the Phecda Tech System, primarily for PCR tyres. Each integrates compound formulation, tyre structure, process engineering, simulation, testing and intelligent manufacturing within a single development framework.
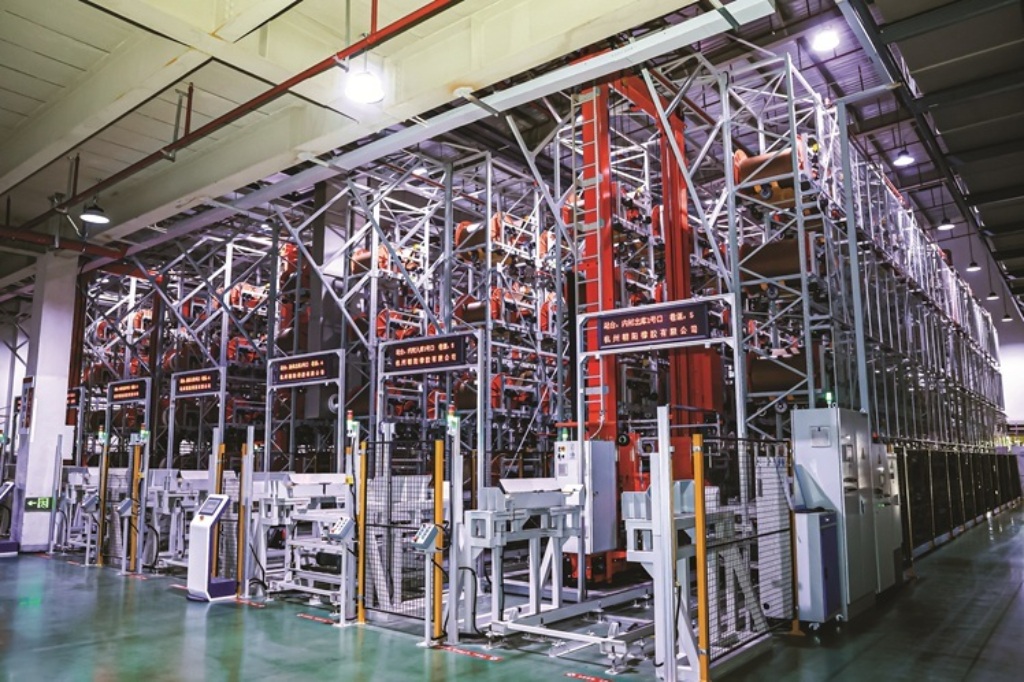
Their defining feature is what the company calls the Forward-development Approach. Traditional development, it explains, “often starts from an existing product and improves it through repeated design and testing cycles”. ZC Rubber starts elsewhere: with the target performance, whether that is vehicle characteristics, duty cycle, climate, road conditions or customer requirements. The compound, tyre structure and manufacturing process are then built around those targets. “This shifts the workflow from repeated iteration to a more integrated, target-driven development process,” the company said.
That, it argues, is where the halving of development time comes from. The 50 percent reduction reflects ‘a more integrated digital development process’, combining engineering expertise with simulation, AI-assisted tools and closer links between R&D, testing and manufacturing. AI lets engineers evaluate more design options against defined performance targets, and virtual simulation cuts out unnecessary physical iterations.
How tightly these platforms are wired into live production data has not been shared publicly. X-Tech and Phecda, the company said, connect R&D, manufacturing and validation within an integrated development process, but the detailed real-time data architecture behind them ‘is not something we currently disclose publicly’.
Henry Shen, ZC Rubber’s Senior Vice President, has made the wider point in the context of the group’s recent State recognition. “Our objective is not simply to develop an individual material, tread pattern or manufacturing process,” he said. “X-Tech and Phecda are complete development systems that connect user requirements with simulation, materials, tyre engineering, manufacturing and validation.”
THE STATE PRIZE
That recognition is significant. ZC Rubber, together with Harbin Institute of Technology, has been awarded the Second Prize of China’s State Science and Technology Progress Award for a project titled ‘Key Technologies and Green Intelligent Manufacturing of High-Performance Tires’. It is one of the country’s highest state-level honours for scientific and technological innovation, and ZC Rubber says it is the only Chinese tyre manufacturer in the past decade to win it at the Second Prize level or above.
The company backs the claim with spending. In 2025, it invested around RMB 1.54 billion (approximately USD 226 million in R&D, equal to 3.43 percent of annual revenue, according to its annual report. The award, it says, recognises technologies that have ‘progressed beyond laboratory research into industrial application’.
GLOBAL FOOTPRINT
ZC Rubber has built a truly global footprint, combining a strong manufacturing base in China with an expanding network of operations across Europe, the Americas, Southeast Asia and beyond. In China, the company operates through multiple sites, including its headquartered in Hangzhou and facilities in Tianjin, Chaoyang, Jiande, Qingquan, Yonggu, Anji and Jintan, supported by dedicated units for recycling technology and automotive aftermarket services in Hangzhou.
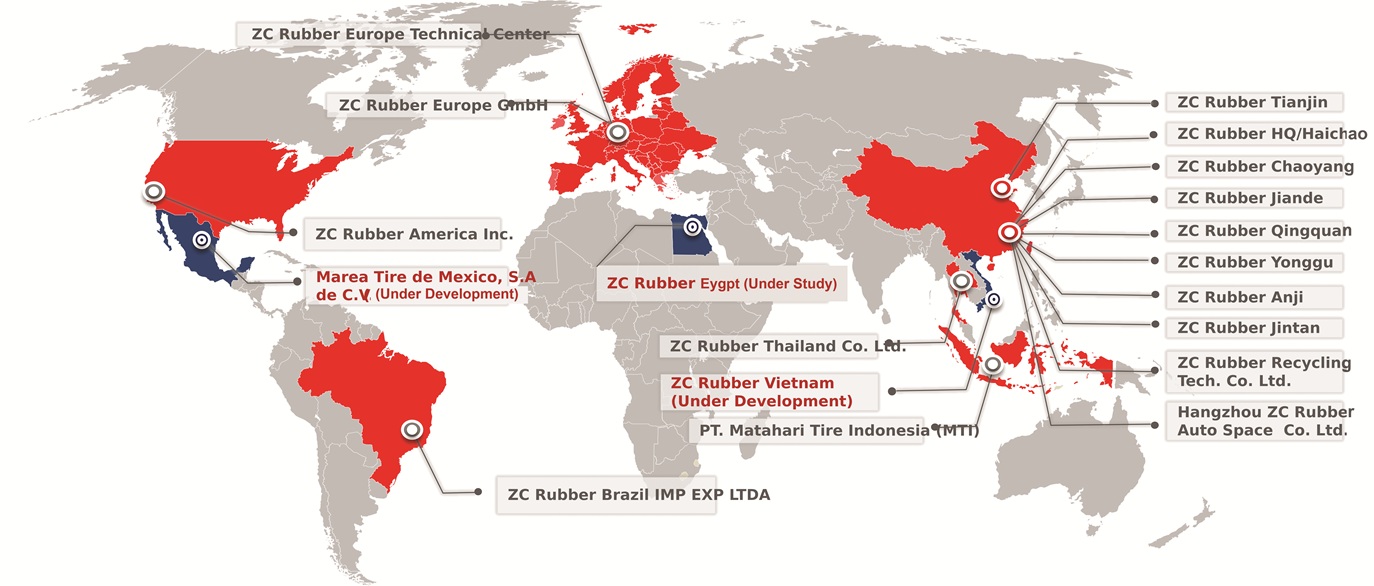
Beyond China, ZC Rubber has established a European presence through ZC Rubber Europe GmbH and its Europe Technical Center, alongside ZC Rubber America Inc. in the United States, ZC Rubber Brazil IMP EXP LTDA in South America and ZC Rubber Thailand Co. Ltd. and PT. Matahari Tire Indonesia (MTI) in Southeast Asia.
The company is also preparing for further expansion, with new projects under development in Vietnam and Mexico (Marea Tire de Mexico, S.A. de C.V.) and a feasibility study underway in Egypt. Together, these locations allow ZC Rubber to serve customers closer to their markets, strengthen supply chain resilience and combine local insight with global technical expertise.
CUSTOMISATION WITHOUT THE PENALTY
The forward-development model has a commercial payoff: tyres tailored to where and how they will be used. Asked whether the platforms allow genuine mass customisation, including regional climates and EV-specific requirements, ZC Rubber answered ‘to a significant degree’.
“X-Tech and Phecda allow us to develop tyres around specific climates, road conditions, vehicle applications and performance targets, including EV-specific requirements,” it said. On the factory floor, flexible production lines adjust output as product mix and orders change. The company does not disclose a separate efficiency figure for customised production, though ‘the goal is clear: to increase product flexibility while keeping production efficient’.
The regional examples are concrete. In Asia, X-Tech underpins the X-Elite Truck Tyre Series. In Europe, it is applied to the WESTLAKE Gen II commercial lineup, with a focus on fleet efficiency, performance and regulatory requirements. Phecda sits behind the WESTLAKE ZuperAce Z-007 and GOODRIDE Solmax 1 passenger tyres, and technologies from both platforms have been applied across ARISUN’s full TBR and PCR ranges for the Americas.
“International markets do not have identical requirements,” Shen said. “A tyre developed for European highway fleets, Southeast Asian transport operations or passenger vehicles in the Americas must respond to different vehicles, roads, climates and customer priorities.”
WHAT COMES NEXT
Much of the technology commonly billed as next-generation is already in service at ZC Rubber. Automated logistics, AI-based visual inspection, process optimisation, digital simulation and virtual testing are all in use. Digital twins are applied in areas such as energy management, and a broader digital-twin virtual factory is part of the next-stage plan.
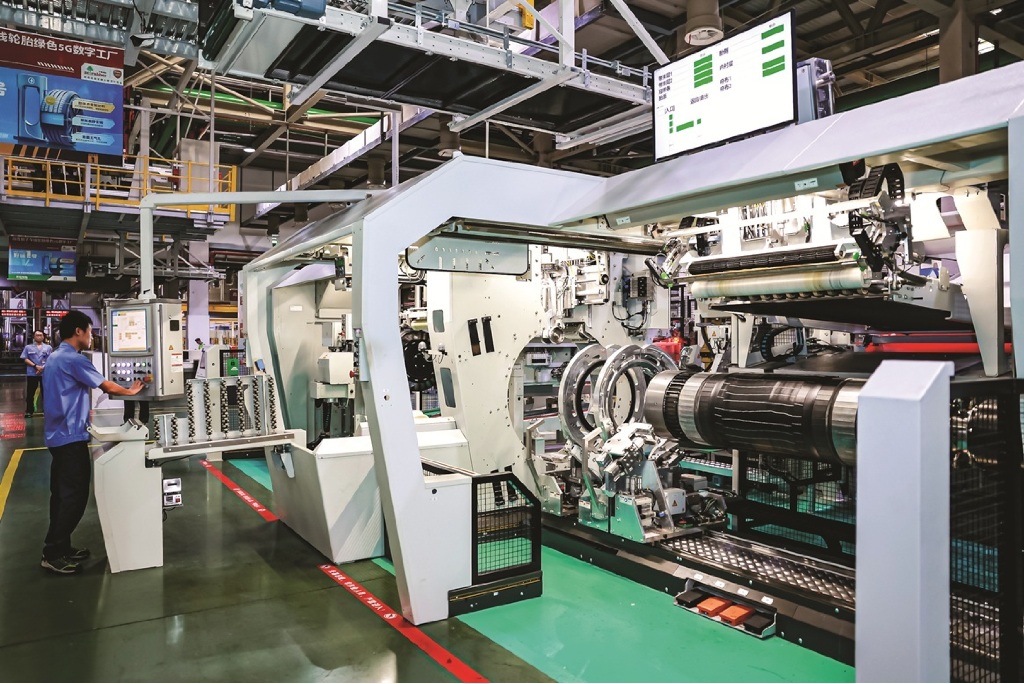 The company frames the coming three years as a period of deepening rather than reinvention: more smart-factory applications, more AI and industry-specific models and close attention to emerging technologies such as humanoid robotics ‘as they mature’.
That phrasing may be the most revealing thing about ZC Rubber’s approach. It is chasing results rather than headlines. As the company itself puts it, the launch of the Hangzhou plant marks ‘a new opportunity and starting point’, and its stated ambition is to become a world-leading tyre company with higher standards. Whether the lights stay on, it seems, is the least of its concerns.
AMETEK Completes USD 5bn Acquisition Of Indicor Instrumentation Businesses
- By TT Bureau
- October 12, 2026
AMETEK recently completed its USD 5- billion all-cash acquisition of a portfolio of instrumentation businesses from Indicor.
The businesses, collectively known as Indicor Instrumentation, make equipment for industrial and scientific applications. Their products serve markets that overlap with AMETEK’s existing operations and generate recurring revenue from consumables, services and aftermarket support.
David A Zapico, AMETEK’s Chairman and Chief Executive, said: “We are excited to complete this highly strategic acquisition and to welcome the Indicor Instrumentation team to AMETEK. With its mission-critical solutions, deep technical expertise, and strong positions in attractive end markets, Indicor Instrumentation is an excellent fit with AMETEK. We also see meaningful opportunities to create value through integration into our proven operating model.”
Indicor Instrumentation is expected to contribute about USD 350 million to AMETEK’s sales in 2026 and to be modestly accretive to adjusted earnings for the year.
The acquired businesses will join AMETEK’s Electronic Instruments Group and Electromechanical Group, according to their products and market focus.
The Goodyear Tire & Rubber Company has elected Joe Hinrichs as chairman of its Board of Directors, effective 7 October 2026. He will also chair the board's Governance and Executive Committees. Hinrichs joined the board in 2023 and succeeds Laurette Koellner, who will retire at the 2027 annual meeting under Goodyear's Corporate Governance Guidelines.
Hinrichs most recently served as President and Chief Executive Officer of CSX Corporation. Before that, he held numerous leadership roles at Ford Motor Company, including President of the Global Automotive Business, Executive Vice President and President of Global Operations, Executive Vice President and President of the Americas, President of Asia Pacific and Africa, and Chairman and Chief Executive Officer of Ford China. He also led Ford Canada. Hinrichs holds a bachelor's degree in electrical engineering from the University of Dayton and an MBA from Harvard Business School.
Koellner previously held several leadership roles at The Boeing Company. She joined Goodyear's board in 2015, became independent Lead Director in 2019, and Non-Executive Chairman in 2024.
Hinrichs said, "I would like to recognise and thank Laurette for her leadership, dedication and unwavering commitment to Goodyear. On behalf of the Board, we are grateful for her many contributions throughout her more than a decade of service. I look forward to working alongside my fellow board members and the leadership team as we continue to innovate, strengthen our competitive position, create long-term value for our shareholders and build a stronger Goodyear."
CEAT Specialty’s Off-Highway Tyre Playbook
- By Sharad Matade
- October 09, 2026
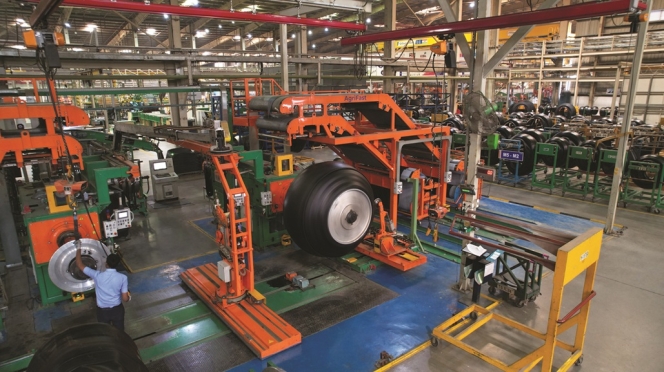
CEAT’s Chennai and Halol plants are the only tyre facilities globally with two WEF Global Lighthouse Network inductions, and the company has also won the Deming Grand Prize for manufacturing excellence.
Yet 30 km from Mumbai, CEAT Specialty’s 49-acre Ambernath plant tells a different story: tyres too heavy for automation, built instead around nitrogen curing, induction presses and orders as small as one unit – a bet that sustainability will win markets in Europe and America.
The stakes: an INR 5 billion investment in all-steel radial technology, capacity expansion to 160 tonnes/day and a Camso manufacturing deal Tolani pegs at up to USD 1 billion – turning a manufacturing constraint into a competitive edge.
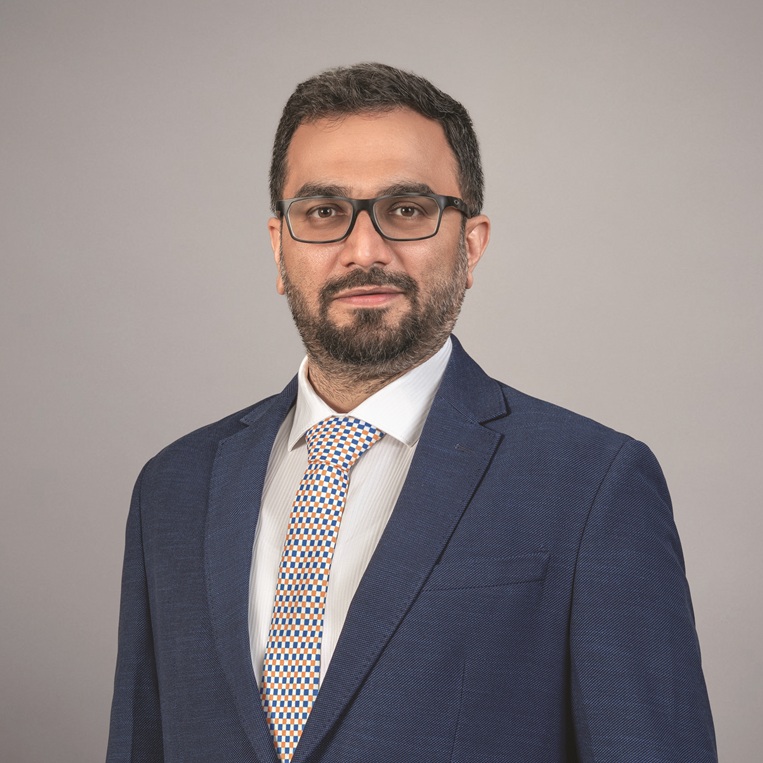
Amit Tolani, Chief Executive of CEAT Specialty, does not talk about tyres the way most executives talk about their products. He talks about them the way an engineer talks about a puzzle that keeps changing shape. “The way to look at it is that the manufacturing processes that we follow – how modern they are, how capable they are, how technically efficient – that’s what matters,” he says, sitting inside the plant that has become the nerve centre of CEAT’s off-highway tyre (OHT) business.
That plant – the Ambernath facility, a division of Mumbai-headquartered RPG Group’s CEAT Limited – is not a conventional tyre factory. It builds tyres that can weigh up to over 600 kilogrammes, tyres too large and too heavy for the automation that has transformed the passenger-car tyre business. And it is this constraint, as much as any strategic masterplan, that has shaped how CEAT Specialty has chosen to compete.
A PLANT THAT CANNOT SIMPLY COPY THE ROBOTS
Ask Tolani why Ambernath has not adopted the wall-to-wall robotic automation seen at CEAT’s Chennai or Halol facility, and the answer is refreshingly unglamorous: physics. “PCR tyres can be lifted by an ordinary human being, or a forklift, or robots,” he explains. “For these tyres, which are 600–700 kg, it’s very difficult to have a conveyor that can just lift them.” In the processes that do lend themselves to automation – mixing, calendering, curing – Ambernath’s equipment, he insists, is ‘as modern as the Chennai plant. More modern’. The plant intends to formalise that claim in the coming months by pursuing Industry 4.0 certification.
Where the physical limits of scale end, digital ones have taken over. A SCADA system tracks steam lines running beneath the plant floor. Where a leak once required a worker to walk the line, take manual temperature readings and diagnose the fault, artificial intelligence now flags the location almost instantly. “The point time taken to identify the problem is close to zero,” Tolani says. Every tyre carries a digital identity from raw material to finished good; a single scan reveals the batch, the machine, the operator and the timestamp behind it. AI is also being trained on the plant’s visual tyre inspection – traditionally a human, eyeball-driven task – using high-resolution cameras to catch defects, and on optimising mixing recipes and cycle times, the invisible chemistry that determines how a tyre performs in a paddy field or a quarry.
CURING WITHOUT STEAM
The most technically striking claim to emerge from Ambernath concerns curing – the energy-intensive process of vulcanising rubber under heat and pressure that has, for a century, meant steam. “This plant has already started using nitrogen curing on one of the lines,” Tolani says. Alongside it sit two proof-of-concept induction curing presses – a steam-free process, while the nitrogen conversion has come via LMT. “There are two presses that are already commissioned here,” he says. “We’ve already started working in that direction, where we want to take a lead in this space.”
The bulk of the plant’s newest investment, however, is going into something more conventional in principle but strategically significant in intent: all-steel radial off-the-road tyres. CEAT Specialty has committed INR 5 billion to this latest phase of expansion, representing a decisive shift in product architecture. Where a car’s tyres are universally radial, only 60–70 percent of truck tyres have made that transition, and agricultural and OTR applications lag further still – agriculture because usage is seasonal, OTR because a fabric-belted bias tyre still does much of the heavy lifting. All-steel radial construction changes that calculus by delivering higher load-carrying capacity and greater comfort, attributes increasingly demanded not only by Indian buyers but, crucially, by European and American customers. “It’s for demand from the European market, the US market – and the Indian market is also growing in such a handsome fashion that we want to cater to it,” Tolani says.
LEAN BY DESIGN, NOT BY SLOGAN
CEAT’s manufacturing philosophy is inseparable from its most prized accolade: in 2017, CEAT became the first tyre company outside Japan to win the Deming Prize, the world’s most prestigious award for total quality management; in 2023, it became the first tyre company anywhere to win the Deming Grand Prize, a distinction held by only 33 organisations globally as of 2025. Inside CEAT, this discipline is branded QBM – Quality Based Management – a homegrown fusion of Total Quality Management, the Toyota Production System and Total Productive Maintenance.
“We are a Deming Grand organisation. That means we follow the philosophy of lean manufacturing – not to use resources or have any wastage in the process,” Tolani says. That philosophy is embedded, quite literally, in the plant’s straight-flow layout, which runs from raw material storage through mixing, stock preparation, tyre building, curing and final finish in a single unbroken line. Even small batch sizes, he says, are produced without the wastage, excess labour or lost efficiency – what the plant’s internal vocabulary calls ‘Muri’ – that might otherwise creep in.
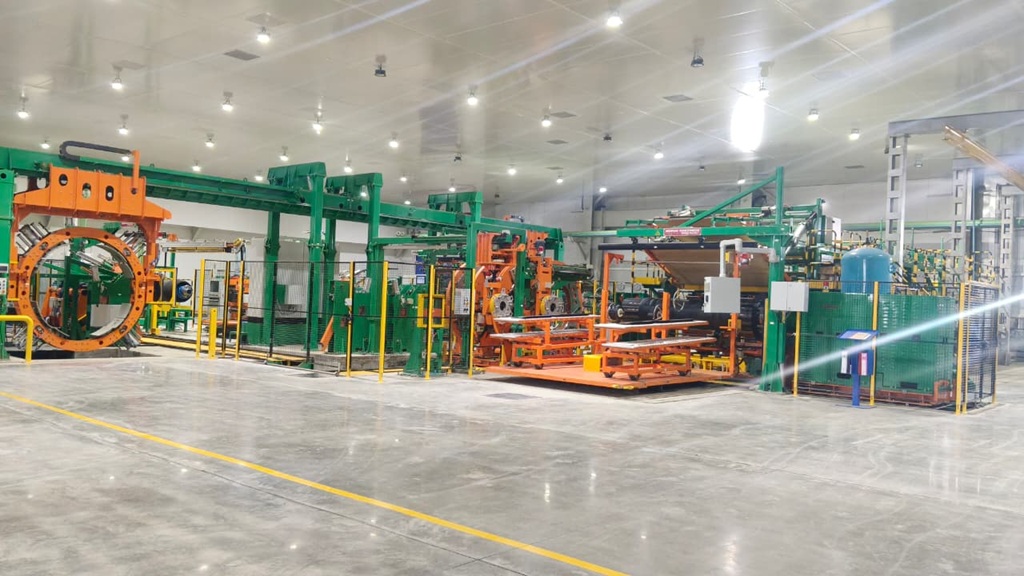
That same lean instinct underpins one of Ambernath’s more unusual competitive claims: a minimum order quantity of one. In an industry historically built around economies of scale, the plant will build a single speciality tyre to a customer’s specification without demanding batch aggregation – a capability the company says few OHT plants worldwide can match. Self-managed teams on the shop floor plan and execute changeovers themselves, allowing a highly automated, digitally traceable line to pivot rapidly to low-volume, customised orders. A related innovation, branded Unistage, builds and shapes an agricultural or OTR radial carcass into its final toroidal form on a single drum rather than the conventional two-stage process, reducing the handovers.
AN R&D CENTRE BUILT FOR SPEED, NOT SCALE
CEAT Specialty operates a dedicated in-house research and development facility at Ambernath, distinct from the group’s broader R&D infrastructure, and Tolani is candid about why. Tolani says, “This business is very, very different. There is no Pareto here – no 80/20 rule where a handful of product sizes serve the bulk of demand. Because farm and off-highway equipment come in such a long tail of sizes and configurations, and because the plant supplies numerous international OEMs directly, the time taken to develop, validate and commercialise a new tyre has to be compressed.”
“We needed a dedicated facility, closer to the manufacturing, so that we can quickly pilot, quickly turn around,” he adds. A new Compound Laboratory, opened in September 2025, now anchors materials science work spanning OTR, agricultural and industrial segments, while AI-assisted testing has trimmed, by Tolani’s estimate, roughly a third off the time from concept to market. The centre’s pipeline currently spans all-steel OTR tyres, a newly launched forestry range, very high flexion (VF) agricultural tyres and expanding work in earthmoving and material handling.
CAMSO ACQUIRED FOR BRAND, CHANNEL AND CATEGORY
CEAT Specialty’s move into Camso – a name Tolani values at up to USD 1 billion in brand potential across agricultural tracks, power sport tracks and material handling – may be its most consequential strategic bet. “It was a natural fit for us in terms of completing our portfolio,” he says. Ambernath, built in 2018 solely for agricultural radial tyres, gains through Camso’s new OEM ties (Massey Ferguson, John Deere) and construction-channel access across South America and Europe.
Under a three-year Michelin agreement, CEAT can currently manufacture and sell only compact construction tyres and tracks under Camso, taking over end-consumer sales in that segment – with other categories opening up once the term ends. The impact is already visible: standalone, CEAT Specialty’s off-highway mix is 85:15 agriculture to non-agriculture; with Camso’s, it shifts toward 50:50.
THE NUMBERS BEHIND THE AMBITION
Ambernath is running at 105 tonnes a day, at 92–95 percent utilisation – ahead of schedule. A further phase, due within 45 to 60 days, will lift capacity to 160 tonnes. Camso, still integrating, runs at roughly 50 percent.
Off-highway tyres make up close to 20 percent of CEAT’s speciality revenue, with the agriculture-to-non-agriculture split narrowing from 85:15 to near 50:50 once Camso is included. Domestically, Tolani credits GST reforms for a strong OEM market, led by Mahindra and TAFE, while mining stays flat – a segment Camso’s construction heritage should help lift as the new all-steel OTR line comes online.
Comments (0)
ADD COMMENT