Apollo Tyres: Driving the Future Of Mobility Through Cutting-Edge R&D
- By Daniele Lorenzetti
- March 03, 2025
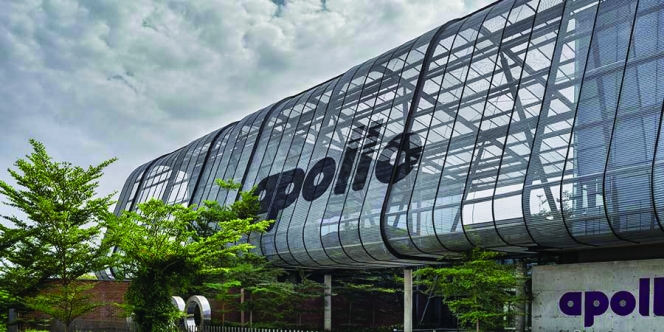
The future of mobility is poised for a revolutionary transformation driven by emerging technologies and changing consumer demands. With an increasing shift towards electrification, autonomous driving and connected ecosystems, the automotive industry is evolving rapidly. Electric vehicles (EVs) are becoming more mainstream, reducing carbon footprints and promoting sustainability. At the same time, advancements in artificial intelligence (AI), machine learning and data analytics are enabling smarter vehicles that can adapt to real-time conditions, enhance safety and provide seamless user experiences. Additionally, the integration of shared mobility solutions, such as ridesharing and autonomous fleets, promises to reshape urban transportation, making it more efficient and reducing congestion. As sustainability becomes a central focus, the future of mobility will also involve the development of greener materials, eco-friendly technologies and circular economy practices that minimise waste and maximise resource efficiency, paving the way for a cleaner, smarter and more connected world.
As the automotive world embraces transformative trends like electrification, sustainability and digital connectivity, Apollo Tyres stands at the forefront, driving innovation with its cutting-edge R&D. With a legacy of pioneering breakthroughs, Apollo’s commitment to shaping the future of mobility is grounded in a holistic approach that blends advanced technologies, sustainability and performance excellence.
Historically, Apollo Tyres has consistently delivered products tailored to diverse market demands. Its R&D operations in India and Europe synergise global expertise to innovate solutions for traditional and electric vehicles. Today, Apollo leads the industry with adaptable tyre platforms and technologies designed to meet the unique requirements of EVs, featuring low rolling resistance, noise reduction, traction and durability enhancements. Innovations such as real-time tyre sensors and noise-cancelling technologies further define the company’s reputation for excellence.
Looking ahead, Apollo Tyres is championing a sustainable future through material innovation and digital transformation. The company integrates renewable and recycled materials, collaborates with leading universities to explore eco-friendly alternatives and advances tyre retreading and circular economy principles. These efforts culminate in passenger vehicle prototype tyres composed of 75 percent sustainable materials, showcasing Apollo’s commitment to environmental stewardship. Meanwhile, digital tools such as virtual prototyping and AI-powered analytics accelerate R&D cycles, ensuring responsiveness to emerging trends.
Apollo Tyres envisions a mobility landscape where tyres transcend their functional role, becoming integral to vehicle connectivity and safety. By leveraging intelligent technologies like Tyre Pressure Monitoring Systems and sensor-enabled diagnostics, Apollo is redefining the tyre’s role in connected ecosystems. Through relentless innovation, Apollo Tyres not only aligns with the future of mobility but actively drives it forward. The R&D vision is to create value to customers by developing products and technologies that are best in class in performance while being profitable to business and sustainable to environment.
THE STRATEGY FOR 2026 IS BUILT ON THE FOLLOWING THREE PILLARS
- 1. Developing advanced tyre technology tailored for traditional and electric vehicles.
- 2. Embracing circular economy principles by integrating renewable and recycled materials.
- 3. Harnessing AI and virtual development tools to accelerate innovation in testing and material science.
Apollo’s investment in R&D has grown to around 2 percent of revenue. With a relentless focus on innovation, sustainability and customer satisfaction, Apollo is poised to continue its journey as a global leader in the tyre industry.
GLOBAL R&D TEAM: A SYNERGISTIC APPROACH
Our global R&D operations are strategically located in Chennai, India and Enschede, The Netherlands. These two centres integrate local expertise with advanced global technologies, addressing diverse market needs. Whether it’s the tropical climate and varied road conditions in India or the high-performance demands of European consumers, our R&D team tackles challenges with a unified approach. With state-of-the-art infrastructure, including advanced material research facility, raw material, predevelopment and simulation technologies, design, testing, advanced engineering, intellectual property, process and product development, Apollo Tyres delivers innovative tyre designs that address both regional and global demands.
ADVANCED MATERIAL RESEARCH AND SUSTAINABILITY INNOVATIONS
At Apollo, sustainability begins with material innovation. We are replacing conventional tyre components with eco-friendly alternatives. Collaborations with leading universities explore nano cellulose as a sustainable substitute for carbon black. Partnerships with Tyromer have revolutionised the quality of recycled rubber through cutting-edge devulcanisation techniques. On top we have signed collaboration projects with Asian premier institutes on bio degradation of ELT. Additionally, we promote natural rubber sustainability through plantation certifications, traceability programmes and education initiatives, achieving ISCC certification in our plants. Our material research extends to bio-based and recycled raw materials that enhance material sustainability. Advanced analytical tools enable precise characterisation of smart materials, supporting breakthroughs in polymer and filler technologies. Our tailored compounds ensure low rolling resistance, high traction and noise reduction, while delivering superior performance across all applications.
PREDEVELOPMENT AND VIRTUAL PROTOTYPING TECHNOLOGIES
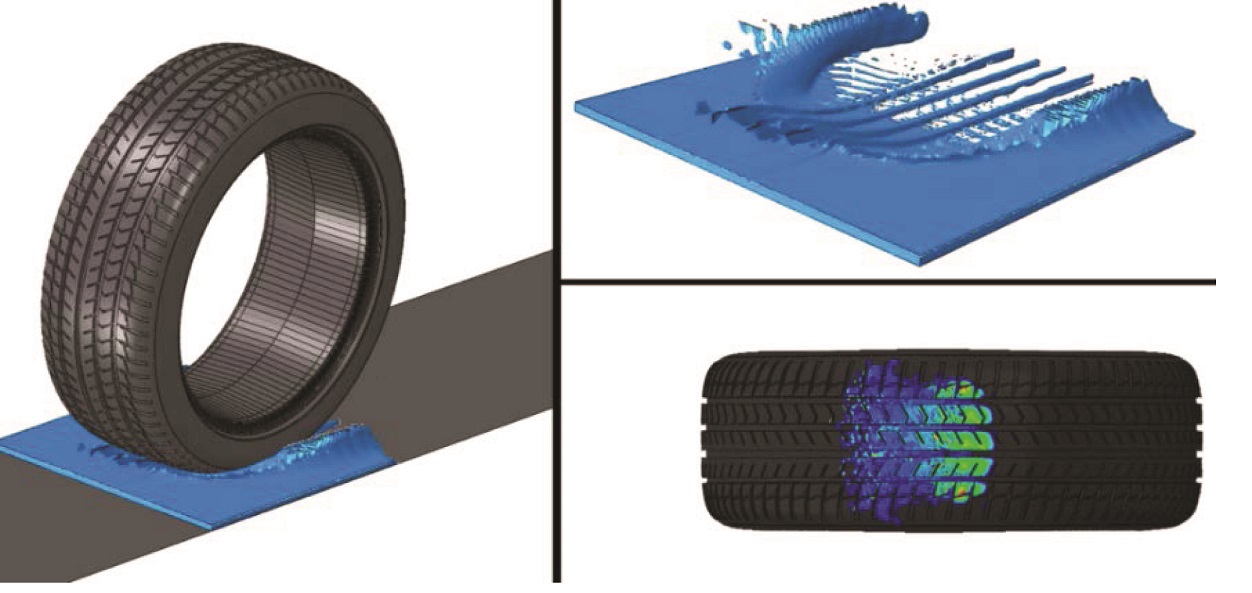
Innovation is the heartbeat of Apollo Tyres. Our predevelopment teams integrate groundbreaking technologies, setting new benchmarks in the industry. FOAM technology exemplifies this spirit, reducing cavity noise for EVs without compromising on durability. This technology addresses the evolving needs of OEMs. Our sustainability-driven initiatives include ultra-low rolling resistance tyres with a rolling resistance coefficient of just 5.5 kg/tonne. Lightweight Truck Bus Radial tyres with a 10 percent weight reduction highlight our focus on environmental stewardship and performance innovation. Across all R&D locations, our focus on high performance drives tyre innovation. Advanced Computer-Aided Design (CAD) tools and real-world simulations help optimise tyre designs for diverse terrains. Detailed aerodynamic analyses further enhance fuel efficiency in vehicles, ensuring superior grip, handling and noise reduction. By leveraging virtual prototyping, we accelerate development cycles, optimising characteristics like rolling resistance, grip, comfort and noise.
INTELLECTUAL PROPERTY
Our Intellectual Property (IP) teams has played a crucial role in safeguarding and advancing the prosperity of our company. Our IP team is tasked with recognising, securing and utilising our intellectual property assets to strengthen our competitive edge and generate lasting value for our stakeholders.
The following are some of the key achievements:
- 1. 25 patent applications were filed in FY24.
- 2. A total of 200+ active patents across geographies.
- 3. 29 design registrations filed in FY24.
- 4. A total of 300+ design registrations across geographies.
Our Intellectual Property (IP) team has cultivated an innovative culture within our organisation by encouraging employees to adhere to best IP practices, leading to the creation of high-value patents and designs. Consequently, we have generated new intellectual property assets and bolstered our product development capabilities.
ADVANCED TESTING EXCELLENCE
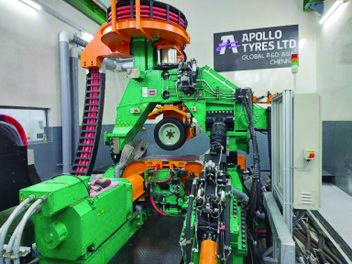 Testing is integral to ensuring the safety, performance and durability of our tyres. Our test facilities feature cutting-edge equipment that validates products under diverse conditions:
Flat-Trac Machine: This sophisticated tool measures force and moment properties, aiding in the design of high-performance tyres.
Anechoic Chamber: Simulating various road conditions, this chamber evaluates tyre noise levels, ensuring quieter and more comfortable rides. We have developed dedicated testing protocols for EVs, focusing on rolling resistance and noise reduction. The newly established Cut and Chip track at NATRAX, Indore, is designed to test tyres under extreme conditions, evaluating durability, uptime and grip. Through experiential drives, we showcase our technological prowess to fleet owners, business partners and media.
INTEGRATING TYRES INTO FUTURE MOBILITY THROUGH ADVANCED ENGINEERING
Apollo Tyres is at the forefront of revolutionising mobility through advanced engineering aligned with key megatrends like sustainability, connected vehicles and autonomous driving. Our intelligent tyres, equipped with sensors, telematics and software, enable seamless communication of vehicle conditions. Tyre Pressure Monitoring Solutions (TPMS), deployed in our tyre as service AVOLVE programme, enhance safety, reduce fuel consumption and provide remote diagnostics. The tyre of tomorrow will not just be a component but a critical element in the vehicle’s connectivity and safety systems.
ADVANCING INNOVATION THROUGH STRATEGIC COLLABORATION
Our R&D endeavours are grounded in robust partnerships with prestigious academic institutions that include both Indian and European universities. Apollo Tyres is also participating in consortium research on pre-competitive technologies. It is also worth mentioning that Apollo Tyres is also actively engaging with our supplier partners and customers to deliver cutting-edge technologies, products and services.

ADDRESSING TECHNICAL CHALLENGES AND INDUSTRY TRENDS
The automotive sector is undergoing rapid regulatory changes, including Europe’s Green Deal and Euro 7 standards. These developments demand stricter compliance with emission and mileage requirements, accelerating the adoption of EVs. Apollo’s R&D efforts address these challenges by focusing on sustainable materials and advanced technologies. Circular economy initiatives, such as tyre retreading and recycling-friendly compounds, reduce waste and maximise resource efficiency. Our development of passenger vehicle prototype tyres containing 75 percent sustainable materials underscores our commitment to innovation and environmental responsibility.
CONCLUSION
Apollo Tyres’ unified R&D operations in India and Europe are more than innovation hubs; they are the pillars of the company’s vision to lead in technology and sustainability. By addressing global challenges and leveraging cutting-edge tools, Apollo Tyres continues to shape the future of mobility, delivering technology excellence with operational excellence to customers worldwide.
Why The Future Of Manufacturing Needs An India–Latin America–China Dialogue
The future of manufacturing is no longer being shaped by technology alone.
Artificial intelligence, automation and advanced materials will certainly transform factories. But geopolitics, trade tensions, access to raw materials and supply-chain security are increasingly determining where companies produce, where they invest and how industrial capacity is distributed around the world.
For the tyre industry, this shift is already visible. Manufacturers are reconsidering their global footprints. Production is moving closer to strategic markets, supply chains are being diversified and companies are balancing efficiency against the risks of excessive dependence on individual countries, suppliers or transport routes.
Manufacturing capacity is once again becoming strategic capacity. And that should lead us to reconsider not only how industrial value is created, but what happens to that value once a product leaves the factory.
THE VALUE ALREADY MANUFACTURED
Can a tyre be considered truly sustainable if it is manufactured efficiently but cannot remain in use?
At first sight, this may appear to be a question about retreading, but it is a question about manufacturing.
When a commercial tyre leaves a factory, it contains much more than rubber and steel. It embodies raw materials, energy, engineering, technology, labour and manufacturing capacity. Considerable industrial value has already been created.
The strategic question, therefore, is not only how efficiently we can manufacture the next tyre. It is also how effectively we can preserve the value of the tyre we have already manufactured by keeping it in productive use.
If access to raw materials matters strategically, using those materials intelligently should matter as well. If manufacturing capacity is valuable, preserving the value created by that capacity should also become part of industrial strategy.
This gives retreadability a different meaning.
Retreading is usually treated as a downstream activity, beginning once the manufacturer’s role has effectively ended. Yet the ability to keep a tyre in productive use begins much earlier. It is influenced by design, engineering, material selection and, fundamentally, the quality and durability of the casing.
Retreadability, therefore, is not only an issue for the retreading industry. It is also a manufacturing consideration.
This does not mean innovation should be constrained to accommodate existing retreading processes. The challenge is whether innovation can advance while preserving the ability of a valuable industrial product to remain safely and economically in use.
As we design the tyre of the future, are we also designing it to remain in use?
THE GEOPOLITICS OF A LOCALLY GROWN TYRE
As geopolitical uncertainty encourages local-for-local manufacturing, shorter supply chains and regional production, the tyre industry is rediscovering the strategic value of proximity. But perhaps the concept of local production should not end when the original tyre leaves the factory.
A retreaded commercial tyre has an interesting characteristic: much of the additional value required to keep that tyre operating can be generated locally.
The casing is already present in the economy. Its continued use can be enabled through local inspection, technical knowledge, skilled workers, retreading plants and domestic transport networks. In that sense, retreading can create something particularly relevant in a more fragmented global economy: a locally grown tyre.
The expression should not be understood literally. The original tyre may have been manufactured thousands of kilometres away and its raw materials may have originated in several countries.
What becomes local is the additional industrial value. An economy can use its own technical and industrial capabilities to keep an existing asset productive rather than depending exclusively on another newly manufactured product entering through an international supply chain.
For many Latin American economies, which remain dependent on imported tyres and industrial inputs, this has particular significance. But the principle reaches beyond Latin America. As countries debate reshoring, nearshoring, strategic autonomy and supply-chain resilience, keeping existing industrial assets in productive use deserves a place in that discussion.
Viewed through this lens, circularity is not only an environmental strategy. It can also become a resilience strategy.
WHY INDIA, LATIN AMERICA AND CHINA?
This brings us to an opportunity that deserves greater attention: an India–Latin America–China dialogue on circular tyre manufacturing. Its value lies precisely in the differences between the three regions.
India is strengthening its position as a global manufacturing power, combining growing international ambitions with an enormous domestic mobility market and significant requirements for raw materials. Latin America operates at a different scale but sits at the intersection of important industrial relationships with North America, Europe and Asia. Commercial tyre retreading has also been part of its transport economy for decades, providing practical experience in keeping manufactured assets in productive use. China brings another dimension: extraordinary manufacturing scale, technological depth and supply-chain capabilities that have reshaped the global tyre industry.
 The purpose would not be to determine which model is superior. None of these regions has all the answers. Their experiences are valuable precisely because they are different.
What could India’s manufacturing expansion learn from markets where extending product use has long been economically necessary? What could Latin America learn from the transformation of Asian manufacturing? And what could India, Latin America and China discover together about designing tyres whose industrial value can be preserved for longer?
Those questions could form the beginning of a very different relationship.
FROM TRADE TO INDUSTRIAL DIALOGUE
India, Latin America and China already have substantial commercial relationships. Tyres, machinery, raw materials, technology and investment move between these markets. But knowledge should move as well.
Much of the relationship between tyre-producing regions is still understood through exports, imports, tariffs and market access. These issues will remain fundamental, particularly as the international trading environment becomes more complex. But the restructuring of global manufacturing creates an opportunity to move from trade relationships towards industrial relationships.
 What should durability mean for the next generation of commercial tyres? Should retreadability become a more explicit consideration in advanced tyre design? Can digital traceability allow manufacturers, fleets and retreaders to better understand the history and remaining value of a casing? And can circular economy policies distinguish more effectively between recovering materials and keeping a manufactured product in productive use?
These are not simply questions about retreading.
They are questions about how industrial value should be managed in the future. Industry associations are particularly well positioned to begin that conversation. Companies naturally approach these issues through commercial interests, while governments see them through trade, industrial or environmental policy. Associations can occupy the space between them, connecting manufacturers, retreaders, fleets, technology providers, researchers and policymakers.
An India–Latin America–China dialogue does not require another international organisation, nor should it begin by attempting to harmonise three very different markets. It could start simply as an exchange about how we manufacture, how long we use and how much industrial value we are capable of preserving.
The purpose would not be to demonstrate that one region has found the correct model. It would be to ask better questions together.
BEYOND THE FACTORY GATE
The factory of the future will undoubtedly be smarter. Artificial intelligence, automation, advanced materials and increasingly efficient production systems will transform how tyres are manufactured. But geopolitics is reminding industry that efficiency alone does not determine industrial strength. Resilience matters. Access to resources matters. Manufacturing capability matters. And the ability to make better use of what an economy already possesses may matter increasingly as well.
For the tyre industry, that means looking beyond the factory gate – not only towards what happens when a tyre eventually becomes waste but towards what happens to the industrial value created when that tyre was manufactured in the first place.
Can a tyre be considered truly sustainable if it is manufactured efficiently but cannot remain in use? Perhaps the future of manufacturing should not be measured only by how intelligently we create industrial value. It should also be measured by how intelligently we keep that value in use.
For a global industry navigating a more fragmented and uncertain world, that may prove to be much more than a circular economy argument. It may become an industrial strategy.
And that is a conversation India, Latin America and China should start together.
Study On Tyre Strength Issues And Evaluation Methods
- By Zhong Ma
- October 26, 2026
The focus of tyre regulations has shifted towards sustainability. Our research on passenger car radial tyres (PCR) strength evaluation and the strength testing requirements in the IS15633 standard aligns precisely with this trend. Before discussing why, the traditional plunger-strength test has become irrelevant for evaluating PCR tyres, let us first consider the benefits of eliminating it. Based on Continental’s engineering experience, waiving the strength test allows for an average reduction of 0.7 kg (range: 0.5–0.9 kg) in cap ply material. This translates to saving approximately USD 0.70 in material costs per tyre while simultaneously lowering rolling resistance, which yields a carbon reduction benefit of about 6 kg per tyre in-use-phase. Given that the Indian PCR market involves approximately 32 million replacement and 20 million original equipment PCR tyres, the potential annual impact includes saving roughly 40,000 tonnes of material, cutting costs by about USD 43 million and reducing carbon emissions by approximately 370,000 tonnes; over a 10- to 20-year horizon, these would yield substantial societal sustainability benefit. This paper examines the history of the strength test and addresses the issue of its unsuitability for evaluating PCR tyres and provides supporting arguments to help realise these prospective benefits.
It is well‑documented that tyre‑strength testing originated to address road‑hazard impact damage. Tyre strength evaluation protocols were developed specifically to address damage caused by such impacts. Literature indicates that, starting in the 1960s, tyre‑and‑wheel damage caused by striking potholes, road shoulders or curbs became a major safety concern for automotive OEMs. The Society of Automotive Engineers (SAE) categorised this form of damaging impact as ‘road hazard impacts’. Over the following six decades, multiple test methodologies – including tyre strength tests (Plunger test), pendulum‑impact tests and full‑vehicle obstacle‑impact tests – were developed for new PCR to assess road‑hazard‑impact effects on treads, sidewalls and wheel assemblies. This work clarifies the fundamental nature of tyre‑strength‑related problems and traces the origin and evolution of these test methods. It aims to furnish a technical basis for industry and regulatory authorities to revise strength‑test standards and to support tyre manufacturers and vehicle OEMs in appropriately applying these evaluation methods when resolving consumer complaints about tyre performance.
I. WHAT IS A ROAD‑HAZARD IMPACT?
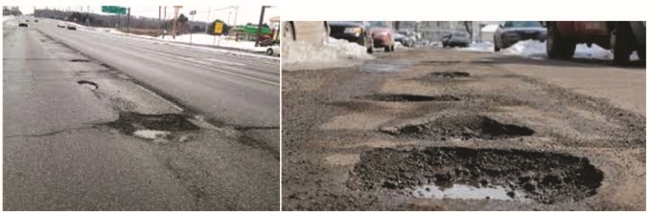
Damage to tyres and wheels resulting from driving over potholes or obstacles such as curbs and speed bumps is defined as a damaging road‑hazard impact (Figure 1). Such events remain common on real‑world roads today.
II. WHAT IS TYRE-STRENGTH EVALUATION?
Tyre‑strength evaluation assesses the external‑force thresholds at which a tyre undergoes structural failure, as well as the corresponding failure force and energy levels. Structural failure denotes rupture of reinforcing cords within the carcass, cap ply or belt layers, leading to air leakage, bulging or related defects. It is critical to distinguish air leakage caused by sharp‑object punctures – a puncture‑resistance and air‑retention concern – from true structural‑strength failure. Sharp‑object punctures can often be repaired, or leakage mitigated through sealant application. By contrast, structural damage arising from severe road‑hazard impacts is non‑repairable. Major tyre‑industry associations uniformly advise consumers against continuing service use of tyres that have sustained such structural failure.
We emphasise that air leakage from sharp‑object punctures does not constitute a tyre‑strength issue. A comparison between damage generated in a plunger‑type strength test (Figure 2(a)) and nail puncture damage (Figure 2(b)) highlights this distinction: plunger‑induced failure ruptures belt layers and creates large tears in the inner liner, whereas nail‑style sharp‑object punctures do not rupture reinforcing layers and produce only a small inner‑liner wound.
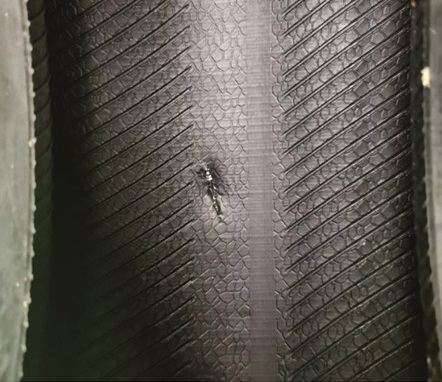
Figure 2(a) Tyre damage caused by plunger strength test
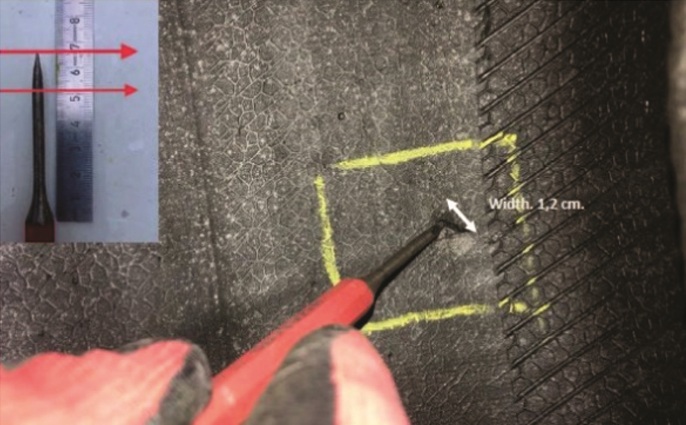
Figure 2(b) Tyre damage caused by nail puncture88
III. DISTINCT DAMAGE PATTERNS FROM ROAD‑HAZARD IMPACTS: RADIAL VERSUS BIAS‑PLY TYRES
Research demonstrates that road‑hazard‑impact damage manifests differently for bias‑ply and radial tyres. For bias‑ply tyres, impacts predominantly generate crown‑region damage; for radial tyres, impacts most commonly produce sidewall bulging and wheel‑assembly damage.
These divergent failure modes stem from fundamental structural and material differences between the two tyre architectures. As shown in Figure 3(a), bias‑ply tyres use rayon, nylon or polyester reinforcing plies arranged in criss‑cross orientations at angles below 90° relative to the tread centreline, running continuously from one bead to the opposite bead. This forms a monolithic structure with high overall integrity and stiff sidewalls. The tyre resists bending, and its constituent structural elements do not deform independently under external loading. By comparison (Figure 3(b)), radial‑tyre carcass plies run at approximately 90° relative to the tread centreline, extending bead‑to‑bead. The tread circumference is further reinforced by two steel belt layers plus a rayon, nylon or polyester cap ply. This creates a dual‑component architecture: a rigid, robust crown coupled with a flexible, air‑spring‑like tyre body. The carcass exhibits high elasticity, sidewalls deform readily under load and the tyre absorbs road impacts with unique dynamic behaviour under external forces.
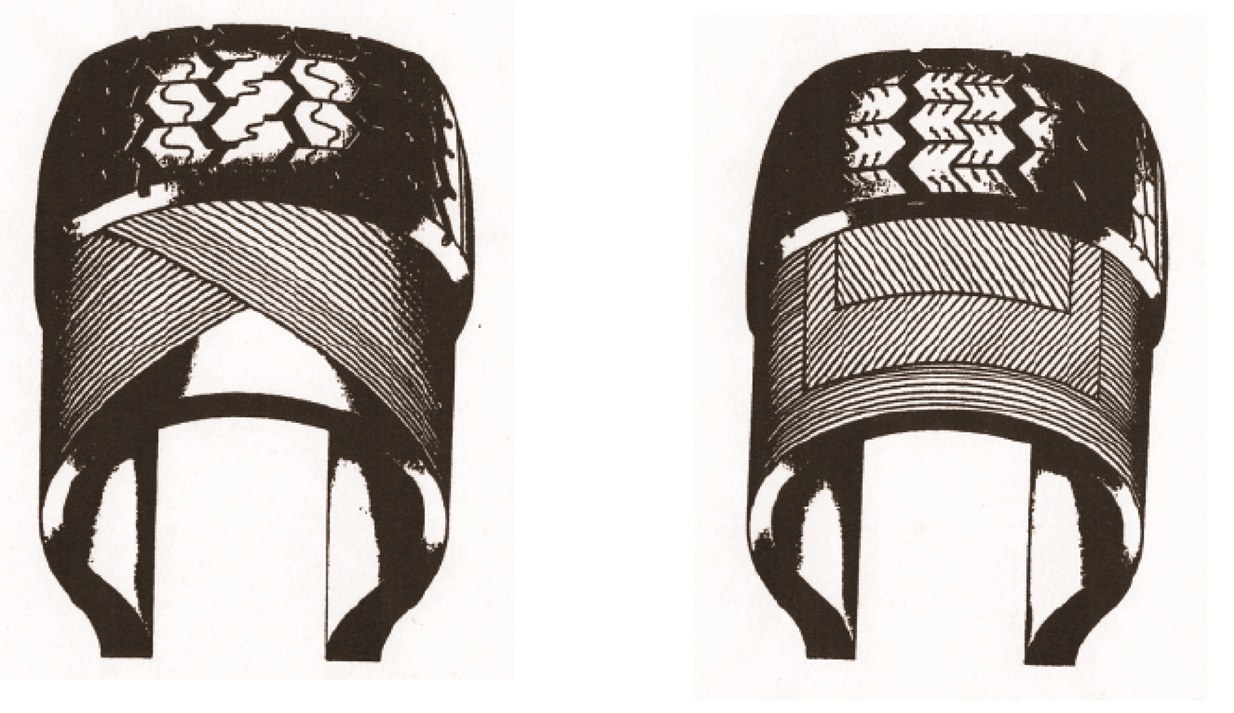
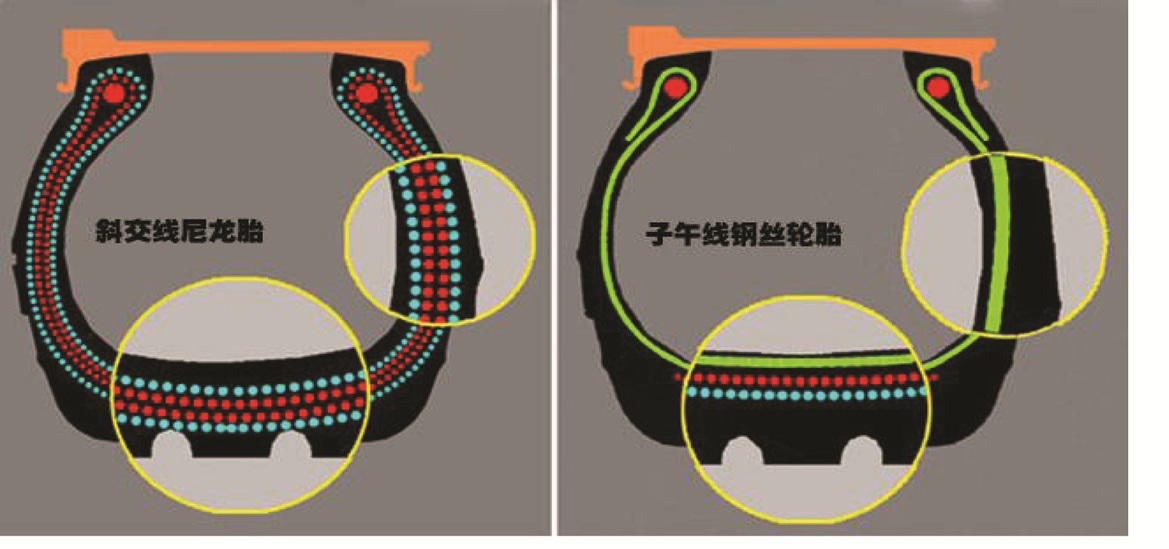 (Figure 3 (a) Schematic of bias-ply tyre design)
(Figure 3 (b) Schematic of radial tyre design)
THE STRUCTURAL CHARACTERISTICS OF BIAS-PLY AND RADIAL TYRES REVEAL THE FOLLOWING:
(1) The materials used for the circumferential cap ply and belt layers in radial tyres possess greater strength than the rayon, nylon or polyester belt materials found in bias-ply tyres;
(2) Because radial tyre sidewalls are highly flexible and prone to deformation, impact forces often cause damage to the vehicle suspension, rim or sidewall (such as bulging) before the tyre crown accumulates enough energy to suffer structural failure. Traditional strength testing involves a 19 mm plunger vertically compressing the tyre crown to simulate the forces experienced when a tyre strikes a small road obstacle (like a stone). CT images captured during a strength test of a 185/60R15 88T tyre clearly show that the plunger must descend almost to the point of touching the rim before it can puncture the crown plies and belt layers to reach the failure energy limit. This process causes incredible sidewall deformation due to the tyre’s high flexibility; however, in real-world driving conditions, the rim or suspension system would sustain damage long before the tyre could undergo such extreme deformation from a road impact.
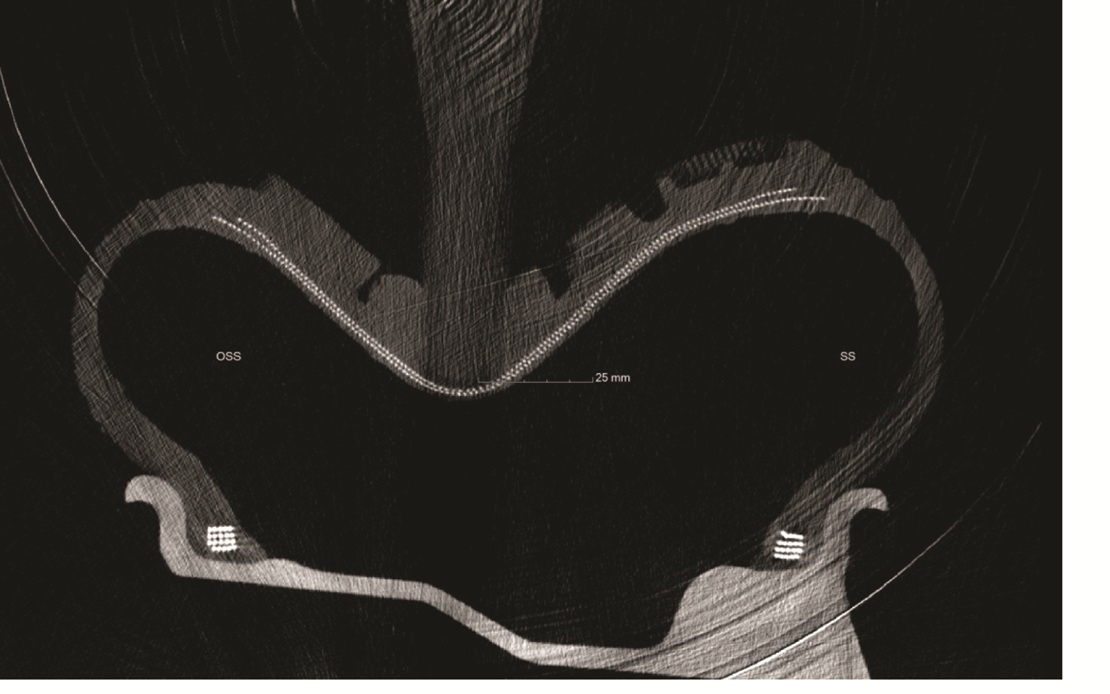 Figure 4 CT scan imagery captured during tyre‑strength testing
A detailed structural comparison between bias‑ply and radial tyres appears in the February 2020 paper Observations on Tyre Plunger Strength and Bead Unseating Performance by Professor Joseph D Walter (University of Akron). Walter notes that bias‑ply plies form a rhombic (parallelogram‑like) structural arrangement, while the combination of belt layers and carcass plies in radial tyres yields a triangulated structural configuration. Figure 5 contrasts the load‑driven deformation characteristics of these two architectures.
Within bias-ply tyres, measurable changes in cord angle occur repeatedly during the loading and unloading cycles of each tyre rotation; consequently, the rhombic structure of the bias plies is also referred to as a ‘shear’ structure. These angular changes induce significant shear strain within the rubber, leading to the accumulation of hysteretic heat – an effect that is markedly reduced in radial tyres due to their triangular structural configuration. In modern radial tyres, the carcass ply material (whether polyester or rayon) situated beneath the steel belt layers forms a stable triangular structure that reinforces the tread area. These deformation-resistant triangles provide vastly superior strength and rigidity compared to other structural designs. Without the underlying carcass plies, the belt cords – whether steel or textile – would simply form a non-rigid rhombic structure, resulting in performance characteristics identical to those of bias-ply tyres.
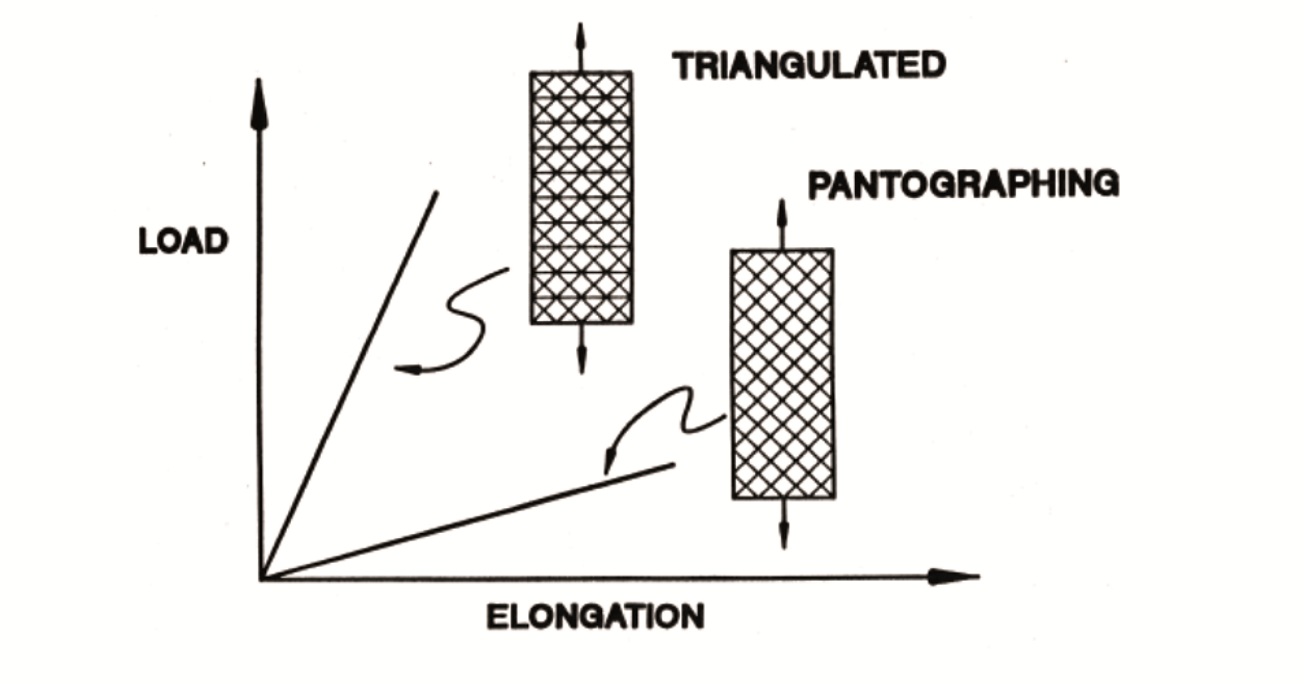
Figure 5 Deformation differences between rhombic‑shear and triangulated structures
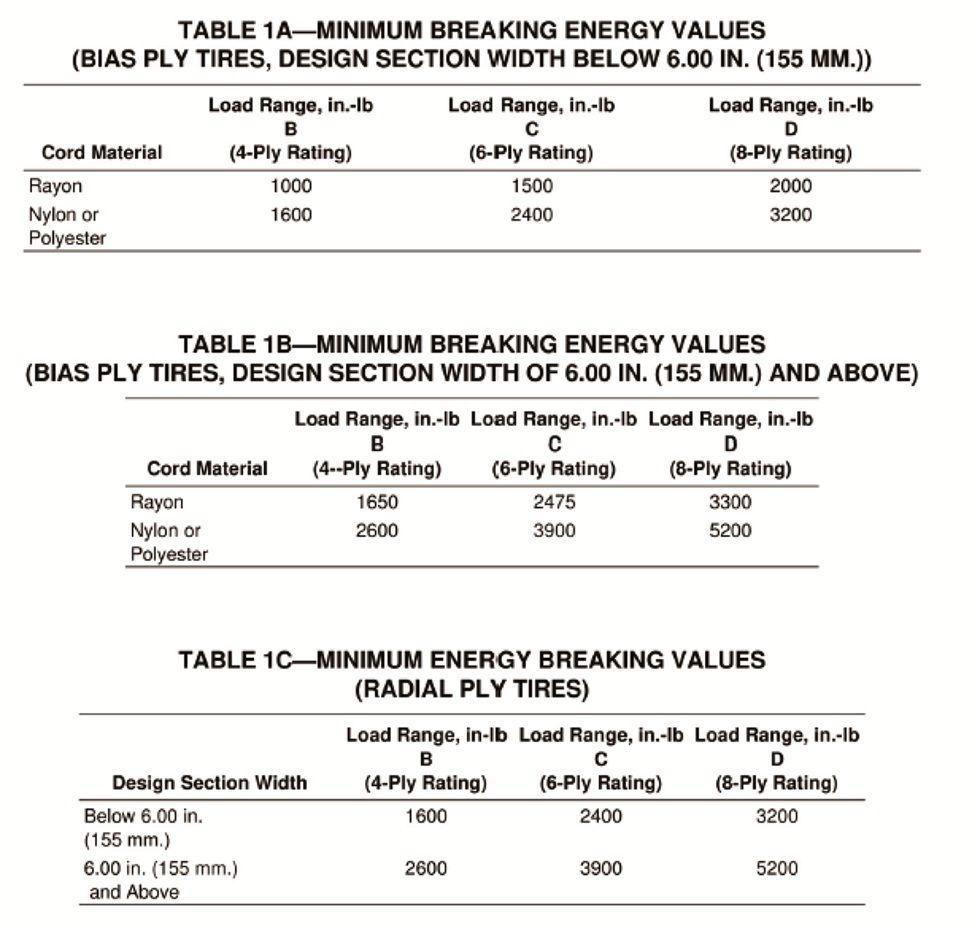 Figure 6 Strength‑evaluation criteria defined within SAE J918
In summary: the monolithic structure of bias‑ply tyres and dual‑component architecture of radial tyres produce fundamentally different failure modes under road‑hazard impact. Radial tyres deliver well‑established advantages in vehicle handling, ride comfort, service life, rolling resistance and lightweight performance. The industry’s shift from bias‑ply to radial construction necessitates updated assessment approaches for impact‑related damage, particularly for low‑aspect‑ratio radial tyres. Legacy strength‑evaluation criteria originally designed for bias‑ply tyres cannot simply be carried over unchanged.
IV. EVALUATION APPROACHES FOR ROAD‑HAZARD‑IMPACT DAMAGE
1. Road‑hazard‑impact evaluation for bias‑ply tyres:
Tyre‑strength testing and crown‑ply‑rupture assessment were pioneered in the United States. In 1965, SAE published SAE J918, Passenger Car Tyre Performance Requirements and Test Procedures, establishing tyre‑strength test procedures and defining minimum failure‑energy acceptance criteria for rayon‑, nylon‑and‑polyester‑constructed bias‑ply tyres.
Full original theoretical rationale for these early performance metrics is no longer traceable. Nevertheless, historical literature yields notable observations:
1) The standards specified higher strength limits for nylon or polyester than for rayon. In effect, strength‑performance limits were calibrated to match the tyre‑construction raw materials in use at that time.
2) The standards established minimum strength requirements not only for bias-ply tyres – which were the norm at the time – but also for radial tyres. Production radial passenger‑car tyres were not fitted as original equipment on US vehicles until 1970. Given the absence of vehicles equipped with radial tyres on the road back then, the limits clearly were not derived from real-world issues specific to radials; instead, the standards simply adopted the bias-ply strength limits – a practice that has persisted for 60 years despite the lack of an empirical basis regarding radial tyres.
2. Road‑hazard‑impact damage for radial‑ply tyres:
By the 1990s, radial‑tyre market penetration in the United States approached 90 percent. SAE practitioners then recognised that road‑hazard‑impact failure modes for radial tyres diverged sharply from those seen with legacy bias‑ply tyres. Real-world radial-tyre impact events typically produce sidewall or rim damage. The plunger‑style strength test, which was designed to assess tread‑crown robustness, provides little meaningful insight into these real‑world radial‑tyre failure modes. Accordingly, SAE released the SAE J1981 in 1994: Road Hazard Impact Test for Wheel/Tyre Assemblies, introducing pendulum-impact test to simulate damage to complete tyre‑wheel assemblies. In a February 2020 letter to the NHTSA (National Highway Traffic Safety Administration), the USTMA (U.S. Tyre Manufacturers Association) stated: “By 2000, the industry recognised that radial tyres were not susceptible to the specific damage modes targeted by [traditional] strength tests; automakers also observed that radial tyre sidewalls were relatively ‘soft’, meaning that impacts with potholes or obstacles often resulted in suspension or rim damage, or sidewall bulging, rather than tread-area failure.”
Our research highlights that both pendulum‑impact tests and plunger‑strength tests originated as successive SAE methodologies addressing road‑hazard hazards, reflecting the distinct failure physics of bias‑ply versus radial tyres. Additional supporting documentation comes from Tyre Laboratory Strength Test Validation Report (NHTSA‑2000‑8011‑0020). In March 2002, NHTSA floated a proposal to replace traditional plunger test with pendulum‑impact testing per SAE J1981, envisioning pendulum impact as a dynamic alternative for tyre‑strength assessment. Figure 7 displays representative impact strikers used within that NHTSA research programme, including wedge‑form impactors and a 50 mm cylindrical striker conceptually analogous to plunger tips used in commercial‑vehicle tyre‑strength testing.
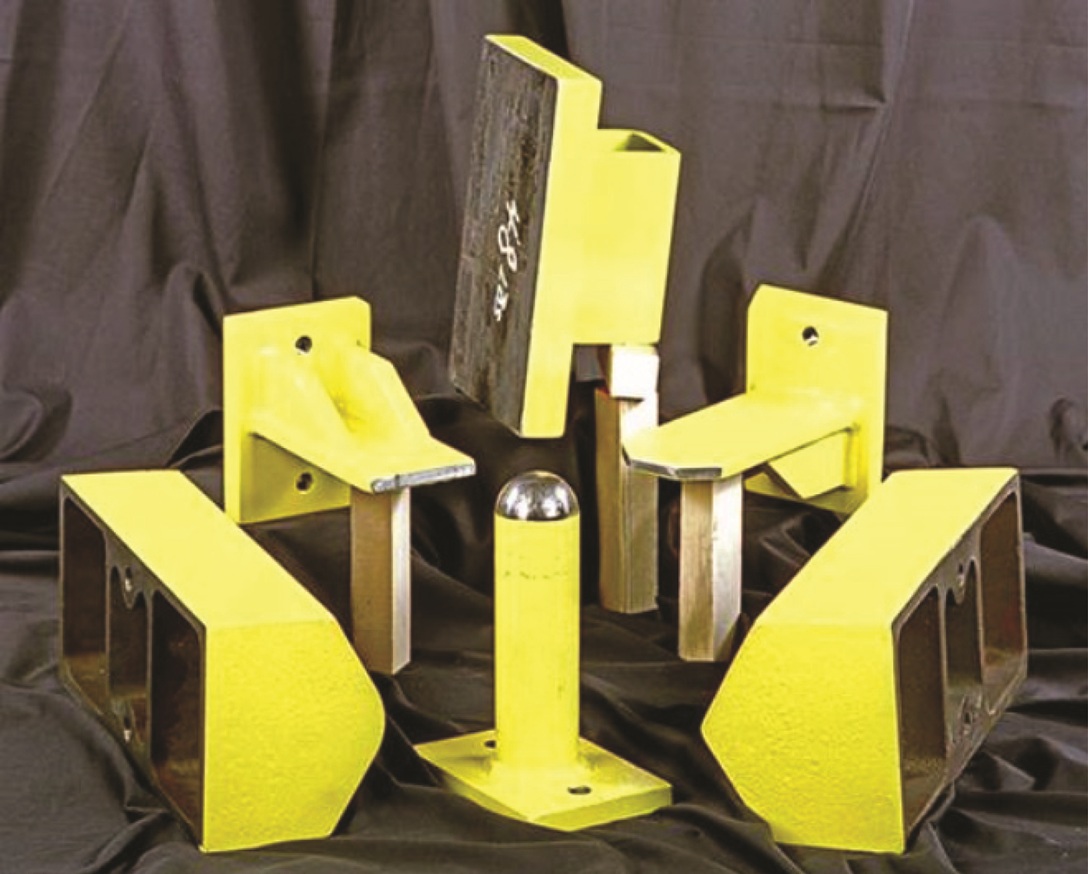 Figure 7 S Impact strikers evaluated for NHTSA pendulum‑surrogate‑strength‑test research
Test outcomes from this project disappointed NHTSA; the proposal failed to gain acceptance across tyre and automotive stakeholders. In 2002, the Rubber Manufacturers Association (RMA), Ford Motor Company and the European Tyre and Rubber Manufacturers’ Association (ETRMA) explicitly commented that pendulum‑impact testing primarily evaluates complete wheel‑assembly damage from road hazards. Its standalone suitability for assessing tyre‑intrinsic strength required further refinement and validation. As a result, NHTSA formally withdrew its proposal to substitute pendulum impact for plunger‑strength testing in June 2003, while research activities targeting radial‑tyre‑suited strength‑assessment methods continued.
During 2011‑2013, Germany’s VDA (German Association of the Automotive Industry) and WDK (German Rubber Industry Association) built upon SAE J1981 to investigate correlations between laboratory pendulum‑impact results and full‑vehicle impact behaviour. Their studies demonstrated poor correlation between pendulum‑impact measured energies and energies observed in full‑vehicle obstacle‑impact events, corroborating why NHTSA’s 2002 proposal could not succeed. WDK member companies nonetheless derived a dimensionless ‘f‑value’ via empirical formulas incorporating tyre‑geometric and load parameters; this f‑value exhibited partial correlation with full‑vehicle impact speeds. These research outputs were subsequently published within the VDA 11‑2016 technical guideline.
It should be noted that the validity of the f-factor evaluation relies on its correlation with vehicle impact speeds; if this correlation is disproven, the f-factor loses its viability. Furthermore, the f-value in the VDA-11 method is intended as a design reference for sidewall strength during the development of specific vehicle models, rather than as a general strength evaluation metric for tyres independent of specific vehicle models. We found that neither the SAE method nor the VDA f-value could serve as a general strength evaluation method for radial tyres without relying on parameters specific to a vehicle model (such as wheel assembly strength, suspension stiffness and vehicle load). To verify this finding and gather evidence, Continental Tyre conducted validation tests in China in collaboration with the National Tyre Quality Supervision and Inspection Center. By comparing vehicle-based impact tests and pendulum impact tests across two vehicle platforms and using various obstacle heights, the following observations were made:
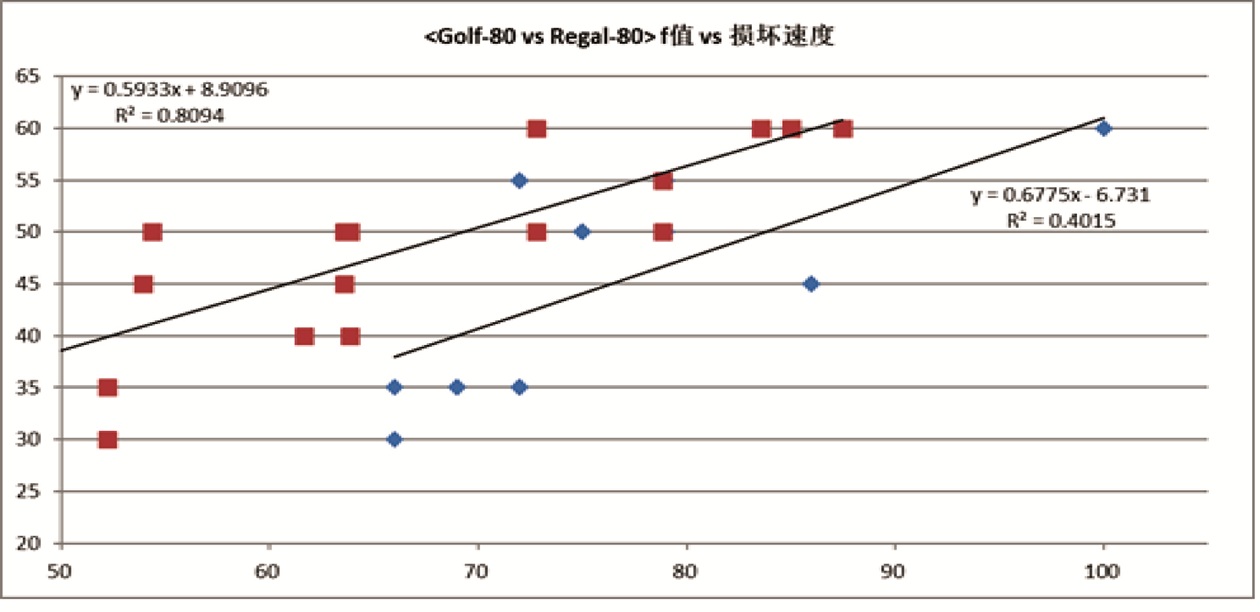
Figure 8 Comparative test results: Golf 7 versus Regal
(red data points = Golf 7; blue data points = Regal)
1. For one fixed vehicle platform, laboratory pendulum‑derived f‑values show partial correlation with real‑vehicle damage‑onset impact speeds, yet this correlation remains unstable. Substantial f‑value scatter can occur at constant impact velocity, and conversely, similar f‑values may correspond to very different impact speeds.
2. Tyres yielding identical f‑values in pendulum testing exhibit divergent damage‑threshold impact speeds when fitted on different production vehicles. In our test campaign, the ratio of damage‑threshold speeds for the Golf 7 and Regal vehicles approximated the ratio of their respective curb weights.
3. Damage‑threshold impact speeds show an approximately exponential dependence on obstacle height. Changing obstacle height therefore exerts an exponential influence on measured test outcomes. (Figure 9)
Many consumer complaints about sidewall bulging relate to damage incurred at relatively low driving speeds, for instance after striking potholes or kerbs. Defining
Figure 9 Regal impact‑test results: 80 mm vs 100 mm obstacle heights (red points = 100 mm obstacle height; blue points = 80 mm obstacle height)
tyre‑performance limits expressed via vehicle‑specific impact speeds or f‑factors – further adjusted for tyre aspect ratio – cannot adequately resolve real‑world consumer‑complaint scenarios. Such an approach also departs from the original technical intent of SAE‑and VDA‑defined pendulum‑based f‑values, which were conceived to correlate against full‑vehicle impact‑speed observations. Consequently, applying f‑factors or vehicle‑specific impact‑test outcomes as universal tyre‑strength‑evaluation criteria remains unfeasible at present.
Legacy plunger‑strength‑test procedures were conceived for bias‑ply tyres. A radial tyre’s plunger‑strength‑test performance tells us nothing about its real‑world propensity for sidewall bulging, rim damage or suspension damage following impact events. Plunger‑strength‑test results cannot characterise radial‑tyre road‑hazard‑impact robustness. Retaining the existing plunger‑strength‑test requirement for radial tyres solely for lack of a replacement methodology serves no practical purpose.
1. Provide sufficient consumer training explaining that radial tyres – particularly low‑aspect‑ratio variants – are inherently vulnerable to road‑hazard‑impact damage (e.g. pothole, curb strikes) as a direct consequence of their structural design.
2. Impact‑resistance degrades as tyre section height decreases. For vehicles intended for harsh‑road operating conditions (e.g. off‑road platforms), vehicle‑designers and end‑users should select appropriately‑specified tyres. Avoid fitting low‑aspect‑ratio wide tread tyres optimised for high‑performance road‑car track use onto off‑road‑oriented vehicles purely for aesthetic reasons.
3. Expand market‑level training and public guidance on identifying sidewall‑bulge damage and associated tyre‑replacement requirements, preventing tyres with observable bulges from remaining in‑service and creating safety hazards.
Radial‑tyre architecture delivers high‑stiffness crown regions paired with flexible, low‑stiffness sidewalls. Ongoing market trends towards lower aspect ratios exacerbate sidewall‑bulge failure risks. Industry stakeholders should communicate realistic operational limitations of radial tyres to end‑users and educate consumers on mitigating road‑hazard‑impact risks, rather than persisting with obsolete, functionally‑irrelevant legacy strength‑test requirements or adopting new, theoretically‑contested strength‑factor metrics to resolve real‑world service‑complaint tensions. In particular, hastily‑mandated sidewall‑strength minimum limits risk impeding market progress towards high‑performance, low‑aspect‑ratio radial‑tyre deployment.
We hope these preliminary research findings support industry and regulatory stakeholders addressing real‑world consumer‑and‑technical challenges. This work informs further deliberation over the continued applicability of legacy tyre‑strength testing, as well as the potential adoption constraints of pendulum‑impact‑based assessment and f‑factor methodologies, while preserving the dynamic‑performance and structural‑design advantages intrinsic to radial tyres.
VI. OUTLOOK FOR FUTURE RADIAL‑TYRE‑STRENGTH‑EVALUATION WORK
1. Owing to radial tyres’ structural‑mechanical characteristics, real‑world road‑hazard‑impact events predominantly produce sidewall damage; secondary damage may occur on wheel‑hubs or vehicle‑suspension components. Crown‑region structural failure is rarely observed. Accordingly, the existing plunger‑strength‑test methodology cannot deliver actionable insights for modern radial‑tyre assessment.
2. The shift towards radial‑tyre construction is irreversible. Removing prescriptive sidewall‑strength mandates unlocks design freedom for tyre dynamic performance, enabling improvements in vehicle handling and low‑emission capability. This represents an advanced tier of automotive safety, realising lightweighting and energy‑saving potential that would otherwise be constrained by rigid strength‑test requirements.
3. When handling consumer complaints about bulging sidewalls on low‑aspect‑ratio UHP/UUHP high‑performance radial tyres, stakeholders must recognise the trade‑offs inherent to radial‑tyre dual‑component architecture: superior dynamic performance comes alongside inherent sidewall‑impact‑vulnerability. Vehicle OEMs need to fully understand the operational characteristics of low‑aspect‑ratio high‑performance tyres, and communicate clearly to end‑users. Consumers should be made aware to avoid abusive curb‑strike events while benefitting from high‑performance‑tyre capabilities. Test data demonstrates that raising obstacle height from 80 mm to 100 mm can reduce the tyre‑damage‑onset safe‑impact speed by as much as 43 percent.
Advancing passenger car radial tyre and high-performance tyre technology to achieve lightweight and sustainable performance is the industry’s forward-looking development priority. This study clarifies the historical context of tyre strength evaluation practice; it supplies technical background to support proposal on revision of relative Indian IS standard and delivers practical guidance for consumers operating high‑performance tyres as well as for vehicle‑OEM tyre‑specification engineers.
The author is the Head Of APAC Standards And Regulations, Continental Tires.
Future Of Tyre Manufacturing: Engineering For An Untamed World
- By Devin Gawarvala
- October 20, 2026
The tyre industry is entering one of the most transformative phases in its history. Manufacturing is no longer defined only by production capacity, compound formulation or tread design. The future will be shaped by how effectively manufacturers combine advanced engineering, intelligent manufacturing, sustainability, application-specific innovation, smart technologies and global competitiveness.
For us at Rubber King Tyre Pvt. Ltd., the direction is clear: the tyre of the future must perform reliably where conditions are most demanding. This philosophy is captured in our brand promise: ‘RULE THE TERRAIN – Tyres for the Untamed’.
It represents more than a tagline. It reflects how we see the future of tyre engineering – developing products capable of performing across challenging agricultural fields, construction sites, mining environments and demanding material-handling applications as per customer expectations.
Devin Gawarvala
FROM TYRE MANUFACTURING TO PERFORMANCE ENGINEERING
Customers today are increasingly evaluating tyres on total performance rather than purchase price alone. Tyre life, traction, load-carrying capability, resistance to cuts and wear, heat management, equipment uptime and overall cost per operating hour are becoming critical considerations.
This is particularly relevant in the OTR, agriculture and industrial segments, where operating conditions can vary dramatically.
The future, therefore, belongs to application-driven tyre engineering. Instead of developing products primarily around dimensions and specifications, manufacturers will increasingly engineer tyres around the machine, terrain, load cycle, operating hours and customer requirements.
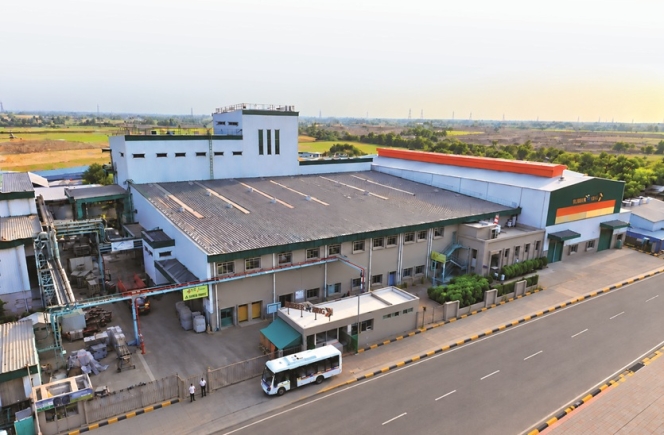
At Rubber King, this approach aligns closely with our focus on pneumatic and solid tyre solutions across agriculture, construction, mining, OTR and industrial applications. The company currently operates four manufacturing facilities in Gujarat and has built its product philosophy around durability, performance and precision engineering.
SMART MANUFACTURING WILL REDEFINE CONSISTENCY
The next major transformation will take place inside tyre factories.
Automation, digital process monitoring, data analytics and increasingly intelligent manufacturing systems will enable manufacturers to achieve greater consistency while improving productivity and reducing process variations.
However, smart manufacturing should not simply mean installing more automated equipment. Its real value comes from connecting people, processes, machines, materials and data.
Data generated across mixing, component preparation, building, curing, inspection and testing can help manufacturers identify variations earlier, improve traceability and strengthen preventive quality systems.
For Indian manufacturers, this presents an important opportunity. Combining our manufacturing capabilities and engineering talent with greater automation and digitalisation can significantly strengthen India’s position as a global tyre manufacturing hub.
SUSTAINABILITY MUST WORK ALONGSIDE PERFORMANCE
Sustainability will also become fundamental to the future of tyre manufacturing.
The industry will need to examine the complete product lifecycle – from sourcing raw materials and improving manufacturing efficiency to extending tyre life and addressing end-of-life recovery. Recent industry research is already demonstrating the potential of bio-sourced materials, recycled inputs and recovered carbon black to reduce the environmental footprint of tyre production while maintaining required performance standards.
For manufacturers, the challenge is to ensure that sustainability does not come at the cost of durability or safety.
In demanding OTR and industrial applications, a tyre that lasts longer can itself contribute to resource efficiency. Extending service life, reducing premature replacement and improving operating efficiency should therefore form an important part of the sustainability conversation.
The future will require manufacturers to achieve both objectives: lower environmental impact and higher product performance.
R&D WILL BECOME THE COMPETITIVE DIFFERENTIATOR
As equipment becomes more powerful and applications become increasingly specialised, research and development will play an even greater role.
Compound technology, casing design, tread geometry, heat dissipation, rolling resistance, cut and chip resistance and load optimisation will continue to evolve. At the same time, faster testing and feedback from real-world applications will allow manufacturers to shorten development cycles.
Rubber King’s R&D approach includes product development, technology upgrades, process optimisation, material evaluation and testing procedures aligned with internationally recognised standards.
The objective must be simple: understand the application before engineering the tyre.
INDIA HAS AN OPPORTUNITY TO LEAD
India’s manufacturing ecosystem is moving from being viewed primarily as a cost-competitive production base towards becoming an engineering and innovation partner for global markets.
For Indian tyre manufacturers, this creates a significant opportunity.
To compete internationally, however, we must benchmark ourselves against global standards – not only on price but on product consistency, technology, service, innovation and application knowledge.
At Rubber King, our international presence across more than 90 countries reinforces our belief that Indian manufacturers can develop products in India while competing confidently across global markets.
The next decade of tyre manufacturing will ultimately be about engineering confidence – confidence that a tyre will perform when the terrain becomes difficult, the load becomes heavier and the operating environment becomes unpredictable.
That is where manufacturing technology, R&D and customer understanding must come together.
Because the future will not always operate on perfect roads or predictable surfaces.
It will be built for the untamed.
RULE THE TERRAIN – Tyres for the Untamed.
The author is Entrepreneurial Founder & Director, Rubber King Tyre Group
Innovative - Intelligent - Integrated Tyre Manufacturing
- By Ertugrul Bahan
- October 16, 2026
The innovative, intelligent and integrated tyre manufacturing system marks a paradigm shift and is an indispensable tool for a fundamentally different vision of the future.
This model fosters a highly networked, data-driven and agile production environment and revolutionises traditional, labour-intensive manufacturing. This model must be combined and integrated with integrated product development, intelligent automation and data-driven optimisation.
In this model, tyre design, materials and manufacturing processes are controlled within a unified framework to achieve defined objectives. The model’s principle is based on a comprehensive and integrated development process, ensuring the achievement of consistent objectives tailored to the vehicle application, operating conditions and customer requirements.
The overall model digitally integrates and networks all phases of the tyre lifecycle, from the development and design of rubber compounds to product marketing. Data relating to design, manufacturing, testing and customer service are consolidated in a centralised and unified digital system.
This model resembles an autonomous system integrating AI and enabling the automation of repetitive tasks, predictive maintenance and real-time quality control without manual intervention. However, it already takes customer expectations into account from the design stage.
The ZC Rubber model represents a transition from theory to practice, requiring a top-down strategic approach that takes into account the product realisation architecture as well as the overall organisational culture.
ZC Rubber incorporates such a model, relying on platform-based strategies that directly leverage its proprietary X-Tech and Phecda Tech Systems. This provides an effective foundation for the continuous development of speciality tyres. The integrated system supports the development of original equipment and replacement tyres for the company’s three main brands.
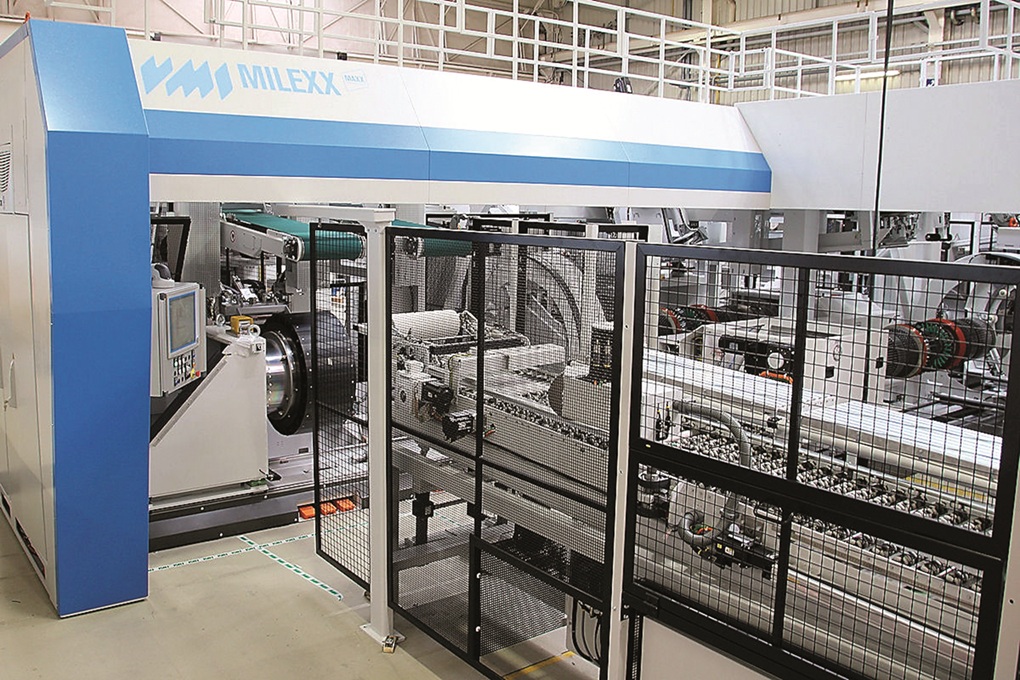
ZC Rubber combines materials research, product development, manufacturing and validation within an integrated development process. This expertise enables faster product development, more consistent production and better alignment with the specific requirements of automotive platforms and markets. As a result, advancements in research and development generate measurable added value for automakers, suppliers, fleet managers, dealerships and drivers worldwide.
ZC Rubber’s model enables manufacturers to simulate production scenarios and identify bottlenecks at every stage of product realisation. It is not an isolated simulation environment but rather a deeply integrated, AI-powered development approach that directly links virtual design and testing with smart manufacturing.
AI models analyse data for predictive maintenance and for overall efficiency, detecting failures before they lead to costly production downtime requiring immediate intervention. With the emergence of trends such as AI-driven automation, latency is becoming an increasingly critical factor.
Since the 1990s, various shop floor management (SFM) systems have proven their worth and have been integrated into enterprise resource planning (ERP) systems. ERP is based on different manufacturing execution systems (MES), which utilise real-time information systems and embedded software, as well as programmable logic controllers (PLCs) and SCADA systems for control and data acquisition. For many years, SFM systems optimised production processes, minimised downtime and increased the productivity of tyre manufacturers. Today, however, the integration of all digital systems, including those involved in the product development phases, is essential.
For an integrated and efficient production model, latency – also known as ‘processing time’, i.e. the calculation or inference time of control systems – is of increasing importance in order to prevent malfunctions and ensure machine synchronisation. It must be virtually zero and is often measured in microseconds (μs) or milliseconds (ms) because industrial servers continuously monitor parameters such as vibration, temperature and pressure.
This is why the Chinese national standard for network architecture in tyre manufacturing mandates extremely low latency, less than or equal to 30 ms – a crucial factor for features such as remote monitoring and predictive maintenance.
Optical detection and image acquisition are playing an increasingly important role and are driven by AI-assisted feature extraction and deep learning systems. High-resolution cameras and laser monitoring systems control critical parameters in real time, such as tread and sidewall cross-section measurements, profiling and regularity, innerliner thickness mapping, bead geometry inspection and measurement of chafer thickness and width. The use of these models optimises the entire manufacturing process and ensures efficiency and precision.
Automated guided vehicles (AGVs) have been used for years in tyre factories to manage and ensure a smooth and efficient transport and flow of materials and tyres between workstations. More recently, autonomous mobile robots (AMRs) have emerged as intelligent tools capable of acting and moving independently, rather than simply being piloted. Their movements within the factory require minimal programming and intervention.
Tyre manufacturing systems are becoming more sophisticated and evolving with AI-powered automation. However, the overall production of the product is safer for long-lasting quality and for the benefit of customers…
For a long time, even a simple change in tyre size in factories required numerous manual interventions in different systems. Consequently, switching from one production plan to another, according to a given set of specifications, presents a classic challenge, as everything relies on the manual configuration of complex parameters, which generates a significant source of errors and scrap.
Following the successful integration of the intelligent and innovative production plan change management system, plan changes are facilitated by networking all systems via a Manufacturing Execution System (MES). Analysis of material consistency using Big Data enables automatic parameter adjustments. This simplifies processes, improves component stability and prevents material mixing errors during line changeovers.
Tyre manufacturing remains a traditional challenge; assembling dozens of components into a complete tyre is a labour-intensive process requiring numerous highly skilled workers. Autonomous tyre manufacturing machines operate without operators, utilising robots for material handling and positioning, thus ensuring high accuracy and repeatability.
The profile stabilisation time is crucial in the extrusion process for optimising the configuration and obtaining a stable, high-quality profile in just a few seconds. Artificial intelligence models analyse this stabilisation time with remarkable accuracy.
Dry cycle time (DCT) during tyre vulcanisation is crucial and a key area for continuous improvement. In a fully integrated, AI-driven tyre production system, vulcanisation parameters are optimised in seconds. This system ensures consistent production and prevents downtime through real-time alerts and near-instantaneous deviation correction. A powerful AI system simultaneously analyses data from over 250 vulcanising presses to identify the root causes of process variations.
A final tyre inspection system can use multiple high-speed laser sensors targeting key areas of the tyre. These sensors require microsecond-precise synchronisation to ensure simultaneous data acquisition from every point on the rotating tyre, creating a precise 3D map of the entire tyre. Intelligent 3D inspection sensors are equipped with integrated processors for instant quality control. They process high-resolution surface scans and determine conformity directly within the system.
The concrete and significant results achieved represent not just improvements but a true revolution in tyre manufacturing. Applying these principles, in line with industry averages, has increased productivity by up to 68 percent, reduced the defect rate by 57 percent and decreased inventory by 34 percent.
Integrated and automated quality control systems, which continuously monitor tyres, represent a true revolution in modern tyre factories. Manual quality control and material handling, which require significant human resources, can be replaced by up to 90 percent with intelligent systems in autonomous production systems. Finished tyres are transported to the warehouse by automated conveyors and software-controlled robotic handling systems.
A fully automated tyre manufacturing system allows for proactive intervention as soon as one parameter among thousands exceeds its control limits, thus preventing malfunctions before they even occur. In a networked system, real-time dashboards display live data to operators from mixers, timers and cutting machines, such as temperatures in temperature control unit (TCU) zones and dynamic pressure.
Automated production systems, combined with innovative, intelligent and integrated models, are particularly valuable for large production facilities. Modern tyre manufacturing goes far beyond mere ‘digitalisation’ or ‘Industry 4.0’, where even minor inefficiencies can lead to significant operational losses and customer dissatisfaction. Integration – from customer expectations to manufacturing control – enables the development and management of high-performing products with optimal overall equipment effectiveness (OEE).
Comments (0)
ADD COMMENT