Cleaner Pyrolysis
- By Sharad Matade
- July 04, 2025
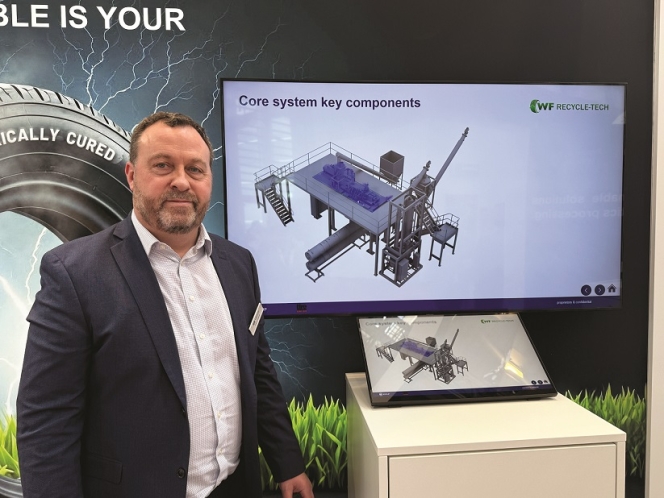
Paul Lloyd: “Farrel Pomini’s core business lies in supplying processing equipment for the plastics and petrochemical industries."
Pyrolysis has long been associated with pollution and inefficiency, particularly in developing markets where outdated methods dominate. However, technological advancements and a stronger push for circularity are transforming this perception. HF Group, through its subsidiary Farrel Pomini and WF Recycle-Tech, is at the forefront of this shift, introducing a continuous pyrolysis system that promises cleaner and more efficient tyre recycling. Unlike traditional batch processing, its technology ensures consistent output, better resource recovery and reduced emissions.
Pyrolysis has always been considered to be a dirty business. However, with the changes in technology and the increasing hunt for circularity across the tyre industry, businesses are attempting to redefine the age-old tyre recycling process and remove the malice associated with it.
Farrel Pomini is one such entity with the HF Group that is attempting to make pyrolysis cleaner. WF Recycle-Tech, established in 2013, started commercial operations in 2022 with selling its first pyrolysis unit in 2024, slated to be operational in 2026.
Speaking to Tyre Trends, President Paul Lloyd said, “Farrel Pomini’s core business lies in supplying processing equipment for the plastics and petrochemical industries. While its continuous mixer can be used for rubber applications, it is primarily designed for plastic masterbatches and compounds. The company operates across multiple divisions with its plastics compounding equipment focusing on niche applications for highly filled and temperature-sensitive materials. Although the plastics market is significantly larger than the rubber sector, Farrel Pomini targets specialised segments within it. Expanding its footprint in sustainability, the company has developed recycling systems for both plastics and rubber. The end-of-life tyre recycling solution was developed in collaboration with its group company, WF Recycle-Tech.”
Tyre pyrolysis has long been regarded as a polluting industry, particularly in developing countries where unregulated plants often operate at night to evade environmental scrutiny. In markets like India, many such facilities shut down due to non-compliance, reinforcing the industry’s reputation as a ‘dirty business’.
Lloyd further explained, “In Europe, the focus is shifting towards sustainability, driving innovation in pyrolysis technology. Traditional methods relied on large kilns, where tyres were burned with external heat over extended periods. The process was inefficient, labour-intensive and environmentally damaging, requiring extensive manual cleanup.
HF Group has taken a different approach, developing a continuous pyrolysis system that eliminates these challenges.”
Instead of batch processing, the system ensures a constant flow of material, allowing for the controlled capture of gases, liquids and solid outputs. The process begins with pre-grinding tyres into metal-free rubber crumb (6–20 mm), which is then fed into the machine via a hopper. Operating at a capacity of 1,500 kilogrammes per hour, the system requires only continuous material input while automatically managing output streams including recovered oil and gas.
Apropos to the pain points that the company wanted to address, he noted, “Over the past decade of developing this solution, several key learnings and priorities emerged. First and foremost, the goal was to create an efficient pyrolysis system that could consistently process tyre waste at an industrial scale. Second, the decision to develop a continuous rather than batch-based system was fundamental as continuous pyrolysis offers greater consistency, scalability and efficiency. Third, integrating a continuous mixer in the pre-processing stage became a major focus as it significantly improved the homogeneity and quality of the output materials. Finally, optimising the recovered output, particularly recovered carbon black, became the primary objective. Initially, the project was focused on tyre-derived oil (TDO), but as the market evolved, the emphasis shifted to producing the highest-quality rCB, aligning with upcoming ASTM standards and stringent industry requirements.”
By integrating advanced processing controls, the solution ensures cleaner, more efficient pyrolysis, positioning itself at the forefront of sustainable and cleaner tyre recycling.
THE OUTPUT
HF Group’s expertise in mixing technology creates a natural synergy between its traditional business and its expansion into tyre recycling. While the company is known for its tyre curing and rubber mixing solutions, it also has a plastics mixing division; this same mixing technology plays a crucial role in its pyrolysis process.
The recycling system starts with tyre crumb, which is fed into a high-shear Farrel Continuous Mixer originally designed for plastics processing. The mechanical shear heating raises the temperature of the material to 330 degrees Celsius. This ensures uniform heating before the material enters the pyrolysis chamber, where temperatures increase to between 520 degrees Celsius and 580 degrees Celsius. The continuous system eliminates inefficiencies seen in traditional batch pyrolysis, where prolonged heating cycles lead to higher energy consumption and inconsistent output.
Material recovery is a key advantage of the system. For every tonne of tyre crumb processed, approximately 50 percent is converted into pyrolysis oil, yielding 550–570 litres. Around 40 percent becomes recovered carbon black (rCB), a critical raw material that can replace virgin carbon black in industrial applications. The remaining 10 percent is gas, which can be used to power the system, further improving energy efficiency.
Beyond throughput, the system’s design significantly reduces overall energy demand. Mechanical shear heating minimises reliance on external thermal energy, while the continuous process prevents heat loss and optimises fuel efficiency.
Additionally, rCB from the pyrolysis process requires 60–70 percent less energy to refine, further enhancing sustainability.
“Pyrolysis fundamentally relies on heat and time in the absence of oxygen. Under these conditions, tyres thermally degrade, breaking down into vapour, which is condensed into oil and a solid residue, which is now widely used as recovered carbon black (rCB). This output can be further refined for industrial applications, creating a circular economy within the rubber industry,” explained Lloyd.
CHALLENGING INTEGRATION
The primary challenge for tyre manufacturers in adopting rCB is achieving performance characteristics comparable to virgin carbon black. Similarly, tyre pyrolysis oil must meet stringent quality standards to serve as a feedstock for high-value applications beyond just fuel. The company’s continuous pyrolysis system addresses these concerns by enhancing the quality and usability of both outputs.
“In the case of tyre pyrolysis oil, if used as a fuel, the calorific value may vary slightly, but it remains a viable option. However, its greater potential lies in serving as a feedstock for sustainable carbon black or even virgin carbon black production. The consistency of the oil’s composition determines its suitability for high-end applications, making process control a critical factor,” noted Lloyd.
He added, “For rCB, higher quality directly translates into increased usability across different applications. While rCB will never completely replicate virgin carbon black, superior grades enable a higher substitution rate. In some cases, a high-quality rCB can replace up to 30 percent of virgin carbon black, whereas lower-quality alternatives may only allow a 15 percent substitution. This increased usability not only enhances sustainability but also raises the material’s commercial value.”
HF Group’s rCB, produced through its WF Recycle-Tech process, has been extensively tested across multiple industries. It has demonstrated strong performance in plastics masterbatch applications, technical rubber goods and even tyre manufacturing. One major tyre producer has already validated its suitability for substitution in new tyres, underscoring its industry acceptance.
A key differentiator of the process lies in its patented two-stage pyrolysis system. While continuous pyrolysis itself is well established, HF Group’s innovation stems from its integration of a high-shear Farrel Continuous Mixer in the first stage.
This approach ensures uniform heating, eliminates direct heat exposure and optimises the pyrolysis reaction in the second stage. The result is a more efficient process that yields higher-quality recovered carbon black and cleaner tyre pyrolysis oil.
PERSEVERING THROUGH LIMITATIONS
The primary limitations of the system, Lloyd noted, revolve around scalability, operational efficiency and material consistency. The current processing capacity of 1,500 kilogrammes per hour is relatively low. Scaling up production rates while maintaining efficiency and reliability is an ongoing challenge. The key challenge is ensuring long-term operational stability and optimising run times.
Another significant factor is feedstock variability, particularly in markets like India, where used tyres from different sources such as passenger cars, trucks and buses are often mixed without segregation. The ideal scenario would involve processing a uniform type of tyre with a consistent rubber composition, but in reality, recycling operations must work with what is available.
“There are two main approaches to addressing this viz-a-viz meticulous sorting, which ensures consistency but is time-consuming and costly, or strategic blending, which creates a stable output by balancing material variations. The current system has been designed to handle diverse feedstocks without sorting, using a consistent blend of tyres to produce a predictable output,” said Lloyd.
In the long term, technological advancements such as artificial intelligence or tracking mechanisms for tyres could enhance sorting processes, making recycling operations more efficient. However, for now, the focus remains on refining the system to handle real-world feedstock conditions while delivering high-quality outputs. The continuous processing system also provides flexibility to adjust parameters and optimise results, making it a robust solution even in environments where feedstock quality is unpredictable.
MARKET TALK
The return on investment for pyrolysis systems is quite favourable, but it carries risks, especially in the early stages. A well-managed system operating efficiently for 6,000–7,000 hours per year, with a stable feedstock supply and consistent product quality, can generate strong financial returns, explained the executive.
However, challenges arise if there are interruptions in material supply, equipment downtime or fluctuations in product quality. These factors introduce uncertainty, which can make securing financing more difficult. That said, the market for TDO and rCB is growing, providing ample opportunities for revenue. Companies that can differentiate its output and meet quality standards can command premium prices, further improving ROI.
The market focus for HF Group’s advanced pyrolysis solutions primarily includes recyclers looking to add more value to their processes, material users such as tyre manufacturers and technical rubber companies seeking sustainable raw materials and new businesses emerging in response to industry needs.
“In the US and Europe, there is a growing entrepreneurial push to bridge the gap between traditional recycling and the sustainability requirements of the tyre industry. However, in markets like India and other parts of Asia, the challenge lies in shifting perceptions. Many existing pyrolysis operations use older-generation systems. The transition to modern, cleaner and more efficient systems requires education, proof of performance and financial support. Despite these challenges, India remains a strong market for HF, as the industry values high-quality technology and is willing to invest in the best solutions once the benefits are clearly demonstrated,” informed Lloyd.
Over the next five years, the company’s primary goal is to establish a proven track record with the first full-scale pyrolysis system, demonstrating its performance, reliability and efficiency. Once this is achieved, the focus will shift to helping potential customers secure financing by reducing perceived risks, making it easier for them to invest in the technology.
Alluding to the next phase of development, Lloyd informed, “The next phase of development focuses on three main areas. The first priority is industrialising the system to ensure it operates efficiently, consistently and reliably over long production cycles. This transition from pilot-scale to full-scale manufacturing is where HF Group’s expertise in engineering advanced processing equipment comes into play. Secondly, efforts are underway to further refine the pyrolysis reaction to enhance output quality and efficiency. Lastly, ongoing research and development is focused on post-processing improvements, particularly the removal of ash from recovered carbon black to increase its usability in high-performance applications.” n
Kraton To Raise Polymer Prices In North America Starting December 2026
- By TT News
- November 07, 2026
Kraton Corporation, a leading global producer of speciality polymers and high-value bio-based chemicals derived from pine wood pulping co-products, has announced a price increase of USD 220 per metric tonne, equivalent to USD 0.10 per pound, across all polymer products sold in North America. The affected lines include Kraton D SBS, Kraton D SIS and Kraton G SEBS/SEPS.
According to the company, the adjustment is necessary to offset significant and sustained increases in feedstocks, energy, logistics, process materials and other manufacturing costs. The increase will take effect on 1 December 2026 or as permitted by applicable contracts.
Evonik Strengthens Global Silicone Network With Essen Expansion
- By TT News
- November 04, 2026
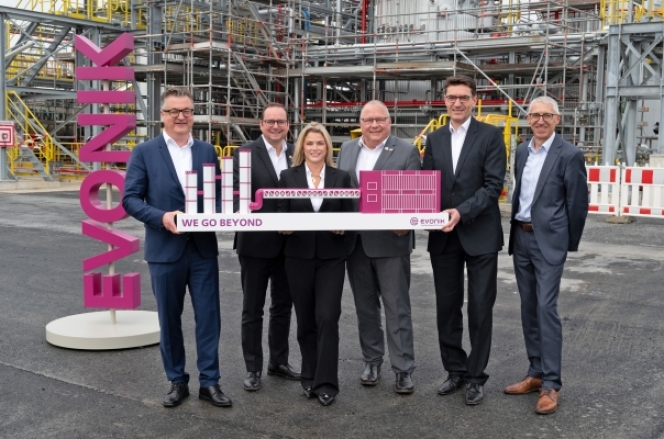
Evonik, a global speciality chemicals company, has completed a EUR 52 million expansion of its silicone platform at the Essen Goldschmidtstrasse site in Germany, constructing a new production plant and a large tank farm. The facility raises output capacity for organomodified silicones, a core product group in the company’s global silicone network.
The Essen site operates as a central node in that network, closely tied to Evonik facilities in Geesthacht, Obernburg and Wittenburg in Germany, Pandino in Italy, Shanghai in China and Hopewell, Virginia, in the United States. The expansion strengthens the resilience of this international production system by lessening the need to ship intermediates and finished goods between locations.
Logistics infrastructure has been optimised to support more efficient operations. A new 150-metre pipe bridge links four production units and 15 manufacturing assets to the tank farm, which comprises five stainless-steel tanks, the tallest standing 24 metere and holding substantial quantities of key raw materials. The result is steadier production, more robust supply chains and reduced reliance on short-term deliveries. The tank farm has enlarged the Essen site from 32 to 35 hectares.
The project was executed with the site fully operational and despite constrained space, drawing on roughly 80 Evonik employees and over 230 contractors from 25 partner companies. Essen Goldschmidtstrasse also features in Evonik’s newly developed long-term plans, which assign a clear profile to each of six major production sites – Essen Goldschmidtstrasse, Marl, Wesseling, Darmstadt/Weiterstadt, Rheinfelden and Hanau – as guidelines for future development. Under this framework, Essen Goldschmidtstrasse is positioned as a centre of excellence for customer-specific formulations.
Lauren Kjeldsen, the Evonik Management Board member responsible for the Custom Solutions segment, to which the business belongs, said, “This expansion strengthens our silicone production platform, enhancing supply chain resilience and creating a strong foundation for profitable growth. This latest investment highlights the important role that our innovative German sites play in the success of our global operations.”
Roberto VilaKeller, head of the responsible Business Line Interface & Polyurethane Additives, said, “The investment in Essen strengthens our global production network and further enhances our ability to serve customers reliably around the world. It significantly expands our production capabilities, reduces potential bottlenecks and creates opportunities for future growth in attractive markets.”
Thomas Kufen, Mayor of Essen, said, “At a time when industrial investment is more important than ever, projects of this scale send a strong signal for Essen’s economy and the wider region. They secure high-quality jobs, strengthen competitiveness and demonstrate the international attractiveness of our city as an industrial hub.”
- Association of Natural Rubber Producing Countries
- ANRPC
- Natural Rubber
- Monthly NR Statistical Report
ANRPC Publishes Monthly NR Statistical Report For September 2026
- By TT News
- October 31, 2026
The Association of Natural Rubber Producing Countries (ANRPC) has published its Monthly Natural Rubber Statistical Report for September 2026, a month marked by broad-based price gains. Firm fundamentals, constrained supply and steady downstream demand combined with geopolitical and macroeconomic uncertainty to lift prices. Renewed Middle East conflict and disruptions to major shipping routes weighed on sentiment, while energy markets were especially affected by the closure of the Strait of Hormuz and attacks on transiting vessels, which raised risks to global energy supplies and strengthened the crude oil risk premium.
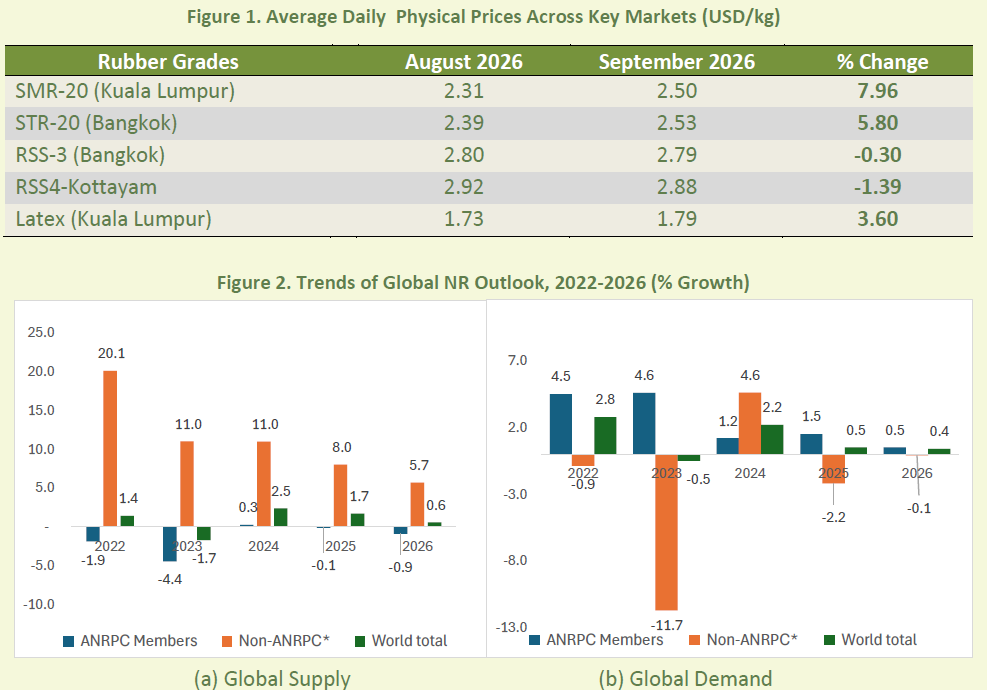
According to the report, physical prices for most major grades advanced. SMR-20 in Kuala Lumpur averaged USD 2.50/kg, up 7.96 percent month-on-month, and STR-20 in Bangkok rose 5.80 percent to USD 2.53/kg. RSS-3 in Bangkok slipped 0.30 percent to USD 2.79/kg, while RSS-4 in Kottayam eased 1.39 percent to USD 2.88/kg. Latex-in-bulk in Malaysia gained 3.60 percent to average USD 1.79/kg. Cautious tyre-manufacturer purchasing, limited to immediate needs after earlier increases, weighed on the RSS market. Latex drew support from tight supply, as persistent rainfall disrupted tapping and limited fresh and concentrated latex availability, while glove, healthcare and industrial demand held stable.
Trade flows diverged. China's imports grew 2.56 percent month-on-month, India's 11.36 percent and Malaysia's 17.85 percent, whereas Viet Nam's fell 3.40 percent. Exports rose 3.07 percent in Thailand, 7.30 percent in Malaysia and 1.91 percent in Cambodia, while Indonesia edged down 1.40 percent and Viet Nam recorded the steepest decline at 9.72 percent.
Global production is projected at 15.039 million tonnes in 2026, up 0.6 percent from 14.953 million tonnes in 2025, with September output estimated at 1.4 million tonnes. Uneven rainfall and elevated temperatures slowed supply recovery across Southeast Asia. Global demand is forecast to rise 0.4 percent to 15.356 million tonnes from 15.301 million tonnes, with the largest volume increases among ANRPC member countries. Prospects depend on vehicle sales, tyre production, shipping conditions and weather-related disruptions, while expanding electric-vehicle markets in China, India and Europe support modest growth.
The ringgit traded between RM4.04 and RM4.10 per US dollar, and the baht between THB 32.89 and 33.55. The SHFE January 2027 contract averaged CNY 19,070/tonne, up 5.3 percent month-on-month, and the SGX December 2026 contract averaged USD 2.41/kg, up 7.6 percent. Brent crude averaged USD 114.16 per barrel, a 25.3 percent monthly increase driven by geopolitical risks and shipping disruptions through the Strait of Hormuz.
- Birla Carbon
- Carbon Black
- Sustainable Carbonaceous Materials
- Sustainable Carbon Blacks
- International Rubber Conference
Birla Carbon To Showcase Electric Mobility-Focused Carbon Black Portfolio At IRC 2026
- By TT News
- October 28, 2026
Birla Carbon, a leading global supplier of carbon materials, will exhibit at the International Rubber Conference (IRC) 2026, scheduled for 2–6 November in Nagoya, Japan, at Booth B. The company aims to address application-specific demands arising from the shift towards electric mobility, which places greater emphasis on tyre wear and energy efficiency while requiring automotive rubber components to balance durability with ride comfort.
A Very High Structure (VHS) lineup awaits manufacturers of passenger car, light truck, truck and bus tyres. These grades were engineered to meet electrification requirements and tightening standards such as Euro 7, delivering gains in tread wear, energy efficiency and tyre longevity.
Sustainability also features prominently. The company's Continua Sustainable Carbonaceous Materials (SCM) and Sustainable Carbon Blacks (SCB) lines, which contain higher levels of recycled or bio-based material, are intended to help tyre makers pursue circularity targets. Their dependable quality and ability to be supplied at scale in large volumes make them viable for production use, and the Continua range carries ISCC PLUS certification.
Mechanical rubber goods round out the display. Grades aimed at bushings enhance mixing and dispersion, contributing to fatigue life and component durability, while formulations for mounts pair low hysteresis and low stiffness with reinforcement so that durable parts can be produced without sacrificing ride comfort. Drop-in grades for extrusion reduce defects, scrap and screen-pack changes while raising throughput and extending service life. Simulation and technical expertise help customers assess materials, and global production plus Asian capacity growth support long-term supply.
Amit Kumar, President – Asia, Birla Carbon, said, “Asia’s tyre and rubber manufacturers are shaping the next phase of mobility, and their material requirements are becoming increasingly stringent. As the clear leader in our industry, Birla Carbon aims to grow alongside our customers, combining application-focused innovation with dependable local supply. We see performance and circularity as priorities that must progress together. By expanding our capabilities in Asia and strengthening customer partnerships, we aim to help manufacturers meet evolving market needs and build greater long-term competitiveness.”
Comments (0)
ADD COMMENT