- MegaRide
- VESevo
- Flavio Farroni
- Aleksandr Sakhnevych
- Andrea Genovese
- weaRIDE
- tyre simulation
- motorsport
- RIDEsuite
Megaride: From Academic Lab To Global Tyre Technology Innovator
- By TT News
- April 16, 2025
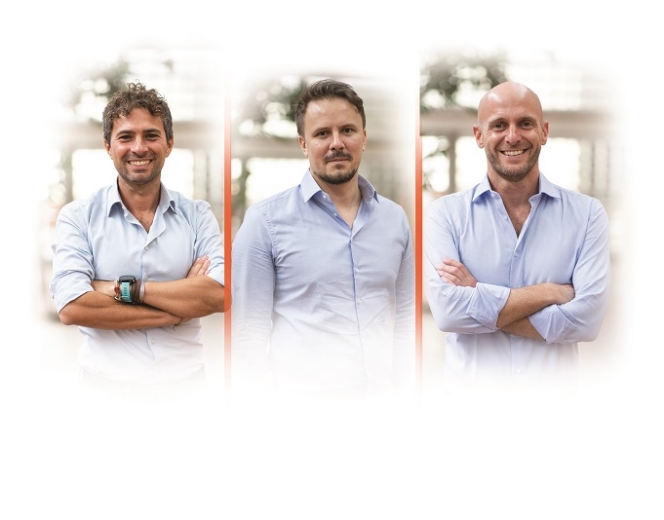
Led by CEO Flavio Farroni, the company has expanded into what he describes as a ‘MegaRide holding’, comprising multiple specialised businesses, each targeting different segments of the automotive technology sector.
“We embrace an unconventional approach to startup building: we invest in organic and gradual growth, which keeps us independent from private funding and allows us to reinvest our revenues into the team and R&D projects fully,” says Farroni, who co-founded the company after conducting tyre research at the university.
FROM ACADEMIA TO INDUSTRY DISRUPTOR
MegaRide’s journey represents a new technology transfer model from academia to industry. Farroni acknowledges that this transition wasn’t without challenges.
“The main leadership challenges we faced along our journey were, first and foremost, gaining acceptance for our role as researcher-entrepreneurs – researchpreneurs – both within academia and in the market. In the beginning, neither was sufficiently advanced to recognise such a new and competitive figure,” Farroni explains.
This ‘researchpreneur’ model has since become central to MegaRide’s competitive advantage. The company maintains close ties with universities and ensures a continuous pipeline of cutting-edge research that feeds into commercial applications.
“Our deep synergy with universities makes research and innovation our core mission. This allows us to explore methodologies and techniques that may not immediately apply to current products but lay the groundwork for future advancements,” explains Aleksandr Sakhnevych, MegaRide’s Chief Technology Officer.
ITALIAN TECH FIRM REVOLUTIONISES TYRE SCIENCE WITH PHYSICS-BASED SIMULATION
In a nondescript business park on the outskirts of Naples, a team of researchers-turned-entrepreneurs is quietly revolutionising how the world’s leading vehicle manufacturers and motorsport teams understand tyre performance. MegaRide, founded by academic researchers from the University of Naples Federico II, has grown from a university spinoff to one of the most innovative players in automotive simulation technology.
The company specialises in physics-based modelling software that predicts tyre behaviour with unprecedented accuracy – crucial information for both racing teams seeking competitive advantages measured in milliseconds and vehicle manufacturers designing safer, more efficient cars for everyday drivers.
THE TECHNOLOGY: DIGITAL TWINS FOR TYRES
These physics-based models simulate how tyres behave under different conditions, predicting temperature changes, grip levels and wear patterns in real time with an accuracy that was previously impossible.
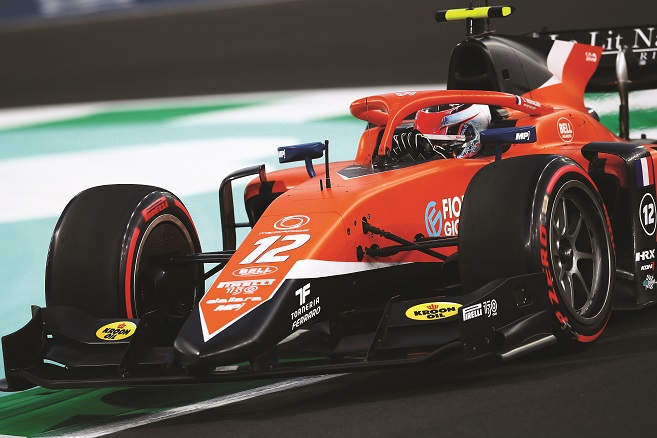
One of its most innovative products, weaRIDE, enables real-time tyre tread wear and chemical degradation simulation. This technology is particularly significant for electric vehicles, whose instant torque delivery creates new challenges for tyre durability.
“We were the first to develop a commercial thermal model for tyres, the first to create a multiphysics Pacejka-based model, and today, we are the first to introduce a wear and degradation model, weaRIDE, internationally awarded for its innovation. We try to be always a step ahead, and scientific research is our ‘secret weapon’,” Farroni says.
Sakhnevych explains that ensuring model accuracy across varied real-world conditions requires a multifaceted approach: “MegaRide ensures the accuracy and reliability of the weaRIDE model through a multifaceted approach. First, there is a continuous effort to enhance the physical fidelity of the model, leveraging a strategic synergy with universities and research institutions.”
He adds, “Additionally, a key focus is placed on improving data processing methodologies. Tyre models often face scrutiny due to the limitations in predictive accuracy, which are strongly influenced by the quality of the calibration data.”
FROM SIMULATION TO MEASUREMENT: THE VESEVO SPINOFF
In 2018, MegaRide expanded its footprint by spinning off VESevo, a company focused on developing innovative testing equipment for tyre materials. VESevo’s flagship product enables non-destructive testing of tyre compounds, providing detailed mechanical property data previously unavailable without destroying the tyre.
Andrea Genovese, CEO of VESevo, explains how the technology has evolved from its motorsport origins: “VESevo is evolving its motorsport-derived technology to enhance industrial applications, leveraging its versatility for real-time quality control in tyre manufacturing. Its non-destructive, non-invasive and rapid-testing capabilities allow each tyre to be analysed directly on the production line.”
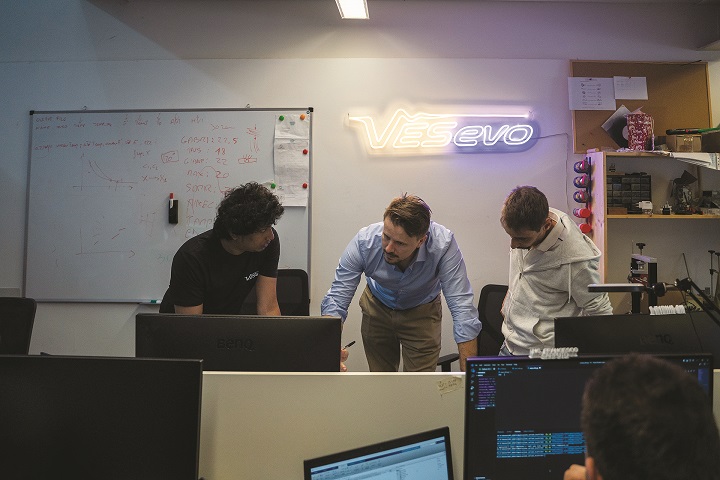
This represents a significant shift in quality control for tyre manufacturers. “This innovation enables mechanical property testing to be performed not just on a sample basis but on the entire production, guaranteeing comprehensive quality assessment,” Genovese adds.
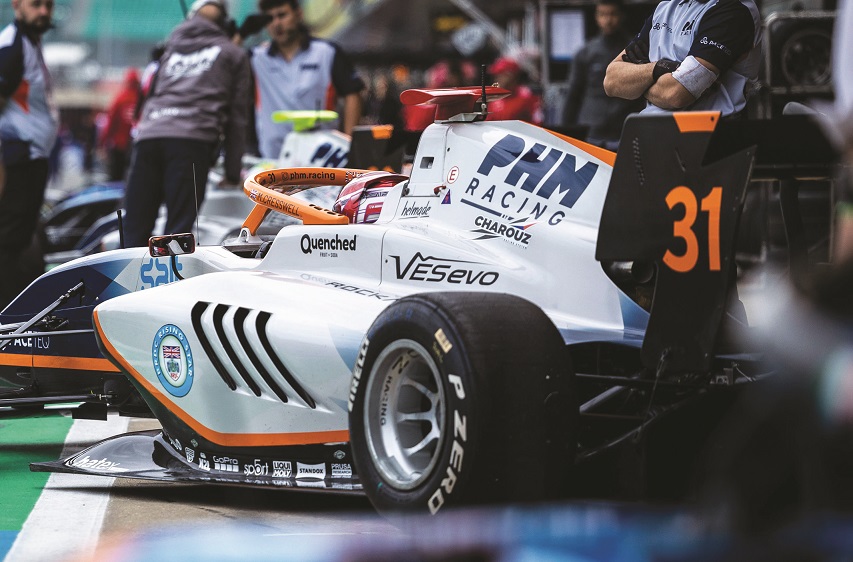
However, VESevo has faced regulatory headwinds in motorsport, particularly after the Fédération Internationale de l’Automobile (FIA) introduced rules limiting the use of its technology in Formula 2 and Formula 3.
“Honestly, we were surprised by this regulatory change, as motorsport has always been a driving force in introducing innovations, especially when they enhance performance, spectacle and safety, benefiting all stakeholders involved,” Genovese admits.
Rather than seeing this as a setback, VESevo has focused more on industrial applications. “By broadening our reach into new applications, we are not just navigating these changes, but we are turning them into opportunities to drive innovation forward,” Genovese says.
STRATEGIC ACQUISITIONS AND GROWTH
MegaRide has augmented its technological capabilities through strategic acquisitions, including the 2022 purchase of Wriggle Solutions’ intellectual property. This acquisition bolstered MegaRide’s capabilities in real-time tyre wear monitoring.
“The acquisition of Wriggle Solutions’ intellectual property in 2022 has expanded MegaRide’s strategic line, accelerating the transition from purely simulation-based technologies to real-time, onboard vehicle sensing,” Sakhnevych explains.
This move has enabled MegaRide to develop virtual sensors that can estimate previously unmeasurable parameters like vehicle sideslip angle, tyre temperature and tread wear. These capabilities have applications for vehicle performance, safety systems and autonomous driving technologies.
MegaRide has also established key partnerships with major industry players. Its collaboration with Prometeon, an industrial tyre manufacturer, illustrates how the company’s technology is being applied beyond high-performance vehicles to commercial transport.
THE CHALLENGE OF SCALING HIGH-PERFORMANCE TECHNOLOGY
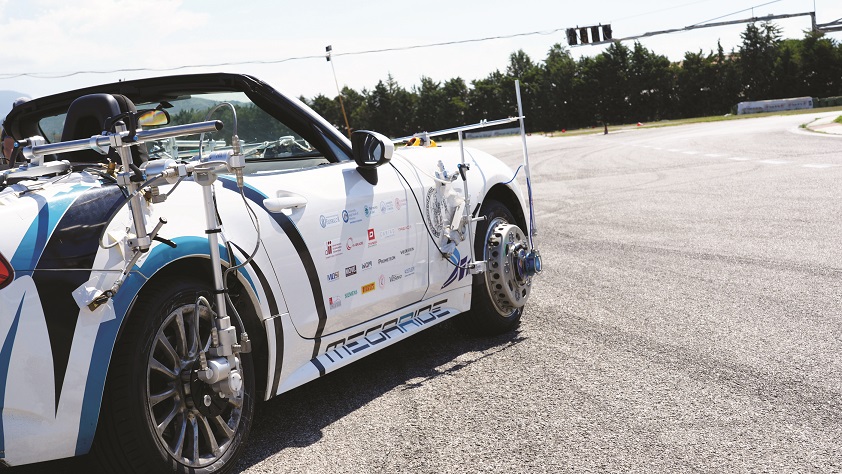
Transferring technologies developed for the extreme demands of motorsport to mass-market applications presents significant challenges. Sakhnevych outlines several hurdles: “One of the main challenges is cost, as motorsport applications rely on high-end sensors and powerful computing. To make these solutions viable for mass production, MegaRide focuses on leveraging existing vehicle sensors and optimising software to run efficiently on standard ECUs.”
He continues, “Scalability is another hurdle, as consumer vehicles operate in diverse and unpredictable conditions. Ensuring robust performance across various road surfaces and driving styles requires extensive validation and adaptive modelling.”
THE AI QUESTION
As artificial intelligence (AI) transforms industries worldwide, MegaRide maintains a measured approach to incorporating machine learning (ML) into its products. The company’s roots in physics-based modelling inform its perspective on AI’s role in tyre simulation.
“MegaRide leverages artificial intelligence and machine learning while staying true to its roots in physics-based modelling,” Sakhnevych says. “Our background in academic research, particularly in mechanical engineering, has shaped our expertise in model-based approaches."
He distinguishes their approach from purely data-driven methods: “Unlike purely data-driven methods, our approach enables prediction without extensive training datasets – simply by parametrising models using well-established physical principles.”
DATA SECURITY CONCERNS
As vehicles become increasingly connected, handling sensitive data securely becomes increasingly important. MegaRide has developed comprehensive approaches to data security, particularly relevant to its onboard sensing technologies.
“MegaRide addresses data privacy and security concerns in tyre technology through a robust combination of encryption, secure data management protocols and role-based access controls,” Sakhnevych explains.
COMPETITION FROM INDUSTRY GIANTS
As a small company operating in an industry dominated by global corporations, MegaRide faces significant competitive pressures. However, Sakhnevych sees advantages in the company’s nimble structure.
THE FUTURE: EXPANSION AND DIVERSIFICATION
Looking ahead, MegaRide plans to continue expanding through organic growth and the development of new ventures within its holding structure.
“The ‘MegaRide holding’ concept will allow us to diversify our strategies, expanding into various sectors we consider strategic,” Farroni explains.
“MegaRide’s models are increasingly used by OEMs, tyre manufacturers and racing teams, and the technological landscape is moving towards a greater adoption of physics-based models like ours, driven by the growing use of real-time simulations.”
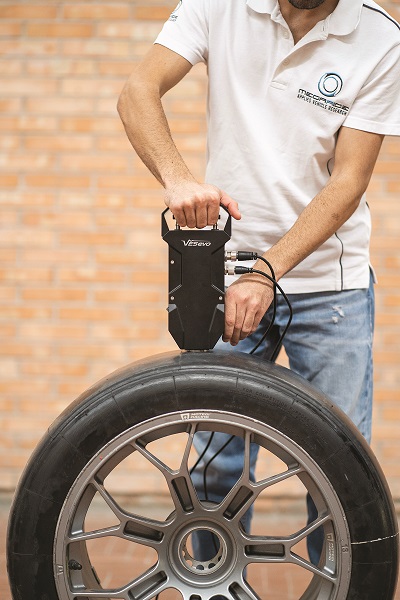 Each company within the holding structure has its strategic direction. “VESevo, originally founded to produce a portable device for motorsport, is now evolving – thanks to key strategic partnerships – into a provider of non-destructive testing solutions and quality control systems for tyres, directly integrated into production lines,” says Farroni. The newest addition, RIDEsense, targets emerging opportunities in vehicle automation. “The increasing onboard computational power of vehicles has led to the creation of a new company, RIDEsense, focused on developing ‘Virtual Sensors’ – real-time algorithms capable of estimating otherwise unmeasurable quantities and providing critical insights for ADAS and autonomous driving systems, which will be pivotal in tackling the mobility challenges of the coming years,” explains Farroni. VESevo’s Genovese describes a similar approach to balancing immediate market needs with long-term innovation: “At VESevo, balancing short-term business goals with long-term research and development is part of our DNA. As an academic spinoff from the University of Naples Federico II and an innovative company, we follow the same path that MegaRide successfully pioneered, transforming cutting-edge research into commercially viable solutions while maintaining a strong focus on technological advancement.”
He elaborates on their dual-track strategy: “In the short term, we focus on delivering market-ready solutions that meet the immediate needs of our customers, particularly in motorsport and industrial applications. By working closely with teams and manufacturers, we ensure our technology provides tangible value and rapid returns, allowing us to sustain growth and reinvest in innovation.”
Meanwhile, the academic connection remains vital: “Our strong ties to the academic world allow us to act as a ‘bridge’ between research and industry. This close connection enables a constant exchange of knowledge, technology, expertise and skills, accelerating innovation while ensuring our developments translate into real-world impact,” says Genovese.
A MODEL FOR RESEARCH COMMERCIALISATION
MegaRide’s success offers a blueprint for commercialising academic research in highly technical fields. The company has carved out a unique position in the automotive technology ecosystem by maintaining close ties to academia while developing practical market applications.
The company’s ‘researchpreneur’ model provides a case study in technology transfer that may be increasingly relevant as universities worldwide seek to translate research into commercial impact. MegaRide demonstrates that deep technical expertise can be successfully paired with entrepreneurial vision when the right structures and leadership are in place.
As vehicle electrification, automation and connectivity create new challenges for tyre performance and safety, MegaRide’s physics-based approach to simulation and testing positions the company to play an increasingly important role in the future of mobility.
What began as academic research in a Naples university laboratory has evolved into a group of companies pushing the boundaries of what’s possible in understanding the complex interactions between tyres and roads – knowledge that underpins both the thrilling spectacle of motorsport and the mundane safety of everyday driving.
Hidden Cost In Tyre Plants: How The Rubber Moves
- By Gaurav Nandi
- October 14, 2026
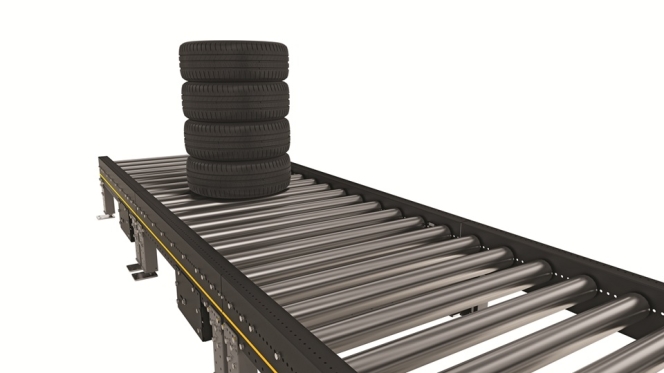
Interroll’s Gianmichele Piciocco argues that some of the largest efficiency gains in tyre manufacturing lie in the interfaces between machines, not only in the machines themselves.
Tyre manufacturers invest heavily in the best building machines and the fastest curing presses. The systems that connect them, however, are often specified late, inherited from earlier projects and seldom revisited, according to Gianmichele Piciocco, Global Strategic Business Development Manager at Interroll.
“Material flow is the backbone of the entire tyre industry,” Piciocco tells Tyre Trends. In his experience, engineers select and position process equipment first, and transport follows. The consequences emerge later, in energy consumption, maintenance stoppages and the cost of expansion. He argues that ‘we have always done it this way’ becomes a design constraint in its own right once technology, product mix, energy costs and safety expectations have changed. The examples that follow point to two closely connected areas: system optimisation during design and expansion, and lifecycle optimisation during operation.
THE LAYOUT TRAP
Piciocco says the pattern is consistent across the tyre manufacturers he advises. “In many cases, the layout initially proposed does not fully match what is ultimately implemented, often to contain the initial investment,” he says. Soon after start-up, plants may find that they need more buffer capacity, or that future expansion was not fully considered. With no floor space left, the remedy for material flow is often inclines, declines and additional levels, which can significantly increase costs.
 The alternative is far cheaper if raised early. “At the design stage, and with possible expansion in mind, it is worth asking whether small changes in machine positioning could support more effective and flexible material flow,” he says.
The issue is especially relevant in India, where sustained market growth does not always mean new greenfield plants. Expansion often happens inside operating sites, where new capacity must coexist with several generations of equipment from multiple vendors. Without a common architectural logic, each extension can add another component family, control standard and maintenance practice, increasing complexity and the potential for integration and compatibility problems.
REOPENING THE BELT QUESTION
Green-tyre transfer illustrates how convention hardens into constraint. Uncured rubber is soft and contamination-sensitive, and belt conveyors have long been the default because a continuous surface supports the tyre and certified belt materials address contamination. Piciocco does not dismiss that logic. He argues it should no longer be treated as absolute.
Left on widely spaced rollers, a green tyre can begin to deform during relatively short stops, and contact with the wrong material can degrade quality after curing. One approach being evaluated by Interroll combines closely spaced rollers, software that keeps them ‘skating’ when the line stops and transfer materials selected to meet contamination requirements. Where a roller solution suits the application, he says, component cost can be materially lower than a belt’s. Because a belt is a continuous element, maintenance work can also take longer and be more complex.
The larger benefit, he argues, is commonality. The same families of rollers, drives and transfer modules can serve both pre-cure and post-cure sections, reducing the spare parts a plant holds and the skills its teams must learn. “Who is interested in saving money in the life cycle of the plant? The user,” he says.
SAVING ENERGY BY DESIGN
Piciocco says moving from conventional 400-volt drive systems to zoned 24/48-volt roller conveyors can reduce energy use, with savings of up to 50 percent in some applications. The low-voltage architecture can also simplify installation and maintenance and reduce exposure to hazardous voltages at machine level, subject to applicable safety standards. The advantage, he stresses, comes chiefly from the on-demand, zoned operating principle, in which only the zones a product needs are active, rather than from voltage alone.
Another example concerns a leading tyre producer that wanted a more compact layout within an existing plant while retaining sufficient buffer capacity and scope for future expansion. The initial conveyor concept required several accumulation loops, curves, inclines and declines, making both engineering and installation relatively complex.
“Working together, we proposed a solution comprising a motorised ascending spiral, an overhead bridge and a gravity spiral for the descent,” Piciocco says. “Each spiral has a footprint of roughly three metres in diameter. At a height of about 7.5 metres, the motorised spiral can provide buffer capacity for approximately 25 to 40 tyres, depending on their dimensions.”
The configuration provided the required buffer in a very compact footprint, with fewer powered components and a cleaner, more modular installation. Its cost was in line with, or slightly above, the conventional solution. Piciocco says the question he put to the customer’s technology director was simple: “Are you thinking about today, or the next 10 years?”
GROWING WITHOUT REBUILDING
A brownfield expansion is not simply a matter of adding more metres of conveyor. New sections must fit existing space, controls and maintenance organisation while the plant keeps running.
Interroll’s modular platforms, including the MCP range, are built from standard modules. RollerDrive EC5000 units, managed by MultiControl electronics, form a highly scalable and energy-efficient material handling system.
In a conventional centralised architecture, adding zones can require additional I/O, cabling and software changes. In a decentralised system, expansion means adding a module and an Ethernet connection. Independently controlled zones can also absorb small cycle-time differences and micro-stoppages without passing every interruption down the line. Upgrades follow the same logic. The 24-volt EC5000 versions rated at 20 and 35 watts with Analogue Interface (AI) can be used as replacements for the earlier EC310, supporting a more straightforward maintenance approach and the extension of existing installations.
ROUTING WITHOUT OVER-ENGINEERING
Not every route variation calls for a sorter. When tyres must be directed to testing, quality inspection, rework or the next process, Interroll’s position is that a modular conveyor backbone with targeted transfers and diverters often gives a better balance of performance, footprint and cost than a sorter built for distribution logistics. Further downstream, particularly after warehousing, higher volumes and more destinations can justify a dedicated sorter such as the company’s MC-S range.
Piciocco’s warehouse example shows the risk of getting this wrong. A large operator that stacks and stores tyres with considerable automation then needs a separate, costly sorting system to retrieve and route them. In this part of the process, he says, a solution such as Interroll’s MC-S can provide the required throughput with a more efficient layout and a significantly smaller footprint.
CONTINUITY INTO DOWNSTREAM HANDLING
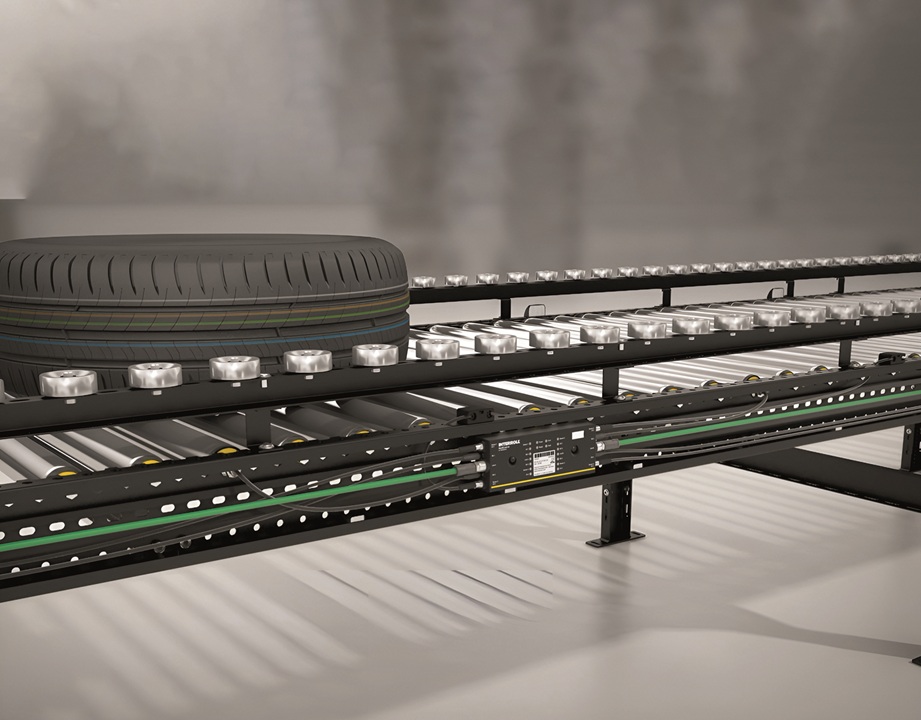
Where load and duty allow, the same architecture can extend past the individual tyre. A 24/48-volt modular pallet conveyor, the MPP platform, can handle a load of up to 500 kilogrammes per metre while retaining decentralised control and zero-pressure accumulation. Rollers of 60 millimetres in diameter allow a closer pitch and more support points, which, after application validation, can reduce vertical undulation when handling tyre stacks.
Piciocco is careful not to make continuity a dogma. Above the platform’s operating envelope, robust 400-volt heavy-duty conveyors remain the correct choice.
FROM REACTION TO PLANNING
Maintenance is where Piciocco sees the most overlooked cost. When total cost of ownership and plant availability are considered, he says, maintenance and stoppage-related costs can account for around 10 to 15 percent of the overall cost associated with material flow in some applications, including labour, spare-parts inventory and lost production during downtime. “Maintenance is often treated as something that simply happens. It should not be. Much of it can be avoided,” he says.
Connected drives, such as the RollerDrive EC5000 BI with MultiControl, make more than 100 parameters available, including operating hours, cycle counts, temperature, system status and error type. If the torque required by a motor rises progressively, the system can flag an abnormal trend before it develops into a stoppage and give the maintenance team a stronger basis for planning an inspection.
Without that information, a failed motor can cause a prolonged stoppage while crews identify the source and check whether the spare part is available. With an early warning, maintenance can schedule the intervention; for an accessible RollerDrive with the spare available, replacement can take less than an hour. Piciocco calls this preventive rather than predictive maintenance. The data does not replace maintenance expertise, but it gives teams a stronger factual basis for decisions, and standard components make diagnostics and training common across the plant.
GLOBAL STANDARDS, LOCAL EXECUTION
A shared catalogue alone does not make a standard, Piciocco says. It also needs consistent selection criteria, spare-parts strategies and support after start-up. Interroll has production, engineering and service capabilities across the world’s main industrial regions, allowing global standards to be supported by local execution. Its life-cycle offering includes structured maintenance programmes, dedicated stock of critical components, periodic audits and staff training, scaled to how critical the application is.
He applies the same logic across markets. Using a smartphone as an analogy, Piciocco says the same platform can be used in a basic configuration or with more advanced functionality, depending on a plant’s needs and technological maturity. A manufacturer can therefore retain common components, diagnostics and training across sites while adapting the level of automation to local conditions.
That flexibility extends to how far automation should go. Speaking for himself, not Interroll, Piciocco says not every producer needs a dark factory. The appropriate level of automation depends on volumes, product mix, process maturity and available skills. “If people do not understand how the technology works, you can have the best technology in the world, but it will not be used properly and may even become a limitation,” he says.
REAL ISSUE
Asked what single mindset shift the industry needs, Piciocco did not hesitate. “Interface,” he says. “The machines are already quite optimised. The problem is how we serve the machine.” As individual machines become increasingly optimised, the interfaces between them play a growing role in improving productivity, simplifying maintenance, reducing energy consumption and enabling future expansion.
“Material flow should not be the last part of the engineering process,” he adds. “If it is considered earlier, we can contribute to a solution that supports optimisation of the entire plant.”
ATIRE Appoints Thierry Miche As Director Of Oem And Product
- By TT News
- October 13, 2026
ATIRE, a leading Sri Lankan Solid tyre maker, has appointed Thierry Miche as director of OEM and product, effective September 2026, bringing more than 25 years of experience in the global tyre and mobility industry to the role.
At ATIRE, Miche will lead the company's OEM and product activities, focusing on portfolio development, OEM relationships and expansion into new technical and commercial markets globally.
Miche joins from Michelin, where he spent 26 years in senior product and operational leadership positions, including roles at Solideal and Camso before their integration into the French group.
His most recent position was product Management Director for Beyond Road, with global strategic and operational responsibility for the product portfolio. He led teams across Belgium, Canada, France and the US, working with research and development, industrialisation, original equipment manufacturer (OEM) and aftermarket sales, and supply chain functions.
Previously, Miche was Product Line Executive Director For material handling, overseeing the global product platform and holding full profit and loss responsibility for three manufacturing sites in Belgium, Germany and the US. He also led global research and development teams in Belgium and Sri Lanka.
His career has spanned product management and engineering, technical support, warranty management, quality assurance and systems. The experience covers the development and delivery of products across engineering, industrialisation, validation, sales and supply chain operations.
The Tyre Giant That Doesn’t Want A Dark Factory
- By Sharad Matade
- October 13, 2026
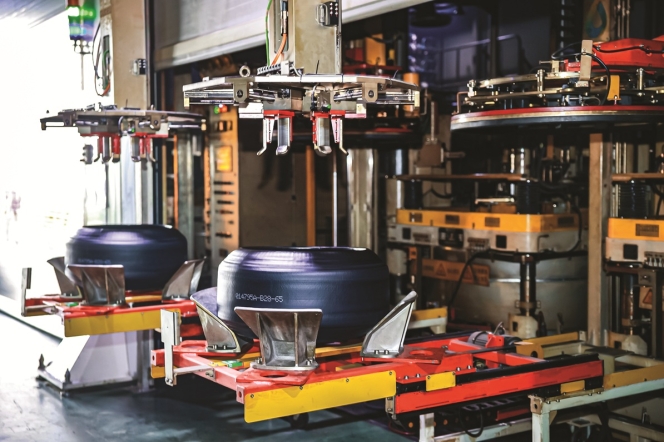
ZC Rubber, China’s largest tyre maker, is running 18 AI agents across its Hangzhou 5G plant. It insists the goal is smarter manufacturing, not emptier factory floors.
Walk into the industrial conversation about automation these days and ‘lights-out’ production tends to come up within minutes: factories with no people, no lighting and machines working in the dark. However, ZC Rubber, the Hangzhou-based group that ranks among the world’s top nine tyre companies, would like to correct that impression before it takes hold.
“We see this as a 5G Smart Factory, or Future Factory V2.0, rather than a ‘dark factory’. The goal is intelligent manufacturing, not simply removing people from the production process,” the company said in an interview.
That is a notable position from a company that has just put 18 AI agents to work across its production chain and reports defect rates well under half those of its earlier operations. It is also a considered one, and the details explain a good deal about how the world’s largest tyre market is approaching the factory of the future.
PEOPLE AT THE EXCEPTIONS
ZC Rubber’s division of labour is simple. Automation, AI and real-time data are steadily taking over what the company calls ‘repetitive and highly standardised operations.’ Its people are being moved towards engineering, process management, quality assurance and the handling of exceptions, meaning the unusual problems that no model has seen before.
“We will continue to increase automation, but fully unmanned production is not the goal,” ZC Rubber said. “It is about combining intelligent systems with human expertise.”
The same logic applies to the future. Asked whether lights-out production is on the roadmap, ZC Rubber was clear. “We do not see fully lights-out production as a goal in itself. Technology will be introduced where it brings clear improvements in quality, efficiency, safety and sustainability,” it said.
EIGHTEEN AGENTS, ONE PRODUCTION CHAIN
The scale of the AI deployment is considerable. Since June 2025, ZC Rubber has introduced 18 AI agents across the full production chain. Their use ranges from AI-assisted formulation and virtual simulation to equipment maintenance, production scheduling and quality control. According to the company, they have helped shorten tyre development cycles by 50 percent and lifted production efficiency by 50 percent.
Where does the value come from? Not from any single stage, the company suggests. “The biggest value comes from using AI to analyse production data, optimise process parameters and support faster decision-making across the manufacturing process,” it said. ZC Rubber does not currently publish a stage-by-stage breakdown of the gains.
INSPECTION AND THE DEFECT RATE
Quality control is where the company’s numbers are most striking. Its latest AI-based visual inspection systems, it says, can achieve a defect detection rate of close to 100 percent, improving both the speed and the consistency of inspection. That matters most in high-volume passenger car radial (PCR) output, where human inspectors face the twin problems of fatigue and sheer throughput.
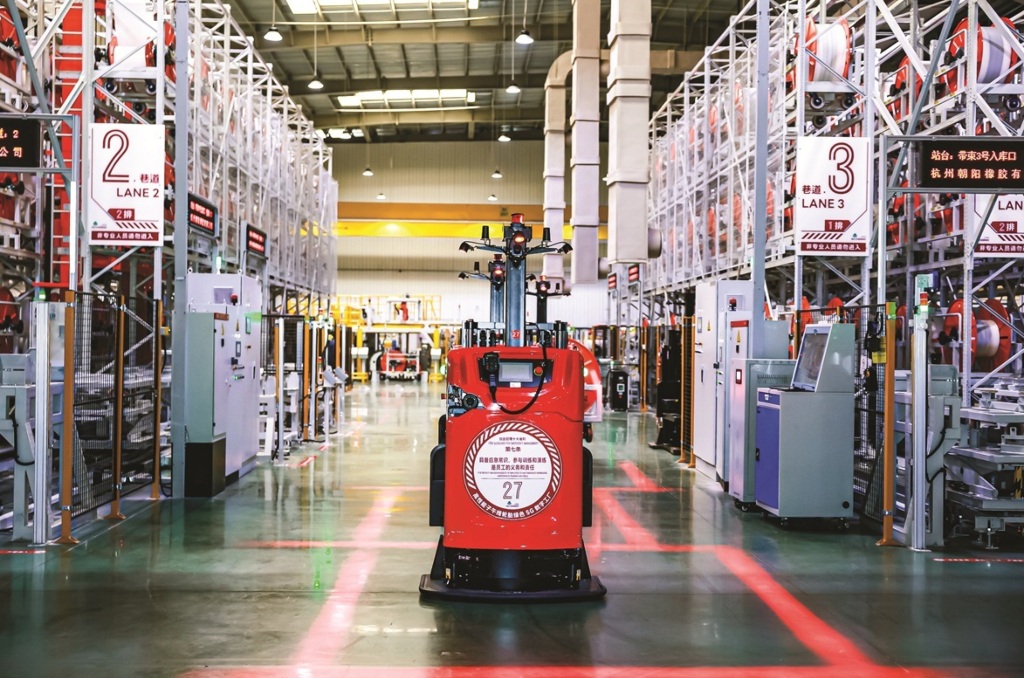 Zooming out, the company says AI and digital quality control across its smart manufacturing system have cut its product defect rate from 1.2 percent to 0.5 percent.
HOW THE SYSTEMS TALK TO EACH OTHER
“Thousands of sensors collect production data in real time, while 5G connects equipment, quality inspection and logistics systems,” the company said. The APS+MES system pulls production, quality and logistics information into one place ‘so operations can be monitored and adjusted quickly’. AI and big data analytics then help staff spot problems and make faster production decisions.
AN EARLIER SET OF NUMBERS, UPDATED
ZC Rubber’s earlier claims of a 15 percent efficiency gain, up to 40 percent lower defect rates and a 5 percent cut in energy use make one notice that the latest figures are considerably better. The company is candid about why. “Those figures reflect an earlier stage of our smart factory development,” it said.
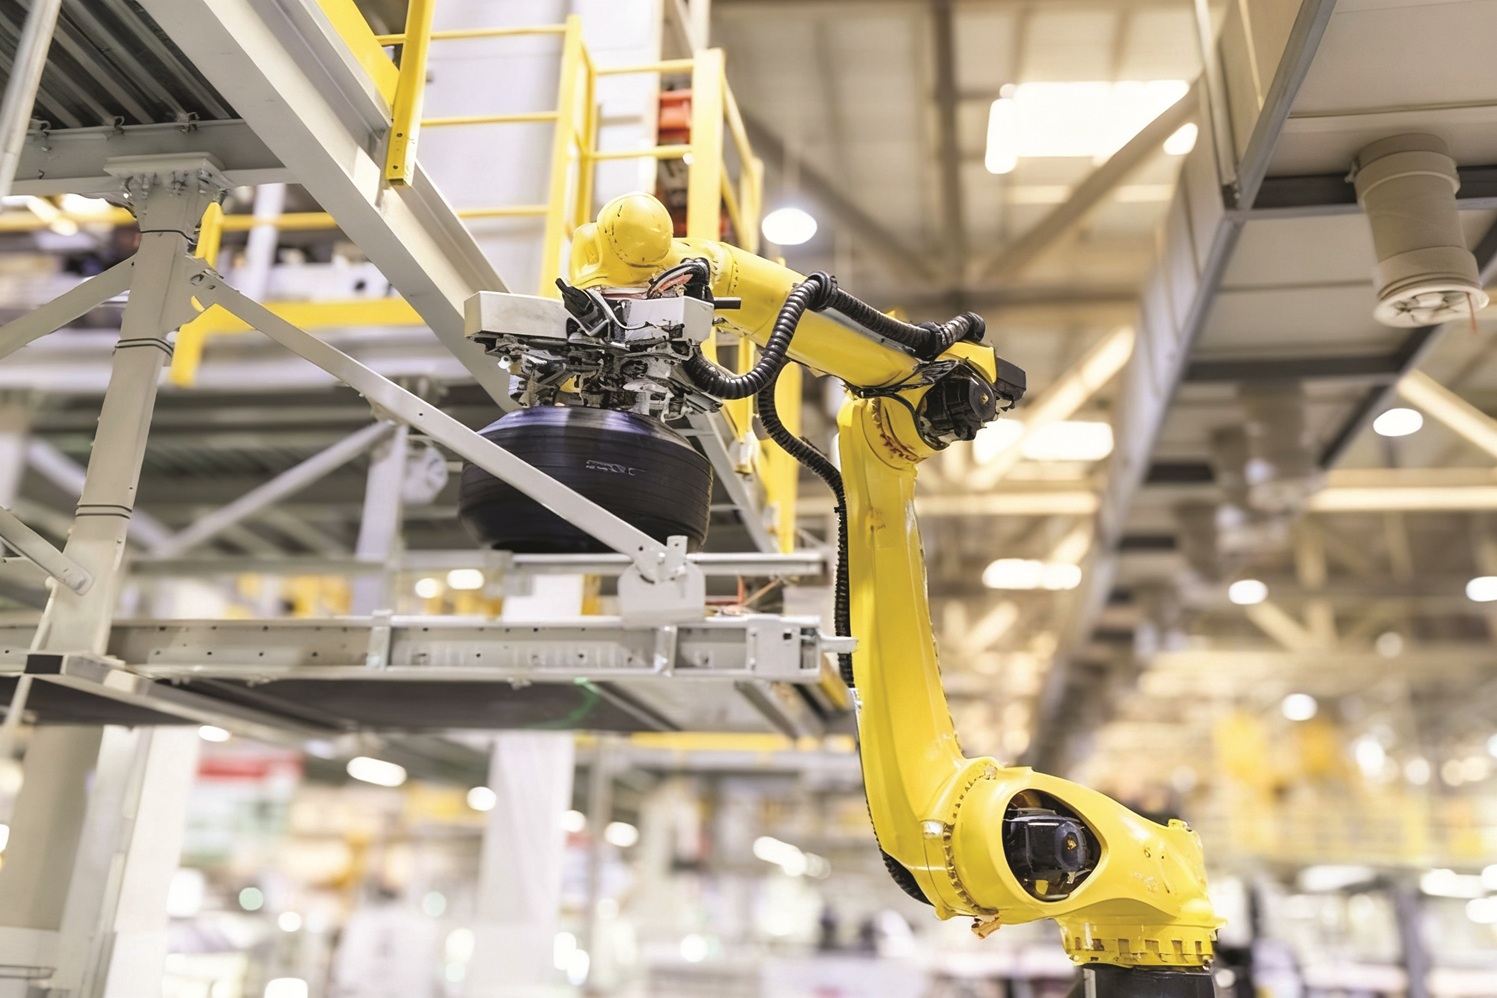
The current numbers, for the 5G Smart Factory, are a 50 percent improvement in production efficiency, defect rates down from 1.2 percent to 0.5 percent and a 10 percent reduction in overall energy consumption.
As for which technology deserves the credit, ZC Rubber declines to rank them. “We do not break down the improvement by individual technology,” it said, naming instead the key components: AI-based process control, automated inspection, intelligent logistics, APS+MES production management and data-driven quality control.
ENERGY, MEASURED VALVE BY VALVE
The energy figure is worth a closer look, because it comes from a fairly granular system. ZC Rubber’s energy management combines 5G, IoT, big data, AI and digital-twin technologies. Smart sensors, smart meters and smart valves feed real-time data into a central energy platform, while AI supports analysis and operational optimisation.
The division of labour among the technologies is neat. “5G provides the connectivity, while AI, big data and digital twins help turn the data into better energy-management decisions,” the company said.
TWO PLATFORMS AND A DIFFERENT STARTING POINT
The manufacturing story is inseparable from the development story. ZC Rubber runs two proprietary technology platforms: the X-Tech System, primarily for truck and bus radial (TBR) tyres, and the Phecda Tech System, primarily for PCR tyres. Each integrates compound formulation, tyre structure, process engineering, simulation, testing and intelligent manufacturing within a single development framework.
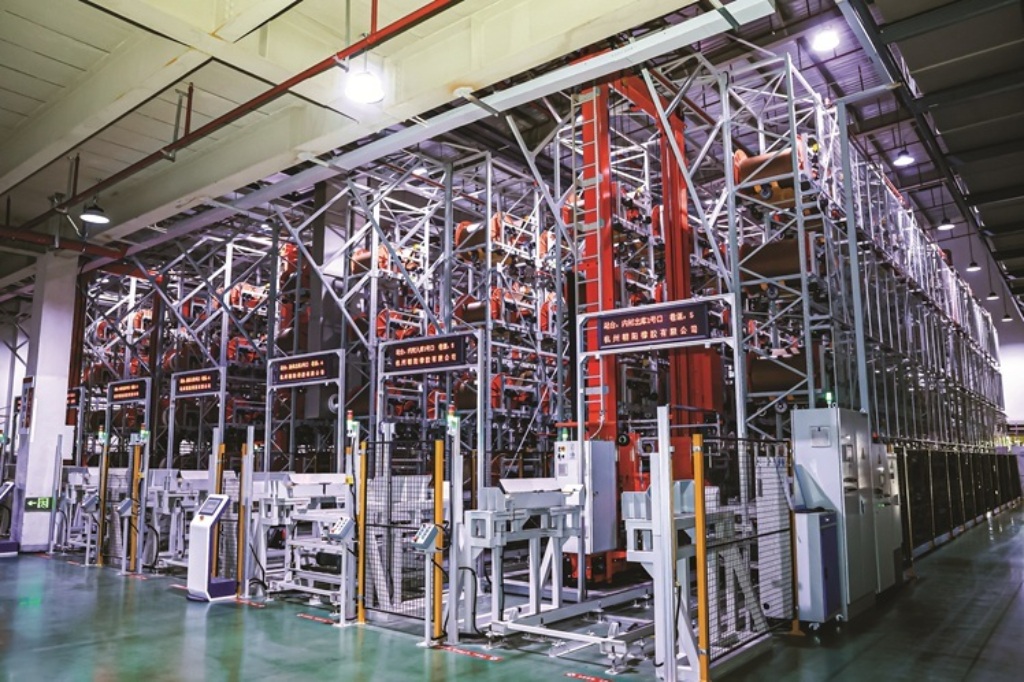
Their defining feature is what the company calls the Forward-development Approach. Traditional development, it explains, “often starts from an existing product and improves it through repeated design and testing cycles”. ZC Rubber starts elsewhere: with the target performance, whether that is vehicle characteristics, duty cycle, climate, road conditions or customer requirements. The compound, tyre structure and manufacturing process are then built around those targets. “This shifts the workflow from repeated iteration to a more integrated, target-driven development process,” the company said.
That, it argues, is where the halving of development time comes from. The 50 percent reduction reflects ‘a more integrated digital development process’, combining engineering expertise with simulation, AI-assisted tools and closer links between R&D, testing and manufacturing. AI lets engineers evaluate more design options against defined performance targets, and virtual simulation cuts out unnecessary physical iterations.
How tightly these platforms are wired into live production data has not been shared publicly. X-Tech and Phecda, the company said, connect R&D, manufacturing and validation within an integrated development process, but the detailed real-time data architecture behind them ‘is not something we currently disclose publicly’.
Henry Shen, ZC Rubber’s Senior Vice President, has made the wider point in the context of the group’s recent State recognition. “Our objective is not simply to develop an individual material, tread pattern or manufacturing process,” he said. “X-Tech and Phecda are complete development systems that connect user requirements with simulation, materials, tyre engineering, manufacturing and validation.”
THE STATE PRIZE
That recognition is significant. ZC Rubber, together with Harbin Institute of Technology, has been awarded the Second Prize of China’s State Science and Technology Progress Award for a project titled ‘Key Technologies and Green Intelligent Manufacturing of High-Performance Tires’. It is one of the country’s highest state-level honours for scientific and technological innovation, and ZC Rubber says it is the only Chinese tyre manufacturer in the past decade to win it at the Second Prize level or above.
The company backs the claim with spending. In 2025, it invested around RMB 1.54 billion (approximately USD 226 million in R&D, equal to 3.43 percent of annual revenue, according to its annual report. The award, it says, recognises technologies that have ‘progressed beyond laboratory research into industrial application’.
GLOBAL FOOTPRINT
ZC Rubber has built a truly global footprint, combining a strong manufacturing base in China with an expanding network of operations across Europe, the Americas, Southeast Asia and beyond. In China, the company operates through multiple sites, including its headquartered in Hangzhou and facilities in Tianjin, Chaoyang, Jiande, Qingquan, Yonggu, Anji and Jintan, supported by dedicated units for recycling technology and automotive aftermarket services in Hangzhou.
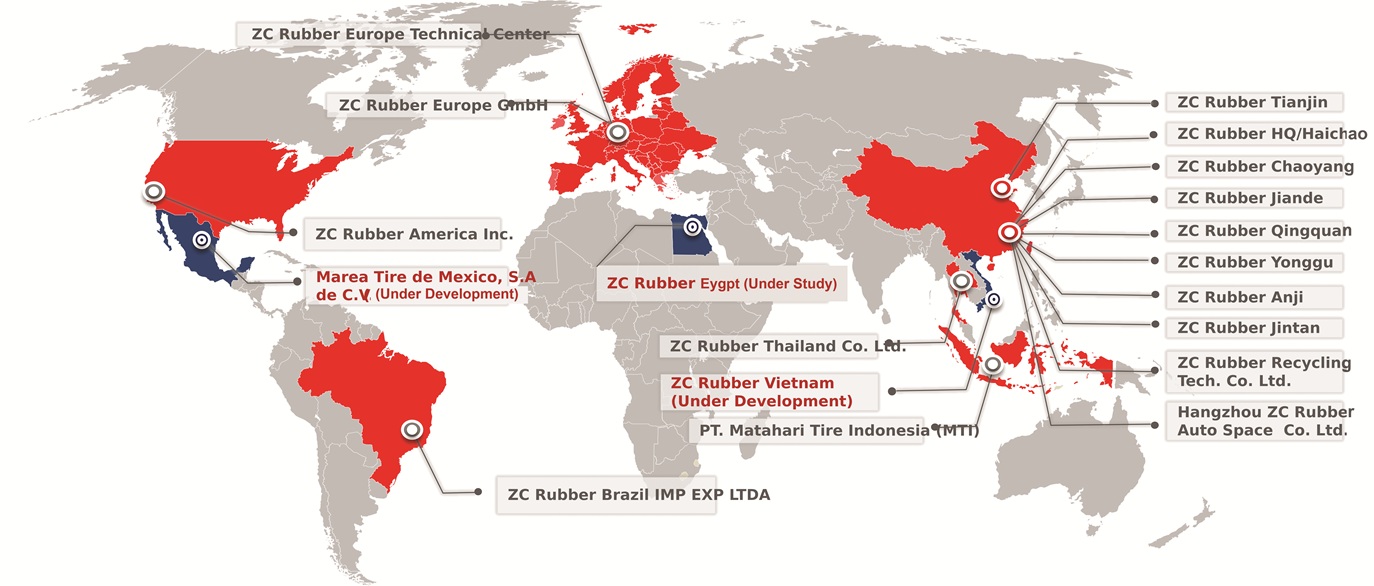
Beyond China, ZC Rubber has established a European presence through ZC Rubber Europe GmbH and its Europe Technical Center, alongside ZC Rubber America Inc. in the United States, ZC Rubber Brazil IMP EXP LTDA in South America and ZC Rubber Thailand Co. Ltd. and PT. Matahari Tire Indonesia (MTI) in Southeast Asia.
The company is also preparing for further expansion, with new projects under development in Vietnam and Mexico (Marea Tire de Mexico, S.A. de C.V.) and a feasibility study underway in Egypt. Together, these locations allow ZC Rubber to serve customers closer to their markets, strengthen supply chain resilience and combine local insight with global technical expertise.
CUSTOMISATION WITHOUT THE PENALTY
The forward-development model has a commercial payoff: tyres tailored to where and how they will be used. Asked whether the platforms allow genuine mass customisation, including regional climates and EV-specific requirements, ZC Rubber answered ‘to a significant degree’.
“X-Tech and Phecda allow us to develop tyres around specific climates, road conditions, vehicle applications and performance targets, including EV-specific requirements,” it said. On the factory floor, flexible production lines adjust output as product mix and orders change. The company does not disclose a separate efficiency figure for customised production, though ‘the goal is clear: to increase product flexibility while keeping production efficient’.
The regional examples are concrete. In Asia, X-Tech underpins the X-Elite Truck Tyre Series. In Europe, it is applied to the WESTLAKE Gen II commercial lineup, with a focus on fleet efficiency, performance and regulatory requirements. Phecda sits behind the WESTLAKE ZuperAce Z-007 and GOODRIDE Solmax 1 passenger tyres, and technologies from both platforms have been applied across ARISUN’s full TBR and PCR ranges for the Americas.
“International markets do not have identical requirements,” Shen said. “A tyre developed for European highway fleets, Southeast Asian transport operations or passenger vehicles in the Americas must respond to different vehicles, roads, climates and customer priorities.”
WHAT COMES NEXT
Much of the technology commonly billed as next-generation is already in service at ZC Rubber. Automated logistics, AI-based visual inspection, process optimisation, digital simulation and virtual testing are all in use. Digital twins are applied in areas such as energy management, and a broader digital-twin virtual factory is part of the next-stage plan.
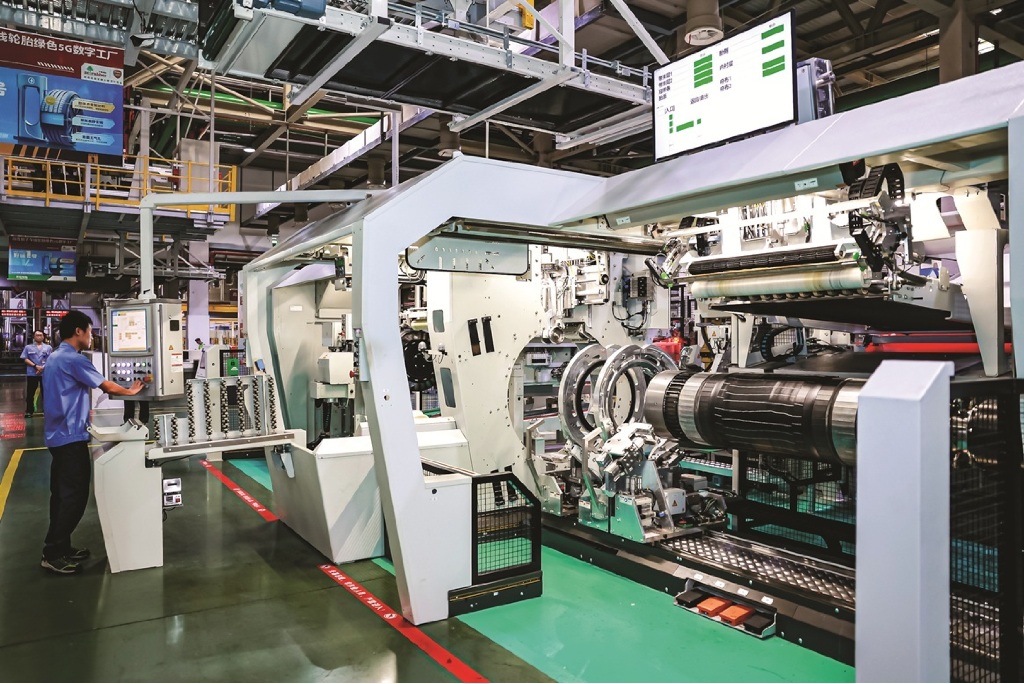 The company frames the coming three years as a period of deepening rather than reinvention: more smart-factory applications, more AI and industry-specific models and close attention to emerging technologies such as humanoid robotics ‘as they mature’.
That phrasing may be the most revealing thing about ZC Rubber’s approach. It is chasing results rather than headlines. As the company itself puts it, the launch of the Hangzhou plant marks ‘a new opportunity and starting point’, and its stated ambition is to become a world-leading tyre company with higher standards. Whether the lights stay on, it seems, is the least of its concerns.
AMETEK Completes USD 5bn Acquisition Of Indicor Instrumentation Businesses
- By TT Bureau
- October 12, 2026
AMETEK recently completed its USD 5- billion all-cash acquisition of a portfolio of instrumentation businesses from Indicor.
The businesses, collectively known as Indicor Instrumentation, make equipment for industrial and scientific applications. Their products serve markets that overlap with AMETEK’s existing operations and generate recurring revenue from consumables, services and aftermarket support.
David A Zapico, AMETEK’s Chairman and Chief Executive, said: “We are excited to complete this highly strategic acquisition and to welcome the Indicor Instrumentation team to AMETEK. With its mission-critical solutions, deep technical expertise, and strong positions in attractive end markets, Indicor Instrumentation is an excellent fit with AMETEK. We also see meaningful opportunities to create value through integration into our proven operating model.”
Indicor Instrumentation is expected to contribute about USD 350 million to AMETEK’s sales in 2026 and to be modestly accretive to adjusted earnings for the year.
The acquired businesses will join AMETEK’s Electronic Instruments Group and Electromechanical Group, according to their products and market focus.
Comments (0)
ADD COMMENT