AUTOMATED TYRE MANUFACTURING: NO TURNING BACK
- By Sharad Matade & Juili Eklahare
- October 14, 2022
There couldn’t be any industry that isn’t implementing, or at least knowing about, automation. And if there’s actually one, then it has probably been living under a rock. The tyre industry has already opened its doors to automation, and this helps make tyre manufacturing more sophisticated and reliable. The tyre manufacturing process itself has been experiencing constant changes – from different tyre sizes and constructions to targeting less usage of energy. Automation must be on every tyre company’s to-do list, if it hasn’t adopted it already. Don Heelis, Sales Manager, Cimcorp, gave Tyre Trends more insights on the different aspects of automation in the tyre industry and its absolute requirement, when we met him at the Tire Technology Expo 2022 in Hannover, Germany. Read on…
The philosophy of tyre manufacturing has changed dramatically. A part of the change in that philosophy relates to automation implementation in the tyre manufacturing process. However, we also find more technical perspectives being adopted and taken into account at new, modern tyre factories today.
This technical perspective can be considered to be coming from a few different areas, one of them certainly being from the actual production part of the tyre factory. Therefore, with production machinery, mixers, extruders and tyre building machines, the level of technology being implemented in these processes is increasing. Moreover, these processes are getting more sophisticated.
The other aspect of this is integrating the production across all the different areas (another factor for the dramatic change in the modern tyre factory). In the past, the different areas of production were not necessarily well connected. However, today we see them getting connected a lot more – and this is being driven and enabled by technology.
This is where companies like Cimcorp come in – who happen to provide material handling and automation technology so that different tyre manufacturing processes are better integrated.
Explaining this, Don Heelis, Sales Manager, Cimcorp, said, “When you produce your work in process, what you’re producing is in synchronisation with what’s being produced in other areas of the factory. This helps minimise the work in process and have a manufacturing process that’s more efficient.”
Going the modular way
But how does one integrate different machines and processes in the plant with all the different machines and manufacturing processes involved? Heelis let us in on this.
“The trick is to implement the automation and connectivity in a modular way,” he revealed and went on, “That way, the connectivity is physical and mechanical but involves software as well. Thus, we take an approach where the modules are flexible and can connect to various inputs and outputs; however, the module is in itself standardised. Hence, the modules can work for different factories – only the interconnection needs to be flexible.”
The green tyre
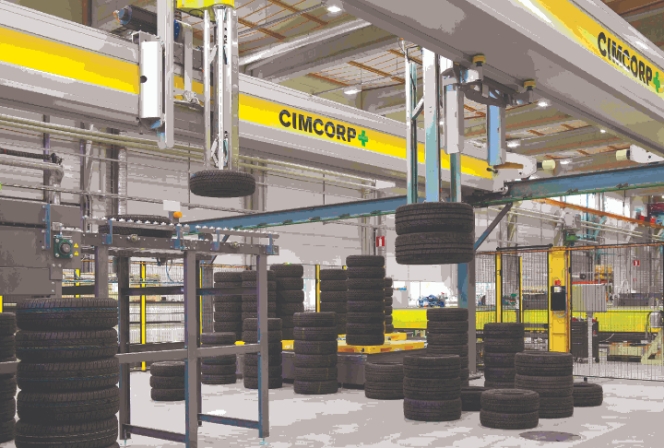
While implementing automation, one, of course, would want to implement it where they get the biggest value. “Traditionally, that has been in the palletising area – in managing and handling the finished product. Basically, palletising, storing and retrieving the finished product,” Heelis informed us and continued, “This is where everyone has traditionally looked in the past. However, a lot of focus has been put on the green tyre area in the past 10 years. That includes green tyre handling, storage and retrieval and its automatic delivery to the curing process.”
A green tyre is work in process – simply put, a tyre that has not been cured. “A green tyre is made up of a number of components. It’s built on a tyre-building machine,” Heelis further told us. “Once a green tyre is built, it is buffered, followed by being cured – and automation machines are required in order to do this. Hence, this is a key element of the modern tyre factory.”
He added, “This has been an area of key focus where productivity and simplicity can be gained. In fact, the whole process can be done with less plant floor space. Ultimately, factories that want to be competitive have to implement automation technologies in that area.”
Increased efficiency
There are many brownfield factories out there that have to modernise and be viable for the future. One of the key areas that they need to modernise and automate in is green tyre handling. Heelis asserted, “By having an automated storage and retrieval system, one can track and trace all of the work in process. Plus, one is able to store in a manner that maximises the quality of the green tyres. And then, one can deliver them from the storage system to the curing process in a very systematic and accurate way. This way, when a particular green tyre is needed in the curing area, it can be delivered there in the appropriate amount of time.”
“In this methodology, when the green tyre arrives at curing, it is at that point in time when it is needed, and the production does not have to stop,” Heelis further shared. “If this can be achieved, then the curing process can be run more efficiently; the efficiency can go from 80 percent to over 95 percent. In theory, one can increase the output of their factory by 10 percent. In such a case, one can imagine how many tyres can be produced in a factory by following this methodology.”
Automation – its role during the pandemic and inflation
While automation tends to bring in efficiency, how have companies managed to keep up their competence and productivity during the thorny period of the Covid pandemic? The pandemic has definitely brought some insights to the tyre industry from a management point of view, like it did to many other sectors. According to Heelis, automation has come to the rescue of the tyre industry in the pandemic as well.
“One important thing that the industry learnt from the pandemic was that it has a risk to its ability to produce products,” he mentioned and went on, “The absence of automation will make any company in the industry highly dependent on the labour force, which might not be available to keep the production going. On the other hand, with automated processes, a company is less at risk to events like a pandemic.”
Another issue we are dealing with right now in the global economy is inflation. Inflation equals to costs going up – from the cost of materials to the cost of labour. “Nonetheless, a company can mitigate some of the impacts of inflation if it has embraced automation. In fact, the ones who automated their brownfield factories three to four years ago are in a much better position today than their competitors who had not,” Heelis pointed out and went on, “This is because the former can mitigate some of the inflation costs, is less dependent on the workforce and is able to produce better-quality products – and at a higher level of efficiency at that. We know that there is a tremendous shortage of people in the workforce in the US right now. Therefore, automated companies have a significant competitive advantage.”
From the tyre industry’s challenges due to the pandemic and inflation, we turned to the challenges Cimcorp itself faces on the commercial side. Heelis responded that, commercially, the current challenge for them is being a low-cost, high-quality producer – which one has to be in order to compete in the market. “Furthering this challenge is how we become a low-cost, high-quality producer and stay that way. And from our perspective, the way to get there is through innovation and technology,” he stated.
Automation in the Asian tyre industry
CIMCORP opened up an office in India roughly three years ago. With its presence in the country and Asia, Heelis told us that the tyre companies in Asia are no stranger to automation and are implementing it. “As a move forward, the mentality is that if you want to be a world-class manufacturer and build a new factory, then you build the factory with automation. And this is a global perspective,” Heelis asserted.
Cimcorp’s customers in Asia range from traditional tyre manufacturers to new manufacturing entrants in the industry, so it’s a mix. Throwing further light on this, Heelis said, “We all know the traditional manufacturers like Bridgestone, Michelin, Goodyear, Continental and more. But beyond these, there are new companies emerging. And these new companies have an advantage in some ways because they are not constrained by the old ways of thinking. They are forward thinking, with a clearer mindset to do things in the current environment – the environment of automation and technology.”
“Moreover, the manufacturers who don’t invest in automation, and try to run the company with practices that were developed in the 1960 and 70s, will not be able to survive or compete,” he further added. “Their market will eventually consider them to be non-competitive, non-global and unable to produce the quality expected of them.”
Cimcorp has plans for India as well. “Our strategy is to continue to grow our business in India with the domestic tyre manufacturers, and we have been successful at that,” Heelis shared and went on, “When I say domestic, that goes for manufacturing facilities within India, from Apollo Tyres to MRF to JK Tyre to Goodyear to Michelin. Thus, we plan to continue to build our business with those factories and customers from an automation perspective, and then from a full customer service point of view.”
The other aspect comes to brownfield factories. Heelis averred, “With brownfield factories, whether in North America or Asia, the cost of automation is the same; there may be different payback scenarios between the two. However, it stands true that no matter where a company is present in the world, if it is operating a brownfield factory, then it needs a strategy to modernise. And the strategy to modernise is based on implementing automation.”
Automation in brownfield factories – what will it take?
The strategy to modernise when automating a brownfield factory is especially challenging in an already existing system. Therefore, when automating a brownfield factory, one of the most important considerations is to not interrupt their day-to-day production, Heelis cited. He mentioned that the factory has to continue making its certain number of tyres each day. Hence, a strategy that enables the factory to do that is needed – while concurrently implementing automation there.
“Besides, when you implement automation, you have to be able to do it in a standardised way,” Heelis further enlightened and continued, “This can be done with the help of flexible automation modules that can work in a lot of different scenarios. Therefore, you can deal with different brownfield factories depending just on how you arrange your automation modules. Thus, you can come up with a custom solution for every different brownfield factory out there with the help of a modular approach and on the basis of how you connect those automation modules together.”
Service provided
From providing standard modular systems to hardware to software, Cimcorp strategically has a service aspect to its business – Success Services. Therefore, the approach from its service side is to enable its customers to be as successful as possible.
“That could be achieved by providing a 24/7 support. So if the customers contact us due to an issue they are facing in the solutions provided by us, we are available at any time of the day or night to support them,” Heelis revealed and added, “We can do it remotely. In fact, as technologies emerge further, we’ll see how we can do this more remotely with virtual techniques. Here, their serviceperson could be using special tools, which enables our people (who are remote) to actually be in virtual situations in our customers’ plants. In such wise, we can be more responsive and be as if we are in place in real-time in order to provide a service.”
Tyre warehouse automation or manual operation – making the choice
Nevertheless, Cimcorp does not just stop at its 24/7 services or providing its automation solutions for tyre manufacturing processes. It goes beyond that – to the finished product warehouses. However, interestingly, that depends to a degree on which part of the world the automation is needed in; while some areas will need automation that is well advanced, some areas will use a more manual operation.
Heelis explained, “There are some key factors that determine whether the facility/area in question needs to be automated or not. For example, the cost of real estate. If it’s a manual operation, then that typically involves a very large warehouse, say around 100,000 sq mt.”
“For automating, on the other hand, you require lands that are much smaller,” Heelis further highlighted. “For instance, land is very expensive in Japan. Thus, one wouldn’t want a very big footprint warehouse over there. Which means, you go vertical wherever land is expensive.”
“On the flip side, land is very cheap in some areas and inexpensive to build the generic building (like in some areas of the US). So there is less incentive to go vertical with automation there,” he added. “But there might be other factors that could dominate.”
Choosing automation over manual operation – why?
While some main factors do influence the decision if a warehouse is going to be a fully automated one or a semi-manual one, an automated one is always preferred. For clear reasons.
“The benefit of an automated warehouse is that everything is extremely well controlled,” Heelis informed. “What’s more, you have complete control of your product – you know exactly where it is, how much of it you have and you can get on-demand access.”
“As for a semi-manual warehouse, there are fork trucks, people moving things around and putting them in different storage locations,” Heelis further clarified. “This process is much more manual, involves a lot more interaction and is time consuming. Therefore, you have much less control over the process.”
Automation – a need not to be confused as a luxury
The automotive industry has been one of the earliest industries to adopt automation. So it’s high time that tyres, an integral component of any vehicle, did so too. It’s clear that automation, today, is not a luxury but a need. No company can afford to not have it. No tyre company must be limited to older technologies, and they must invest in automation for the long term. This would not just help tyre manufacturers meet their customers’ demands without any delay, but also help modernise the industry with the world’s rapidly changing technologies.
From Data Overload To Decisive Action
- By Nilesh Wadhwa
- October 23, 2026
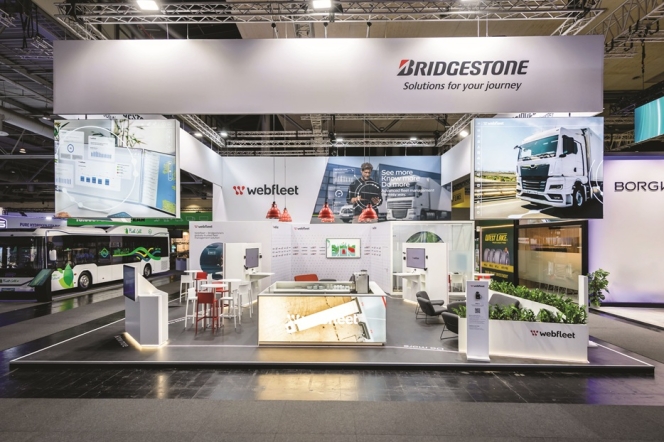
As commercial vehicle operators face mounting pressure from regulations, rising costs and the shift to electric power, Webfleet, a subsidiary of Bridgestone, is focusing on turning ever-growing volumes of vehicle data into practical recommendations that improve performance and ease the daily burden on fleet managers.
Founded in Leipzig in 1999 as one of the world’s first web-based fleet management platforms, Webfleet has grown from a pioneering software-as-a-service (SaaS) start-up to Europe’s leading solution and a core part of Bridgestone’s global offering. Today it serves drivers across more than 180 countries with AI-powered insights, electric-vehicle tools and sustainability data that turn complex operations into clearer, more efficient decisions.
In an exclusive interaction with Tyre Trends, Marc Notenboom, Director of Product Management at Webfleet, shares how the company has watched the fleet-management sector evolve over more than a quarter of a century. Interestingly, it was just last year the company marked its 25th anniversary.
From its inception, Webfleet has seen the volume of available data explode, yet the real challenge remains converting that information into meaningful guidance.
“Fleets give you more data but not more insights, which continues to be a challenge. Because of new regulations, new sensors, increasing competition and customer demands, we end up generating more data. We also have access to more data, which is growing exponentially. And then comes the real question, how do you make sense of that data?” Notenboom observed.
 Marc Notenboom, Director of Product Management, Webfleet
Webfleet obtains its information through black-box devices installed in vehicles, sensors or direct connections to original-equipment manufacturers. This includes telematics, GPS, video, driver behaviour and vehicle diagnostics, among others. The company then processes that stream to deliver fleet-management services.
The next step, he explained, is moving beyond retrospective analysis. “Insights tell you what happened and why it happened, perhaps, but not what you need to do to improve your performance. That is what we are doing now with the help of artificial intelligence (AI). For example, we analyse data, see if patterns are different or you have anomalies in your data to predict what is happening or what is going wrong. And then we also use AI to analyse our data to see how you are performing, for instance, against competition. And then give customers suggestions on how to improve on certain topics like fuel consumption or driver safety,” he said.
The industry, in Webfleet’s view, is therefore evolving from raw data collection towards insights, recommendations and concrete actions.
SHARED PRESSURES ACROSS DIVERSE FLEETS
Webfleet serves a wide spectrum of customers, from large transport and logistics operators to small fleets of one or two vehicles, service-and-maintenance businesses and last-mile delivery companies.
Each customer faces distinct operational issues, yet common themes emerge. “What they all have in common is that the amount of data and the pressure to enhance their performance is increasing a lot. And then there is the regulatory compliance pressures as well,” said Notenboom.
Performance, in this context, covers delivery times, cost per kilometre, driver wages, safety and fuel consumption – metrics that matter differently according to the sector, but all that demand continuous improvement.
One of Europe’s most persistent difficulties is the shortage of skilled drivers, which has led to greater reliance on migrant workers whose experience of road conditions may vary widely between countries.
Webfleet addresses part of this challenge through tools such as OptiDrive, which shows fleet managers how individual drivers perform on fuel use and safety. Language barriers are tackled with automatic translation features built into the driver’s work app or tablet.
“They can interact with their fleet manager in their own language, and the fleet manager can also interact back in their own language,” explained Notenboom. The same interface delivers active coaching: if a driver exceeds the speed limit, for example, an immediate warning appears. These software-based interventions help maintain standards without requiring constant direct supervision.
MEASURABLE GAINS AND EV TRANSITION
Notenboom agrees that customers understandably scrutinise the return on any additional technology cost. He reported that Webfleet users typically achieve efficiency improvements of up to 15 percent, though results depend heavily on the starting point. This ranges from fuel savings, faster turnaround, downtime reduction or improved driver behaviour, among others.
“If a company is already really good at saving fuel, then adding tools and driver coaching and technology might not change a lot. At the same time, even if it’s a small improvement, especially with the high fuel prices today, it could already translate to a lot of savings,” averred Notenboom.
The arrival of electric trucks introduces a fresh set of complexities. Research indicates that driver behaviour exerts an even greater influence on energy consumption in electric vehicles than in conventional combustion models. Smooth operation becomes critical to range, while decisions about when and where to charge add further layers of planning. Webfleet supports the transition by helping managers determine the right vehicle for each duty cycle.
“If you do long-distance transport, electric trucks are perhaps not the best option. But if you do inner-city deliveries, then electric trucks become an interesting option. And trying to find out where the optimum is, when to use Internal Combustion Engine-vehicles, where to use electric vehicles, that is also a part where we can help the fleet manager to make that decision,” he said.
On the technology package itself, every Webfleet customer receives the software platform. Hardware can be selected according to need, or in some cases, dispensed with entirely through the OEM.connect service (access vehicle data directly from OEMs via APIs), without installing extra hardware that draws data directly from the vehicle manufacturer.
“A number of customers are preferring to use OEM.connect. So that is a solution where we don’t install hardware but take the data directly from the OEM offerings,” he explained. On the other hand, where original-equipment data fall short, Webfleet’s own devices remain available.
PRIVACY, BENCHMARKING AND THE ROAD AHEAD
Growing data volumes inevitably raise questions of privacy and regulatory compliance. Webfleet adheres strictly to General Data Protection Regulation (GDPR) – a strict European Union (EU) law that protects information privacy and data rights for individuals in the EU and the European Economic Area (EEA) – requirements.
Certain categories of information can be processed only with explicit customer permission, and for benchmarking purposes, the company anonymises data so that individual vehicles or fleets cannot be identified.
A recent example is Webfleet’s Commercial Trip Monitor, which aggregates anonymised information across the entire customer base to generate comparative insights.
Looking three to five years ahead, Notenboom identified three principal challenges for the commercial-vehicle industry: the practical difficulties of electrification, the continuing shortage of drivers (with autonomous vehicles potentially addressing certain use cases over a longer horizon) and relentless competitive pressure to deliver higher quality service at lower cost.
He regards these same pressures as sources of opportunity for those able to convert them into advantage.
Interestingly, he shared that Webfleet itself continues to evaluate new markets beyond its established presence in Europe, South Africa, South America and Australia. Bridgestone’s ownership of the US-focused Azuga platform complements the portfolio, while Asia-Pacific, including India, remains under active review even if no immediate plans have been confirmed.
As Notenboom puts it, the goal is not to simply collect more information but to translate that information into clearer decisions that keep vehicles productive, drivers safer and costs under control – regardless of whether the powertrain is diesel or electric.
Vaculug Rolls Out VMS Pro Max Next-Gen Fleet Management App
- By TT News
- October 20, 2026
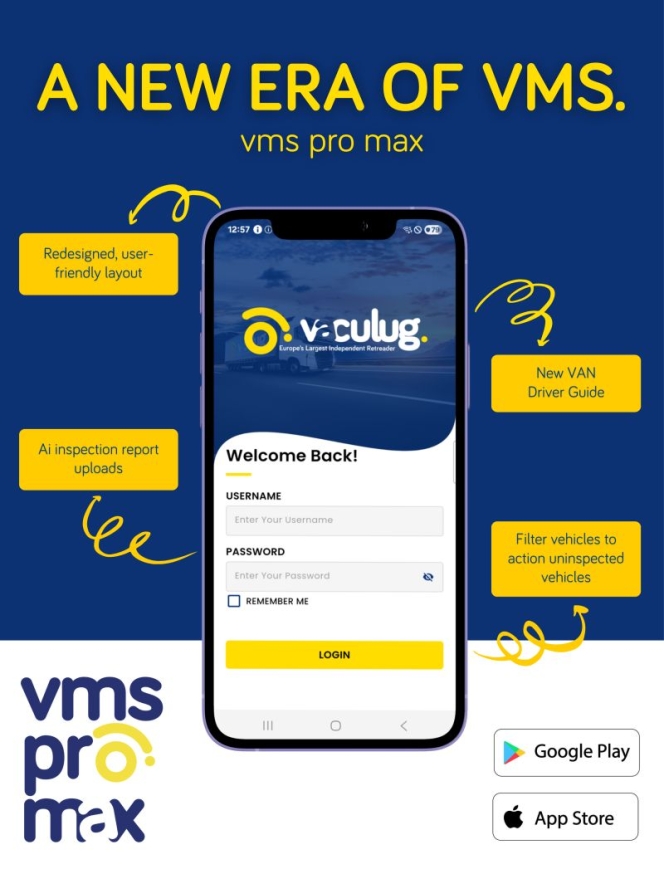
Vaculug has released VMS Pro Max, the next generation of its fleet management application. The product, developed over a three-year period, pairs a redesigned interface with AI-enhanced software intended to make commercial fleet management faster and more intelligent. The app is now available for download through the Apple App Store and Google Play Store.
The upgraded platform offers clear, real-time access to tyre and vehicle data, accelerates background report uploads to reduce driver time and allows measuring tools to be connected for automatic tread depth capture. It also incorporates an embedded VAN Driver Guide and can instantly flag vehicles left uninspected across 30, 60 or 90 days. Existing users must sync all pending inspections and confirm cloud upload before updating to prevent data loss.
Yokohama Rubber, dotData Partner On Human-In-The-Loop AI Agent For Manufacturing R&D
- By TT News
- October 15, 2026
The Yokohama Rubber Co., Ltd. and dotData, Inc. have announced joint development an AI agent to help engineers form hypotheses, interpret findings and make decisions in manufacturing R&D. Before full deployment, the initiative will validate the agent's required capabilities and technical feasibility.
The solution combines technical documents such as design specifications and experimental reports with engineers' accumulated expertise and features extracted from measurement data via dotData's Signal Intelligence technology. It will provide insights tailored to each project's objectives, circumstances and constraints.
The agent is not meant to produce a single correct answer. Operating in a human-in-the-loop framework where engineers retain decision-making authority, it will present multiple possibilities, perspectives and risks to broaden thinking and support professional development.
Manufacturing R&D generates diverse data through experiments, simulations, production and evaluation. Developing hypotheses requires specialised knowledge and context. Since new technology R&D rarely has one predetermined answer, abductive reasoning plays a key role. AI can add value by using data and organisational knowledge to widen engineers' perspectives rather than replace judgment.
The agent will explore measurement and experimental data patterns beyond factors engineers previously identified, combining quantitative insights with design documents and expert knowledge to reveal difficult-to-spot relationships. It will offer input from materials, design, analysis, production and evaluation perspectives, challenge existing hypotheses and raise questions about alternative interpretations and conditions. Engineers will then test hypotheses and feed results back into further dialogue, guiding Signal Intelligence processes so non-specialists can explore data features as needed.
Yokohama Rubber has advanced HAICoLab since 2020, using dotData as a foundational technology in tyre design and rubber mixing. This joint development expands those efforts, with engineers interpreting and evaluating the agent's suggestions using their own expertise rather than accepting them unquestioningly. The companies aim to transform R&D processes while strengthening engineers' creativity and judgment, establishing a new model for human-AI collaboration in manufacturing R&D.
Motoji Fujita, Head of Research & Advanced Development Division, The Yokohama Rubber Co., Ltd., said, “Since 2020, we have conducted research and development under the HAICoLab framework, drawing on the complementary strengths of people and AI to create a collaborative environment. We believe AI agents will give engineers access to perspectives beyond their own experience and enable them to evaluate hypotheses from multiple angles. Through this development initiative, we aim to advance our R&D capabilities while supporting the continued growth of our engineers.”
Ryohei Fujimaki, CEO, dotData, Inc., said, “Success in manufacturing R&D depends heavily on an organisation’s ability to connect its proprietary data and knowledge with AI. The quantitative context generated from data through automated Signal Intelligence provides a foundation for AI agents to engage engineers in practical, data-driven discussions. Together with Yokohama Rubber, which has many years of experience in advanced data utilisation, we intend to establish standards for using AI in highly specialised business domains.”
Bridgestone Deploys Easytrack At SR Technics Spain MRO Hub
- By TT News
- October 10, 2026
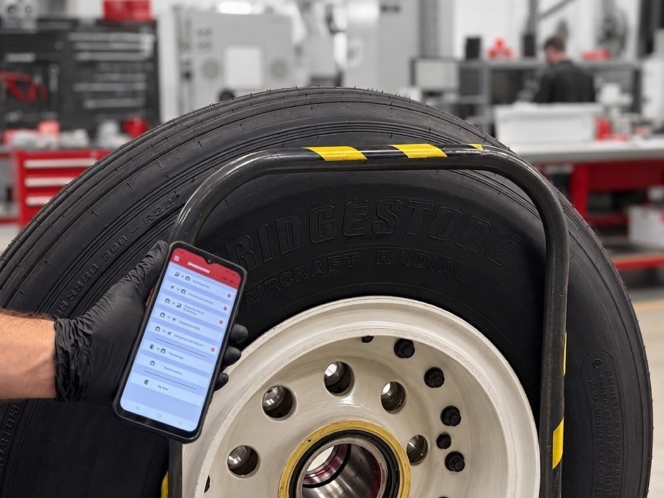
Bridgestone Aircraft Tire (Europe), a Bridgestone Corporation subsidiary, has announced the deployment of its ‘easytrack’ tyre management system at SR Technics Spain SAU, the tyre and wheel maintenance hub of global maintenance, repair & overhaul (MRO) provider SR Technics. The scalable digital platform is accessible on desktop and mobile devices.
Designed for airlines and MROs, ‘easytrack’ manages inbound and outbound tyre and wheel flows across single- or multi-site operations. It delivers real-time identification, tracking and documentation throughout each asset’s lifecycle. The project follows the solution’s first airline implementation in 2025, becoming its second customer rollout and first MRO application.
MRO providers handle large tyre and wheel volumes for multiple airlines, complicating operations. ‘easytrack’ simplifies asset management and improves traceability, accuracy, safety and productivity. At SR Technics Spain SAU, it digitalised paper-based processes, cutting processing time by 45 percent, reducing data-entry and identification errors and improving flow management across Palma de Mallorca and Madrid.
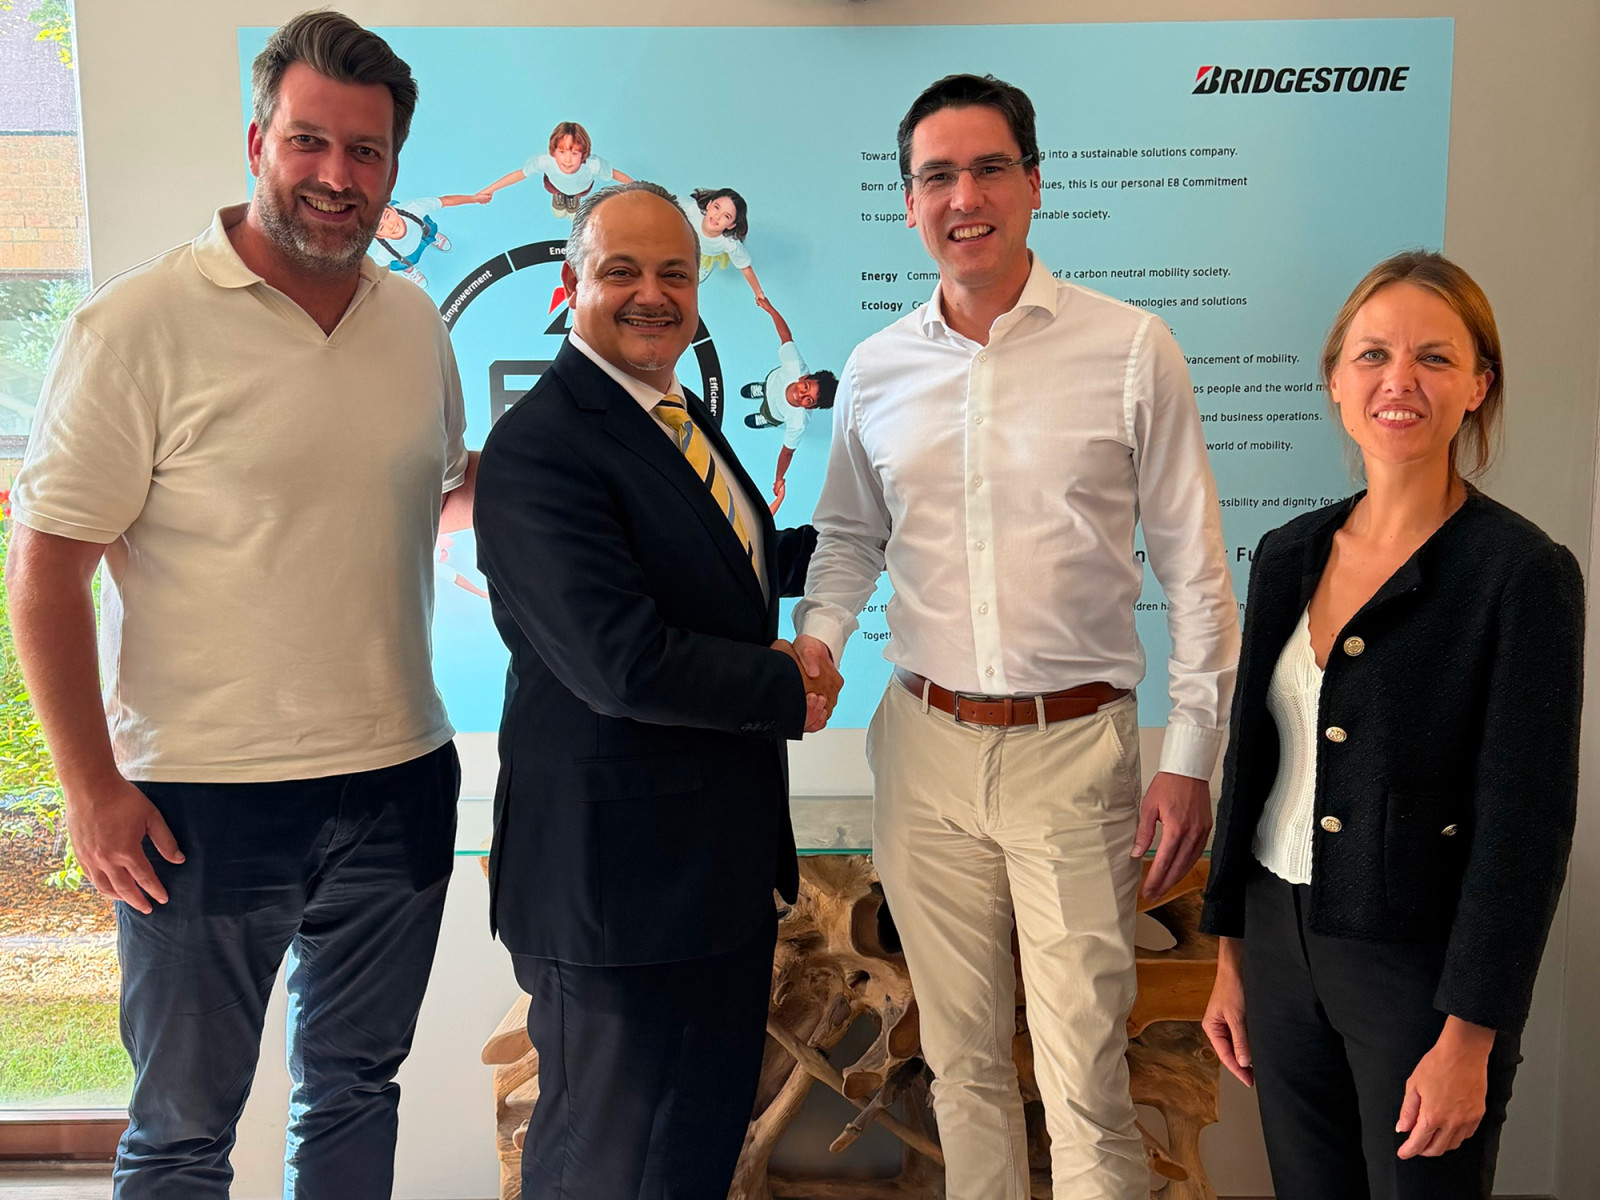
From left: David Sautois, ‘easytrack’ Product Manager, Bridgestone Aircraft Tire (Europe) S.A.; Antonio Colella, General Manager, SR Technics Spain SAU; Jean-Philippe Minet, Managing Director, Bridgestone Aircraft Tire (Europe) S.A.; Eugenie Baradzina, Commercial Director, SR Technics Spain SAU.
The results stem from a Bridgestone and SR Technics Spain SAU co-creation initiative built on long-standing partnership. ‘easytrack’ was adapted to support tyre and wheel combinations for the hub’s wheel and brake operations. Bridgestone’s expansion of airline and MRO solutions aligns with its E8 Commitment, emphasising efficiency and ecology.
Antonio Colella, General Manager, SR Technics Spain SAU, said, "The successful implementation of easytrack is a significant achievement for SR Technics Spain SAU and our teams in Mallorca and Madrid. From the very beginning, the collaboration with Bridgestone was built on trust, openness and a shared vision for innovation. Together, we have developed a solution that not only improves efficiency and traceability but also creates lasting value for our operations. We are proud to be the first MRO in the world to adopt this technology and look forward to continuing this journey with Bridgestone Corporation.”
Jean-Philippe Minet, Managing Director, Bridgestone Aircraft Tire Europe, said, “I’d like to thank SR Technics for their trust and another fruitful collaboration with Bridgestone. What the teams have jointly achieved is remarkable: co-creating through efficient teamwork and customising the Bridgestone easytrack application to digitise SR Technics tyre and wheel tracking operations. This is a brilliant example of how Bridgestone amplifies the value created at our partners.”
Comments (0)
ADD COMMENT