- Tyre Materials Conference 2025
- Tom Thomas
- Eonix Management Solutions
- Srikanth Chakravarthy
- HF Group
- Anil Nair
- Hasteri
- Dr Saikat Das Gupta
A Spectacle Of Excellence And Innovation Dazzles TMC 2025
- By Gaurav Nandi
- September 02, 2025
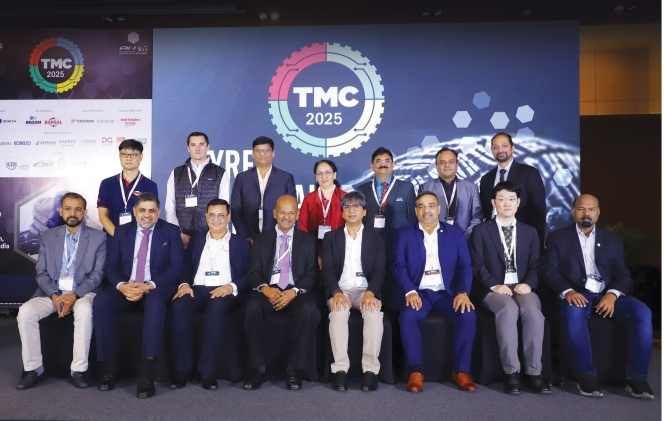
The Tyre Materials Conference 2025 unfolded as a high-octane showcase of innovation, urgency and collaboration amid the industry’s accelerating shift towards sustainability. With participation from global leaders, researchers and policymakers, the event addressed the fundamental transformation of tyre materials, from raw rubber to recycled steel and from EV-ready compounds to AI-powered sorting systems. Yet, beneath the applause and optimism lay sobering truths like systemic supply chain disruptions, regulatory uncertainty and the technological gap in scalable green alternatives. India’s growing ambition, collaborative initiatives and research strength emerged as hopeful beacons in a sector still grappling with fragmented standards and circularity bottlenecks.
A banquet hall in a posh New-Delhi hotel turned into an intellectual crucible to host a spectacle that drew in participants from different corners of the world for defining the future of the global tyre material industry.
As the emcee announced the commencement of the Tyre Materials Conference 2025 (TMC 2025), organised by Tyre Trends, applause rippled through the room, momentarily shaking the circular tables and rows of chairs that seated over 100 participants, each with eager eyes, ready to unwrap the future.
The hall gradually turned into a melting pot of ideas, innovation and future trends as the day unfolded. The spirit of excellence and innovation reverberated through the entire establishment with such grandeur that even outsiders wanted a peek inside.
Following the inaugural lamp lighting by Conference Chairman Tom Thomas and others, the stage was now set for insightful speeches and interactive sessions that encompassed everything from development of sustainable materials for the tyre industry to a panel discussion discussing the trends within the tyre materials sector.
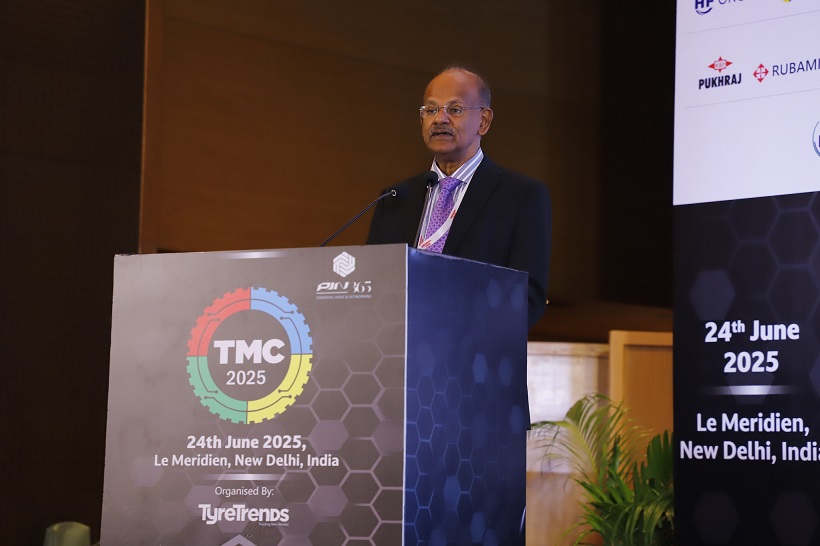 “The theme of this year’s conference that hinges upon raw material of tyres for future mobility could not be timelier. This conversation comes at a pivotal moment for our industry as we face a new generation of challenges and opportunities. There is a growing and urgent push for sustainability across the value chain. As an industry, we must reduce our dependence on petroleum-based raw materials, which currently make up nearly 55–60 percent of the material mix used by tyre manufacturers,” said Thomas in his inaugural address.
“Today, we are writing the next chapter of tyre material science – one that achieves sustainability without sacrificing performance, embraces innovation without compromising reliability and drives technological advancement while protecting our environment,” he added.
Highlighting the importance of collective collaboration in driving the industry forward during a special address, Eonix Management Solutions Managing Director Srikanth Chakravarthy said, “The future should be something we don’t fear and something that excites us. With Zenith Group, we’re not just talking about another supplier but about the world’s largest steel cord maker in the making, backed by USD 2 billion in investment, a USD 30 billion parent and the industry’s most advanced solar-powered, automated plant.
It’s the only company tracking carbon emissions in real time and targeting 100 percent recycled steel by 2027. As India’s steel cord demand doubles, Zenith plans to support with imports, warehousing and eventually local manufacturing. Collaboration across suppliers, competitors and customers is essential to create lasting value for our industry.”
Speaking at the conference, HF Group Business Development Director Anil Nair delivered a sharp, data-driven keynote outlining the structural and technological turbulence reshaping the global tyre industry. From volatile raw material costs to rising demands for electric vehicle-ready compounds, he painted a picture of an industry at a critical inflection point.
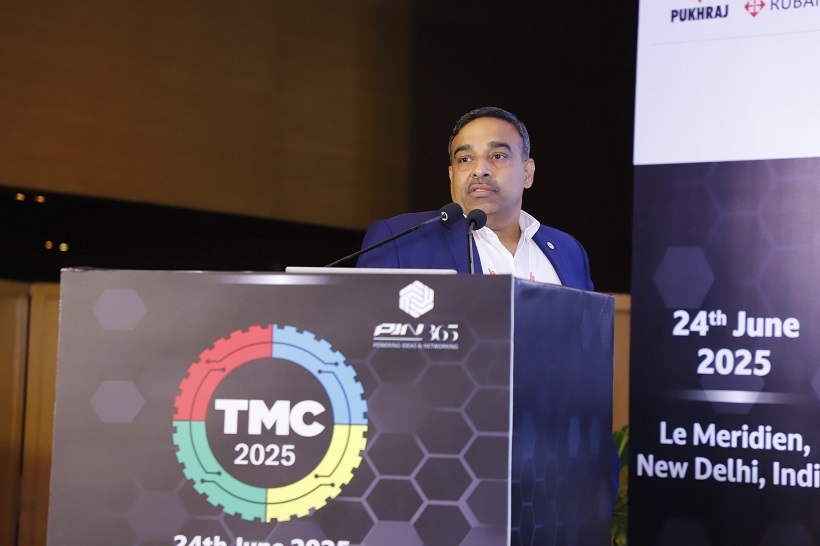 “Challenges are mounting across regions. Europe leads in sustainability regulation with the push for digital tyre passports, while US buyers remain cost-focused. In Asia, Japan and Korea prioritise performance even as China leans into price efficiency. Globally, manufacturers are grappling with premature crosslinking, high-silica formulations that undermine shelf life and erratic compound quality, especially when integrating bio-oils and recovered carbon black,” Nair explained.
He noted that artificial intelligence emerges as a vital tool amid production shifts as tyre majors relocate factories to cheaper regions, triggering expertise gaps and costly closures. Nair emphasised that artificial intelligence can bridge generational knowledge loss by codifying best practices from veteran staff.
On the innovation front, he spotlighted smart tyres with real-time monitoring capabilities and self-adjusting pressure systems. He also stressed recyclability by design with tyres engineered for chemical disassembly and multi-cycle retreading. For EVs, the shift is clear, which includes quieter, lighter and longer-lasting tyres built around high-silica and nano-enhanced fillers.
Nair concluded with a call to rethink longevity, promoting materials that resist ageing, disperse uniformly and maintain performance across diverse geographies.
“This isn’t just evolution – it’s re-engineering the tyre from the molecule up,” Nair declared.
EMERGING MATERIALS
The tyre industry is embracing a sustainability revolution driven by regulation, innovation and performance demands. From circular economy models and advanced bead wire solutions to breakthrough chemical additives and EV-optimised rubber compounds, manufacturers are reshaping production to deliver high-efficiency, eco-conscious tyres fit for the future of mobility.
Speaking at the conference on sustainable materials, Hasteri Chief Scientist explained, “The global tyre industry is undergoing a profound transformation driven by increasingly stringent regulations and a commitment to sustainability. No longer a mere buzzword, sustainability is now central to manufacturing, encompassing economic, social and environmental considerations.”
 “This shift is seeing a move from a linear ‘use and throw’ model to a circular economy with significant investment in bio-based materials, advanced recycling of end-of-life tyres and decarbonisation efforts across the supply chain. New regulations including extended producer responsibility and limits on tyre wear particles are accelerating this change. With the market for sustainable tyre materials projected to see over 26 percent growth by 2029, the sector is embracing innovation, from bio-sourced rubbers and recycled steel to energy-efficient production, aiming for a future where tyres are both high-performing and environmentally responsible,” he added.
Drawing from nine real-world defect cases, Sun Hong Kim, Technical Head of Tyre Bead Wire Division at Bansal Wire Industries, outlined how bead wire stiffness and mechanical behaviour critically affect tyre beading performance.
He noted that stiffness, regulated by the take-off machine’s killing roller, determines how the wire responds under load. “Low stiffness wires deform more easily, while high stiffness variants resist structural failure. Defects such as wire lift-up, bending, tilting and S-type straightness are linked to mismatched stiffness, over- or under-killing, reduced yield points and inconsistent brake tension during payoff,” explained Kim.
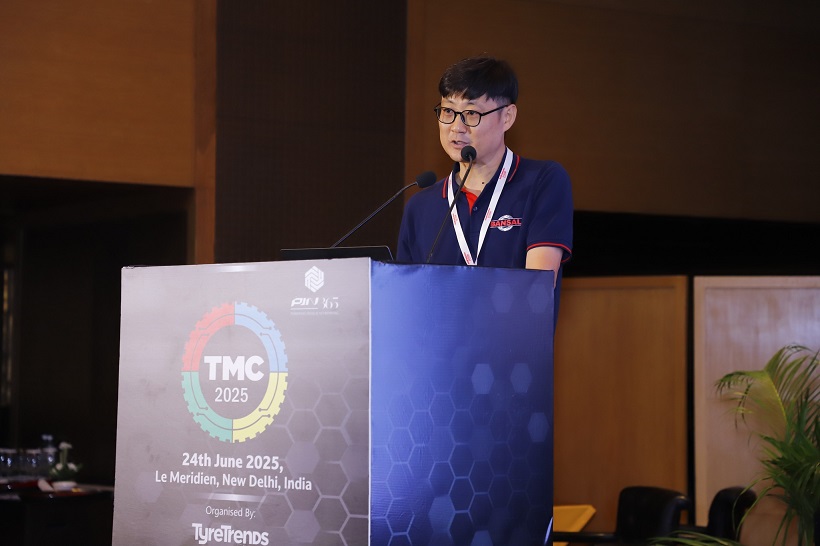 Furthermore, Kim pointed out that one recurring issue, namely fluctuating brake pressure, was resolved by installing an air regulator, highlighting the role of stable mechanical inputs.
He also categorised defects into four types (A–D), each requiring specific interventions ranging from stiffness adjustment to wire straightening control. As tyre manufacturers demand higher consistency, his data-led approach offers a template for addressing bead wire variability across global production environments.
Leading chemical firm Schill + Seilacher “Struktol” is pioneering significant advancements in tyre manufacturing through its innovative additive, BP 19797, designed to enhance both production efficiency and product performance.
Speaking remotely at the conference, the company’s Senior Technical Sales Manager, Robert Kobel-Bryk, detailed how this new process promoter drastically improves silica dispersion in rubber compounds, enabling faster mixing cycles and a notable reduction in energy consumption during the manufacturing process. This translates directly into more efficient operations and a smaller carbon footprint.
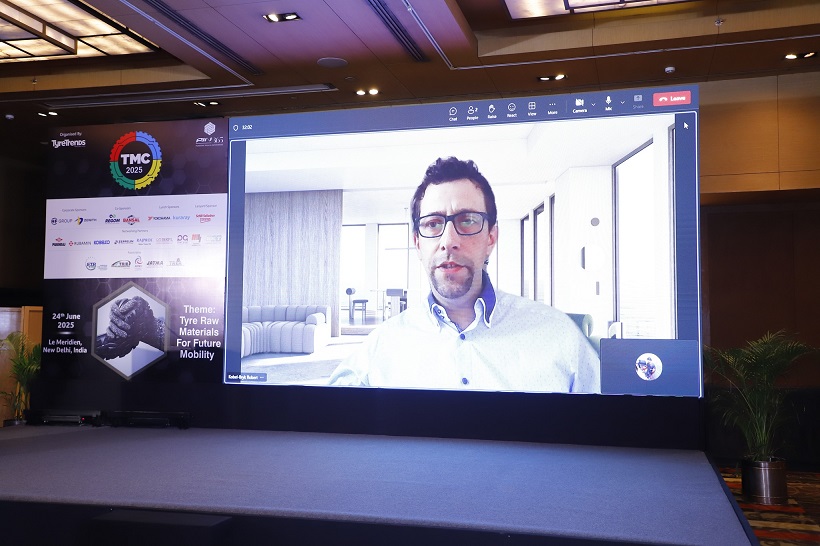 “BP 19797 yields superior extrusion properties and smoother surfaces for tyre components, leading to lower scrap rates. The introduction of this additive maintains or even minimally enhances the final physical properties of the tyre including tensile strength while concurrently improving the complex balance between wet grip and rolling resistance,” said Kobel-Bryk.
The company emphasises these developments as key to addressing industry demands for cleaner, safer and more efficient production methods.
Japanese speciality chemical firm Kuraray’s Technical Service Engineer at Elastomer Division, Naoto Takahashi, highlighted the company’s nearly 100-year history and detailed how its unique low-molecular-weight rubber acts as a reactive plasticiser, preventing bleed-out by co-vulcanising with base rubber.
“GS-L-BR significantly enhances crucial EV tyre properties including high wear resistance for heavy, high-torque vehicles and low rolling resistance for extended range and energy efficiency. Our novel approach for tyre treads involves increasing natural rubber content, a combination traditionally challenged by filler interaction. GS-L-BR overcomes this by improving the bond between natural rubber and silica, outperforming conventional formulations in wear and rolling resistance while also boosting wet grip,” contended Takahashi.
He added, “For sidewalls, replacing carbon black with silica becomes viable as GS-L-BR dramatically improves fatigue resistance. This groundbreaking material promises to be a key component for the next generation of EV and even commercial vehicle tyres, addressing critical performance and sustainability needs.”
GOING GREEN
The tyre industry is undergoing a technological shift for going green with innovations in recycling, advanced materials and processing systems. From AI-driven sorting of end-of-life tyres to self-healing elastomers and high-silica mixing technologies, these breakthroughs are driving greater efficiency, sustainability and performance across the entire value chain.
Speaking at the conference, Senior Manager of Process Technology (Asian Countries and Global) at HF Group, Dr M N Aji, emphasised the critical role of combining machinery and processing expertise for optimal silica mixing, especially as silica usage in tyre technology is rapidly increasing with some applications reaching up to 160 parts-per-hundred-rubber (PHR).
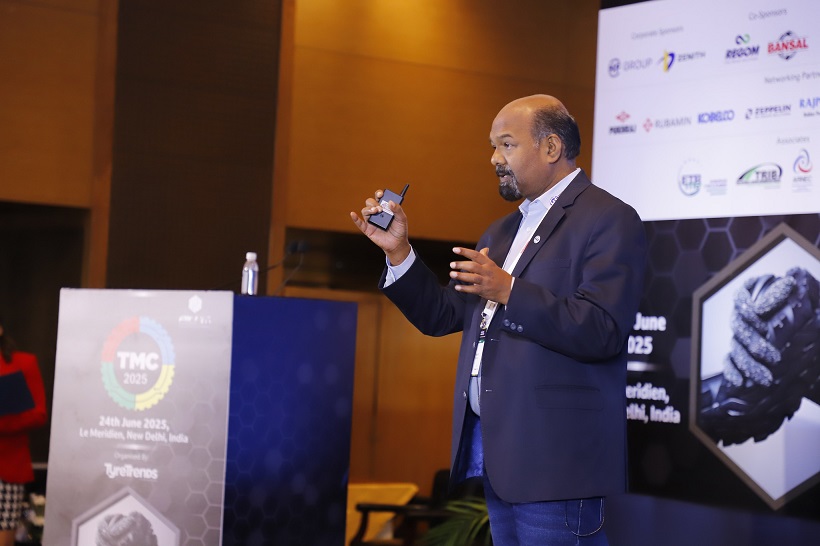 “Incorporating high levels of silica with specialised polymers is crucial to achieve superior properties like better mileage, lower noise levels and improved traction. HF Group’s innovative mixer technologies including tangential (Z4 rotor) and intermeshing (PS7/PS5 rotor) designs offer enhanced shear, cooling efficiency and intake. The Z4 rotor’s versatility for both silica and final batch mixing is noted along with the development of new wear-resistant materials (HFSI 50) and intelligent ram technology (i-EXL) for energy and cost savings,” averred Aji.
He added that key to successful silica mixing were precise temperature control, viscosity reduction and excellent dispersion. The importance of maintaining optimal water quality for cooling and adhering to strict acid cleaning schedules for mixer maintenance is imperative.
“Tandem mixing technology was introduced as a cutting-edge solution for high-fill silica masterbatches, offering 100 percent productivity and superior temperature control by separating dispersion and distribution processes. HF Group’s TRC co-axial rotor technology was specifically designed for ultra-high silica content, ensuring better material cohesion and quality,” noted Aji.
Dr Shib Shankar Banerjee, Assistant Professor from IIT Delhi’s Department of Material Science and Engineering, presented cutting-edge research in polymer and elastomer materials, focusing on ‘new generation elastomeric materials’ that transcend conventional rubber properties. These materials aim for enhanced performance, functionality and processability, incorporating features like shape memory, self-healing, conductivity and magnetic properties.
One key area of research involved thermoplastic elastomers with improved phase compatibility and self-healing capabilities, particularly leveraging shape memory assistance to repair micro-cracks.
Dr Banerjee noted that his team is also exploring 3D printing of rubber-like materials for complex geometries and developing soft and multi-functional materials using liquid metals (Gallium and eutectic Gallium-Indium alloy) to create conductive, magnetic, yet soft elastomers for flexible and stretchable electronics.
A significant portion of his presentation was dedicated to the development of hydrogenated SBR (HSBR) based vulcanisates with superior traction performance, a collaborative effort with Hasetri. HSBR exhibits a more homogeneous network structure, leading to better ageing resistance, higher modulus at elongation, improved wet and dry traction, better rolling resistance and enhanced abrasion and fatigue properties compared to conventional SBR.
His research also explored the synergistic effect of hybrid fillers like CNT in HSBR, noting improved filler dispersion due to higher viscosity and styrene content.
Innovating tyre recycling with smart sorting technology, France-based Regom’s Chief Executive Officer, Arthur Wagner, introduced his company’s innovative approach to maximising the value of end-of-life tyres through advanced sorting. Recognising the challenges of manual sorting and the lack of data in the used tyre industry, Wagner stated, “Our core innovation is a machine that processes tyres individually, capturing images and using artificial intelligence to analyse brand, model, dimensions, load and speed indices and DOT codes in less than a second. This system, refined over six years with a vast database from processing over 20 million tyres annually, can operate efficiently even with wet or muddy tyres.”
He went on to say that the system allows customers to configure custom rejection criteria, automatically diverting tyres with no value to shredding and streamlining manual grading for valuable tyres. This automation significantly increases resale prices, optimises retreading and enhances material recovery, while also reducing labour pain points and costs.
A key application of Regom’s technology is in pyrolysis, where precise sorting of tyres helps maximise the quality of the output. The company is also at the forefront of integrating RFID technology into tyre sorting.
MARKET ECONOMICS
Natural rubber remains vital to the global tyre industry, yet its supply chain faces mounting pressures from climate change, labour shortages, regulatory shifts and price volatility. As demand grows, industry stakeholders are exploring innovation, sustainability and traceability to secure long-term supply and meet ambitious environmental goals.
Explaining the volatile raw material landscape, Yokohama Off Highway Tires Chief Sustainability Officer Padmakumar G said, “Change is the predominant challenge in the tyre industry’s raw material supply chain. Current volatility stems from several factors, which include the EU Deforestation Regulation causing natural rubber price and availability issues, Indian import restrictions impacting steel and unpredictable crude oil prices affecting petrochemical-derived materials like carbon black and synthetic rubber.”
“Global shipping faces constant disruptions from Suez Canal blockages to geo-political conflicts forcing longer, costlier routes. Even evolving trade policies such as new US-Mexico green corridors demand continuous vigilance. Looking ahead, the industry’s ambitious 2050 sustainability goals present formidable challenges. Shifting to 100 percent sustainable raw materials necessitates developing bio-based alternatives for carbon black, synthetic rubber, and fabrics, which is a significant hurdle given current technological limitations and lack of mass production,” he added.
He asserted that India’s ingenuity will be crucial in overcoming these profound material and supply chain transformations, ensuring the industry’s future viability amidst relentless change.
Alluding to the global natural rubber landscape ANRPC Senior Economist Dr Lekshmi Nair said, “Natural rubber (NR) is a crucial strategic raw material with use in diverse applications beyond tyres, though the tyre industry accounts for 70 percent of its global consumption. A significant challenge stems from the fact that approximately 90 percent of global NR production originates from small growers in tropical regions. These farmers face issues such as low productivity, limited access to resources, volatile prices and the changing demographics as younger generations are less interested in labour-intensive rubber tapping. The lengthy 30-year lifecycle of rubber trees including a six-year immaturity period also deters investment and quick innovation adoption.”
She noted that globally, Thailand, Indonesia and Ivory Coast are the largest NR producers, contributing around 65 percent of the world’s supply, with Vietnam emerging as the fourth. Historically, Asian producers accounted for 91-92 percent of global production, but this has decreased to 79 percent, while West Africa, particularly Ivory Coast, has seen its share rise to 21 percent.
Consumption patterns have also shifted with 67 percent of NR usage now in Asian countries like China, India and Thailand. Despite a projected deficit of 0.7 million tonnes (demand of 15.5 million tonnes versus supply of 14.8 million tonnes), price volatility is often driven by speculative factors rather than market fundamentals, partly due to low investment in replanting.
A key regulatory challenge is the EU Deforestation Regulation, which came into force in June 2023. Compliance for large and medium-sized operators is required by 31 December 2025 and for micro and small enterprises by 30 June 2026. This regulation demands full traceability to prove that NR and products containing it are not sourced from land deforested or degraded after 31 December 2020. While NR is inherently sustainable, this regulation complicates supply chains, especially for producers exporting to Europe, which accounts for 12 percent of total NR consumption in its final products.
“Initiatives like the Global Platform for Sustainable Natural Rubber are working on common guidelines, traceability programmes and capacity building to help the entire value chain, including smallholders, adapt to these new demands. Collaboration and policy support are will be essential for successful implementation of these sustainable transitions and for navigating price volatility, climate change impacts and evolving trade policies,” contended Nair.
THE PANEL
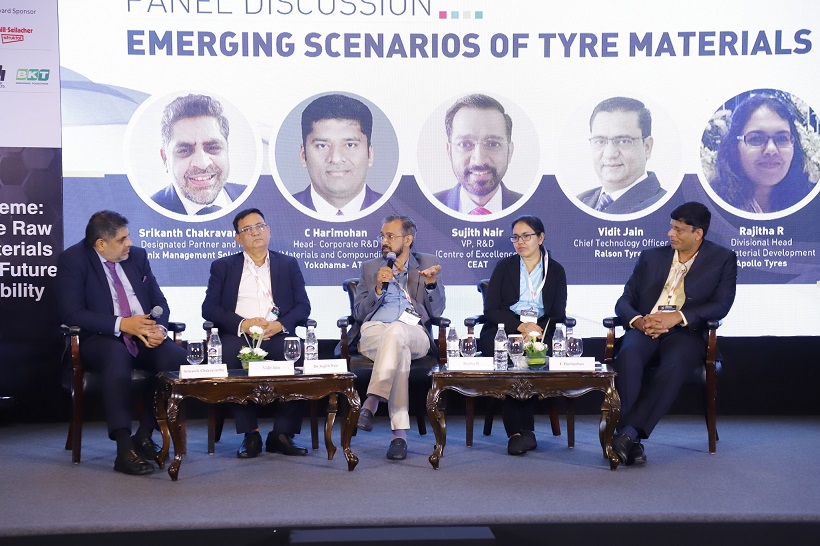
The panel discussion on ‘Emerging Scenarios of Tyre Materials’ brought together leading minds from India’s tyre industry to dissect the monumental shift towards sustainability. It featured CEAT Vice President of Research and Development (Centre of Excellence), Sujith Nair; Yokohama-ATG Head – Corporate Research and Development (Materials and Compounding), C Harimohan; Apollo Tyres’ Divisional Head Raw Material Development, Rajitha R and Ralson Tyres Chief Technology Officer Vidit Jain. The panel was moderated by Eonix Management Solutions Managing Director Srikanth Chakravarthy.
Chakravarthy opened the session by highlighting the immense scale of the transformation ahead. Citing projections of a five to six-fold growth in tyre production and a shift from 35 percent to 100 percent sustainable materials within 25 years, he posed the fundamental question: How is the Indian tyre industry preparing for this paradigm shift, particularly concerning the move away from petroleum-based materials like synthetic rubber and carbon black?
Nair outlined the industry’s approach in three key phases, namely sustainable and green materials with a focus on environmentally friendly and SoC-free options; reduce, recycle and reuse, aiming to lessen tyre weight, reduce carbon dioxide emissions and minimise material wear, encompassing practices like retreading and renewal and sustainable sourcing, exploring new and responsible ways to procure raw materials.
Nair underscored the excitement around green materials, particularly natural alternatives, despite inherent challenges in development and application and highlighted the push for recycled materials with a focus on enhancing the strength of high-tensile materials for use in compounds. The scaling up of new materials, maintaining quality and navigating diverse specifications and certifications across factories present significant hurdles.
Harimohan reinforced Nair’s points, stressing the importance of a holistic understanding of sustainability. He narrowed the focus to the six material types that constitute 85-88 percent of total raw material consumption in tyre manufacturing, namely natural rubber, synthetic rubber, carbon black, steel cord, textiles and rubber process oil.
While natural rubber is largely considered a sustainable material, Harimohan identified synthetic rubber and carbon black as the two areas requiring breakthroughs. He noted that bio-sourced butadiene (for synthetic rubber) is technologically proven with pilot plants in operation and collaborations underway such as Michelin’s European partnerships and Yokohama’s collaboration with a Japanese synthetic rubber company.
The challenge, however, lies in the circularity of carbon black. Harimohan explained that recovered carbon black currently acts more as a filler than a direct replacement for virgin carbon black due to significant degradation during pyrolysis.
He advocated for research to improve the properties of recovered carbon black to 80-90 percent of its original capabilities. Similarly, he called for advancements in recycled rubber, which currently retains only 5-6 MPA of tensile strength compared to 20-25 MPA for virgin compounds.
Recognising the shared nature of the sustainability challenge, the discussion turned to the need for greater collaboration within the industry. Nair revealed that the Indian Tyre Technical Advisory Committee (ITTAC) has already initiated a consortium of tyre companies to work with raw material manufacturers on developing common specifications.
Three such projects primarily focused on sustainable IT space, pyrolysis of carbon black and reclaim rubber are underway. Nair emphasised the necessity of expanding these efforts, citing examples like the European tyre industry’s consortiums.
He also called for greater investment in research and development centres across all tyre companies as a foundational step for effective collaboration and advocated for partnerships with academic institutes.
Rajitha introduced a sobering data point, which stated that in the last 50 years, no new major entrant has emerged in the global tyre industry, while some established players have diminished. She highlighted the immense potential of large Indian conglomerates like the Reliance Group, who are already involved in many tyre-related products to drive significant breakthroughs.
 The panel unanimously agreed that achieving sustainability goals requires a holistic approach, encompassing the entire supply chain. Rajitha underlined the importance of selecting suppliers with strong research and development capabilities and a quick adaptability to new technologies, also stressing the need for local partners to meet global standards.
A key challenge raised by the moderator was the often-lengthy tyre approval process, especially when introducing entirely new materials. Rajitha acknowledged that validation processes would need to evolve.
She suggested that validation time could be minimised when new materials maintain similar basic molecular structures and properties and highlighted the increasing use of virtual and physical simulations and advanced ageing testing to expedite validation.
The standardisation of recycled materials like recovered carbon black with established specifications could also significantly streamline the process. Nair added that while striving for 100 percent performance equivalence when replacing virgin materials is ideal, a pragmatic approach might involve accepting 85-90 percent and then compensating through redesign.
Industry leaders from CEAT, Yokohama-ATG, Apollo Tyres, and Ralson Tyres engage in a dynamic panel on ‘Emerging Scenarios of Tyre Materials,’ moderated by Srikanth Chakravarthy.
He introduced a fourth ‘R’, calling it ‘redesign’, as a faster approach to validation. The potential of artificial intelligence and its integration with simulation models to accelerate the decision-making process for new materials was also briefly touched upon with the consensus that this is indeed the way to go.
The panel discussion underscored the Indian tyre industry’s earnest efforts in navigating the complex landscape of sustainable materials. While challenges abound in material science, supply chain collaboration and regulatory alignment, the collective commitment to innovation and a greener future appears strong.
TMC 2025 made clear that the journey to sustainable tyre materials is as complex as it is critical. While innovation is abundant, real progress hinges on global cooperation, scalable technology and faster validation systems. The path ahead demands collective resolve to redesign not just materials but the very approach to tyre manufacturing.
The next edition will be held in 2027 on a bigger scale!
The Tyre Giant That Doesn’t Want A Dark Factory
- By Sharad Matade
- October 13, 2026
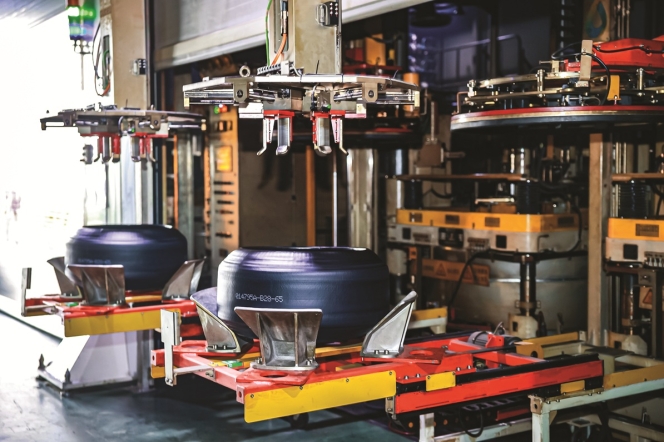
ZC Rubber, China’s largest tyre maker, is running 18 AI agents across its Hangzhou 5G plant. It insists the goal is smarter manufacturing, not emptier factory floors.
Walk into the industrial conversation about automation these days and ‘lights-out’ production tends to come up within minutes: factories with no people, no lighting and machines working in the dark. However, ZC Rubber, the Hangzhou-based group that ranks among the world’s top nine tyre companies, would like to correct that impression before it takes hold.
“We see this as a 5G Smart Factory, or Future Factory V2.0, rather than a ‘dark factory’. The goal is intelligent manufacturing, not simply removing people from the production process,” the company said in an interview.
That is a notable position from a company that has just put 18 AI agents to work across its production chain and reports defect rates well under half those of its earlier operations. It is also a considered one, and the details explain a good deal about how the world’s largest tyre market is approaching the factory of the future.
PEOPLE AT THE EXCEPTIONS
ZC Rubber’s division of labour is simple. Automation, AI and real-time data are steadily taking over what the company calls ‘repetitive and highly standardised operations.’ Its people are being moved towards engineering, process management, quality assurance and the handling of exceptions, meaning the unusual problems that no model has seen before.
“We will continue to increase automation, but fully unmanned production is not the goal,” ZC Rubber said. “It is about combining intelligent systems with human expertise.”
The same logic applies to the future. Asked whether lights-out production is on the roadmap, ZC Rubber was clear. “We do not see fully lights-out production as a goal in itself. Technology will be introduced where it brings clear improvements in quality, efficiency, safety and sustainability,” it said.
EIGHTEEN AGENTS, ONE PRODUCTION CHAIN
The scale of the AI deployment is considerable. Since June 2025, ZC Rubber has introduced 18 AI agents across the full production chain. Their use ranges from AI-assisted formulation and virtual simulation to equipment maintenance, production scheduling and quality control. According to the company, they have helped shorten tyre development cycles by 50 percent and lifted production efficiency by 50 percent.
Where does the value come from? Not from any single stage, the company suggests. “The biggest value comes from using AI to analyse production data, optimise process parameters and support faster decision-making across the manufacturing process,” it said. ZC Rubber does not currently publish a stage-by-stage breakdown of the gains.
INSPECTION AND THE DEFECT RATE
Quality control is where the company’s numbers are most striking. Its latest AI-based visual inspection systems, it says, can achieve a defect detection rate of close to 100 percent, improving both the speed and the consistency of inspection. That matters most in high-volume passenger car radial (PCR) output, where human inspectors face the twin problems of fatigue and sheer throughput.
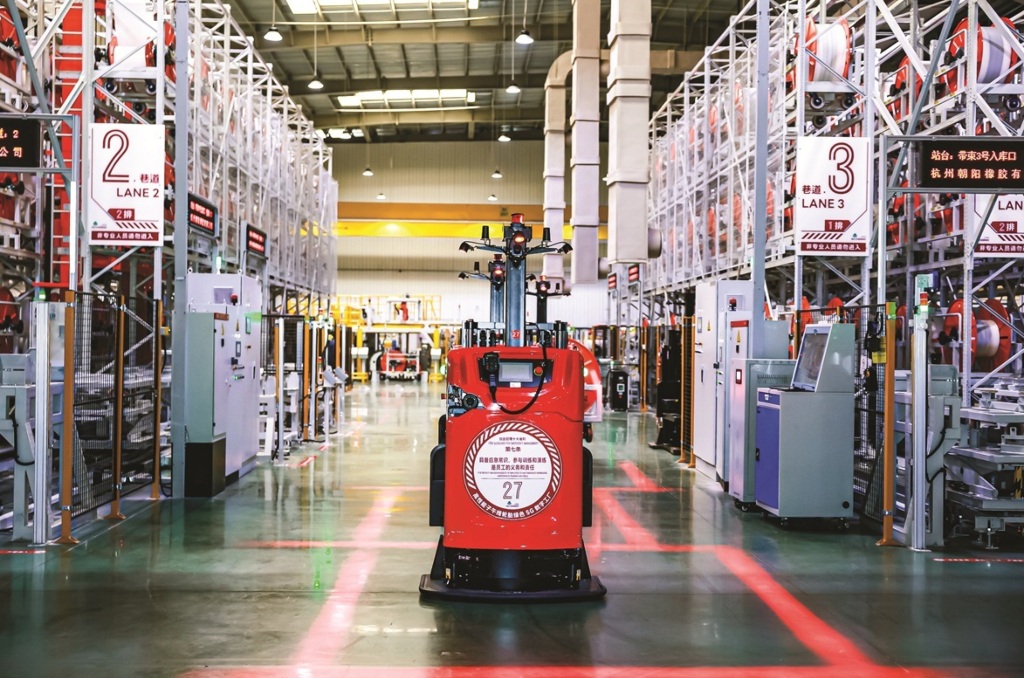 Zooming out, the company says AI and digital quality control across its smart manufacturing system have cut its product defect rate from 1.2 percent to 0.5 percent.
HOW THE SYSTEMS TALK TO EACH OTHER
“Thousands of sensors collect production data in real time, while 5G connects equipment, quality inspection and logistics systems,” the company said. The APS+MES system pulls production, quality and logistics information into one place ‘so operations can be monitored and adjusted quickly’. AI and big data analytics then help staff spot problems and make faster production decisions.
AN EARLIER SET OF NUMBERS, UPDATED
ZC Rubber’s earlier claims of a 15 percent efficiency gain, up to 40 percent lower defect rates and a 5 percent cut in energy use make one notice that the latest figures are considerably better. The company is candid about why. “Those figures reflect an earlier stage of our smart factory development,” it said.
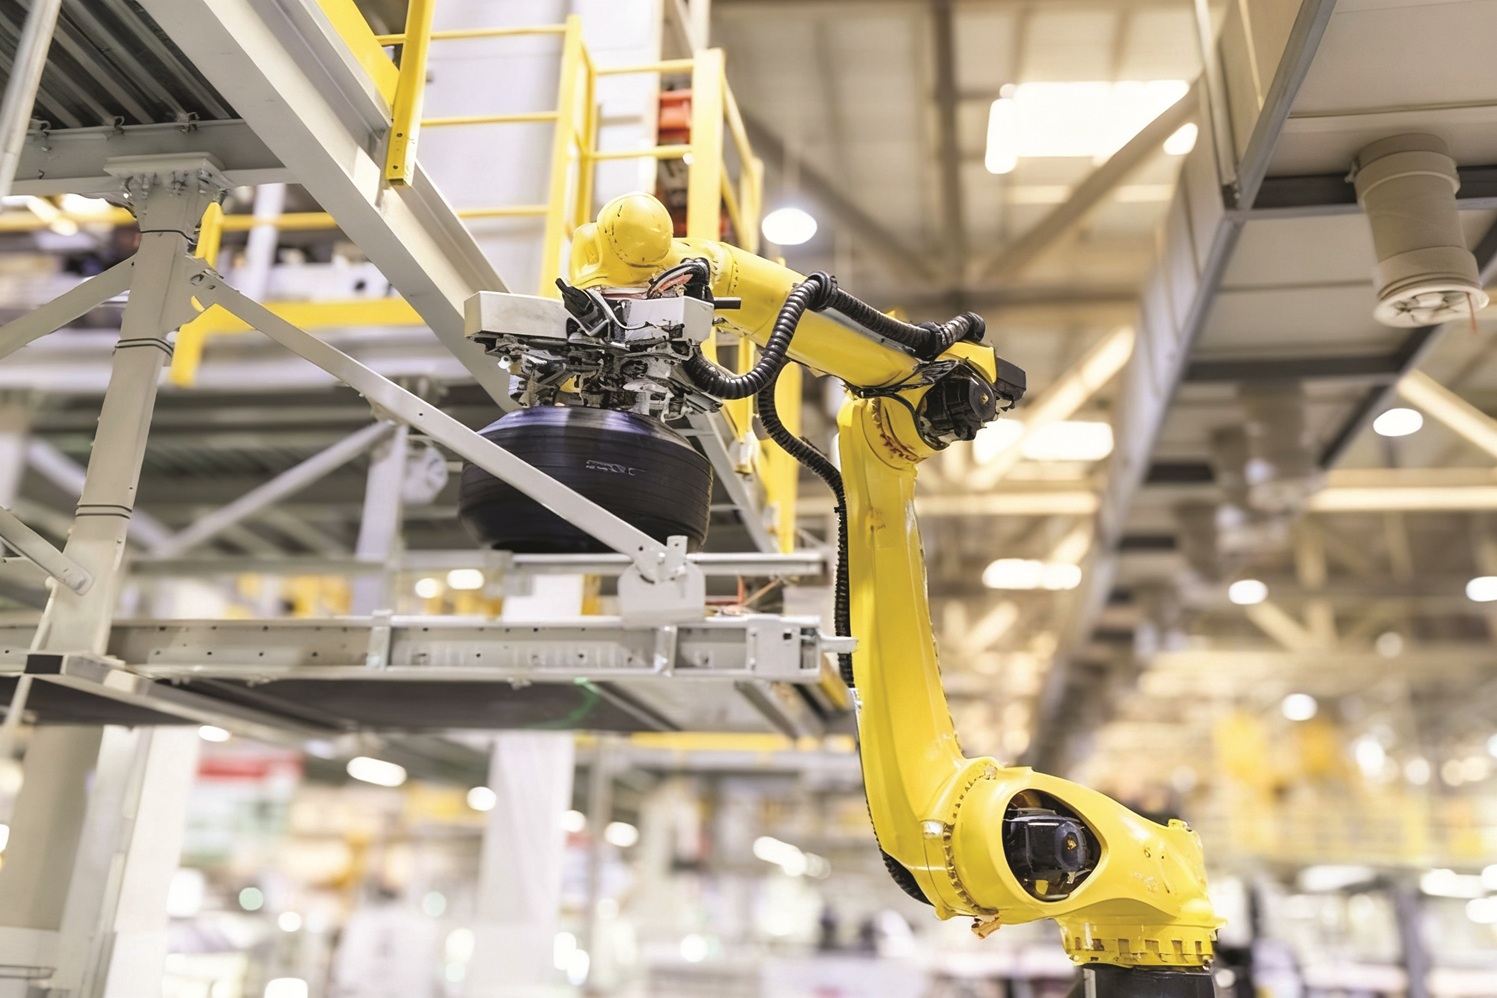
The current numbers, for the 5G Smart Factory, are a 50 percent improvement in production efficiency, defect rates down from 1.2 percent to 0.5 percent and a 10 percent reduction in overall energy consumption.
As for which technology deserves the credit, ZC Rubber declines to rank them. “We do not break down the improvement by individual technology,” it said, naming instead the key components: AI-based process control, automated inspection, intelligent logistics, APS+MES production management and data-driven quality control.
ENERGY, MEASURED VALVE BY VALVE
The energy figure is worth a closer look, because it comes from a fairly granular system. ZC Rubber’s energy management combines 5G, IoT, big data, AI and digital-twin technologies. Smart sensors, smart meters and smart valves feed real-time data into a central energy platform, while AI supports analysis and operational optimisation.
The division of labour among the technologies is neat. “5G provides the connectivity, while AI, big data and digital twins help turn the data into better energy-management decisions,” the company said.
TWO PLATFORMS AND A DIFFERENT STARTING POINT
The manufacturing story is inseparable from the development story. ZC Rubber runs two proprietary technology platforms: the X-Tech System, primarily for truck and bus radial (TBR) tyres, and the Phecda Tech System, primarily for PCR tyres. Each integrates compound formulation, tyre structure, process engineering, simulation, testing and intelligent manufacturing within a single development framework.
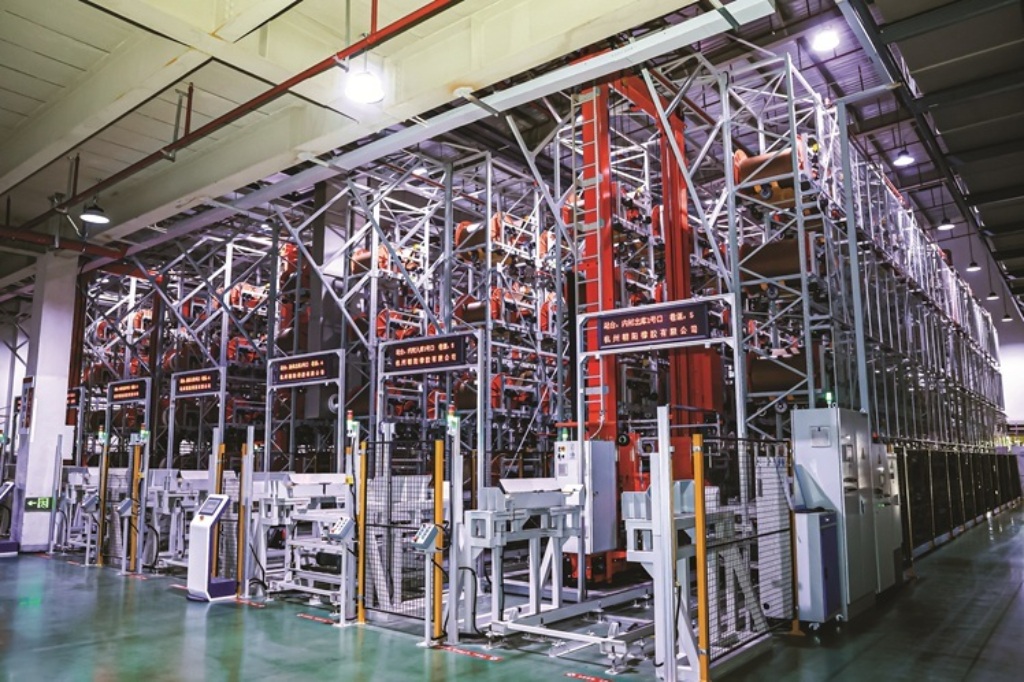
Their defining feature is what the company calls the Forward-development Approach. Traditional development, it explains, “often starts from an existing product and improves it through repeated design and testing cycles”. ZC Rubber starts elsewhere: with the target performance, whether that is vehicle characteristics, duty cycle, climate, road conditions or customer requirements. The compound, tyre structure and manufacturing process are then built around those targets. “This shifts the workflow from repeated iteration to a more integrated, target-driven development process,” the company said.
That, it argues, is where the halving of development time comes from. The 50 percent reduction reflects ‘a more integrated digital development process’, combining engineering expertise with simulation, AI-assisted tools and closer links between R&D, testing and manufacturing. AI lets engineers evaluate more design options against defined performance targets, and virtual simulation cuts out unnecessary physical iterations.
How tightly these platforms are wired into live production data has not been shared publicly. X-Tech and Phecda, the company said, connect R&D, manufacturing and validation within an integrated development process, but the detailed real-time data architecture behind them ‘is not something we currently disclose publicly’.
Henry Shen, ZC Rubber’s Senior Vice President, has made the wider point in the context of the group’s recent State recognition. “Our objective is not simply to develop an individual material, tread pattern or manufacturing process,” he said. “X-Tech and Phecda are complete development systems that connect user requirements with simulation, materials, tyre engineering, manufacturing and validation.”
THE STATE PRIZE
That recognition is significant. ZC Rubber, together with Harbin Institute of Technology, has been awarded the Second Prize of China’s State Science and Technology Progress Award for a project titled ‘Key Technologies and Green Intelligent Manufacturing of High-Performance Tires’. It is one of the country’s highest state-level honours for scientific and technological innovation, and ZC Rubber says it is the only Chinese tyre manufacturer in the past decade to win it at the Second Prize level or above.
The company backs the claim with spending. In 2025, it invested around RMB 1.54 billion (approximately USD 226 million in R&D, equal to 3.43 percent of annual revenue, according to its annual report. The award, it says, recognises technologies that have ‘progressed beyond laboratory research into industrial application’.
GLOBAL FOOTPRINT
ZC Rubber has built a truly global footprint, combining a strong manufacturing base in China with an expanding network of operations across Europe, the Americas, Southeast Asia and beyond. In China, the company operates through multiple sites, including its headquartered in Hangzhou and facilities in Tianjin, Chaoyang, Jiande, Qingquan, Yonggu, Anji and Jintan, supported by dedicated units for recycling technology and automotive aftermarket services in Hangzhou.
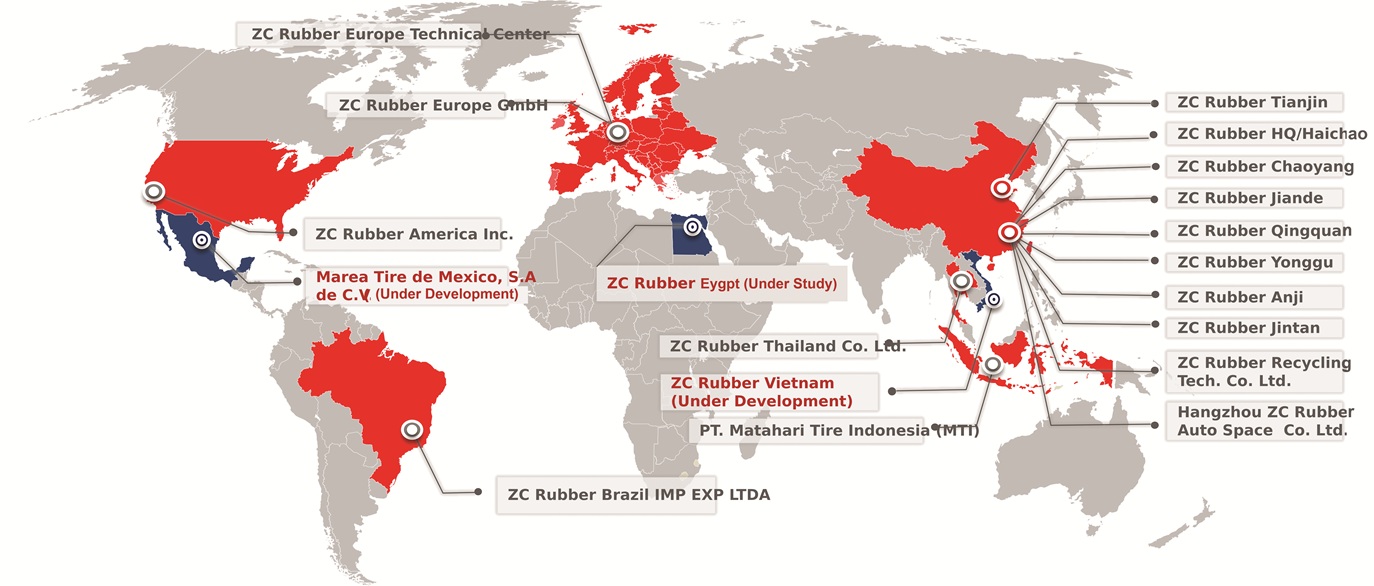
Beyond China, ZC Rubber has established a European presence through ZC Rubber Europe GmbH and its Europe Technical Center, alongside ZC Rubber America Inc. in the United States, ZC Rubber Brazil IMP EXP LTDA in South America and ZC Rubber Thailand Co. Ltd. and PT. Matahari Tire Indonesia (MTI) in Southeast Asia.
The company is also preparing for further expansion, with new projects under development in Vietnam and Mexico (Marea Tire de Mexico, S.A. de C.V.) and a feasibility study underway in Egypt. Together, these locations allow ZC Rubber to serve customers closer to their markets, strengthen supply chain resilience and combine local insight with global technical expertise.
CUSTOMISATION WITHOUT THE PENALTY
The forward-development model has a commercial payoff: tyres tailored to where and how they will be used. Asked whether the platforms allow genuine mass customisation, including regional climates and EV-specific requirements, ZC Rubber answered ‘to a significant degree’.
“X-Tech and Phecda allow us to develop tyres around specific climates, road conditions, vehicle applications and performance targets, including EV-specific requirements,” it said. On the factory floor, flexible production lines adjust output as product mix and orders change. The company does not disclose a separate efficiency figure for customised production, though ‘the goal is clear: to increase product flexibility while keeping production efficient’.
The regional examples are concrete. In Asia, X-Tech underpins the X-Elite Truck Tyre Series. In Europe, it is applied to the WESTLAKE Gen II commercial lineup, with a focus on fleet efficiency, performance and regulatory requirements. Phecda sits behind the WESTLAKE ZuperAce Z-007 and GOODRIDE Solmax 1 passenger tyres, and technologies from both platforms have been applied across ARISUN’s full TBR and PCR ranges for the Americas.
“International markets do not have identical requirements,” Shen said. “A tyre developed for European highway fleets, Southeast Asian transport operations or passenger vehicles in the Americas must respond to different vehicles, roads, climates and customer priorities.”
WHAT COMES NEXT
Much of the technology commonly billed as next-generation is already in service at ZC Rubber. Automated logistics, AI-based visual inspection, process optimisation, digital simulation and virtual testing are all in use. Digital twins are applied in areas such as energy management, and a broader digital-twin virtual factory is part of the next-stage plan.
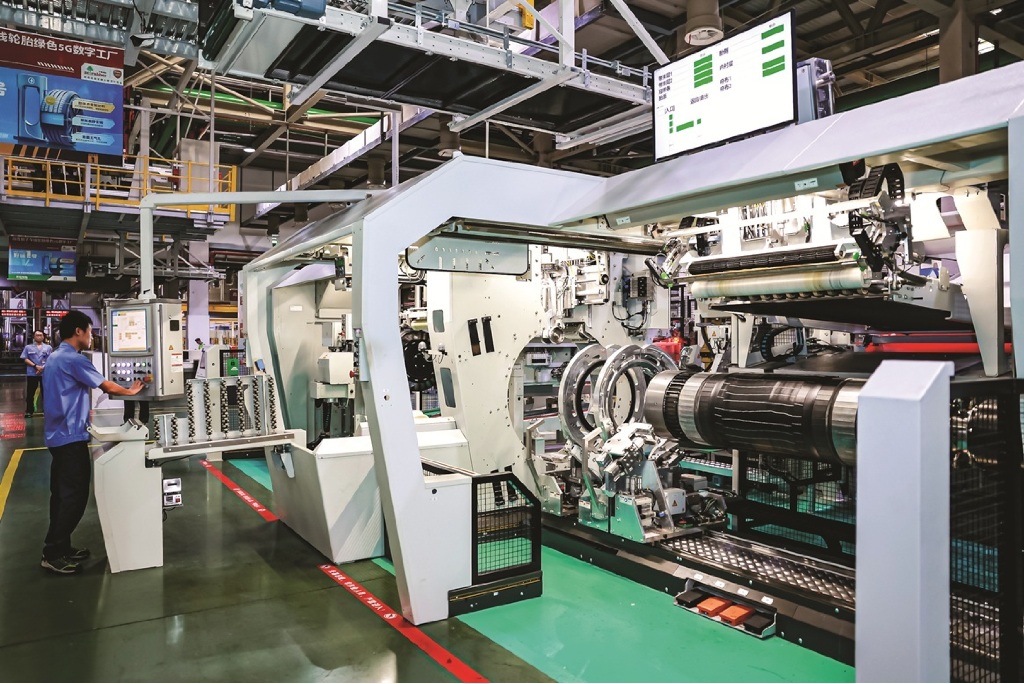 The company frames the coming three years as a period of deepening rather than reinvention: more smart-factory applications, more AI and industry-specific models and close attention to emerging technologies such as humanoid robotics ‘as they mature’.
That phrasing may be the most revealing thing about ZC Rubber’s approach. It is chasing results rather than headlines. As the company itself puts it, the launch of the Hangzhou plant marks ‘a new opportunity and starting point’, and its stated ambition is to become a world-leading tyre company with higher standards. Whether the lights stay on, it seems, is the least of its concerns.
AMETEK Completes USD 5bn Acquisition Of Indicor Instrumentation Businesses
- By TT Bureau
- October 12, 2026
AMETEK recently completed its USD 5- billion all-cash acquisition of a portfolio of instrumentation businesses from Indicor.
The businesses, collectively known as Indicor Instrumentation, make equipment for industrial and scientific applications. Their products serve markets that overlap with AMETEK’s existing operations and generate recurring revenue from consumables, services and aftermarket support.
David A Zapico, AMETEK’s Chairman and Chief Executive, said: “We are excited to complete this highly strategic acquisition and to welcome the Indicor Instrumentation team to AMETEK. With its mission-critical solutions, deep technical expertise, and strong positions in attractive end markets, Indicor Instrumentation is an excellent fit with AMETEK. We also see meaningful opportunities to create value through integration into our proven operating model.”
Indicor Instrumentation is expected to contribute about USD 350 million to AMETEK’s sales in 2026 and to be modestly accretive to adjusted earnings for the year.
The acquired businesses will join AMETEK’s Electronic Instruments Group and Electromechanical Group, according to their products and market focus.
The Goodyear Tire & Rubber Company has elected Joe Hinrichs as chairman of its Board of Directors, effective 7 October 2026. He will also chair the board's Governance and Executive Committees. Hinrichs joined the board in 2023 and succeeds Laurette Koellner, who will retire at the 2027 annual meeting under Goodyear's Corporate Governance Guidelines.
Hinrichs most recently served as President and Chief Executive Officer of CSX Corporation. Before that, he held numerous leadership roles at Ford Motor Company, including President of the Global Automotive Business, Executive Vice President and President of Global Operations, Executive Vice President and President of the Americas, President of Asia Pacific and Africa, and Chairman and Chief Executive Officer of Ford China. He also led Ford Canada. Hinrichs holds a bachelor's degree in electrical engineering from the University of Dayton and an MBA from Harvard Business School.
Koellner previously held several leadership roles at The Boeing Company. She joined Goodyear's board in 2015, became independent Lead Director in 2019, and Non-Executive Chairman in 2024.
Hinrichs said, "I would like to recognise and thank Laurette for her leadership, dedication and unwavering commitment to Goodyear. On behalf of the Board, we are grateful for her many contributions throughout her more than a decade of service. I look forward to working alongside my fellow board members and the leadership team as we continue to innovate, strengthen our competitive position, create long-term value for our shareholders and build a stronger Goodyear."
CEAT Specialty’s Off-Highway Tyre Playbook
- By Sharad Matade
- October 09, 2026
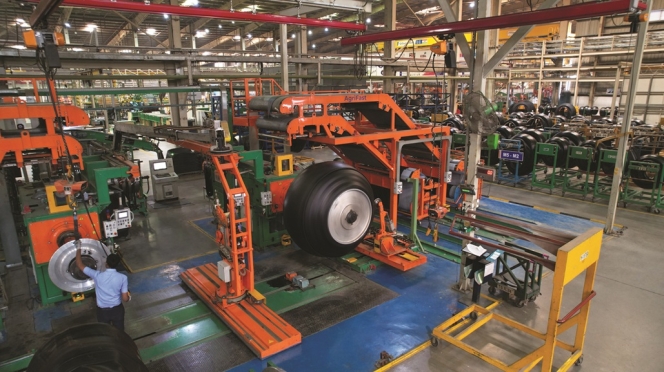
CEAT’s Chennai and Halol plants are the only tyre facilities globally with two WEF Global Lighthouse Network inductions, and the company has also won the Deming Grand Prize for manufacturing excellence.
Yet 30 km from Mumbai, CEAT Specialty’s 49-acre Ambernath plant tells a different story: tyres too heavy for automation, built instead around nitrogen curing, induction presses and orders as small as one unit – a bet that sustainability will win markets in Europe and America.
The stakes: an INR 5 billion investment in all-steel radial technology, capacity expansion to 160 tonnes/day and a Camso manufacturing deal Tolani pegs at up to USD 1 billion – turning a manufacturing constraint into a competitive edge.
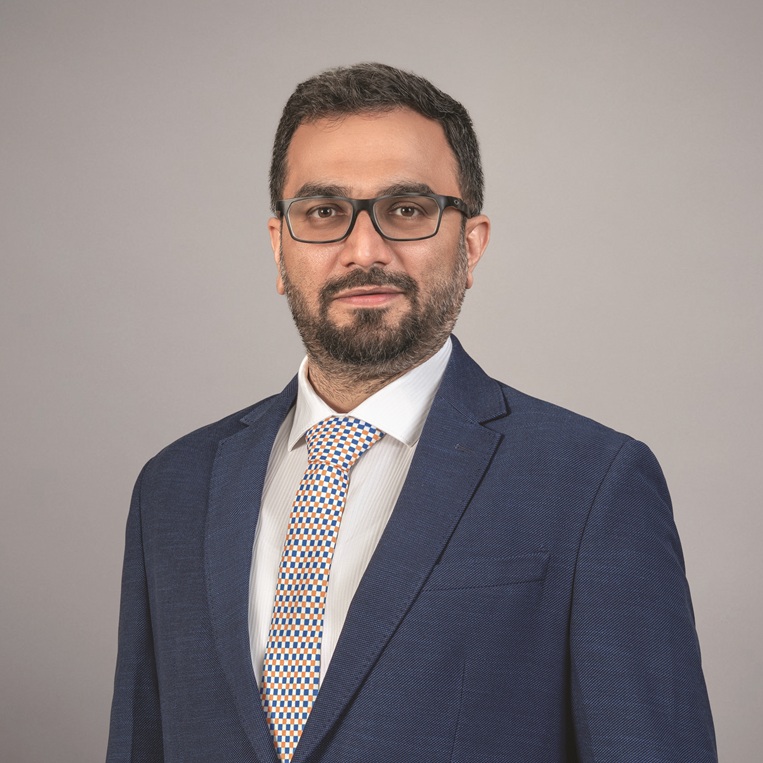
Amit Tolani, Chief Executive of CEAT Specialty, does not talk about tyres the way most executives talk about their products. He talks about them the way an engineer talks about a puzzle that keeps changing shape. “The way to look at it is that the manufacturing processes that we follow – how modern they are, how capable they are, how technically efficient – that’s what matters,” he says, sitting inside the plant that has become the nerve centre of CEAT’s off-highway tyre (OHT) business.
That plant – the Ambernath facility, a division of Mumbai-headquartered RPG Group’s CEAT Limited – is not a conventional tyre factory. It builds tyres that can weigh up to over 600 kilogrammes, tyres too large and too heavy for the automation that has transformed the passenger-car tyre business. And it is this constraint, as much as any strategic masterplan, that has shaped how CEAT Specialty has chosen to compete.
A PLANT THAT CANNOT SIMPLY COPY THE ROBOTS
Ask Tolani why Ambernath has not adopted the wall-to-wall robotic automation seen at CEAT’s Chennai or Halol facility, and the answer is refreshingly unglamorous: physics. “PCR tyres can be lifted by an ordinary human being, or a forklift, or robots,” he explains. “For these tyres, which are 600–700 kg, it’s very difficult to have a conveyor that can just lift them.” In the processes that do lend themselves to automation – mixing, calendering, curing – Ambernath’s equipment, he insists, is ‘as modern as the Chennai plant. More modern’. The plant intends to formalise that claim in the coming months by pursuing Industry 4.0 certification.
Where the physical limits of scale end, digital ones have taken over. A SCADA system tracks steam lines running beneath the plant floor. Where a leak once required a worker to walk the line, take manual temperature readings and diagnose the fault, artificial intelligence now flags the location almost instantly. “The point time taken to identify the problem is close to zero,” Tolani says. Every tyre carries a digital identity from raw material to finished good; a single scan reveals the batch, the machine, the operator and the timestamp behind it. AI is also being trained on the plant’s visual tyre inspection – traditionally a human, eyeball-driven task – using high-resolution cameras to catch defects, and on optimising mixing recipes and cycle times, the invisible chemistry that determines how a tyre performs in a paddy field or a quarry.
CURING WITHOUT STEAM
The most technically striking claim to emerge from Ambernath concerns curing – the energy-intensive process of vulcanising rubber under heat and pressure that has, for a century, meant steam. “This plant has already started using nitrogen curing on one of the lines,” Tolani says. Alongside it sit two proof-of-concept induction curing presses – a steam-free process, while the nitrogen conversion has come via LMT. “There are two presses that are already commissioned here,” he says. “We’ve already started working in that direction, where we want to take a lead in this space.”
The bulk of the plant’s newest investment, however, is going into something more conventional in principle but strategically significant in intent: all-steel radial off-the-road tyres. CEAT Specialty has committed INR 5 billion to this latest phase of expansion, representing a decisive shift in product architecture. Where a car’s tyres are universally radial, only 60–70 percent of truck tyres have made that transition, and agricultural and OTR applications lag further still – agriculture because usage is seasonal, OTR because a fabric-belted bias tyre still does much of the heavy lifting. All-steel radial construction changes that calculus by delivering higher load-carrying capacity and greater comfort, attributes increasingly demanded not only by Indian buyers but, crucially, by European and American customers. “It’s for demand from the European market, the US market – and the Indian market is also growing in such a handsome fashion that we want to cater to it,” Tolani says.
LEAN BY DESIGN, NOT BY SLOGAN
CEAT’s manufacturing philosophy is inseparable from its most prized accolade: in 2017, CEAT became the first tyre company outside Japan to win the Deming Prize, the world’s most prestigious award for total quality management; in 2023, it became the first tyre company anywhere to win the Deming Grand Prize, a distinction held by only 33 organisations globally as of 2025. Inside CEAT, this discipline is branded QBM – Quality Based Management – a homegrown fusion of Total Quality Management, the Toyota Production System and Total Productive Maintenance.
“We are a Deming Grand organisation. That means we follow the philosophy of lean manufacturing – not to use resources or have any wastage in the process,” Tolani says. That philosophy is embedded, quite literally, in the plant’s straight-flow layout, which runs from raw material storage through mixing, stock preparation, tyre building, curing and final finish in a single unbroken line. Even small batch sizes, he says, are produced without the wastage, excess labour or lost efficiency – what the plant’s internal vocabulary calls ‘Muri’ – that might otherwise creep in.
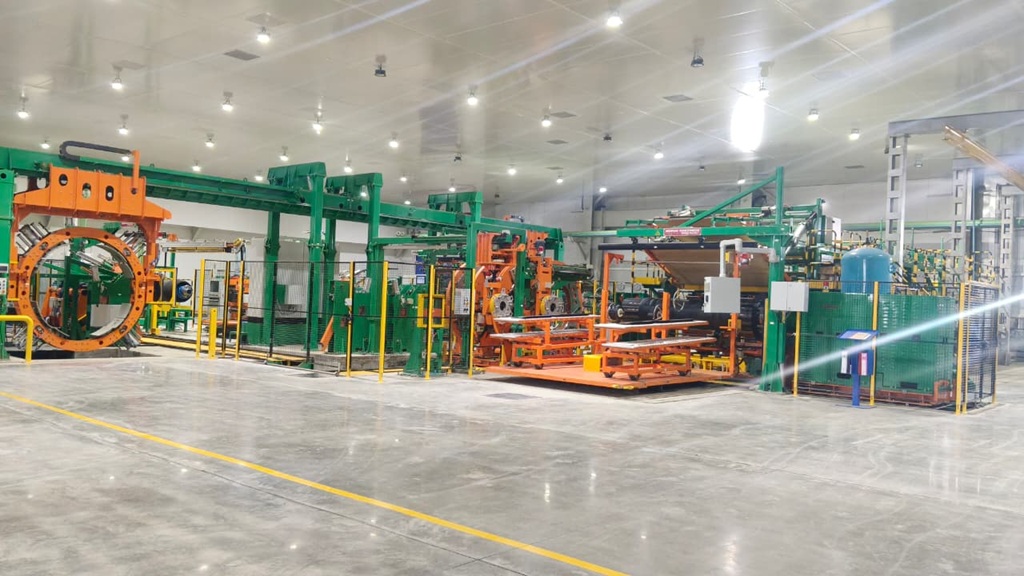
That same lean instinct underpins one of Ambernath’s more unusual competitive claims: a minimum order quantity of one. In an industry historically built around economies of scale, the plant will build a single speciality tyre to a customer’s specification without demanding batch aggregation – a capability the company says few OHT plants worldwide can match. Self-managed teams on the shop floor plan and execute changeovers themselves, allowing a highly automated, digitally traceable line to pivot rapidly to low-volume, customised orders. A related innovation, branded Unistage, builds and shapes an agricultural or OTR radial carcass into its final toroidal form on a single drum rather than the conventional two-stage process, reducing the handovers.
AN R&D CENTRE BUILT FOR SPEED, NOT SCALE
CEAT Specialty operates a dedicated in-house research and development facility at Ambernath, distinct from the group’s broader R&D infrastructure, and Tolani is candid about why. Tolani says, “This business is very, very different. There is no Pareto here – no 80/20 rule where a handful of product sizes serve the bulk of demand. Because farm and off-highway equipment come in such a long tail of sizes and configurations, and because the plant supplies numerous international OEMs directly, the time taken to develop, validate and commercialise a new tyre has to be compressed.”
“We needed a dedicated facility, closer to the manufacturing, so that we can quickly pilot, quickly turn around,” he adds. A new Compound Laboratory, opened in September 2025, now anchors materials science work spanning OTR, agricultural and industrial segments, while AI-assisted testing has trimmed, by Tolani’s estimate, roughly a third off the time from concept to market. The centre’s pipeline currently spans all-steel OTR tyres, a newly launched forestry range, very high flexion (VF) agricultural tyres and expanding work in earthmoving and material handling.
CAMSO ACQUIRED FOR BRAND, CHANNEL AND CATEGORY
CEAT Specialty’s move into Camso – a name Tolani values at up to USD 1 billion in brand potential across agricultural tracks, power sport tracks and material handling – may be its most consequential strategic bet. “It was a natural fit for us in terms of completing our portfolio,” he says. Ambernath, built in 2018 solely for agricultural radial tyres, gains through Camso’s new OEM ties (Massey Ferguson, John Deere) and construction-channel access across South America and Europe.
Under a three-year Michelin agreement, CEAT can currently manufacture and sell only compact construction tyres and tracks under Camso, taking over end-consumer sales in that segment – with other categories opening up once the term ends. The impact is already visible: standalone, CEAT Specialty’s off-highway mix is 85:15 agriculture to non-agriculture; with Camso’s, it shifts toward 50:50.
THE NUMBERS BEHIND THE AMBITION
Ambernath is running at 105 tonnes a day, at 92–95 percent utilisation – ahead of schedule. A further phase, due within 45 to 60 days, will lift capacity to 160 tonnes. Camso, still integrating, runs at roughly 50 percent.
Off-highway tyres make up close to 20 percent of CEAT’s speciality revenue, with the agriculture-to-non-agriculture split narrowing from 85:15 to near 50:50 once Camso is included. Domestically, Tolani credits GST reforms for a strong OEM market, led by Mahindra and TAFE, while mining stays flat – a segment Camso’s construction heritage should help lift as the new all-steel OTR line comes online.
Comments (0)
ADD COMMENT